显示标签为“inductionheatingsystem”的博文。显示所有博文

2024年4月28日星期日

Is induction heating cheaper than gas heating?

The cost-effectiveness of induction heating compared to gas heating depends on various factors, including the application, local energy prices, efficiency rates, and initial setup costs. As of my last update in 2024, here's how the two compare in general terms:

Efficiency and Operating Costs

  • Induction Heating: Induction heating is highly efficient because it directly heats the object using electromagnetic fields, with minimal heat loss to the surrounding environment. This direct method of heating often results in quicker heating times compared to gas heating. Since it uses electricity, its cost will depend on local electricity rates, which can vary widely around the world.
  • Gas Heating: Gas heating, which often involves combustion to produce heat, can be less efficient due to heat loss through exhaust gases and the surrounding environment. However, natural gas is typically cheaper per unit of energy produced than electricity in many regions, which can offset the efficiency differences and make gas heating cheaper in operational costs in those areas.
Setup and Maintenance Costs

  • Induction Heating: The upfront cost for induction heating equipment can be higher than conventional gas heating setups. Induction heaters also require a supply of electricity, which might necessitate upgrades to the electrical system in some instances. On the maintenance side, induction systems generally have fewer moving parts and do not combust fuel, potentially leading to lower maintenance costs over time.
  • Gas Heating: Initial setup for gas heating can be lower, especially if the infrastructure for gas is already in place. However, maintenance might be more demanding and costly due to the combustion process and the requirement for venting exhaust gases, checking for leaks in the gas supply, and regular cleaning of combustion chambers.

Environmental Considerations

While not directly related to cost, environmental impact is an increasingly important consideration. Induction heating produces no direct emissions at the point of use, making it a cleaner option if the electricity is sourced from renewable or low-emission sources. Gas heating involves the combustion of fossil fuels, leading to CO2 and potentially other harmful emissions, although advances in technology and the use of biogas can mitigate this impact somewhat.

Conclusion

Whether induction heating is cheaper than gas heating is highly contextual. For areas with low electricity costs, especially where those costs are lower due to a high proportion of renewable energy sources, induction heating can be more cost-effective in the long run, factoring in its higher efficiency and potentially lower maintenance costs. In regions where natural gas is cheap and electricity is expensive, gas heating might be the more economical choice, at least in terms of operating costs. It's also crucial to consider the specific application (e.g., industrial, commercial, or residential), as the scale and nature of the heating requirements can significantly influence which method is more cost-effective.
https://dw-inductionheater.com/is-induction-heating-cheaper-than-gas-heating.html?feed_id=243558&_unique_id=662ec95e84232

Is induction heating cheaper than gas heating?

The cost-effectiveness of induction heating compared to gas heating depends on various factors, including the application, local energy prices, efficiency rates, and initial setup costs. As of my last update in 2024, here's how the two compare in general terms:

Efficiency and Operating Costs

  • Induction Heating: Induction heating is highly efficient because it directly heats the object using electromagnetic fields, with minimal heat loss to the surrounding environment. This direct method of heating often results in quicker heating times compared to gas heating. Since it uses electricity, its cost will depend on local electricity rates, which can vary widely around the world.
  • Gas Heating: Gas heating, which often involves combustion to produce heat, can be less efficient due to heat loss through exhaust gases and the surrounding environment. However, natural gas is typically cheaper per unit of energy produced than electricity in many regions, which can offset the efficiency differences and make gas heating cheaper in operational costs in those areas.

Setup and Maintenance Costs

  • Induction Heating: The upfront cost for induction heating equipment can be higher than conventional gas heating setups. Induction heaters also require a supply of electricity, which might necessitate upgrades to the electrical system in some instances. On the maintenance side, induction systems generally have fewer moving parts and do not combust fuel, potentially leading to lower maintenance costs over time.
  • Gas Heating: Initial setup for gas heating can be lower, especially if the infrastructure for gas is already in place. However, maintenance might be more demanding and costly due to the combustion process and the requirement for venting exhaust gases, checking for leaks in the gas supply, and regular cleaning of combustion chambers.
Environmental Considerations

While not directly related to cost, environmental impact is an increasingly important consideration. Induction heating produces no direct emissions at the point of use, making it a cleaner option if the electricity is sourced from renewable or low-emission sources. Gas heating involves the combustion of fossil fuels, leading to CO2 and potentially other harmful emissions, although advances in technology and the use of biogas can mitigate this impact somewhat.

Conclusion

Whether induction heating is cheaper than gas heating is highly contextual. For areas with low electricity costs, especially where those costs are lower due to a high proportion of renewable energy sources, induction heating can be more cost-effective in the long run, factoring in its higher efficiency and potentially lower maintenance costs. In regions where natural gas is cheap and electricity is expensive, gas heating might be the more economical choice, at least in terms of operating costs. It's also crucial to consider the specific application (e.g., industrial, commercial, or residential), as the scale and nature of the heating requirements can significantly influence which method is more cost-effective.
https://dw-inductionheater.com/is-induction-heating-cheaper-than-gas-heating.html?feed_id=243456&_unique_id=662e533363f2c

2024年2月8日星期四

Induction Heating System Topology Review

Induction Heating System Topology Review

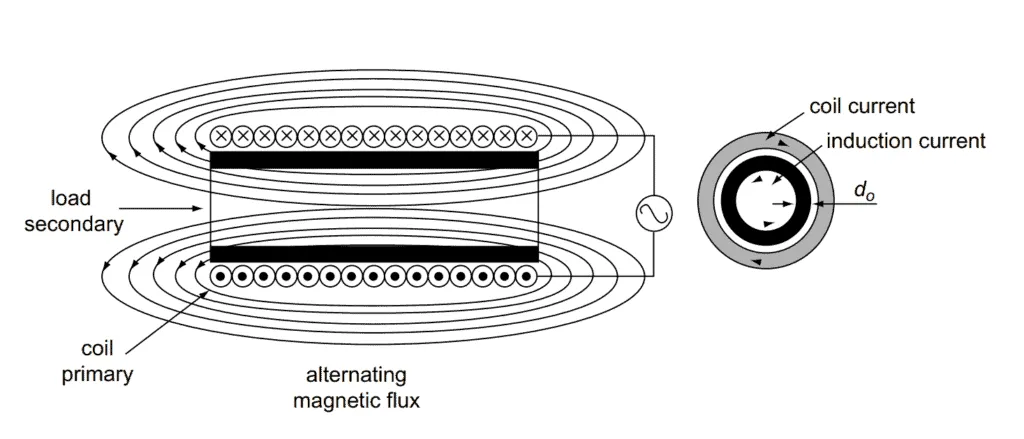
[caption id="attachment_7044" align="alignnone" width="1024"] Induction Heating System Topology Review[/caption] All induction heating systhems are developed using electromagnetic induction which was first discovered by Michael Faraday in 1831. Electromagnetic induction refers to the phenomenon by which electric current is generated in a closed circuit by the fluctuation of current in another circuit placed next to it. The basic principle of induction heating, which is an applied form of Faraday’s discovery, is the fact that AC current flowing through a circuit affects the magnetic movement of a secondary circuit located near it. The fluctuation of current inside the primary circuit provided the answer as to how the mysterious current is generated in the neighboring secondary circuit. Faraday’s discovery led to the development of electric motors, generators, transformers, and wireless communications devices. Its application, however, has not been flawless. Heat loss, which occurs during the induction heating process, was a major headache undermining the overall functionality of a system. Researchers sought to minimize heat loss by laminating the magnetic frames placed inside the motor or transformer. Faraday’s Law was followed by a series of more advanced discoveries such as Lentz’s Law. This law explains the fact that inductive current flows inverse to the direction of changes in induction magnetic movement. Induction Heating System Topology Review https://dw-inductionheater.com/induction-heating-system-topology-review.html?feed_id=233686&_unique_id=65c4c4ce13df2

2024年1月28日星期日

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe

This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: HLQ 30kw air cooled induction heater Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods. https://dw-inductionheater.com/induction-preheating-before-welding-steel-pipe.html?feed_id=233086&_unique_id=65b67c835eaf5

2023年6月16日星期五

Induction Heating System Topology Review

Induction Heating System Topology Review

[caption id="attachment_7044" align="alignnone" width="1024"] Induction Heating System Topology Review[/caption] All induction heating systhems are developed using electromagnetic induction which was first discovered by Michael Faraday in 1831. Electromagnetic induction refers to the phenomenon by which electric current is generated in a closed circuit by the fluctuation of current in another circuit placed next to it. The basic principle of induction heating, which is an applied form of Faraday’s discovery, is the fact that AC current flowing through a circuit affects the magnetic movement of a secondary circuit located near it. The fluctuation of current inside the primary circuit provided the answer as to how the mysterious current is generated in the neighboring secondary circuit. Faraday’s discovery led to the development of electric motors, generators, transformers, and wireless communications devices. Its application, however, has not been flawless. Heat loss, which occurs during the induction heating process, was a major headache undermining the overall functionality of a system. Researchers sought to minimize heat loss by laminating the magnetic frames placed inside the motor or transformer. Faraday’s Law was followed by a series of more advanced discoveries such as Lentz’s Law. This law explains the fact that inductive current flows inverse to the direction of changes in induction magnetic movement. Induction Heating System Topology Review https://dw-inductionheater.com/induction-heating-system-topology-review.html?feed_id=213736&_unique_id=648d4a17115ca

2023年6月6日星期二

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe

This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: HLQ 30kw air cooled induction heater Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods. https://dw-inductionheater.com/induction-preheating-before-welding-steel-pipe.html?feed_id=210811&_unique_id=647efedc6922b

2023年5月26日星期五

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe

This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: HLQ 30kw air cooled induction heater Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods. https://dw-inductionheater.com/induction-preheating-before-welding-steel-pipe.html?feed_id=208111&_unique_id=6471323642641

2023年5月3日星期三

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe

This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: HLQ 30kw air cooled induction heater Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods.

2023年4月30日星期日

Induction Heating System Topology Review

Induction Heating System Topology Review

[caption id="attachment_7044" align="alignnone" width="1024"] Induction Heating System Topology Review[/caption] All induction heating systhems are developed using electromagnetic induction which was first discovered by Michael Faraday in 1831. Electromagnetic induction refers to the phenomenon by which electric current is generated in a closed circuit by the fluctuation of current in another circuit placed next to it. The basic principle of induction heating, which is an applied form of Faraday’s discovery, is the fact that AC current flowing through a circuit affects the magnetic movement of a secondary circuit located near it. The fluctuation of current inside the primary circuit provided the answer as to how the mysterious current is generated in the neighboring secondary circuit. Faraday’s discovery led to the development of electric motors, generators, transformers, and wireless communications devices. Its application, however, has not been flawless. Heat loss, which occurs during the induction heating process, was a major headache undermining the overall functionality of a system. Researchers sought to minimize heat loss by laminating the magnetic frames placed inside the motor or transformer. Faraday’s Law was followed by a series of more advanced discoveries such as Lentz’s Law. This law explains the fact that inductive current flows inverse to the direction of changes in induction magnetic movement. Induction Heating System Topology Review

2023年4月10日星期一

Induction Heating System Topology Review

Induction Heating System Topology Review

[caption id="attachment_7044" align="alignnone" width="1024"] Induction Heating System Topology Review[/caption] All induction heating systhems are developed using electromagnetic induction which was first discovered by Michael Faraday in 1831. Electromagnetic induction refers to the phenomenon by which electric current is generated in a closed circuit by the fluctuation of current in another circuit placed next to it. The basic principle of induction heating, which is an applied form of Faraday’s discovery, is the fact that AC current flowing through a circuit affects the magnetic movement of a secondary circuit located near it. The fluctuation of current inside the primary circuit provided the answer as to how the mysterious current is generated in the neighboring secondary circuit. Faraday’s discovery led to the development of electric motors, generators, transformers, and wireless communications devices. Its application, however, has not been flawless. Heat loss, which occurs during the induction heating process, was a major headache undermining the overall functionality of a system. Researchers sought to minimize heat loss by laminating the magnetic frames placed inside the motor or transformer. Faraday’s Law was followed by a series of more advanced discoveries such as Lentz’s Law. This law explains the fact that inductive current flows inverse to the direction of changes in induction magnetic movement. Induction Heating System Topology Review

2023年2月15日星期三

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe


This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint.


Industry: Manufacturing

Equipment: HLQ 30kw air cooled induction heater

Time: 300 secs.

Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F)

Materials: Steel pipe

Details for butt-welded steel pipe:
Total length: 300 mm (11.8 inch)
DIA: 152.40 mm (5.9 inch)
Thickness: 18.26 mm (0.71 inch)
Heating length: 30-45 mm from middle (1.1 – 1.7 inch)

Details for butt welded steel plate.
Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch)
Thickness: 10 mm (0.39 inch)
Heating length: 20-30 mm (0.7-1.1 inch) from middle.

Fixture details for butt welded steel pipe:
Material: Mica.
Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch)
Thickness: 20 mm (0.7 inch)
Withstands temperature of 900 °C (1652°F)


Process:

We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses.

Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods.

2023年2月2日星期四

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe

This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: HLQ 30kw air cooled induction heater Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods.

2022年12月22日星期四

Induction Heating System Topology Review

Induction Heating System Topology Review

[caption id="attachment_7044" align="alignnone" width="1024"] Induction Heating System Topology Review[/caption] All induction heating systhems are developed using electromagnetic induction which was first discovered by Michael Faraday in 1831. Electromagnetic induction refers to the phenomenon by which electric current is generated in a closed circuit by the fluctuation of current in another circuit placed next to it. The basic principle of induction heating, which is an applied form of Faraday’s discovery, is the fact that AC current flowing through a circuit affects the magnetic movement of a secondary circuit located near it. The fluctuation of current inside the primary circuit provided the answer as to how the mysterious current is generated in the neighboring secondary circuit. Faraday’s discovery led to the development of electric motors, generators, transformers, and wireless communications devices. Its application, however, has not been flawless. Heat loss, which occurs during the induction heating process, was a major headache undermining the overall functionality of a system. Researchers sought to minimize heat loss by laminating the magnetic frames placed inside the motor or transformer. Faraday’s Law was followed by a series of more advanced discoveries such as Lentz’s Law. This law explains the fact that inductive current flows inverse to the direction of changes in induction magnetic movement. Induction Heating System Topology Review

2022年11月17日星期四

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe

This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: HLQ 30kw air cooled induction heater Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods.

2022年10月7日星期五

Induction Heating System Topology Review

Induction Heating System Topology Review

[caption id="attachment_7044" align="alignnone" width="1024"] Induction Heating System Topology Review[/caption] All induction heating systhems are developed using electromagnetic induction which was first discovered by Michael Faraday in 1831. Electromagnetic induction refers to the phenomenon by which electric current is generated in a closed circuit by the fluctuation of current in another circuit placed next to it. The basic principle of induction heating, which is an applied form of Faraday’s discovery, is the fact that AC current flowing through a circuit affects the magnetic movement of a secondary circuit located near it. The fluctuation of current inside the primary circuit provided the answer as to how the mysterious current is generated in the neighboring secondary circuit. Faraday’s discovery led to the development of electric motors, generators, transformers, and wireless communications devices. Its application, however, has not been flawless. Heat loss, which occurs during the induction heating process, was a major headache undermining the overall functionality of a system. Researchers sought to minimize heat loss by laminating the magnetic frames placed inside the motor or transformer. Faraday’s Law was followed by a series of more advanced discoveries such as Lentz’s Law. This law explains the fact that inductive current flows inverse to the direction of changes in induction magnetic movement. Induction Heating System Topology Review

2022年8月31日星期三

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe

This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: HLQ 30kw air cooled induction heater Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods. https://dw-inductionheater.com/induction-preheating-before-welding-steel-pipe.html?feed_id=150452&_unique_id=630f56c49f7ba

2022年4月23日星期六

Ultraudio Frequency Induction Heating System

Ultraudio Frequency Induction Heating System

Ultraudio frequency induction heating systems can work at the power of 30^300KW and its frequency ranges from 10 to 30KHz. Wih its digital design control system.All the DW-URF series can display the working voltage, current, working frequency and indicate the error. Its compact design makes small installation space and flexible working environment available. As a professional induction heating machine manufacturer, HLQ has also applied the mature and reliable IGBT series resonant design into the design of the circuit of  URF series.  The maintenance of DW-URF series are convenient and simple. Any non-professional operator can handle it. Furthermore, the fast heating and high power features of DW-URF series have also made theirselves one of the most energy-saving heating methods compare with all the electric heating systems. The induction generators of ultraudio frequency induction heating systems allow the equipment of remote control systems according to customers' request for actual usages, such as  0-10V/4-20mA power control interface, RS485 and RS232. This machines can also work automatically under the external control system and are suitable for different applications such as billets heating, auto parts heat treatment. Main model and specifications
Model DW-URF-30A DW-URF-30ABS DW-URF-40ABS DW-URF-50ABS DW-URF-40AB DW-URF-50AB DW-URF-60AB
Max output power 30KW 30KW 40KW 50KW 40KW 50KW 60KW
frequency 10-40KHz 10-40KHz 10-40KHz 10-40KHz 10-40KHz 10-40KHz 10-40KHz
Max input current 48A 48A 62A 75A 62A 75A 90A
Working voltage 342-430V
Input voltage 3phase 380V 50HZ or 60HZ
Duty cycle 100%
Water flow 15L/min (0.2Mpa) 15L/min (0.2Mpa) 32L/min (0.2Mpa) 32L/min (0.2Mpa) 32L/min (0.2Mpa) 32L/min (0.2Mpa) 40L/min (0.2Mpa)
Generator weight 55KG 35KG 36KG 38KG 74KG 75KG 75KG
Transformer weight x 25KG 26KG 28KG 38KG 50KG 60KG
Generator size(mm) 600x300x610 600x300x610 600x300x610 600x300x610 670x460x830 670x460x830 670x460x830
Transformer Size(mm) x 420x320x330 420x320x330 420x320x330 410x405x390 410x405x390 470x450x465
 Size 690x400x730 670x660x730 670x660x730 670x660x730 1010x900x990 1010x900x990 1010x900x990
 Weight 79kg 92kg 95kg 99kg 176kg 185kg 195kg
 
Model DW-URF-80AB DW-URF-100AB DW-URF-120AB DW-URF-160AB DW-URF-200AB DW-URF-250AB DW-URF-300AB
Max output power 80KW 100KW 120KW 160KW 200KW 250KW 300KW
Frequency 10-40KHz 10-40KHz 10-40KHz 8-30KHz 8-30KHz 8-30KHz 8-30KHz
Max input current 125A 155A 185A 245A 310A 380A 455A
Working voltage 342-430V
Input voltage 3phase 380V 50HZ or 60HZ
Duty cycle 100%
Water flow 50L/min (0.2Mpa) 50L/min (0.2Mpa) 68L/min (0.2Mpa) 68L/min (0.2Mpa) 80L/min (0.2Mpa) 80L/min (0.2Mpa) 100L/min (0.2Mpa)
Generator weight 130KG 130KG 138KG 145KG 185KG 192KG 198KG
Transformer weight 86KG 86KG 95KG 101KG 116KG 123KG 126KG
Generator size(mm) 750x550x1065 750x550x1065 750x550x1165 750x550x1065 850x600x1850 850x600x1850 850x600x1850
Transformer Size(mm) 410x435x460 410x435x460 410x435x460 410x435x460 835x540x595 835x540x595 835x540x595
Size 1160x1040x1320 1160x1040x1320 1160x1040x1320 1160x1040x1320 1170x1040x2000 890x650x700 1170x1040x2000 890x650x700 1170x1040x2000 890x650x700
 Size 282kg 282kg 305kg 316kg 275kg 156kg 285kg 168kg 292kg 175kg
Main characteristics
  • IGBT inversion technology based LC series circuit.
  • Phase locking looping technology and soft switch ensure good reliability, realize power and frequency tracking automatically.
  • Diode rectifier cause high power factor more than 0.95
  • Working continuously with 100% duty cycle, power can be instantly turned on or shut off.
  • Perfect protective circuit and cooling system design, which ensure the good reliability of machine.
  • Low energy consumption: converts up to 97.5% above of the expended energy into useful heat. energy saving 15%-30% compared with SCR induction heating machine.
  • Environment friendly, clean, non-polluting process which will help protect the environment, improves working conditions for your employees by eliminating smoke, waste heat, noxious emissions and loud noise.
  • Operating and installation easily and safely
  • Can substitute traditional heating methods.
Application Rod forging, rod hardening. Bolt,nut forging Heat treatment of shaft, gear, pin, etc. Shrink-fitting Steel wire and pipe annealing Pipe bending. Brazing  

Ultraudio Frequency Induction Heating System

Ultraudio Frequency Induction Heating System

Ultraudio frequency induction heating systems can work at the power of 30^300KW and its frequency ranges from 10 to 30KHz. Wih its digital design control system.All the DW-URF series can display the working voltage, current, working frequency and indicate the error. Its compact design makes small installation space and flexible working environment available. As a professional induction heating machine manufacturer, HLQ has also applied the mature and reliable IGBT series resonant design into the design of the circuit of  URF series.  The maintenance of DW-URF series are convenient and simple. Any non-professional operator can handle it. Furthermore, the fast heating and high power features of DW-URF series have also made theirselves one of the most energy-saving heating methods compare with all the electric heating systems. The induction generators of ultraudio frequency induction heating systems allow the equipment of remote control systems according to customers' request for actual usages, such as  0-10V/4-20mA power control interface, RS485 and RS232. This machines can also work automatically under the external control system and are suitable for different applications such as billets heating, auto parts heat treatment. Main model and specifications
Model DW-URF-30A DW-URF-30ABS DW-URF-40ABS DW-URF-50ABS DW-URF-40AB DW-URF-50AB DW-URF-60AB
Max output power 30KW 30KW 40KW 50KW 40KW 50KW 60KW
frequency 10-40KHz 10-40KHz 10-40KHz 10-40KHz 10-40KHz 10-40KHz 10-40KHz
Max input current 48A 48A 62A 75A 62A 75A 90A
Working voltage 342-430V
Input voltage 3phase 380V 50HZ or 60HZ
Duty cycle 100%
Water flow 15L/min (0.2Mpa) 15L/min (0.2Mpa) 32L/min (0.2Mpa) 32L/min (0.2Mpa) 32L/min (0.2Mpa) 32L/min (0.2Mpa) 40L/min (0.2Mpa)
Generator weight 55KG 35KG 36KG 38KG 74KG 75KG 75KG
Transformer weight x 25KG 26KG 28KG 38KG 50KG 60KG
Generator size(mm) 600x300x610 600x300x610 600x300x610 600x300x610 670x460x830 670x460x830 670x460x830
Transformer Size(mm) x 420x320x330 420x320x330 420x320x330 410x405x390 410x405x390 470x450x465
 Size 690x400x730 670x660x730 670x660x730 670x660x730 1010x900x990 1010x900x990 1010x900x990
 Weight 79kg 92kg 95kg 99kg 176kg 185kg 195kg
 
Model DW-URF-80AB DW-URF-100AB DW-URF-120AB DW-URF-160AB DW-URF-200AB DW-URF-250AB DW-URF-300AB
Max output power 80KW 100KW 120KW 160KW 200KW 250KW 300KW
Frequency 10-40KHz 10-40KHz 10-40KHz 8-30KHz 8-30KHz 8-30KHz 8-30KHz
Max input current 125A 155A 185A 245A 310A 380A 455A
Working voltage 342-430V
Input voltage 3phase 380V 50HZ or 60HZ
Duty cycle 100%
Water flow 50L/min (0.2Mpa) 50L/min (0.2Mpa) 68L/min (0.2Mpa) 68L/min (0.2Mpa) 80L/min (0.2Mpa) 80L/min (0.2Mpa) 100L/min (0.2Mpa)
Generator weight 130KG 130KG 138KG 145KG 185KG 192KG 198KG
Transformer weight 86KG 86KG 95KG 101KG 116KG 123KG 126KG
Generator size(mm) 750x550x1065 750x550x1065 750x550x1165 750x550x1065 850x600x1850 850x600x1850 850x600x1850
Transformer Size(mm) 410x435x460 410x435x460 410x435x460 410x435x460 835x540x595 835x540x595 835x540x595
Size 1160x1040x1320 1160x1040x1320 1160x1040x1320 1160x1040x1320 1170x1040x2000 890x650x700 1170x1040x2000 890x650x700 1170x1040x2000 890x650x700
 Size 282kg 282kg 305kg 316kg 275kg 156kg 285kg 168kg 292kg 175kg
Main characteristics
  • IGBT inversion technology based LC series circuit.
  • Phase locking looping technology and soft switch ensure good reliability, realize power and frequency tracking automatically.
  • Diode rectifier cause high power factor more than 0.95
  • Working continuously with 100% duty cycle, power can be instantly turned on or shut off.
  • Perfect protective circuit and cooling system design, which ensure the good reliability of machine.
  • Low energy consumption: converts up to 97.5% above of the expended energy into useful heat. energy saving 15%-30% compared with SCR induction heating machine.
  • Environment friendly, clean, non-polluting process which will help protect the environment, improves working conditions for your employees by eliminating smoke, waste heat, noxious emissions and loud noise.
  • Operating and installation easily and safely
  • Can substitute traditional heating methods.
Application Rod forging, rod hardening. Bolt,nut forging Heat treatment of shaft, gear, pin, etc. Shrink-fitting Steel wire and pipe annealing Pipe bending. Brazing   https://dw-inductionheater.com/product/ultraudio-frequency-induction-heating-system?feed_id=114928&_unique_id=6263e2f5b5ddd

2022年4月2日星期六

Induction Heating System Topology Review

Induction Heating System Topology Review

[caption id="attachment_7044" align="alignnone" width="1024"] Induction Heating System Topology Review[/caption] All induction heating systhems are developed using electromagnetic induction which was first discovered by Michael Faraday in 1831. Electromagnetic induction refers to the phenomenon by which electric current is generated in a closed circuit by the fluctuation of current in another circuit placed next to it. The basic principle of induction heating, which is an applied form of Faraday’s discovery, is the fact that AC current flowing through a circuit affects the magnetic movement of a secondary circuit located near it. The fluctuation of current inside the primary circuit provided the answer as to how the mysterious current is generated in the neighboring secondary circuit. Faraday’s discovery led to the development of electric motors, generators, transformers, and wireless communications devices. Its application, however, has not been flawless. Heat loss, which occurs during the induction heating process, was a major headache undermining the overall functionality of a system. Researchers sought to minimize heat loss by laminating the magnetic frames placed inside the motor or transformer. Faraday’s Law was followed by a series of more advanced discoveries such as Lentz’s Law. This law explains the fact that inductive current flows inverse to the direction of changes in induction magnetic movement. Induction Heating System Topology Review

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.