显示标签为“inductionquenchingmachine”的博文。显示所有博文

2024年2月13日星期二

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel https://dw-inductionheater.com/induction-heating-for-surface-quenching-of-steel.html?feed_id=234013&_unique_id=65cbe8de8e33f

2024年2月6日星期二

INDUCTION HEATING FOR SURFACE QUENCHING

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. The kinetics of induction heating for surface quenching of steel https://dw-inductionheater.com/induction-heating-for-surface-quenching.html?feed_id=233596&_unique_id=65c2a071bd756

2024年1月1日星期一

induction quenching surface applications

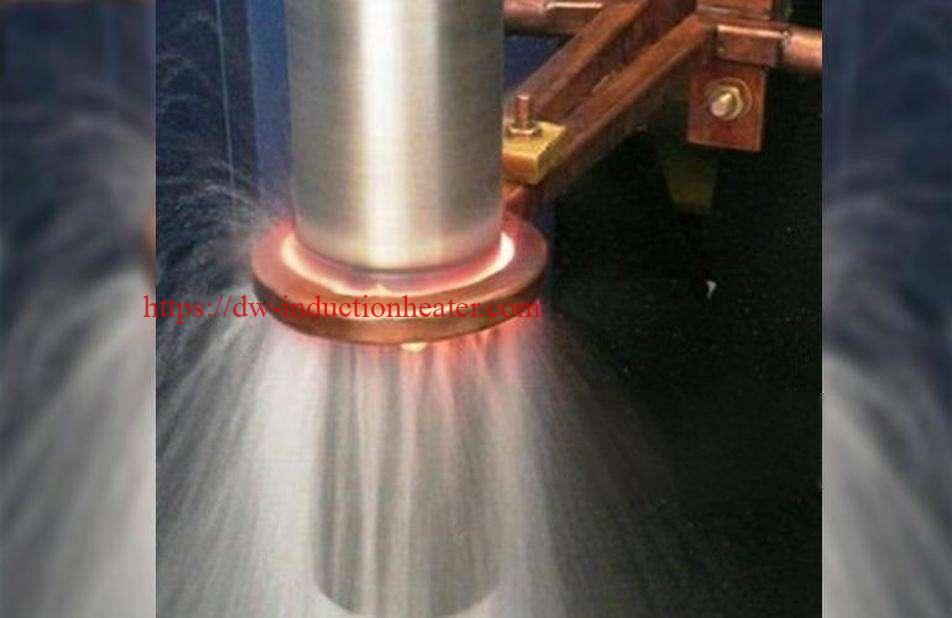
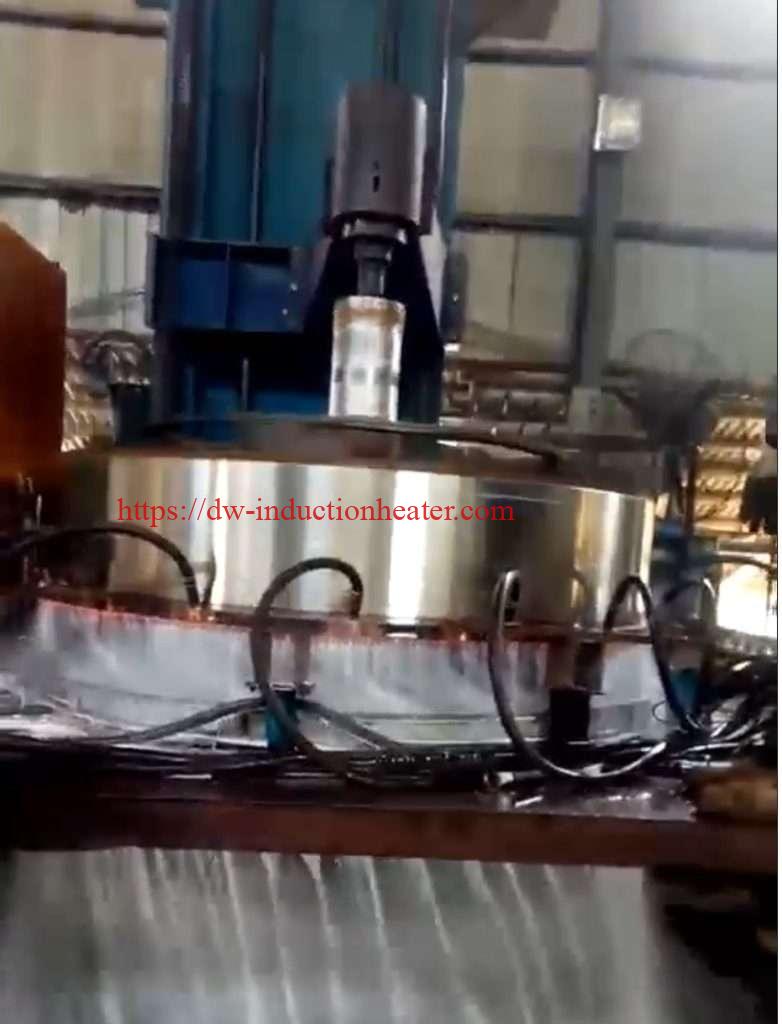
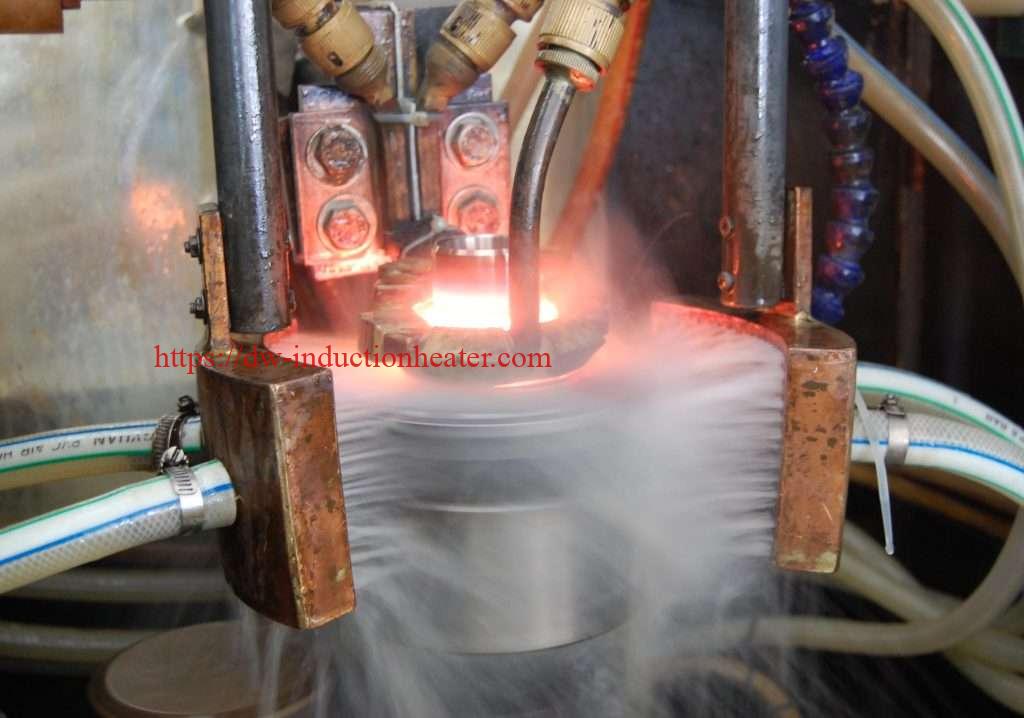
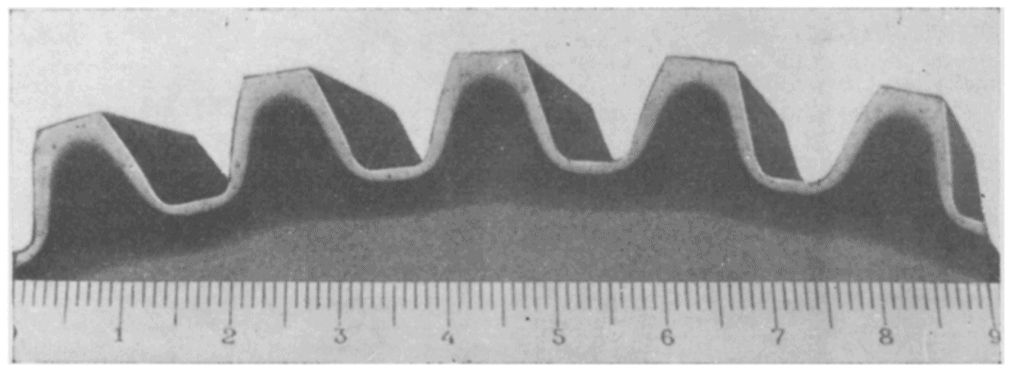
Induction quenching is a surface hardening process that involves heating a metal component using induction heating and then rapidly cooling it to achieve a hardened surface. This process is widely used in various industries, including automotive, aerospace, and manufacturing, to improve the wear resistance and durability of metal components. In this article, we will explore the applications of induction quenching surface treatment and its benefits in different industries. Automotive Industry: The automotive industry is one of the largest users of induction quenching for surface hardening applications. Components such as gears, shafts, and camshafts are often subjected to induction quenching to improve their wear resistance and fatigue strength. Induction quenching allows for precise control over the hardening depth and pattern, making it an ideal choice for automotive components that require high precision and consistency. Aerospace Industry: In the aerospace industry, induction quenching is used to improve the performance and longevity of critical components such as landing gear parts, turbine blades, and engine components. These parts are often subjected to extreme conditions during operation, and induction quenching helps to increase their resistance to wear, corrosion, and fatigue. The ability to selectively harden specific areas of a component makes induction quenching an attractive option for aerospace applications where weight reduction and performance optimization are critical. Manufacturing Industry: In the manufacturing industry, induction quenching is used for a wide range of applications, including tooling, dies, molds, and machine components. These components are often subjected to high levels of wear and abrasion during operation, making them ideal candidates for induction quenching. By increasing the hardness and wear resistance of these components' surfaces through induction quenching, manufacturers can extend their service life and reduce downtime due to premature failure. Benefits of Induction Quenching Surface Treatment: 1. Improved Wear Resistance: Induction quenching significantly increases the hardness of a metal component's surface layer, making it more resistant to wear from frictional forces. 2. Enhanced Fatigue Strength: Components that undergo induction quenching exhibit improved fatigue strength due to the transformation of their microstructure into a hardened state. 3. Precise Control: Induction quenching allows for precise control over the depth and pattern of hardening on a component's surface, enabling tailored solutions for specific applications. 4. Reduced Distortion: Compared to traditional heat treatment methods such as flame or furnace heating, induction quenching minimizes distortion in metal components due to its localized heating approach. 5. Energy Efficiency: Induction heating is an energy-efficient process that minimizes heat loss compared to other heating methods like flame or furnace heating. 6. Environmentally Friendly: Induction quenching produces minimal emissions or waste products compared to other heat treatment methods that involve combustion processes. 7. Cost-Effective: The precision control offered by induction quenching reduces material waste by minimizing over-treatment or rework requirements. Conclusion: Induction quenching surface treatment offers numerous benefits across various industries by improving the wear resistance and durability of metal components while maintaining tight tolerances on critical dimensions. Its ability to selectively harden specific areas makes it an attractive option for applications where precision control is essential. As technology continues to advance in this field with improvements in equipment design and process optimization techniques, we can expect further advancements in induction quenching's capabilities across different industries in the future. https://dw-inductionheater.com/induction-quenching-surface-applications.html?feed_id=231286&_unique_id=6592b325aff4a
2023年12月18日星期一

induction quenching surface applications

Induction quenching is a surface hardening process that involves heating a metal component using induction heating and then rapidly cooling it to achieve a hardened surface. This process is widely used in various industries, including automotive, aerospace, and manufacturing, to improve the wear resistance and durability of metal components. In this article, we will explore the applications of induction quenching surface treatment and its benefits in different industries. Automotive Industry: The automotive industry is one of the largest users of induction quenching for surface hardening applications. Components such as gears, shafts, and camshafts are often subjected to induction quenching to improve their wear resistance and fatigue strength. Induction quenching allows for precise control over the hardening depth and pattern, making it an ideal choice for automotive components that require high precision and consistency. Aerospace Industry: In the aerospace industry, induction quenching is used to improve the performance and longevity of critical components such as landing gear parts, turbine blades, and engine components. These parts are often subjected to extreme conditions during operation, and induction quenching helps to increase their resistance to wear, corrosion, and fatigue. The ability to selectively harden specific areas of a component makes induction quenching an attractive option for aerospace applications where weight reduction and performance optimization are critical. Manufacturing Industry: In the manufacturing industry, induction quenching is used for a wide range of applications, including tooling, dies, molds, and machine components. These components are often subjected to high levels of wear and abrasion during operation, making them ideal candidates for induction quenching. By increasing the hardness and wear resistance of these components' surfaces through induction quenching, manufacturers can extend their service life and reduce downtime due to premature failure. Benefits of Induction Quenching Surface Treatment: 1. Improved Wear Resistance: Induction quenching significantly increases the hardness of a metal component's surface layer, making it more resistant to wear from frictional forces. 2. Enhanced Fatigue Strength: Components that undergo induction quenching exhibit improved fatigue strength due to the transformation of their microstructure into a hardened state. 3. Precise Control: Induction quenching allows for precise control over the depth and pattern of hardening on a component's surface, enabling tailored solutions for specific applications. 4. Reduced Distortion: Compared to traditional heat treatment methods such as flame or furnace heating, induction quenching minimizes distortion in metal components due to its localized heating approach. 5. Energy Efficiency: Induction heating is an energy-efficient process that minimizes heat loss compared to other heating methods like flame or furnace heating. 6. Environmentally Friendly: Induction quenching produces minimal emissions or waste products compared to other heat treatment methods that involve combustion processes. 7. Cost-Effective: The precision control offered by induction quenching reduces material waste by minimizing over-treatment or rework requirements. Conclusion: Induction quenching surface treatment offers numerous benefits across various industries by improving the wear resistance and durability of metal components while maintaining tight tolerances on critical dimensions. Its ability to selectively harden specific areas makes it an attractive option for applications where precision control is essential. As technology continues to advance in this field with improvements in equipment design and process optimization techniques, we can expect further advancements in induction quenching's capabilities across different industries in the future. https://dw-inductionheater.com/induction-quenching-surface-applications.html?feed_id=231259&_unique_id=6580f9d493705

induction quenching surface applications

Induction quenching is a surface hardening process that involves heating a metal component using induction heating and then rapidly cooling it to achieve a hardened surface. This process is widely used in various industries, including automotive, aerospace, and manufacturing, to improve the wear resistance and durability of metal components. In this article, we will explore the applications of induction quenching surface treatment and its benefits in different industries. Automotive Industry: The automotive industry is one of the largest users of induction quenching for surface hardening applications. Components such as gears, shafts, and camshafts are often subjected to induction quenching to improve their wear resistance and fatigue strength. Induction quenching allows for precise control over the hardening depth and pattern, making it an ideal choice for automotive components that require high precision and consistency. Aerospace Industry: In the aerospace industry, induction quenching is used to improve the performance and longevity of critical components such as landing gear parts, turbine blades, and engine components. These parts are often subjected to extreme conditions during operation, and induction quenching helps to increase their resistance to wear, corrosion, and fatigue. The ability to selectively harden specific areas of a component makes induction quenching an attractive option for aerospace applications where weight reduction and performance optimization are critical. Manufacturing Industry: In the manufacturing industry, induction quenching is used for a wide range of applications, including tooling, dies, molds, and machine components. These components are often subjected to high levels of wear and abrasion during operation, making them ideal candidates for induction quenching. By increasing the hardness and wear resistance of these components' surfaces through induction quenching, manufacturers can extend their service life and reduce downtime due to premature failure. Benefits of Induction Quenching Surface Treatment: 1. Improved Wear Resistance: Induction quenching significantly increases the hardness of a metal component's surface layer, making it more resistant to wear from frictional forces. 2. Enhanced Fatigue Strength: Components that undergo induction quenching exhibit improved fatigue strength due to the transformation of their microstructure into a hardened state. 3. Precise Control: Induction quenching allows for precise control over the depth and pattern of hardening on a component's surface, enabling tailored solutions for specific applications. 4. Reduced Distortion: Compared to traditional heat treatment methods such as flame or furnace heating, induction quenching minimizes distortion in metal components due to its localized heating approach. 5. Energy Efficiency: Induction heating is an energy-efficient process that minimizes heat loss compared to other heating methods like flame or furnace heating. 6. Environmentally Friendly: Induction quenching produces minimal emissions or waste products compared to other heat treatment methods that involve combustion processes. 7. Cost-Effective: The precision control offered by induction quenching reduces material waste by minimizing over-treatment or rework requirements. Conclusion: Induction quenching surface treatment offers numerous benefits across various industries by improving the wear resistance and durability of metal components while maintaining tight tolerances on critical dimensions. Its ability to selectively harden specific areas makes it an attractive option for applications where precision control is essential. As technology continues to advance in this field with improvements in equipment design and process optimization techniques, we can expect further advancements in induction quenching's capabilities across different industries in the future. https://dw-inductionheater.com/induction-quenching-surface-applications.html?feed_id=231224&_unique_id=65803f420c91f

2023年9月12日星期二

INDUCTION HEATING FOR SURFACE QUENCHING

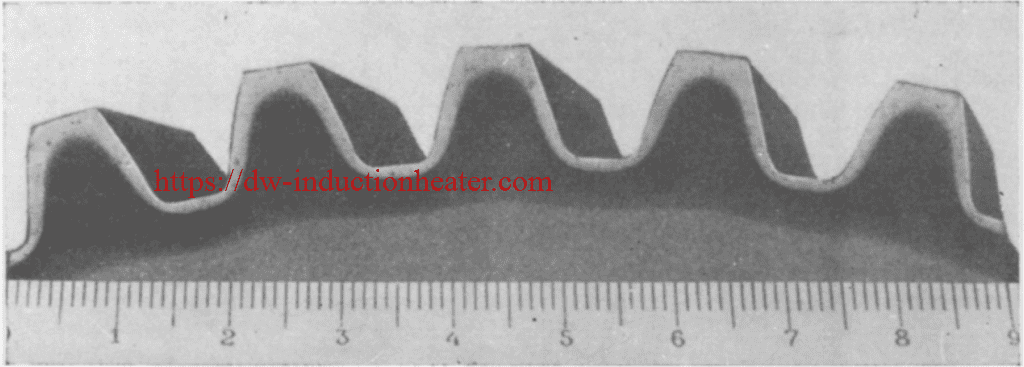
The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. The kinetics of induction heating for surface quenching of steel
2023年7月25日星期二

INDUCTION HEATING FOR SURFACE QUENCHING

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. The kinetics of induction heating for surface quenching of steel

2023年7月11日星期二

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel

2023年6月22日星期四

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel https://dw-inductionheater.com/induction-heating-for-surface-quenching-of-steel.html?feed_id=215311&_unique_id=64946fdc75959

2023年6月15日星期四

INDUCTION HEATING FOR SURFACE QUENCHING

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. The kinetics of induction heating for surface quenching of steel https://dw-inductionheater.com/induction-heating-for-surface-quenching.html?feed_id=213361&_unique_id=648b25381cddc

2023年5月11日星期四

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel

2023年4月20日星期四

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel

2023年2月10日星期五

INDUCTION HEATING FOR SURFACE QUENCHING

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. The kinetics of induction heating for surface quenching of steel

2023年1月17日星期二

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel

2023年1月15日星期日

INDUCTION HEATING FOR SURFACE QUENCHING

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. The kinetics of induction heating for surface quenching of steel

2023年1月11日星期三

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel

2022年12月21日星期三

INDUCTION HEATING FOR SURFACE QUENCHING

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. The kinetics of induction heating for surface quenching of steel

2022年11月24日星期四

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel

2022年11月21日星期一

induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). These factors are related to the change in the parameters of the inductors during the heating of steel and to the peculiarities of a given design of the high-frequency apparatus, i.e., whether the power utilized is regulated during the heating process. In most cases the intensity of the electromagnetic field of the inductor does not remain constant during heating, and this change affects the shape of the temperature-time curve. Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. Surface Quenching of Machine Parts After Induction Heating. Induction heating is widely used for surface treatment of parts. The kinetics of induction heating for surface quenching of steel

2022年10月31日星期一

INDUCTION HEATING FOR SURFACE QUENCHING

The kinetics of induction heating for surface quenching of steel depend on factors: 1) which induce changes in the electric and magnetic parameters of steels as the result of the increased temperature (these changes lead to changes in the amount of absorbed heat at a given intensity of the electric field at a given induction current) and, 2) on factors which are responsible for the change of the intensity of the electromagnetic field during heating (i.e., change of the current in the inductor). Induction heating in the heat treatment of automobile parts was first used at our plant. In 1937-1938 surface quenching of the necks of crank shafts of the ZIS-5 engine was developed at our plant in collaboration with the staff of the V. P. Vologdin laboratory. The equipment was installed as part of the continuous production line,in which the parts were subjected to mechanical treatment on semi-automatic high-frequency apparatus. More than 61% of alt the parts of the engines of ~ae ZIL-164A and ZIL-157K automobiles are surface hardened by induction heating. The kinetics of induction heating for surface quenching of steel

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.