2023年8月25日星期五
Induction annealing copper wires
Continuous Induction annealing copper wires with High frequency heating system
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes

2023年7月17日星期一
Induction annealing copper wires
Continuous Induction annealing copper wires with High frequency heating system
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes
2023年3月6日星期一
Induction annealing copper wires
Continuous Induction annealing copper wires with High frequency heating system
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes
2023年2月28日星期二
Induction annealing copper wires
Continuous Induction annealing copper wires with High frequency heating system
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes
2022年10月25日星期二
Induction annealing copper wires
Continuous Induction annealing copper wires with High frequency heating system
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes
2022年7月23日星期六
Induction annealing copper wires
Continuous Induction annealing copper wires with High frequency heating system
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes
2022年6月6日星期一
Induction annealing copper wires
Continuous Induction annealing copper wires with High frequency heating system
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes
2022年2月4日星期五
Induction annealing copper wires
Continuous Induction annealing copper wires with High frequency heating system
Objective Continuously anneal a copper wire used in electric motors at a rate of 16.4 yds (15m) per minute to eliminate work hardening caused during the drawing process.
Material Square copper wire 0.06” (1.7mm) dia., temperature indicating paint
Temperature 842 ºF (450 ºC)
Frequency 300 kHz
Equipment • DW-UHF-60kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0μF
• An induction heating coil designed and developed specifically for this application.
Process A twelve turn helical coil is used. A ceramic tube is placed inside the coil to isolate the copper wire from the copper coil and to allow the copper wire to flow smoothly through the coil.
Power runs continuously to anneal at a rate of 16.4 yds (15m) per minute.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Flameless process
• Ideal for in-line production processes
2021年11月13日星期六
Induction Annealing Copper Wire
Induction Annealing Copper Wire And Silver Wire
Objective Anneal a brazing wire for preform production.
Material Copper Nickel Silver 2774 Alloy rod 0.070" (1.8mm) diameter.
Temperature 650ºF(343.3ºC)
Frequency 500 kHz
Equipment • DW-UHF-6KW-III induction heating system equipped with a remote workhead with one 1.0 μF capacitor, and a 4-20 mA input controller to aid in voltage ramping.
• An induction heating coil designed and developed specifically for this application.
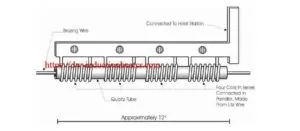
Process A unique helical coil consisting of four consecutive coils connected in parallel with a quartz tube lining is used to heat the wire to 650ºF (343.3ºC) for annealing.
Results/Benefits Induction heating provides:
• Higher productivity of 27’ (8.2m) per minute
• Reduction in surface oxidation & scaling
• Consistent, repeatable results

订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.