显示标签为“brazingcoppertostainlesssteel”的博文。显示所有博文

2024年3月23日星期六

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
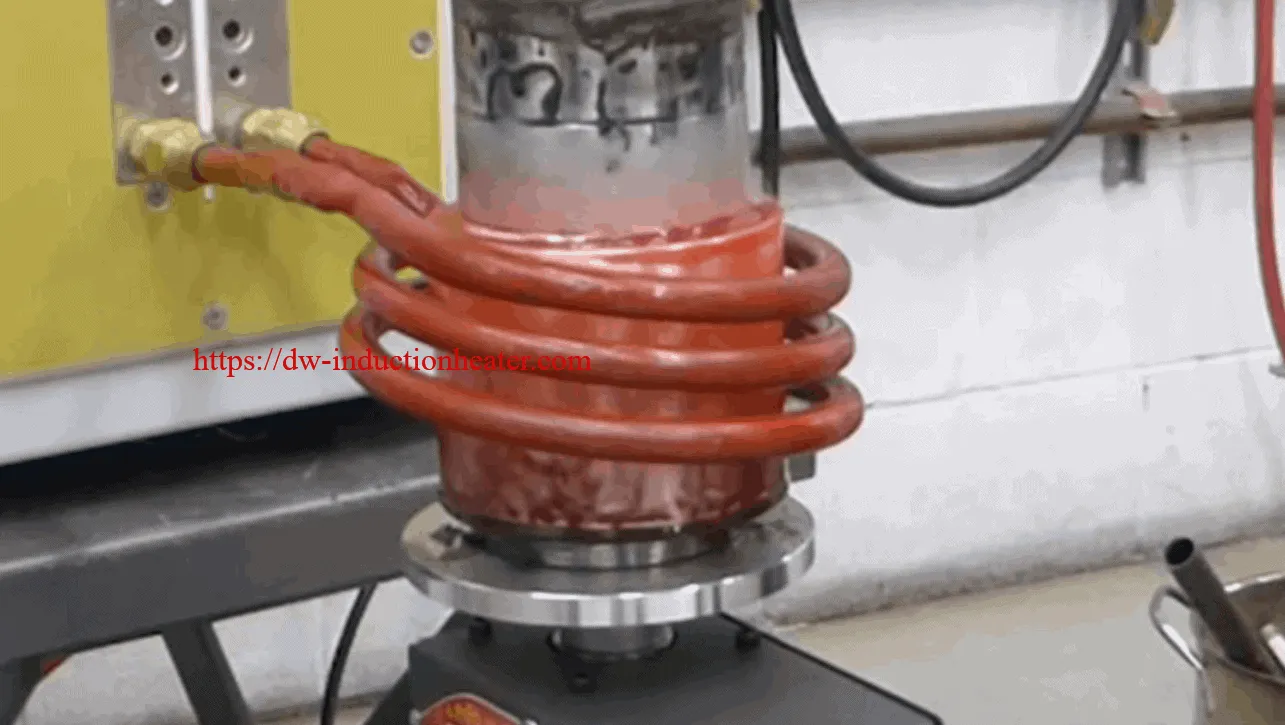
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 
https://dw-inductionheater.com/high-frequency-induction-brazing-copper-to-stainless-steel-process.html?feed_id=238126&_unique_id=65ff5460eaa7b

2023年7月31日星期一

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
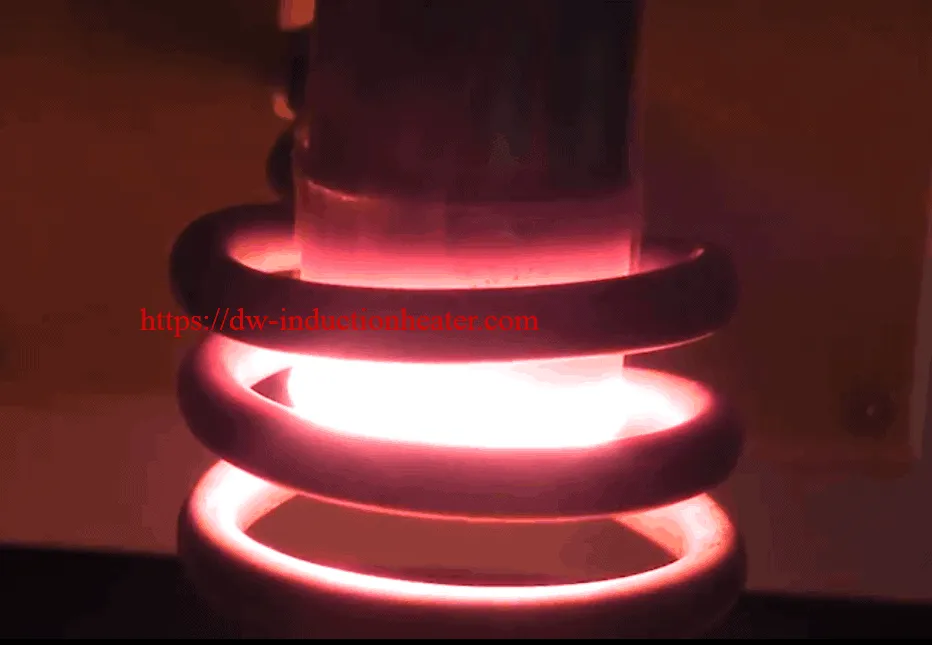
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 
https://dw-inductionheater.com/high-frequency-induction-brazing-copper-to-stainless-steel-process.html?feed_id=221311&_unique_id=64c7e28e1adb8

2023年6月11日星期日

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

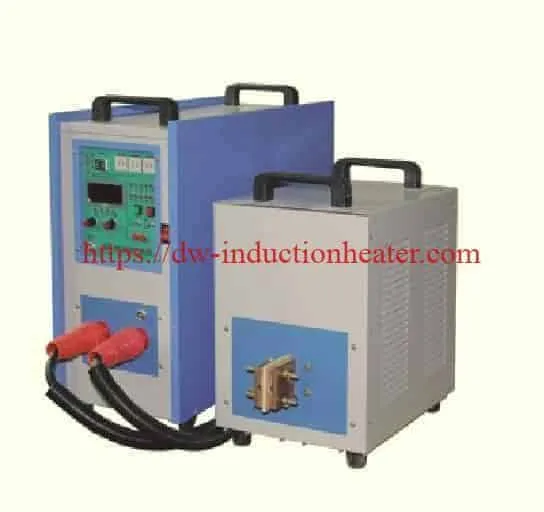
Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 

2023年4月23日星期日

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 

2022年12月16日星期五

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
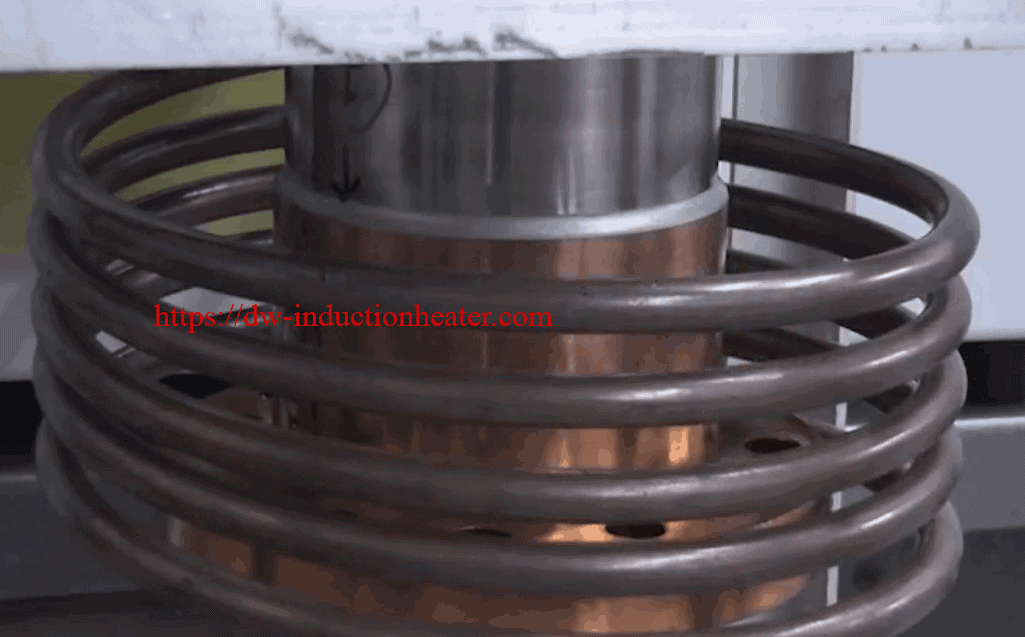
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 

2022年10月19日星期三

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 

2022年9月9日星期五

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 

2022年5月23日星期一

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 

2022年5月14日星期六

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 

2022年1月25日星期二

Induction Brazing Copper to Stainless Steel Process

High Frequency Induction Brazing Copper to Stainless Steel Process Technology

Objective The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station Equipment DW-UHF-40KW Induction Heating Power Supply HLQ custom coil Key Parameters Power: 23.65 kW Temperature: Approximately 1300°F (704)°C Time: 3.5 mins
Materials Cooper 4.5″ OD 0.5″ Wall Thickness Stainless Steel  4″ OD Braze Joint 2″
Process: In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits: The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
 

2021年12月30日星期四

brazing copper to stainless steel

Objective Induction Brazing copper pipe to stainless steel pipe. Cryogenic Pumps and Housings. Equipment DW-HF-15kw/25KW/45KW induction heating equipment
DW-HF-45KW induction heater
Test 1 Materials Cryogenic Pumps and Housings – Copper cap (2” (25.4mm) OD, 3” (76.2mm) long, 0.15” (3.81mm) thick wall, sits on stainless steel shaft 1.4” (3.81mm) deep), stainless steel shaft (1.7” (43.18mm) OD, 6” (152.4mm) long and attached to larger mass when it ends, 0.1”(2.54mm) thick.) Power: 25 kW Temperature: 1145°F +(618°C) Time: Under 40 seconds
Test 2 Materials Cryogenic Pumps and Housings – Copper Sleeve (3.6” (91.44mm) OD, 0.1”(2.54mm) thick wall that is 2.7” (68.5mm) tall, 3.8” (96.52mm) OD lip on the bottom that is 0.6”(15.2mm) tall with a thickness of approximately 0.85”(21.5mm), part with lip is 3.14”(79.7mm) tall overall, SS shaft sits 2.66” (67.5mm) deep), SS Shaft (3.4”(86.3mm) OD, 3.2”(81.2mm) ID, over 7.5”(190.5mm) tall, has smaller cap and shaft attached on one end and a larger 8”(203.2mm) base at the other) Power: 16.06kW Temperature: 1145°F + (618°C) Time: 1 minute 30 seconds to 3 minutes
Test 3 Materials Cryogenic Pumps and Housings – Copper Sleeve (3.5” (88.9mm) OD, 0.1” (2.54mm) thick wall that is 2.1” (53.3mm) tall, 5.3” (134.6mm) OD lip on the bottom that is 0.74” (18.7mm) tall with a thickness of approximately 1” (25.4mm), part with lip is 2.8” (71.1mm) tall overall, stainless steel shaft sits 2.66” (67.5mm) deep), stainless steel shaft (3.35”(85.0mm) OD, 3.2” (81.2mm) ID, over 7.5” (190.5mm) tall, has smaller cap and shaft attached on one end and a larger 5.5” (139.7mm) base at the other) Power: 9.09kW Temperature: 1145°F + (618°C) Time: approximately 20 to 30 seconds
Test 4 Materials Cryogenic Pumps and Housings – Copper cap (2.7” (68.5mm) OD, 2.85” (72.3mm) high, 0.6” (15.2mm) wall, sits on stainless steel shaft 1.4”  (35.5mm) deep), stainless steel shaft (1.54” (39.1mm) OD, 0.9” (22.8mm) thick wall, 6.5″ (165.1mm) high and attached to larger mass when it ends) additional stainless steel cap on the other side of the copper, 2.44” (61.9mm) OD, 0.8” (20.3mm) high or more, 0.88” (22.35mm) stem on top that is 1.4” (35.5mm) tall with 0.66” (16.7mm) ID Power: 14kW Temperature: 1145°F + (618°C) Time: 1 minute 50 seconds
Results and Conclusions: Test 1: Test started with much lower power and ramped up to 25 kW after 15 seconds. The induction brazing was successful. Recommended to use a tighter coil that wraps around only half of the copper cap. This would concentrate the heat at only the location of where the alloy is and should decrease the heat time. Test 2: Test was done with an oversized coil due to clearance issues created by the lip on the part.  The approximate time for full cycle is 20 to 30 seconds. The lower frequency seemed to be beneficial for the application by causing the field to penetrate deeper past the copper and into the steel itself, resulting in quicker heat times. Test 3: Test was done with 14 kW to simulate the time cycle necessary for our DW-HF-15KW induction heating system. This part will require the longest heat time due to the mass of the copper. Heat times can be decreased by using a larger power supply. The heat times for all the tests can be improved upon by optimizing the induction heating coils for the specific parts and by lowering the frequency. A temperature controller and pyrometer are strongly recommended to ensure no damage is done to the parts if going with a larger induction system. If using a 15kW induction heating system, the temperature controller and pyrometer are still recommended but the risk of part damage is reduced.
  [wpforms id="3947"]

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.