显示标签为“Buyinductionbrazingheater”的博文。显示所有博文

2024年3月4日星期一

induction brazing steel tube to copper tube

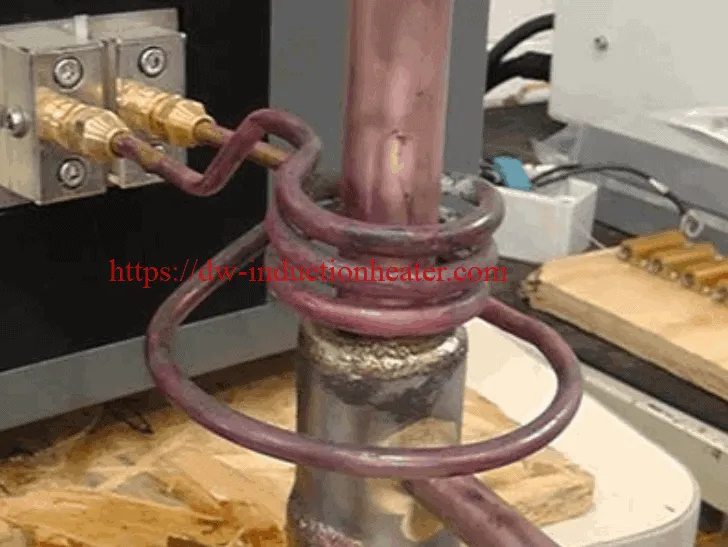
High Frequency Induction Brazing Steel Tube to Copper Tube

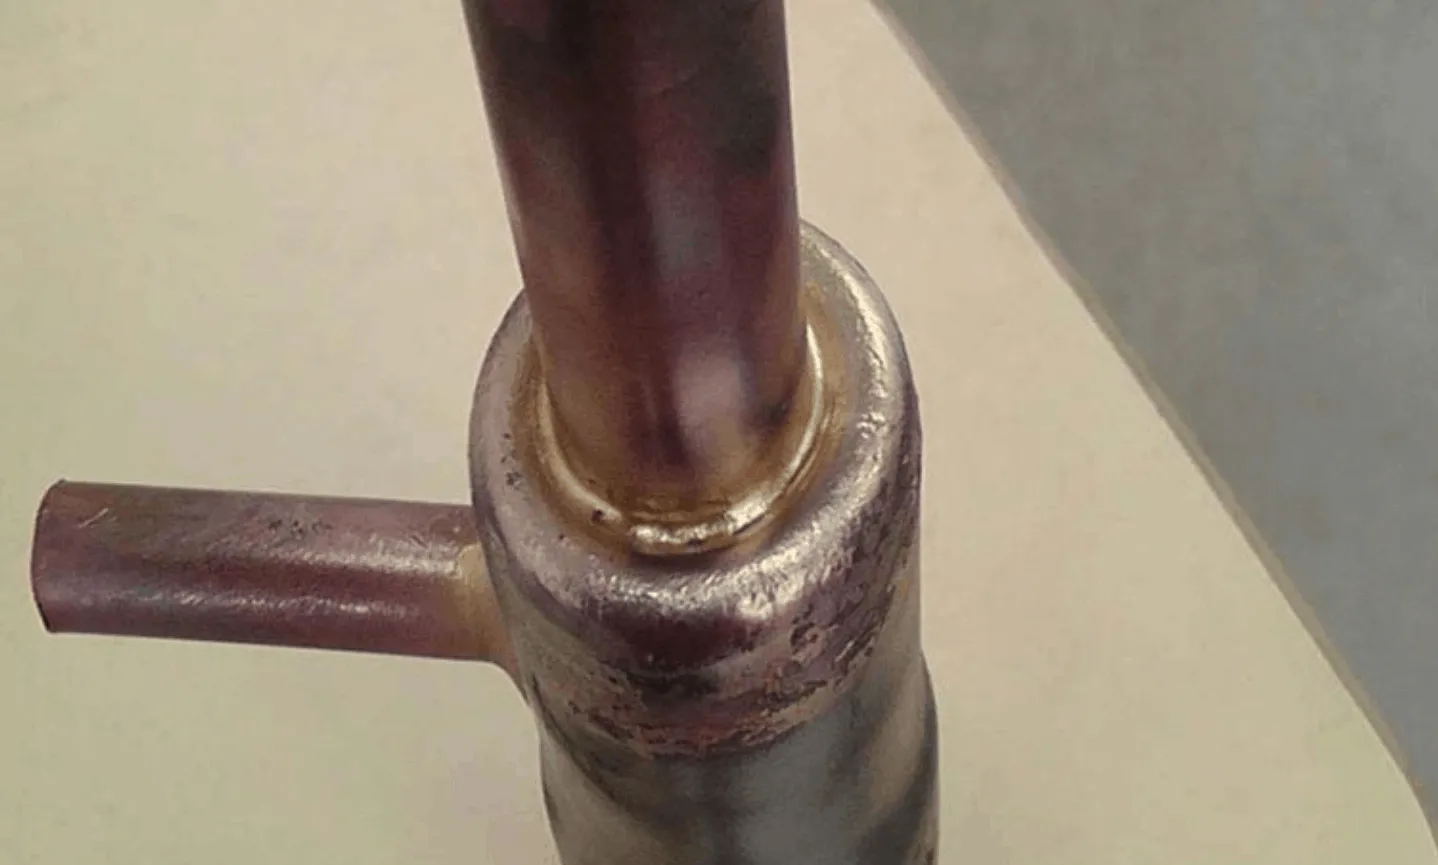
Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process
https://dw-inductionheater.com/induction-brazing-steel-tube-to-copper-tube.html?feed_id=235607&_unique_id=65e65518d8a86

2023年8月9日星期三

induction brazing steel tube to copper tube

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

2023年7月12日星期三

induction brazing steel tube to copper tube

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process
https://dw-inductionheater.com/induction-brazing-steel-tube-to-copper-tube.html?feed_id=218611&_unique_id=64aedfb67501c

2023年4月26日星期三

induction brazing steel tube to copper tube

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

2023年4月12日星期三

induction brazing steel tube to copper tube

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

2022年11月3日星期四

induction brazing steel tube to copper tube

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

2022年9月29日星期四

induction brazing steel tube to copper tube

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

2022年9月20日星期二

induction brazing steel tube to copper tube

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

2022年1月5日星期三

Brazing Steel Tube to Copper Tube with Induction Heater

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

Brazing Copper Tubing with Induction

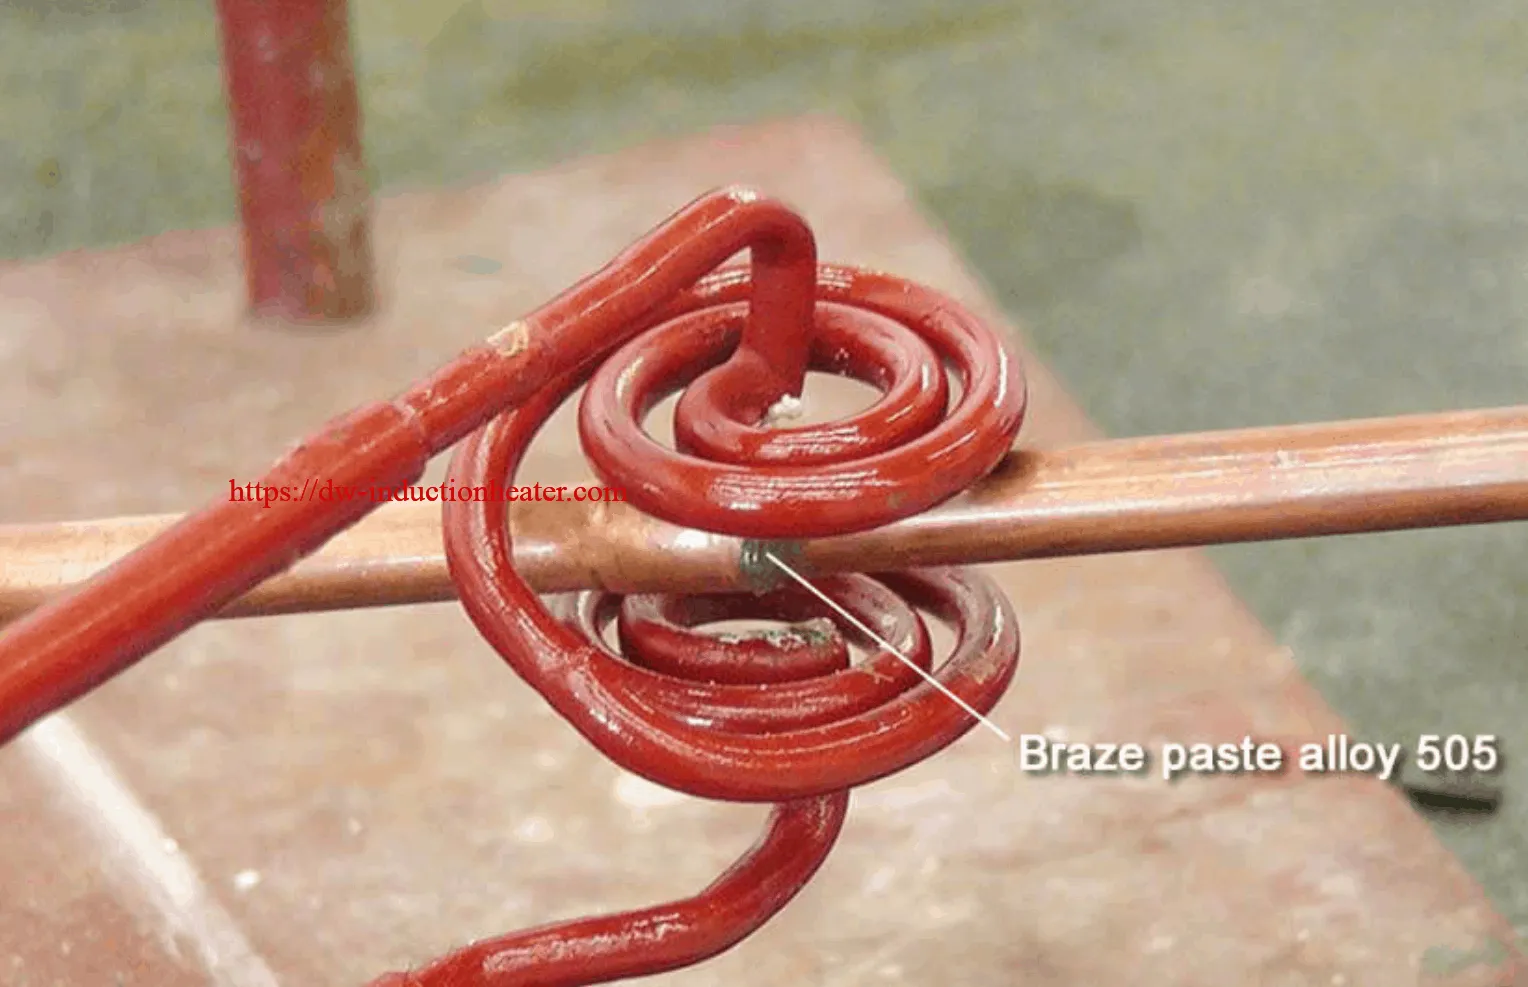
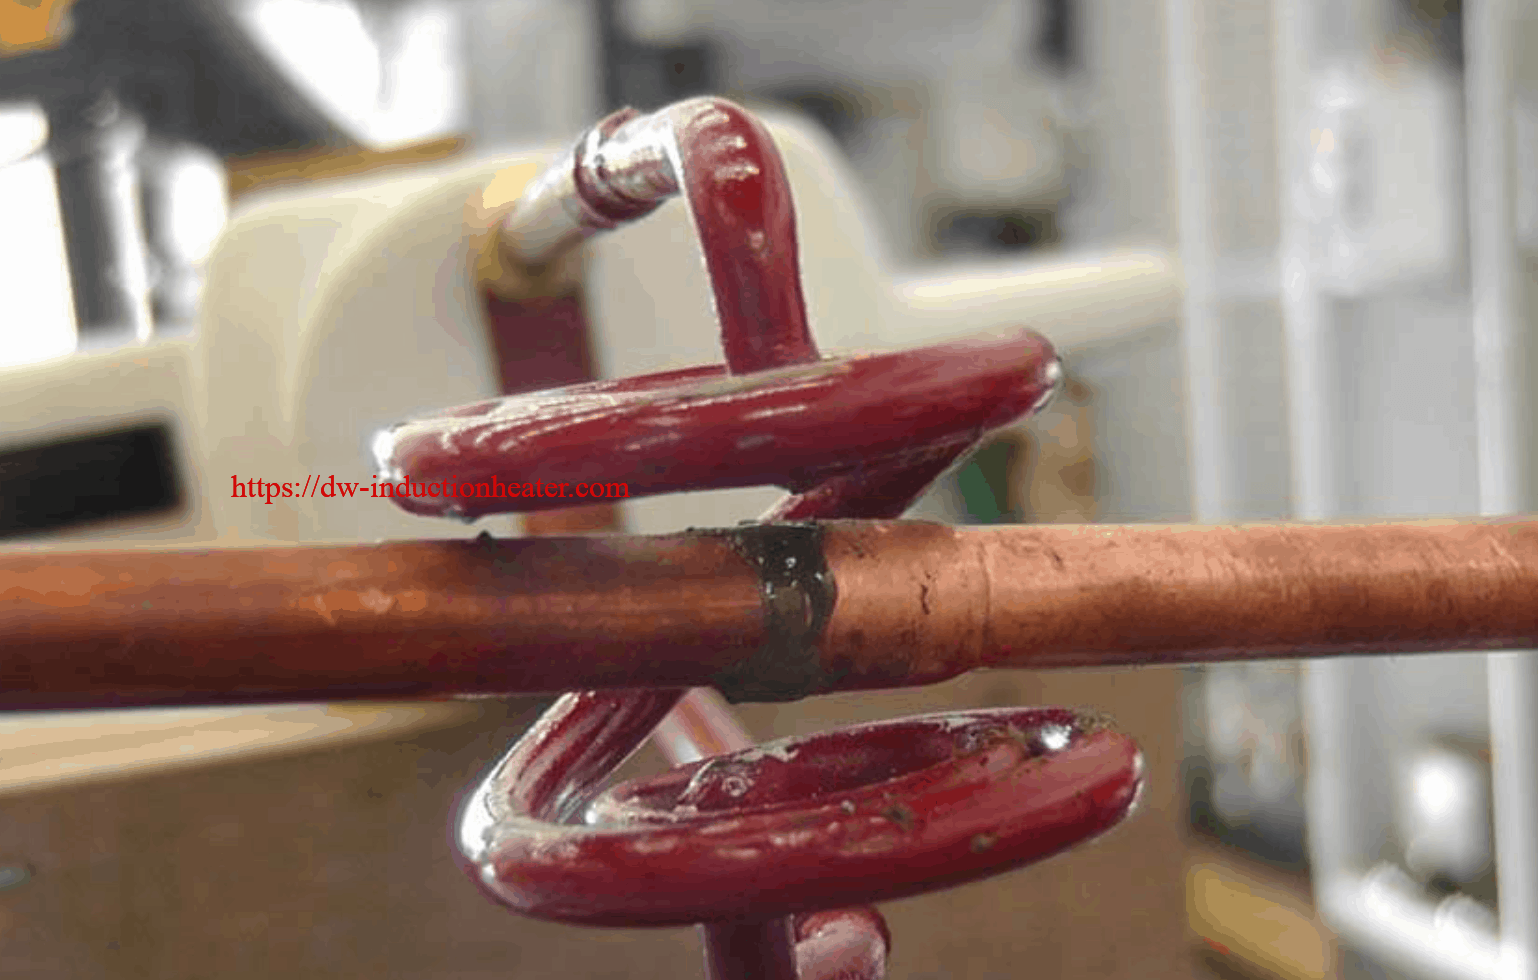
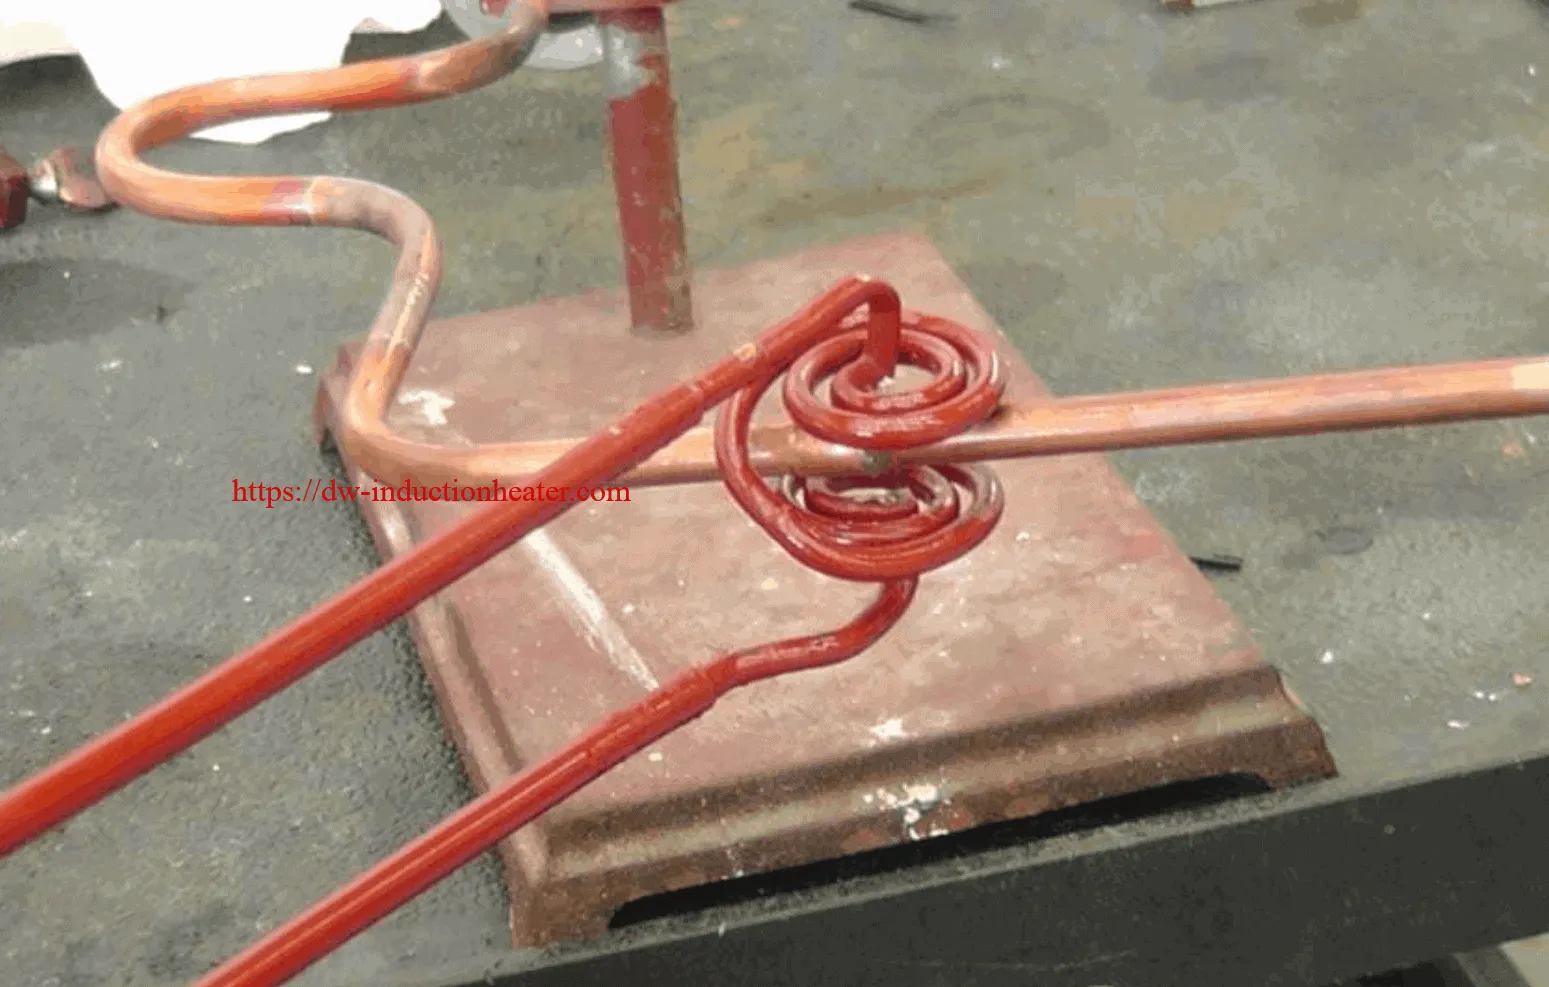
Objective Demonstrating induction brazing copper tubing and braze time using the DW-UHF-10 kW system and available split lab coil Equipment DW-UHF-10KW induction brazing machine Materials • Copper tubing – Suction Tube • Braze paste Key Parameters Power: 10 kW Temperature: Approximately 1500° F (815° C) Time: 5 – 5.2 sec Process: As only one assembly was provided for the test, we set up a test load using a heavy wall 5/16” copper tubing set up such as one tube accepted the other at a formed open flange end. Heat time was estimated based on using tempilaque paint to indicate the temperature. The test assembly, (followed by the provided components) were assemble with a coating of 505 alloy braze paste and placed in the lab test coil per the attached photographs) A heat cycle 5 – 5.2 seconds was found to flow the alloy and make the joint. Results/Benefits:
  1. As demonstrated, the DW-UHF model induction brazing system is capable of heating both the largest and smallest tube to tube sections to complete a brazed joint. Heat times using an available test coil are within the production heat time expectations required by Electrolux.
  2. HLQ will require a full assembly for review in order to develop the final coil design that can accommodate all 12 joints indicated on your layout photograph. It is necessary to know and see the clearances between the tube connections to be brazed and the steel compressor section to insure that the steel housing is not affected by the resulting RF field created at the load coil. This final design may require the addition of ferrite materials in the coil that will serve to focus the RF field to the copper leads and not to the steel housing.
  3. Initial tests were completed on the  DW-UHF-10kW utilizing an available lab coil. The production coil will be contained in a none-conductive housing that will permit the operator to use it to locate the coil against the copper leads for accurate and positive heating location for the braze process. The production coil design will incorporate shorter leads than the test coil and be configured such that the heat cycles will be improved (shorter heat times).
 

2021年11月5日星期五

induction brazing steel tube to copper tube

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

2021年11月1日星期一

Brazing Copper Tubing with Induction

Objective Demonstrating induction brazing copper tubing and braze time using the DW-UHF-10 kW system and available split lab coil Equipment DW-UHF-10KW induction brazing machine Materials • Copper tubing – Suction Tube • Braze paste Key Parameters Power: 10 kW Temperature: Approximately 1500° F (815° C) Time: 5 – 5.2 sec Process: As only one assembly was provided for the test, we set up a test load using a heavy wall 5/16” copper tubing set up such as one tube accepted the other at a formed open flange end. Heat time was estimated based on using tempilaque paint to indicate the temperature. The test assembly, (followed by the provided components) were assemble with a coating of 505 alloy braze paste and placed in the lab test coil per the attached photographs) A heat cycle 5 – 5.2 seconds was found to flow the alloy and make the joint. Results/Benefits:
  1. As demonstrated, the DW-UHF model induction brazing system is capable of heating both the largest and smallest tube to tube sections to complete a brazed joint. Heat times using an available test coil are within the production heat time expectations required by Electrolux.
  2. HLQ will require a full assembly for review in order to develop the final coil design that can accommodate all 12 joints indicated on your layout photograph. It is necessary to know and see the clearances between the tube connections to be brazed and the steel compressor section to insure that the steel housing is not affected by the resulting RF field created at the load coil. This final design may require the addition of ferrite materials in the coil that will serve to focus the RF field to the copper leads and not to the steel housing.
  3. Initial tests were completed on the  DW-UHF-10kW utilizing an available lab coil. The production coil will be contained in a none-conductive housing that will permit the operator to use it to locate the coil against the copper leads for accurate and positive heating location for the braze process. The production coil design will incorporate shorter leads than the test coil and be configured such that the heat cycles will be improved (shorter heat times).
 

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.