显示标签为“coppertube”的博文。显示所有博文

2022年1月5日星期三

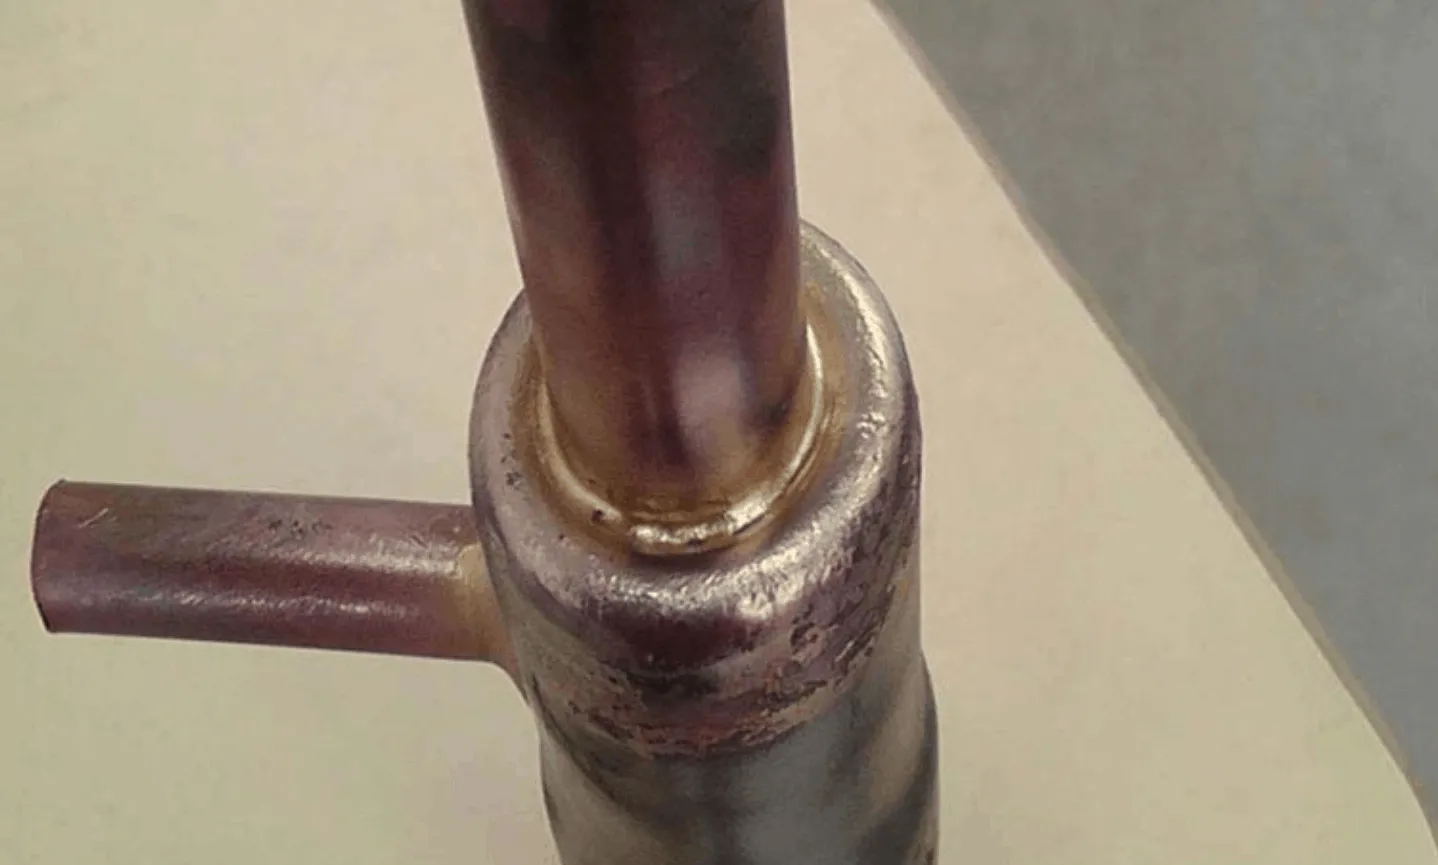
Brazing Steel Tube to Copper Tube with Induction Heater

High Frequency Induction Brazing Steel Tube to Copper Tube

Objective The goal is to braze a steel tube to a copper tube in 60 seconds using flux and brazing alloy.
Equipment DW-UHF-10kw induction brazing heater Three turns dual diameter coil Materials • Steel tube and copper receiver • Braze alloy (CDA 681) • B-1 flux Key Parameters Temperature: Approximately 1750° F (954° C) Frequency: 148 kHz
Process:
  1. The assembly section was pre-assembled and fluxed (B-1) then located in the two diameter coil with a single pre-formed alloy ring set at the interface area.
  2. Alloy flow and joint completed in 60 seconds.
  3. The material was cooled in water following the completion of induction brazing.
  4. The joint was then cross-sectioned to validate that the brazing process had produced a strong, high quality joint.
Results/Benefits:
  • Strong durable joints with induction heating
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
induction brazing steel tube to copper tube process

2021年11月11日星期四

Induction Annealing Copper Tube

Induction Annealing Copper Tube With High Frequency Induction Heating System

Objective To heat both ends of a copper tube to anneal as soft as possible 1.5” (38.1mm) from end and retain full hardness next to anneal Material 1.625” (41.275mm) dia x 24” (609.6mm) long copper tube Temperature 1500 ºF (815.5 ºC) Frequency 60 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0μF capacitors for a total of 8.0 μF induction-annealing-copper-tube • An induction heating coil designed and developed specifically for this application. Process A four turn helical coil is used for this annealing process. The copper tube is placed in the coil and power is applied for a total of 7.5 seconds. At 3.75 seconds the copper tube is rotated half a turn to insure uniform annealing. The copper is tube immediately quenched to guarantee the annealed area is only 1.5” (38.1mm) from end of tube. The tube is then flipped to anneal the other end. Results/Benefits Induction heating provides: • Controlled application of heat to very specific area • Faster process time, increased production • High efficiency, low energy cost • Hands-free heating that involves no operator skill for manufacturing

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.