2024年1月28日星期日

induction preheating before welding steel pipe

Induction Preheating Before Welding Steel Pipe

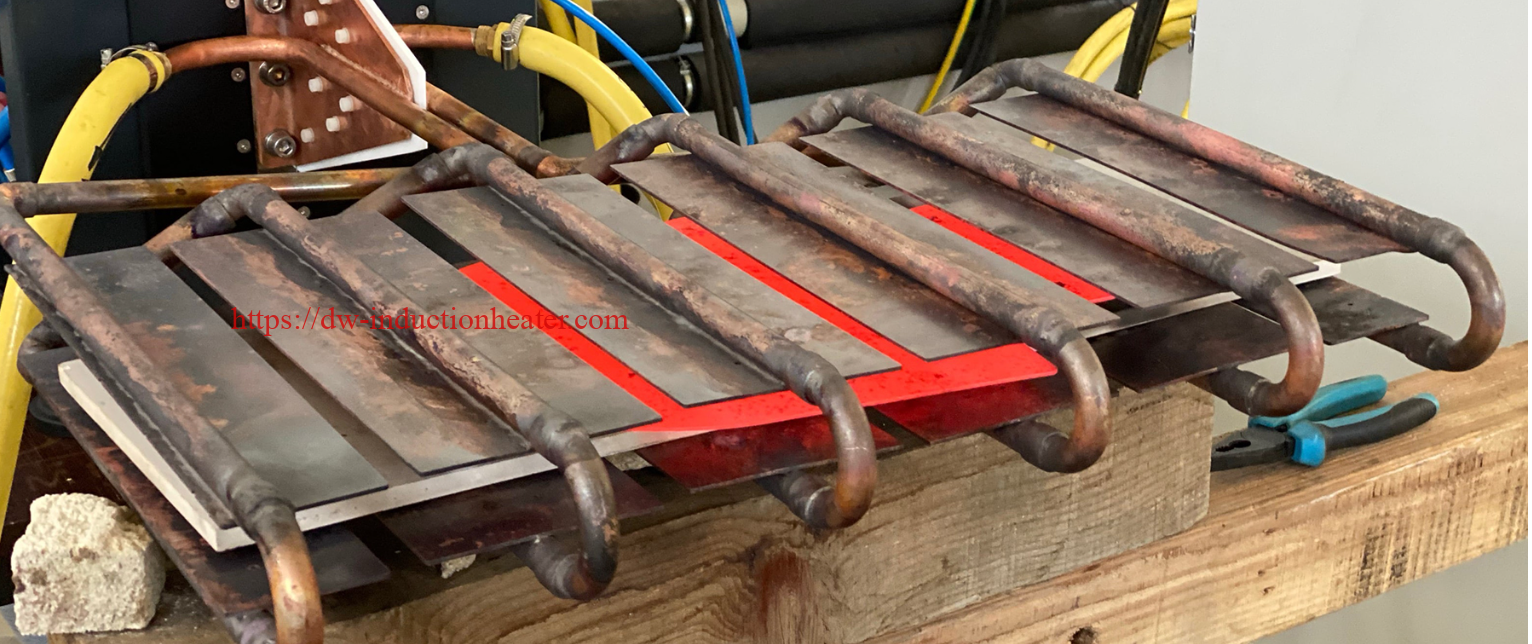
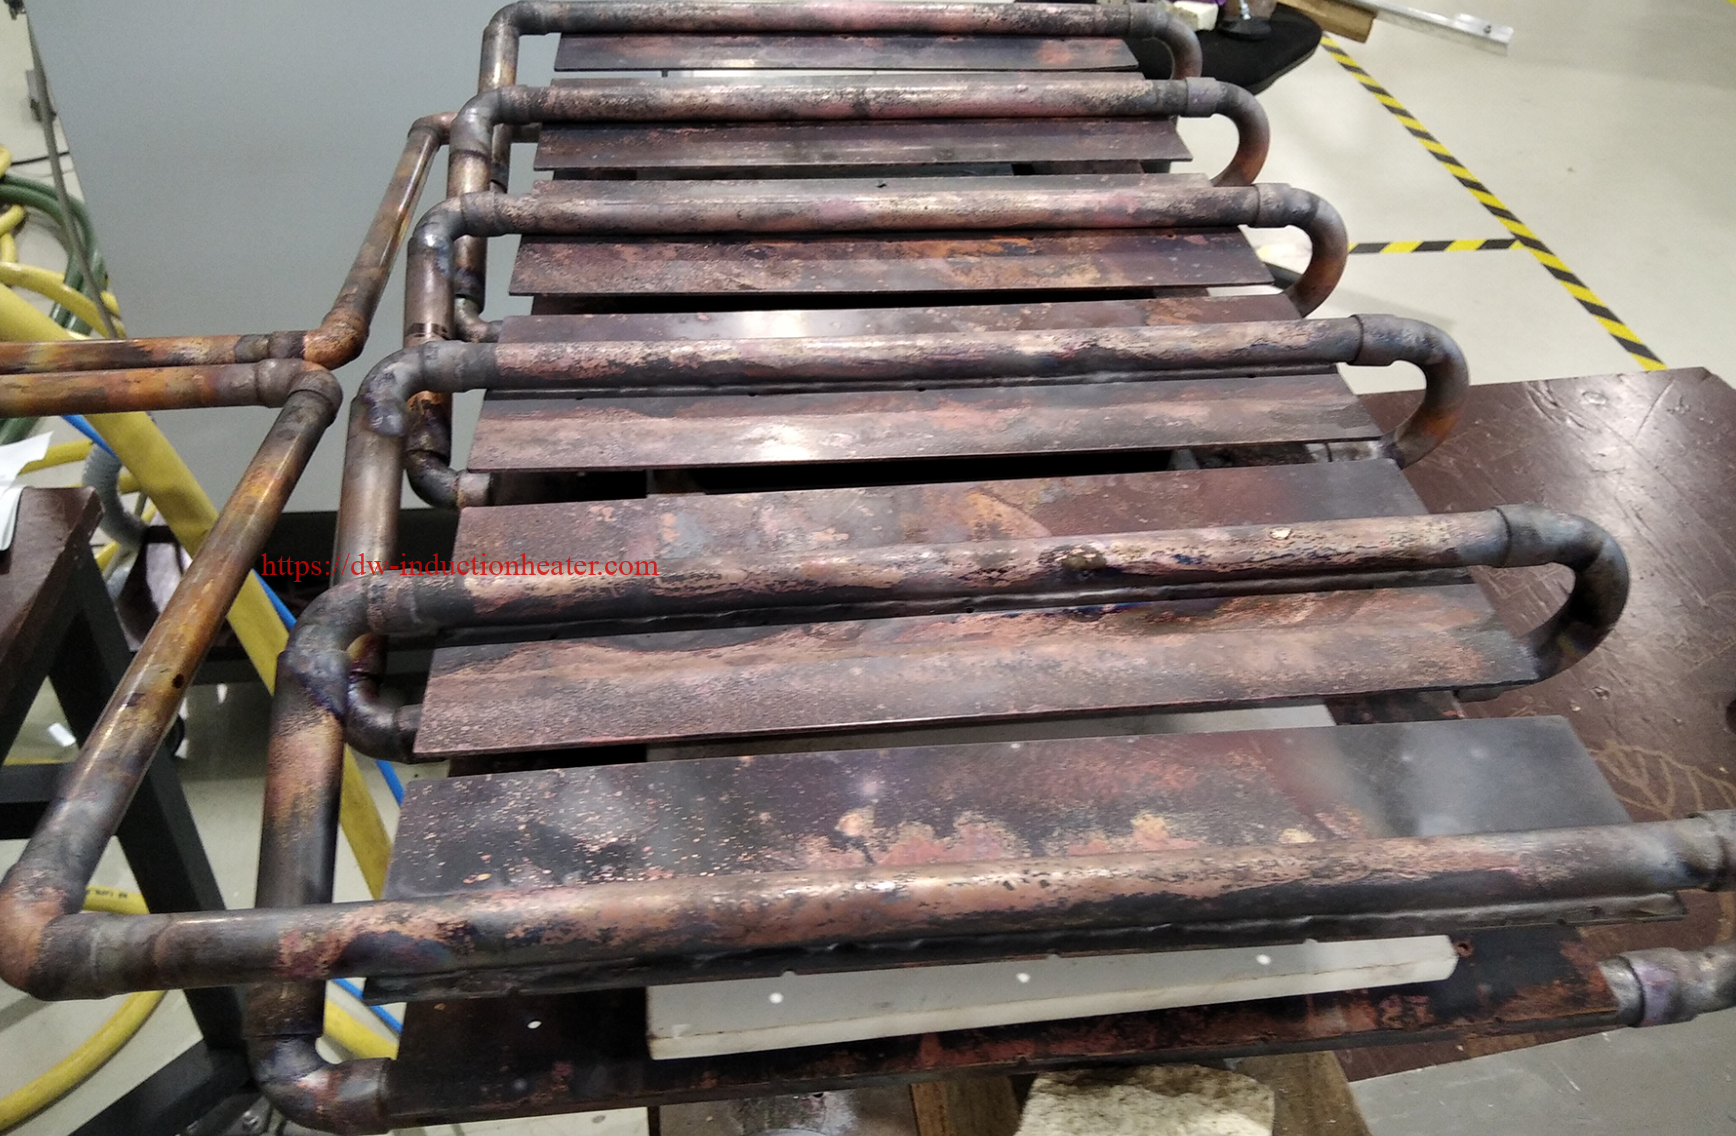
This induction heating application shows the preheating of steel pipe before welding with 30kW air-cooled induction power supply and air-cooled coil. Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: HLQ 30kw air cooled induction heater Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our mobile air-cooled 30kW induction heating system which allows us to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temperature monitoring tools. The induction heating method is very efficient because it minimizes the heat loss that often occurs during other heating methods. https://dw-inductionheater.com/induction-preheating-before-welding-steel-pipe.html?feed_id=233086&_unique_id=65b67c835eaf5

2024年1月27日星期六

hot water boiler with induction heating

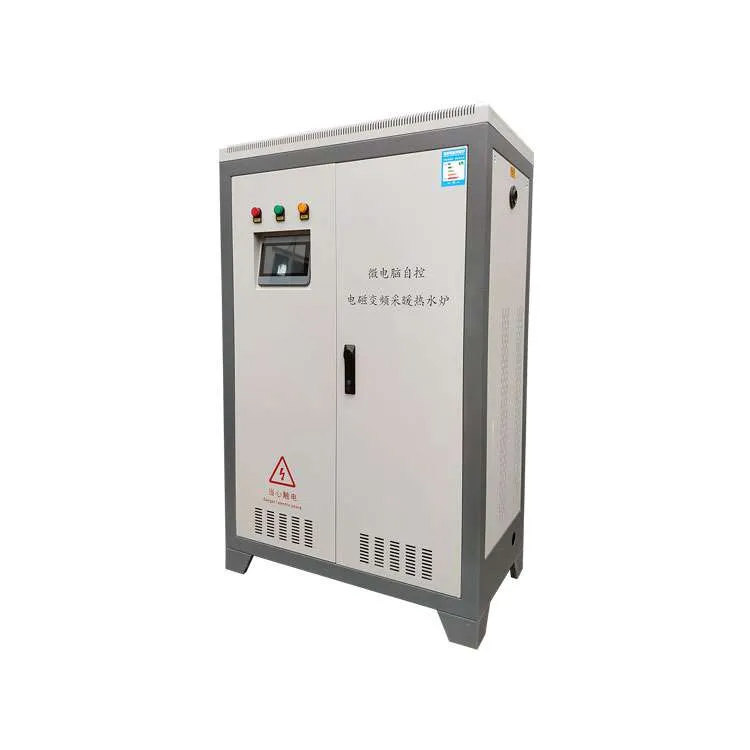
Industrial Hot Water Heating Boiler With Electromagentic Induction-Hot Water Heating Boiler Generator

Industrial Hot Water Boiler with Electromagnetic Induction Parameter  
  Items   Unit 60KW 80KW 100KW 120KW 160KW 180KW 240KW 240KW-F 360KW
Rated power kW 60 80 100 120 160 180 240 240 360
Rated current A 90 120 150 180 240 270 360 540 540
Voltage/Frequency V/H z 380/50-60
Cross section area of power cable mm ²   ≥25   ≥35   ≥50   ≥70   ≥120   ≥150   ≥185   ≥185   ≥240
Heating efficiency % ≥98 ≥98 ≥98 ≥98 ≥98 ≥98 ≥98 ≥98 ≥98
Max. pressure of heating Mp a   0.2   0.2   0.2   0.2   0.2   0.2   0.2   0.2   0.2
Min. flow of pump L/m in 72 96 120 144 192 216 316 336 384
Expansion tank volume L 60 80 80 120 160 180 240 240 320
Max. heating temperature 85 85 85 90 90 90 90 90 90
Temperature of low temperature protection     5   5   5   5   5   5   5   5   5
65ºC hot water output L/m 19.5 26 26 39 52 58.5 78 78 104
 
Dimensions mm 1000*650* 1480 1000*650* 1480 1100*1000* 1720 1100*1000* 1720 1100*1000* 1720 1315*1000* 1910 1315*1000* 1910 1720*1000* 1910 1720*1000* 1910
Inlet/outlet connection DN 50 50 65 65 65 80 80 100 100
Heating area 480-720 720-960 860-1100 960-1440 1280-1920 1440-2160 1920-2880 1920-2880 2560-3840
Heat dissipation of enclosure % ≤2 ≤2 ≤2 ≤2 ≤2 ≤2 ≤2 ≤2 ≤2
Max. volume of heating L 1100 1480 1840 2200 2960 3300 4400 4400 5866
Heating space 1920-2400 2560-3200 2560-3200 4150-5740 6000-8000 6300-8550 8300-11480 8300-11480 11040- 15300
Electric meter A 3-phase power meter 1.5-1.6A, metering transformer needs to be installed rationally by professional personnel
Protection grade IP 33
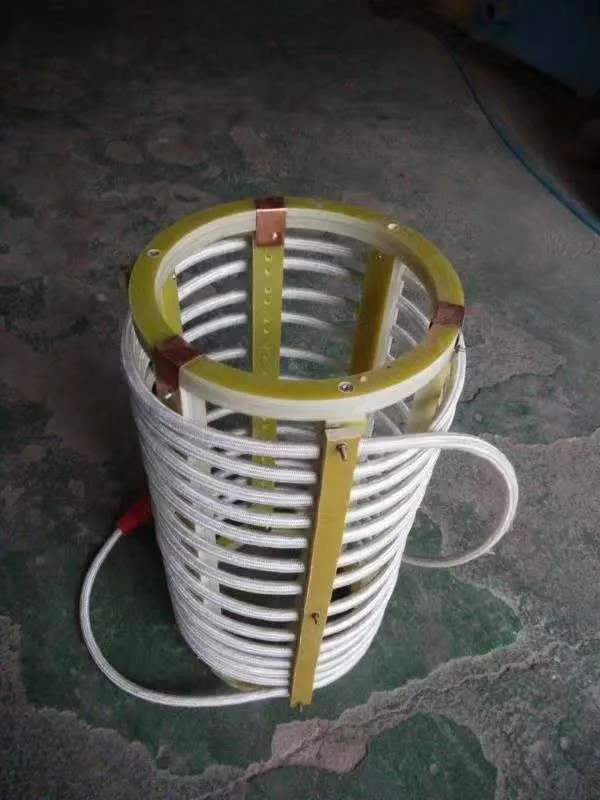
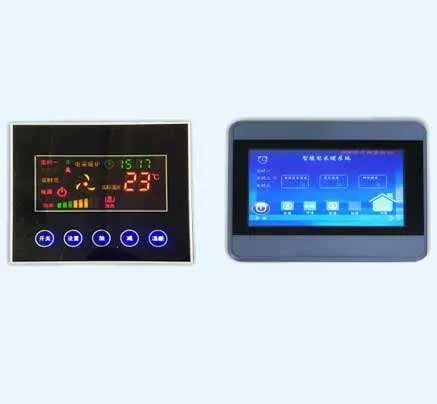
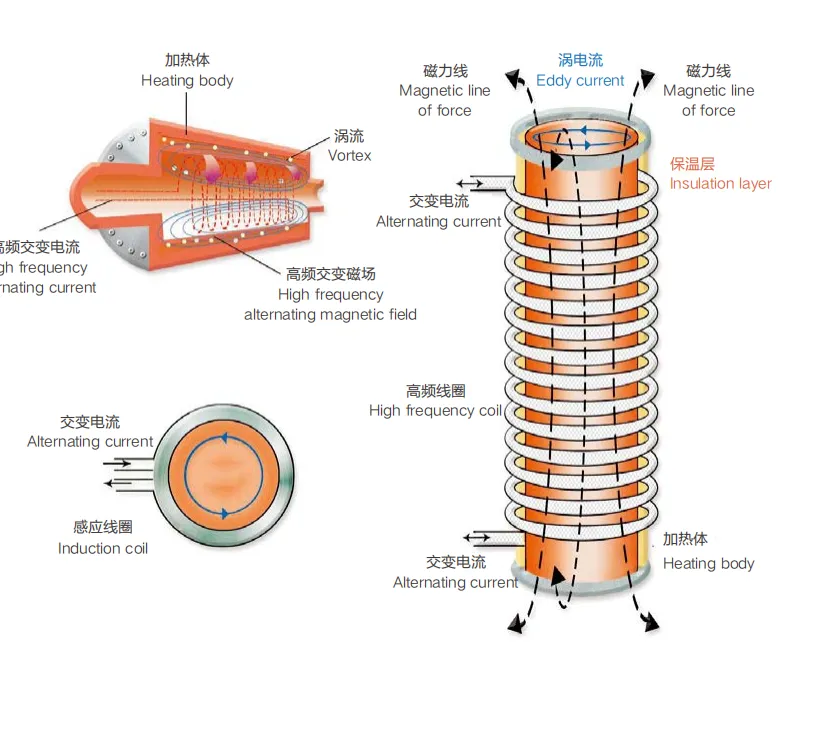
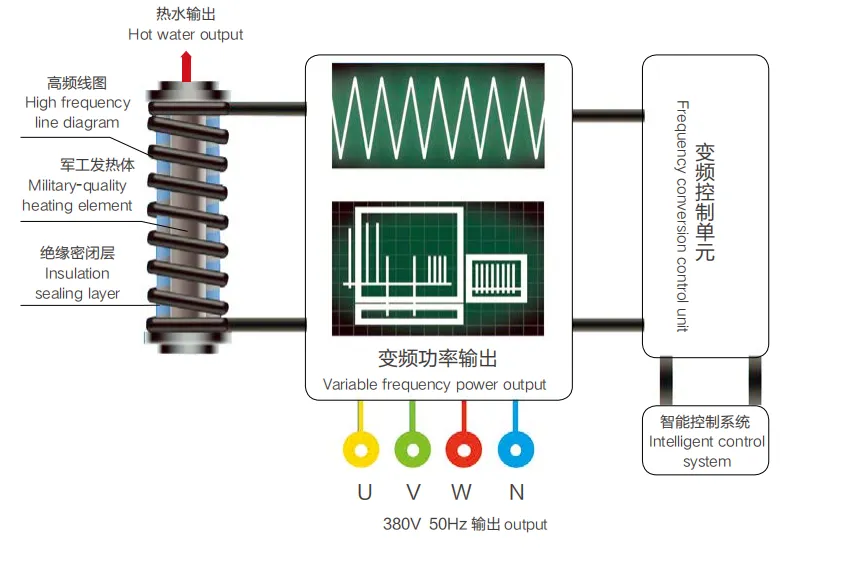
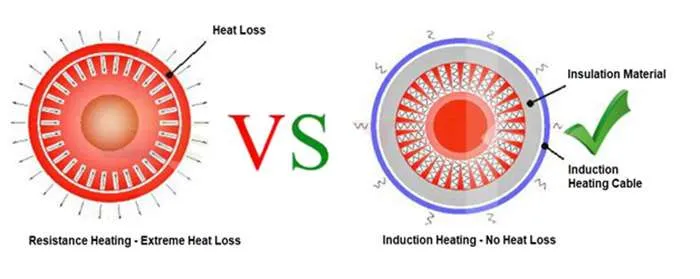
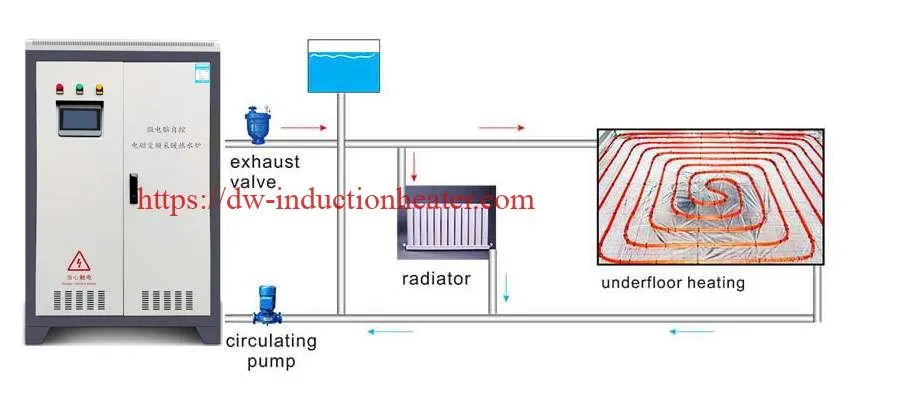
  The Principle of Induction Heating Hot Water Boiler Features 1.Energy Saving When the indoor temperature exceeds the pre-set value, the central heating boiler will be automatically turned off, thus efficiently saving more than 30% energy. And it can save energy by 20% in comparison with traditional boilers that use resistance heating method.Constant Temperature and Comfortable Space Water temperature can be controlled within a range of 5~90ºC, and the precision of temperature control can reach ±1ºC, providing a comfortable atmosphere for your space. Unlike air conditioning equipment, induction heating does not create an ideal environment for bacteria to grow. 2.No Noise In contrast to central heating boilers using air cooling method, water cooled heating boilers are more quiet and unobtrusive. 3.Safe Operation Utilizing induction heating achieves separation of electricity and water, providing a safer operation. Besides, multiple protection functions such as antifreeze protection, electricity leakage protection, short circuit protection, phase loss protection, overheating protection, overcurrent protection, overvoltage protection, undervoltage protection, self-inspection protection are equipped. Safe usage is guaranteed for 10 years. 4.Intelligent Control Our induction water heating boilers can be WIFI remotely controlled by smart phones. 5.Easy to Maintain Induction heating do not constitute the condition of fouling, eliminating the need for fouling removing treatment.   FAQ Please Contact Our Customer Service before Make a Purchase   About Choosing Appropriate Power Choosing a suitable boiler based on your actual heating area For low-energy buildings, 60~80W/m² boilers are suitable; For general buildings, 80~100W/m² boilers are suitable; For villas and bungalows, 100~150W/m² boilers are suitable; For those buildings where sealing performance is not well and room height is greater than 2.7m or people frequently enter, the building heat load is correspondingly increased and the power of central heating boiler should be higher.   About Installation Conditions What are installation conditions Take a 15kW induction central heating boiler as an example: The cross section are of main power cable should not be less than 6mm3, main switch 32~45A, voltage 380V/50, minimum water flow of pump is 25L/min, the water pump needs to be selected according to building height. About Accessories What accessories are required Since every installation site of customer is different, so that various accessories are required. We only provide central heating boilers, other accessories such as pump valve, piping and union connectors need to be purchased by customers.   About Connections For Heating What are applicable connections for heating HLQ’s induction central heating boilers can be flexibly connected to floor heating system, radiator, hot water storage tank, fan coil unit (FCU), etc.   About Installation Service Our products can be installed by our authorized local dealers. We also accept advance reservation, and we designate engineers to offer installation service and technical guidance on site.   About Logistics Shipping time and logistic distribution We promise to ship our ready-to-ship products within 24 hours, and ship our made-to-order products within 7-10 days. And the logistics service is based on customers’ requirements.   About Service Life How long is this product’s service life HLQ’s induction central heating boiler adopts high-frequency induction coil and industrial grade inverter, all key parts are made of imported high grade materials, its service life can reach 15 years or more.     https://dw-inductionheater.com/hot-water-boiler-with-induction-heating.html?feed_id=233056&_unique_id=65b5c5dc49c10

Removal Paint With Induction Heating For Pipeline and Steel Plate

Induction RPR System, Removal Paint With Induction Heating For Pipeline and Steel Plate

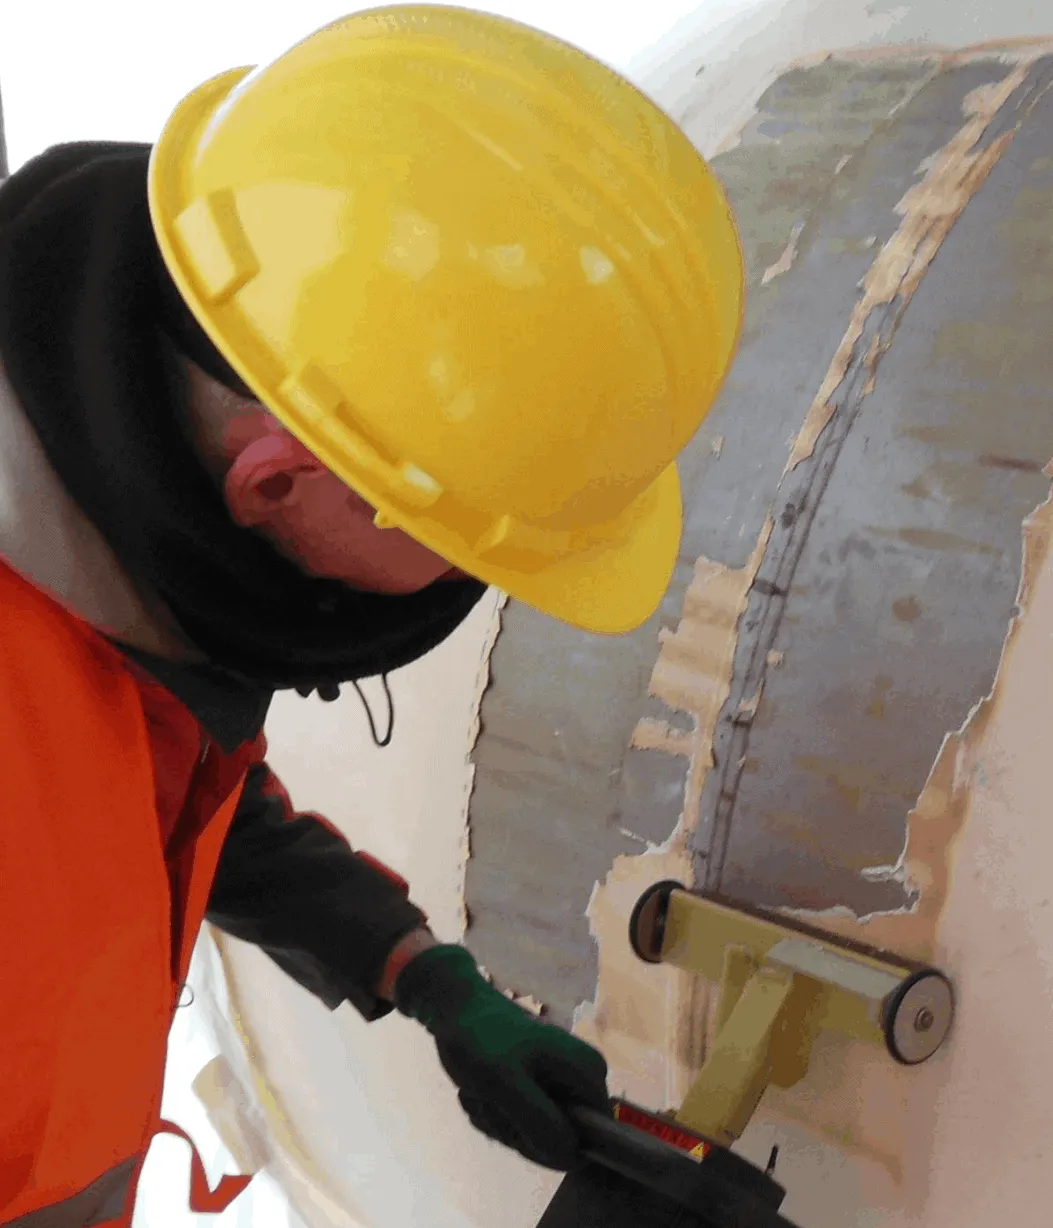
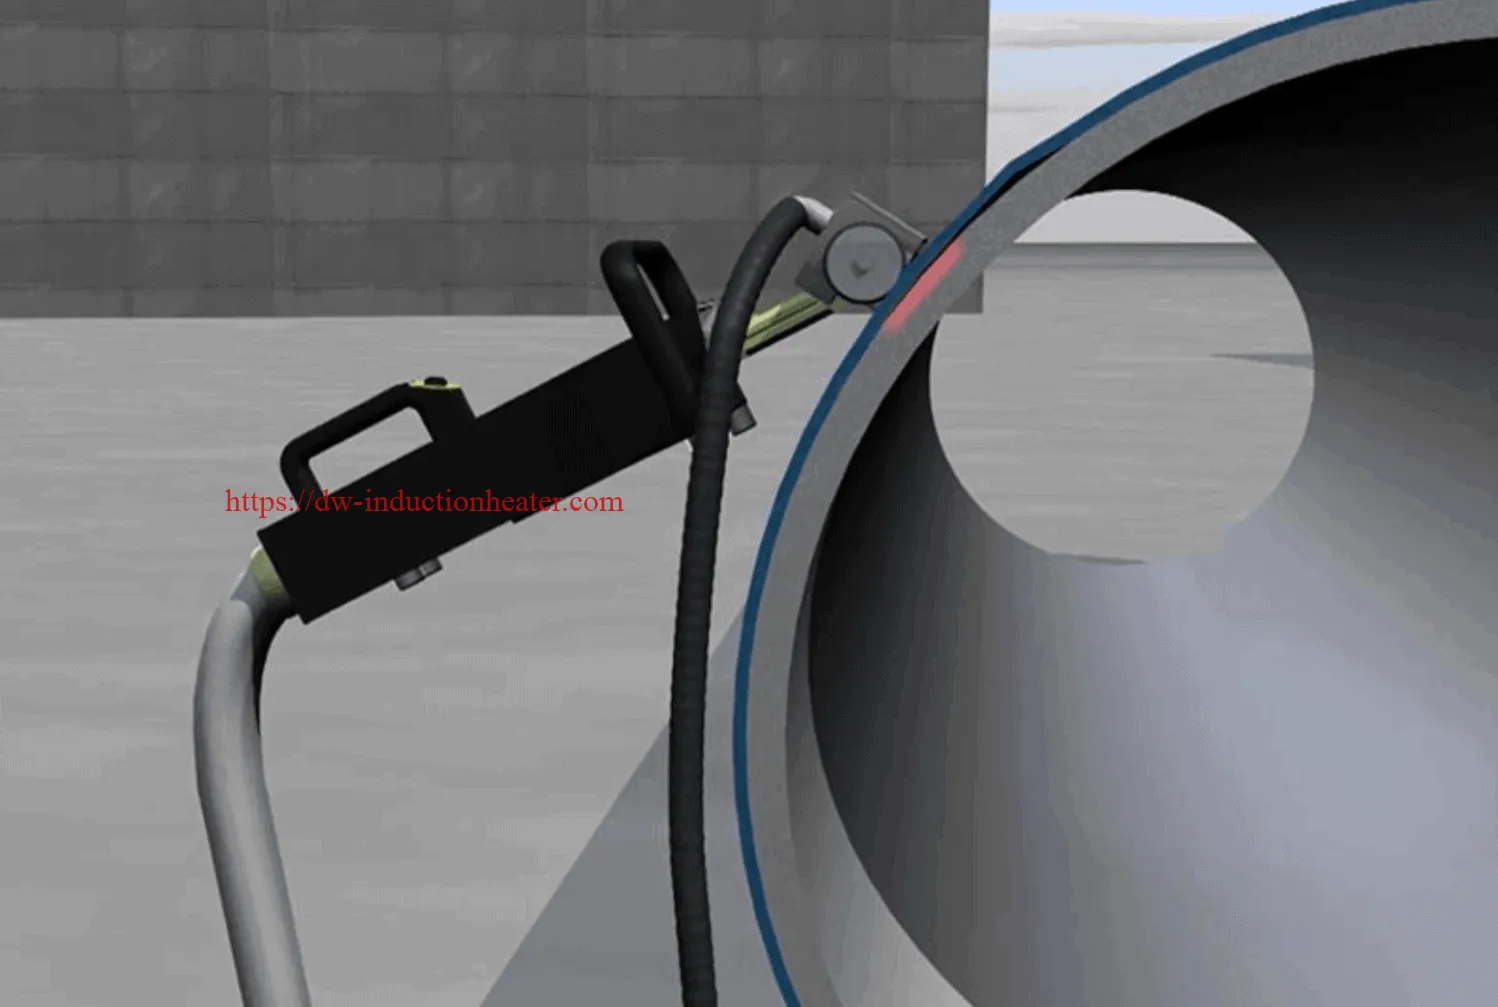
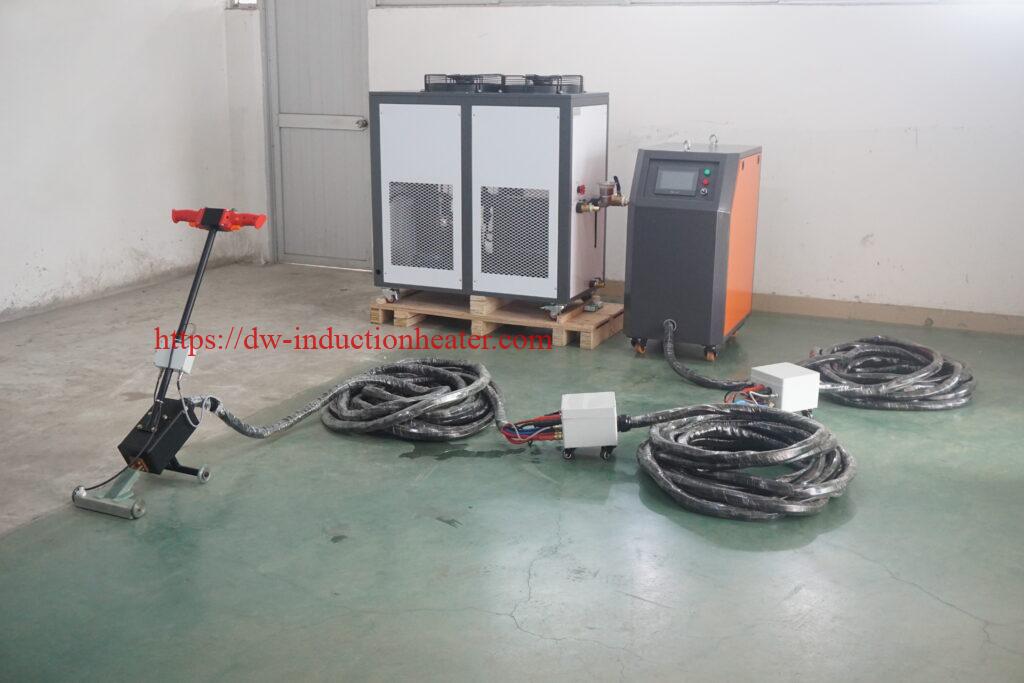
HLQ Long distance RPR induction coating removal heater is consisted of medium frequency induction heating generator, long distance cable and hand-held heating head. Power ranges from 30 to 60KW, and output frequency 20KHz around, cable length can be 20 or 40m long. HLQ RPR induction coating removal heater can be used for heating for coatings removing,rubber removal,paint removal,copper connector brazing, copper tube brazing, surface heating,etc.

[caption id="attachment_6966" align="alignnone" width="1024"] RPR Induction coating removal heater[/caption]
Working theory and acteristics

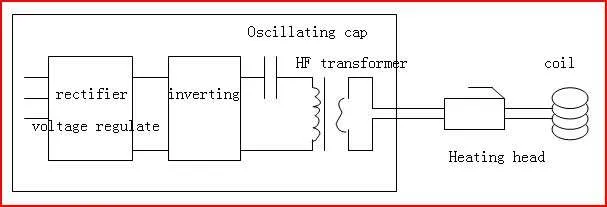
HLQ induction heating machines adopt series oscillating circuit, inverting high frequency power is output through transformer and oscillating cap to the heating head, and then output to coil for heating. In HLQ RPR Induction Coating Removal Heater, our latest third generation inverting and adjust technologies are adopted to realize soft switching of the IGBT components and independent adjusting of the power and frequency, so as to reach a marvelous heating feature of the machine.
Model DWS-25P DWS-30P DWS-60P
Max input power 25kw 30kw 60kw
Length of heating head 20M 20-40M
Output frequency 20-50KHz
Output current 5~45A 6-54A 12-108A
Output voltage 70~520V
Input voltage 380V,3phases,50/60Hz
Duty cycle 50%
Cooling water ≥0.5MPa ≥30L/min
Inner water chiller Yes
Weight Generator 280KG 316KG 580KG
Heating head 2.2KG 2.7KG 4.5KG
Size/cm Generator 103L×750W×156.6H 103L×750W×156.6H 70L×40W×103.5H
Heating head Ф6.5×16.5L Ф8×18.5L Ф11.8×24L

How RPR induction coating removal | RPR Induction Stripping Works?

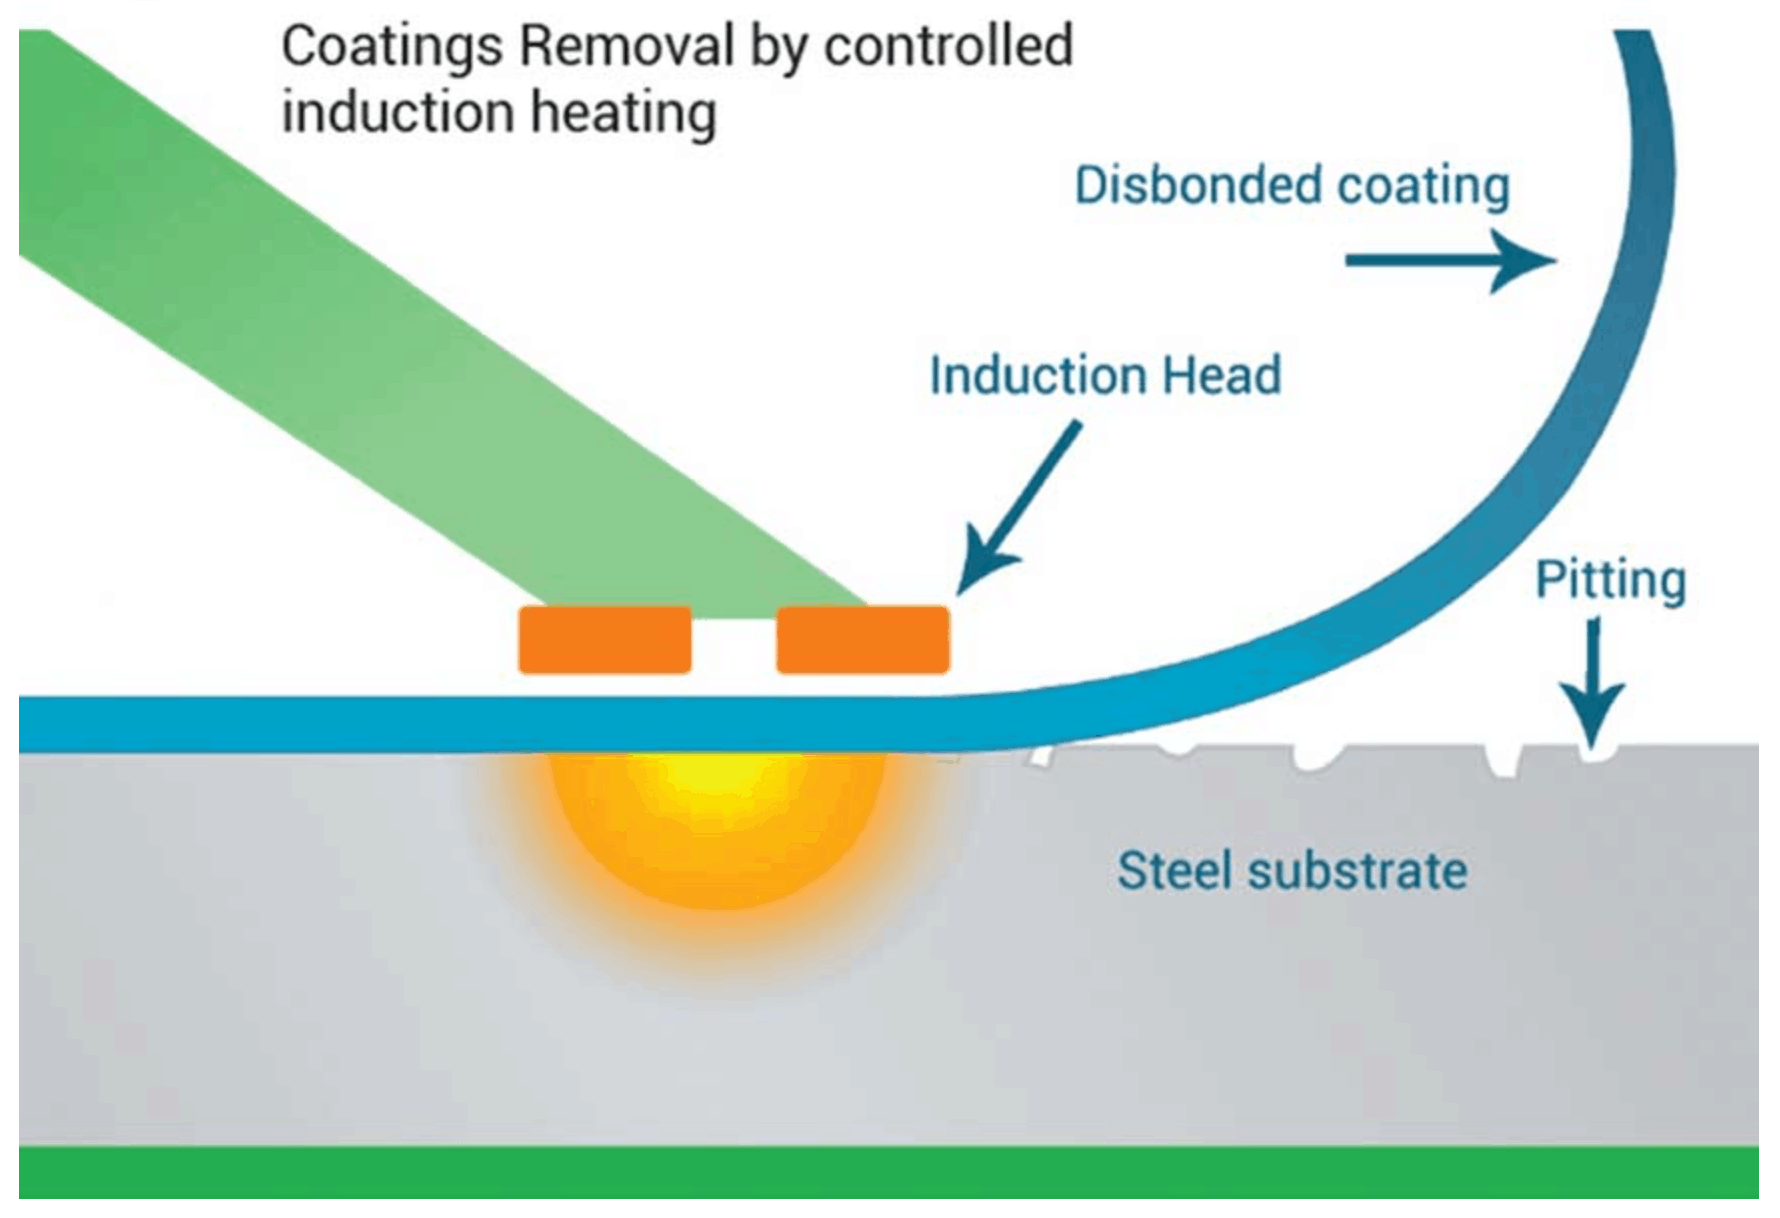
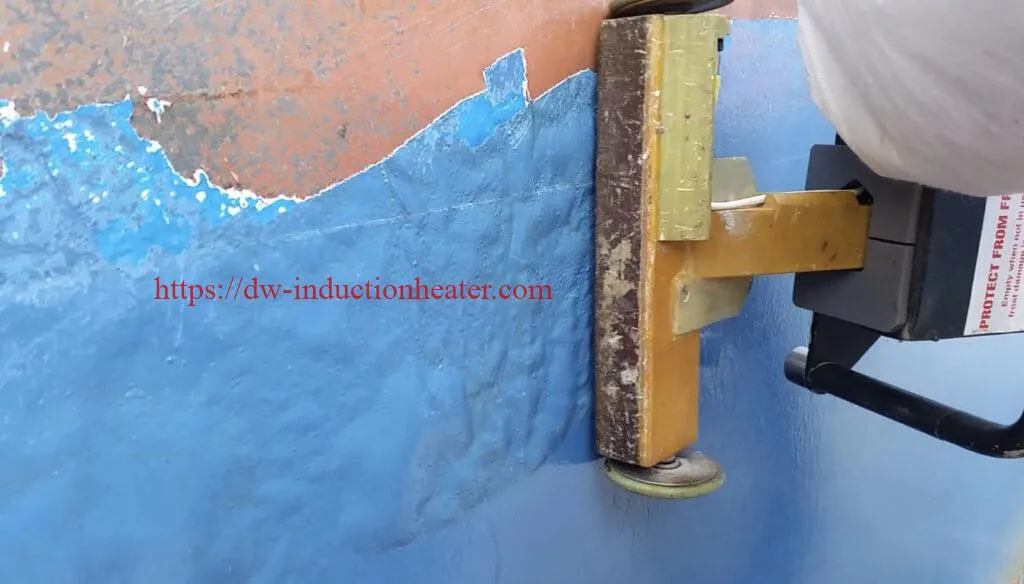
RPR induction coating removal | Induction stripping is a hot surface preparation process.An induction heating generator sends alternating current through an induction coil, which generates an electromagnetic field. This field induces currents that are converted into heat in contact with conducting materials such as steel. The heat is generated beneath the coating, causing the coating to peel rapidly. This method is suitable for treating flat or curved surfaces on the jobsite and does not require any confinement. The RPR induction coating removal|induction stripping system will strip paint, other coatings, heavy rust, bacterial corrosion and oil and grease electrically conductive surfaces (ferromagnetic steel) breaking the interfacial bonding between the material and the substrate etch residues, induction heating localized and controlled which consumes minimal energy. HLQ simplifies your coatings removal needs with yet another revolutionary technology: Induction Stripping! HLQ’s induction stripping equipment removes your toughest coatings from steel structures with no noise or secondary waste—getting right down to the steel.
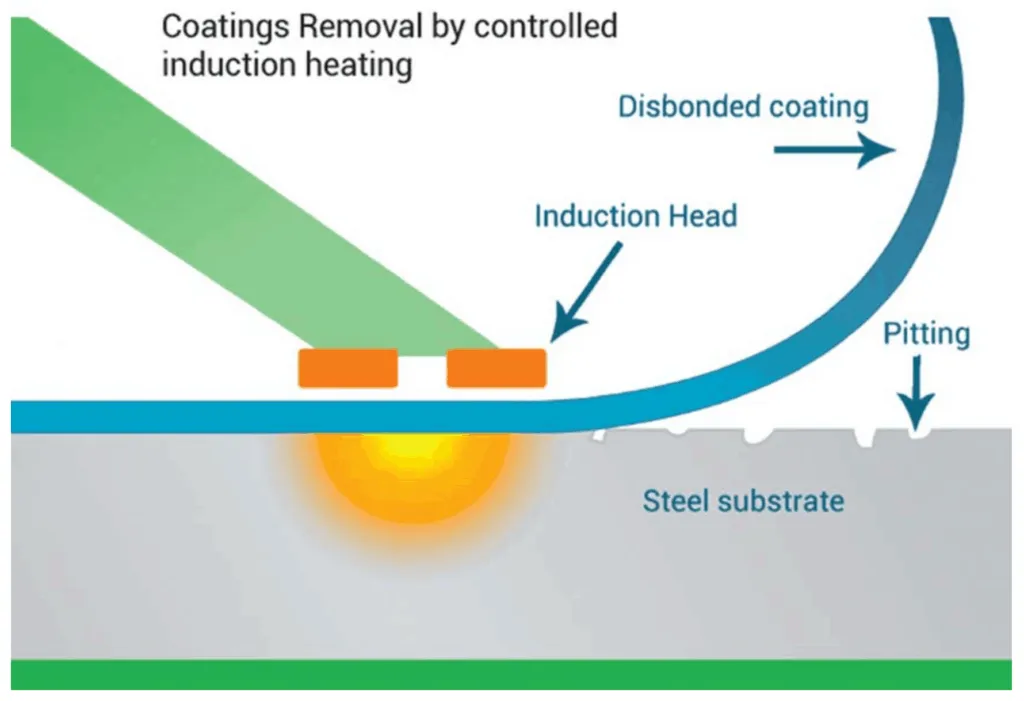
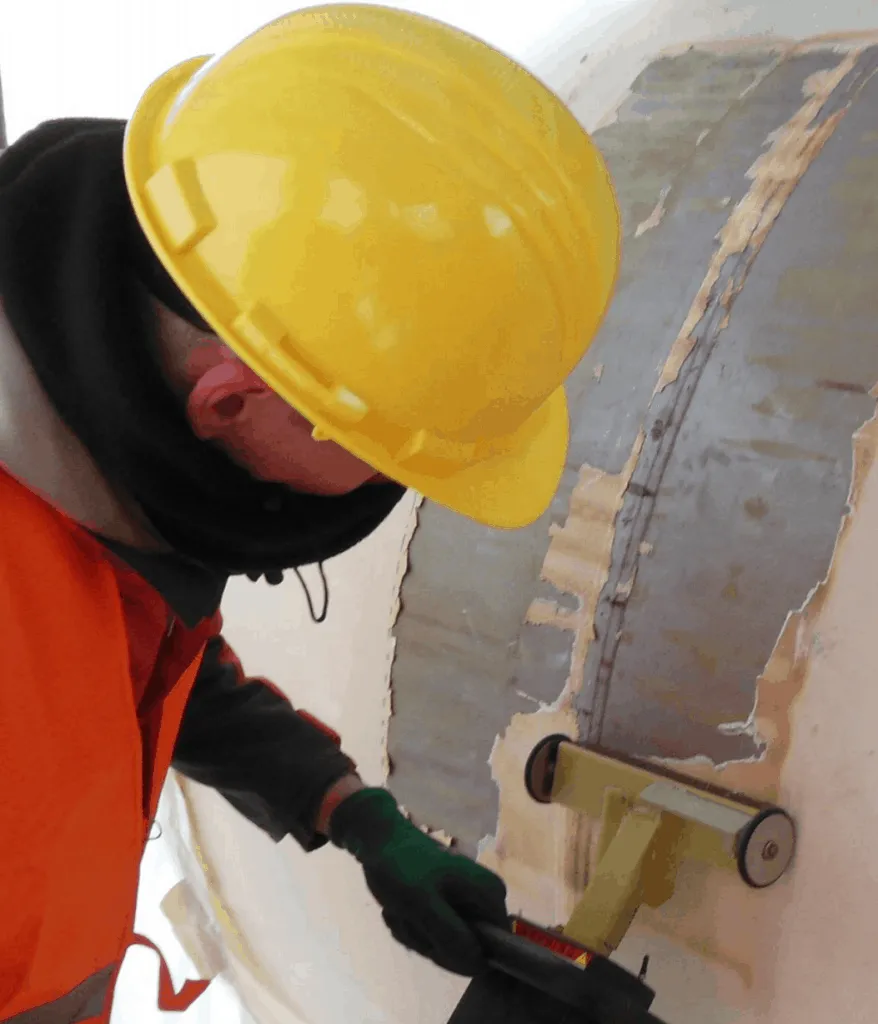
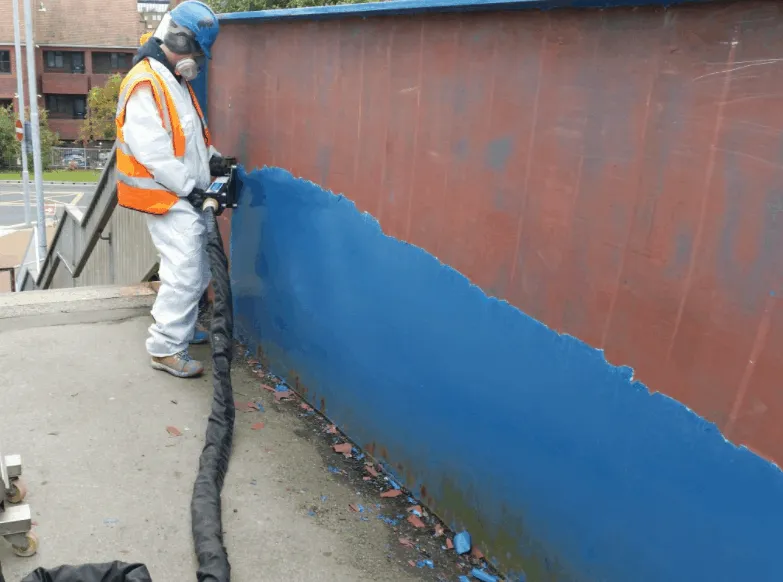
If you have ever wished for a magic wand to solve your coatings removal headaches, HLQ has the next best thing. HLQ technician can wave our induction wand over your coating catastrophe and dis-bond some of the hardest to remove coatings at rates that are up to 10 times faster than competing technologies like sandblasting.It’s not magic, but our induction stripping technology is a close second! When HLQ technicians move our induction head over a steel surface, it creates sufficient heat (typically 300 to 400 degrees) to quickly unbond most coatings from tanks, tankers, pipelines, ships and offshore platforms, allowing coatings (up to 1-inch thick) to be removed in sheets. RPR Heat Induction coating removal works by the principle of induction. Heat is generated in the steel substrate and the bond at the steel and coating interface is broken. The coating is then removed entirely without disintegrating and completely free from contaminating agents, i.e.. blast media. This makes disposal and recycling of waste easier and more cost effective.   With minimum power consumption even the thickest and hardest coatings can be completely removed. RPR  Induction Coating Removal  is faster than conventional methods. A silent method of coating removal means that our engineers can operate day or night with no noise pollution. Because of the many advantages of our induction heating process, we’ve been able to provide a wide range of Alliance customers with the service they need. We’ve worked with customers in industries such as:
  • Oil & gas
  • Financial
  • Food & beverage processing
  • Retail and food services
  • Marine
  • Hotels & hospitality
  • Commercial pools and aquariums
HLQ’s jaw-dropping induction dis-bonding process removes most coating types, including:
  • Coal Tar Epoxy
  • Polyethylene
  • Fiberglass
  • Anti-skid
  • Rubber
  • Chartek fireproofing or other intumescent coatings
Faster, Quieter, Cleaner, Safer Surface Preparation

A faster, safer and cleaner method for removing industrial coatings from steel surfaces. Some might say induction stripping is the “quick and dirty” way to get the job done, but truthfully it’s quick, and not messy at all. Because induction stripping creates no secondary waste, cleanup is simplified. Dealing with sheets or strips of coating is infinitely easier than dealing with blast media and dust.
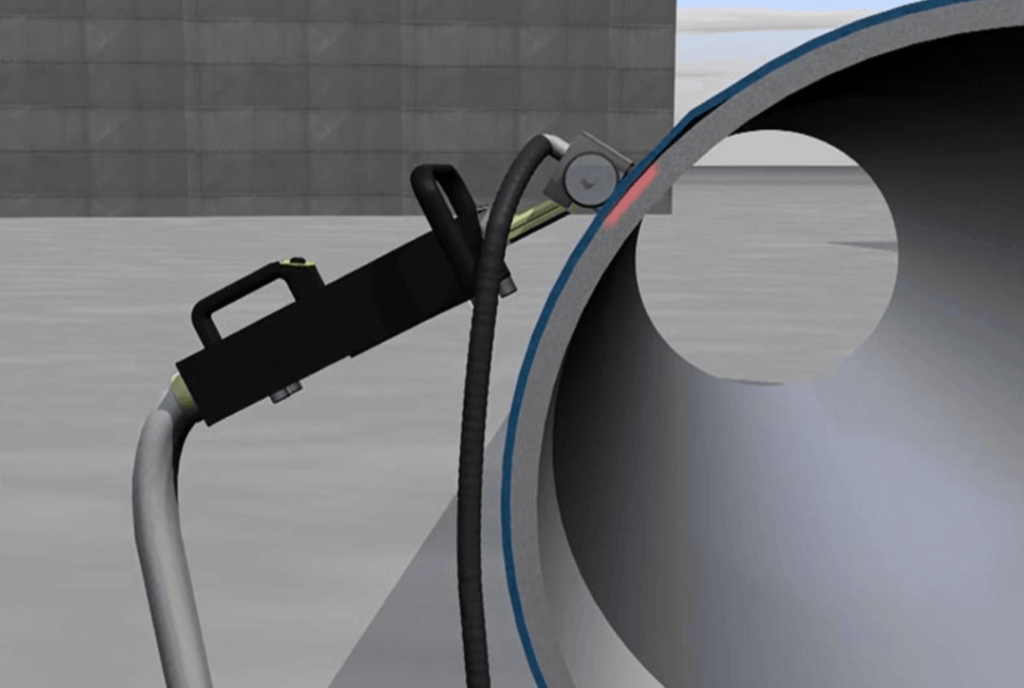
In many cases, containment can be simplified or eliminated altogether. Imagine eliminating a costly scaffolding and containment project and replacing it with a snorkel lift and a drop cloth! Other trades can work in close proximity to HLQ’s induction stripping activities because it is a very quiet process that will not create obnoxious noises that disrupt the productivity of other contractors you may have working on your project. Our induction stripping equipment has no moving parts, making our process much safer than hydro-blasting or sandblasting for your employees, other contractors, customers and passersby. RPR induction removes paint, coatings, thick rust, bacterial corrosion and oil & grease residues from electrically conductive surfaces (steel, etc.) by breaking the interfacial bonding between the material to be removed and the substrate using controlled, localized induction heating with a mini- mum consumption of energy.
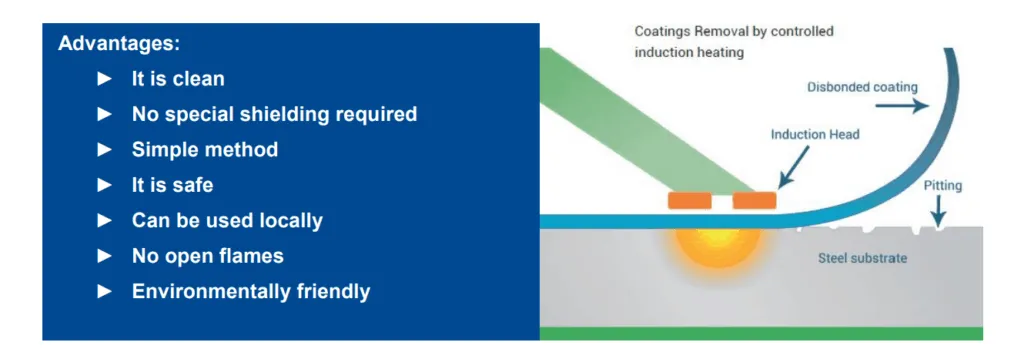
The induction heating principle

The RPR induction generator sends alternating current through an induction heating coil, which gener- ates an electro-magnetic field. This magnetic field induces eddy currents in a conductive mate- rial like steel. Due to the resistance of the steel, these currents are converted to heat = induction heating. The heat is generated below the coat- ing, resulting in quick and clean disbonding. RPR Heat Induction works by the principle of induction. Heat is generated in the steel substrate and the bond at the steel and coating interface is broken. The coating is then removed entirely without disintegrating and completely free from contaminating agents, i.e.. blast media. This makes disposal and recycling of waste easier and more cost effective. With minimum power consumption even the thickest and hardest coatings can be completely removed. RPR Heat Induction heating is faster than conventional methods. A silent method of coating removal means that our engineers can operate day or night with no noise pollution. The RPR Induction Coating Removal system is ideal for the removing paint, rust, and other coatings (vulcanized rubber, fire protectant, epoxies, etc. with control possibili- ties for the following functions: • Energy consumption • Disbonding temperature range • Heat penetration • Removal speed With above setting possibilities, RPR delivers unequalled performance and is the system of choice for cost-effective, safe and environmentally friendly surface coating removal from steel substrates. RPR is ideal for: marine, tanks, offshore and land-based pipelines
https://dw-inductionheater.com/removal-paint-with-induction-heating-for-pipeline-and-steel-plate.html?feed_id=233026&_unique_id=65b50f09914a4

2024年1月26日星期五

steel plate-shovels hot forming with induction preheating

Steel plate-shovels hot forming with induction preheating system

What is induction pre-heating? Induction preheating is a process where materials or workpieces are heated by induction prior to further processing. The reasons for pre-heating vary. In the cable and wire industry, cable cores are pre-heated before insulation extrusion. Steels strips are pre-heated prior to pickling and zinc coating. Induction pre-heating also softens metals before bending, and prepares tubes and pipes for welding. Mobile pre-heating solutions facilitate onsite repairs of bearing assemblies. The induction preheating process is an efficient means of preheating steel plate-shovels for hot forming. This involves bending or shaping a metal billet after being heated to a temperature at which there is less resistance to forming. Induction Heating Objective: A steel shovel manufacturer is looking for an induction heating solution to replace a gas furnace and achieve temperature uniformity, repeatability, and fast heat cycles. Induction Heating Equipment: High Frequency Induction Heater DW-HF-45KW is the recommended induction heating equipment for this induction preheating application. With this induction heating generator, the customer heats the steel shovel molds sustainably and achieves faster heat cycles, especially for the bigger samples. Induction Heating Process: This application aims to preheat 4 steel plate sheets to 1742 F/950 C before posting them in a press to form them as shovels. The goal is for the shovel to reach the desired temperature in less than 5 seconds. Benefits: Implementing induction heating has significant advantages:
  • Greater thermal efficiency, resulting in substantial decrease in energy consumption.
  • Shorter heating times
  • Improved uniformity
  • Improved working conditions
https://dw-inductionheater.com/steel-plate-shovels-hot-forming-with-induction-preheating.html?feed_id=232996&_unique_id=65b4584045c27

Glass Frit Furnace-High Temperature Frit Furnace

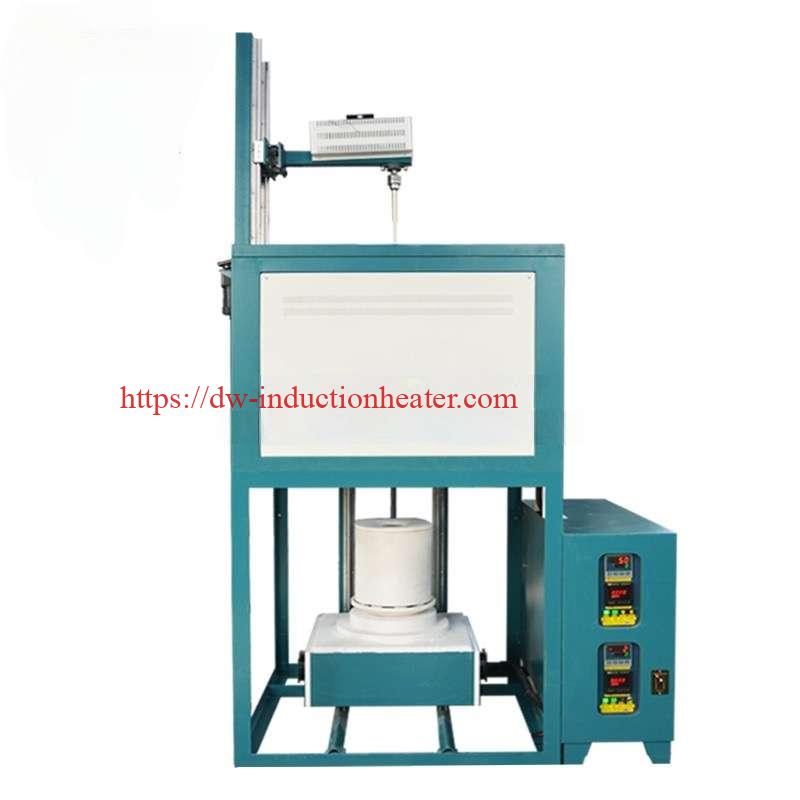
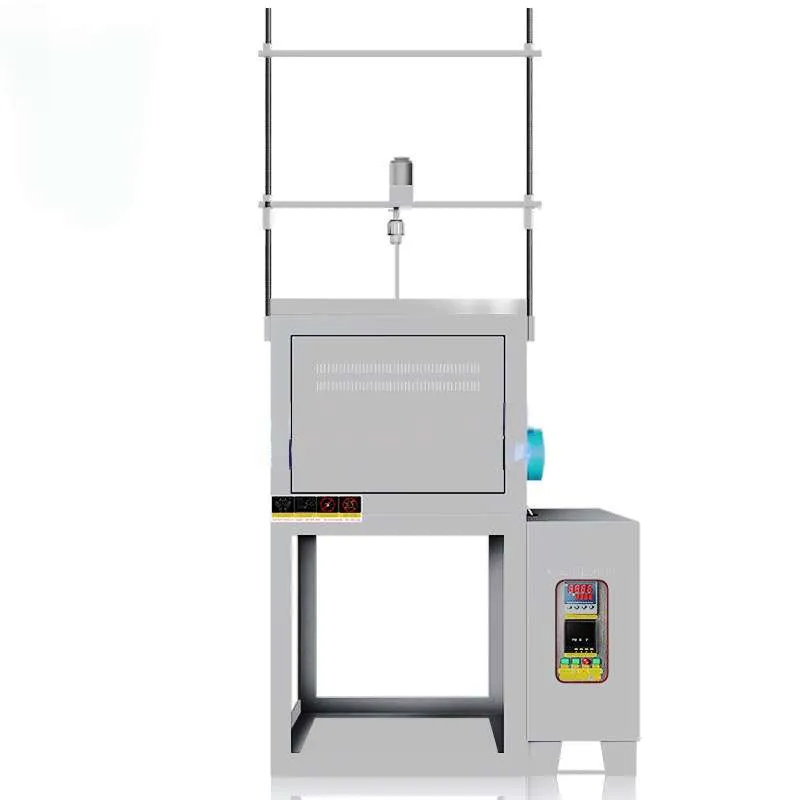
A glass frit furnace | High frit furnace is a type of industrial furnace used for melting and fusing glass frit, which is a powdered form of glass used in various applications such as ceramics, electronics, and decorative arts. The furnace typically operates at high temperatures to melt the glass frit into a liquid state, allowing it to be formed into various shapes and products. These furnaces are commonly used in glass manufacturing facilities and other industries that require the processing of glass materials. High Temperature glass frit furnace equip with Loading platform (for the easy place the crucible, more suitable for large cubage requirements) the lifting system chooses precision screw mandrel, more stable and reliable, the crucible chooses high purity zirconium quartz (99.9%) more durable to use. Characteristic: -Intelligent control,Electromechanical transmission. -The control panel equipped with the intelligent adjustment device, power control switch, main working/stop button,voltmeter、ammeter、Computer interface、Observe port /Air inlet port,for convenience to observe the furnace working status, the product using reliable integrated circuit, excellent working environment, anti-interference, the highest temperature of furnace shell temperature is less than 45℃ can greatly improve the working environment,micro computer program control, programmable setting temperature rise curve,Fully automatic temperature rise / cooling,Temperature control parameters and programs can be modified during operation, which is flexible, convenient and simple in operation. -Furnace hearth materials made up by vacuum forming high purity alumina light materials(Will be changing due to the temperature required), High temperature for use, Less heat storage amount,Tolerance the extremely heating and cold、no crack, No dregs, Excellent thermal insulation performance (the energy saving effect is over 60% of the traditional furnace).Reasonable structure, Double layer furnace cover,Air cooling,Greatly shortening the experimental period. Features: -1750 °C maximum operating temperature; normal operating,temperature range 800 °C - 1700 °C -Maximum crucible cubage 17L (Can be customized) -Double Layer Furnace Shell, With Air Cooling -Double heating system(Loading platform+Furnace chamber) -Simplicity for operation, programmable, pid automatic modify, automatic temperature rise, automatic temperature retaining, automatic cooling, unattended operation; -High speed temperature rise rate. (temperature rise rate 1℃/h to 30℃/min can be modified); -Temperature Control Accuracy:± 1℃, -Temperature Constant Accuracy:±1℃. -Fast Temperature rise rate, Maximum heating rate≤30℃/min.   Options (specify these at time of order) -Control software and system. -Multi-face heating -Anti-corrosion -Multi-temperature control -Touch screen control -Agitation system Applications:  The glass frit furnace is designed for pyrolysis, melting, analysis and production ceramics, metallurgy, electronics, machinery, chemical, glass, refractories, for develop new material, special materials, construction materials, the equipment is suitable for institutions of higher learning and laboratory of scientific research institute and industrial and mining enterprises.
Model GWL Glass Frit Furnace
Working Temperature 1200℃ 1400℃ 1600℃ 1700℃ 1800℃
Maximum Temperature 1250℃ 1450℃ 1650℃ 1750℃ 1820℃
Temperature Control Accuracy ±1℃
Temperature Uniformity ±1℃
Temperature Rise Rate Temperature Rise Rate Can Be Modify(30℃/min | 1℃/h), Company Suggest: 1-20℃/min
Crucible Cubage 1.6L/3L/5L/10L/17L
Heating Element Silicon Carbide Rod Silicon molybdenum rod
Placing Crucible Method Top side to placing crucible and remove
Material Passes in and out Top side to passes in and Bottom side pass out.
Crucible Material High purity zirconium quartz (99.9%)
Cooling Structure Double Layer Furnace Shell, With Air Cooling.
Standard Accessories Heating Elements, Specification Certificate, Heat Insulation Brick, Crucible Pliers, High Temperature Gloves.
Characteristic Can be adding material under high temperature environment, The High temperature solution can be timely outflow. 1. Temperature accuracy:±1℃ ; Constant temperature:±1℃(Base on Heating zone size ) 。 2. Simplicity for operation ,programable,PID automatic modify, automatic temperature rise, automatic temperature retaining , automatic cooling, unattended operation; 3. High Speed Temperature rise rate. (temperature rise rate 1℃/h to 30℃/min can be modify); 4. Energy- Saving (furnace hearth made up by import fiber material, excellent thermostability, Tolerance the extreme heat and cold) 5. Double layer loop protection. (over temperature protection, over pressure protection, over current protection, thermocouple protection, Power supply protection and so on) 6. Furnace surface after spraying plastics it will resistance acid and alkali and also having corrosion-proof, the furnace wall temperature approaching the indoor temperature. 7. Furnace hearth materials: 1200℃:High Purity Alumina Fiber Board; 1400℃:High purity alumina (Contain zirconium) fiberboard;1600℃:Import High Purity Alumina Fiber Board; 1700℃-1800℃:High Purity alumina polymer fiber board. 8. Crucible Cubage below 5L need to equip with an extension plug.
Furnace Hearth Dimension And Crucible Can Be Customized
https://dw-inductionheater.com/product/glass-frit-furnace-high-temperature-frit-furnace?feed_id=232962&_unique_id=65b3b1534a9f8

Brazing Steel Automotive Parts With Induction Heating System

Brazing Steel Automotive Parts With Induction Heating System

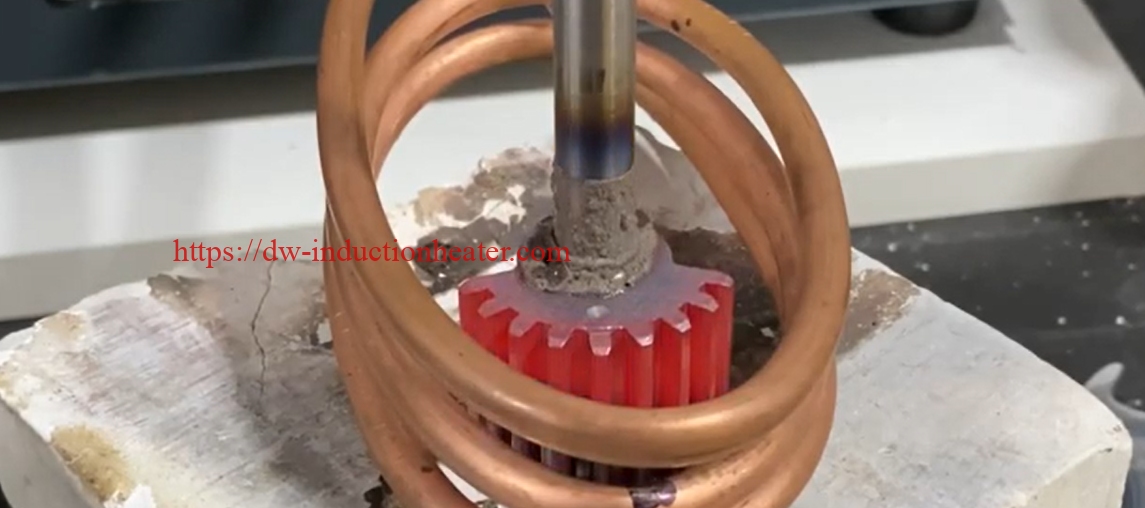
Automotive Parts Use For Induction Heating The automotive industry utilizes many different parts that require heat for assembly. Processes such as brazing, soldering, hardening, tempering, and shrink fitting are common thought-out the automotive industry. These heating processes can be improved significantly through the use of induction heating technology. Induction heating technology can provide many advantages for the auto industry. First and foremost is incredibly precise and consistent control over time and temperature. This means that a process can be performed in exactly the same way with the same results time after time. This reduces the number of rejected parts and thus decreases waste. Induction heating is also extremely clean because it does not involve any sort of combustion. This negates the need for special ventilation and removes key hazards from the workplace such as open flame and compressed gas cylinders. This has the added benefit of opening up more options for plant layout because certain procedures involving heat no longer require transporting parts of the property or to a separate area of the facility. The flexibility of the plant layout is also facilitated by another advantage of induction technology which is the compact footprint. Induction systems often take up less space than other options such as flame, furnace, infrared, or resistance heaters. Automotive Parts Produced with Induction Equipment HLQ Induction Equipment Co has a well-established history of designing induction heating equipment that is used for heat-treating parts for assembly. Bearings Brakes Drive train Gears Joints Shafts Objective:   A manufacturer of steel parts for the automotive industry is interested in upgrading their old induction equipment. HLQ Company received samples of steel shafts, plates, and fittings for the induction brazing test. A challenge for this application was conducting the tests with our induction heater and the client’s induction heating coil. Industry: Automotive & Transportation Equipment: The induction heating power supply we chose for the brazing test was DW-UHF-10kW Induction Heating System. Process:  Our engineers conducted three tests for the three different parts. With each test, the power supply worked with setups of 10kW of induction heating power and a temperature of 1400°F (760°C). The heat cycle time for the first test was 40 sec., and the heat cycle time for the second test was 60 sec. Both were performed with the customer’s single-turn coil. For the third test, we used the customer’s three-turn coil, and the processing time was 30 sec. This application was complete with coils provided by the customer. If a specially designed induction coil is used, the cycle time will be reduced. Benefits:  Investing in new induction heating equipment can optimize the production process on many levels. One of the main goals is to reduce energy costs, which can be achieved with more efficient technology. Additional benefits of induction heating also include increased repeatability and productivity, as well as low maintenance requirements. https://dw-inductionheater.com/brazing-steel-automotive-parts-with-induction-heating-system.html?feed_id=232939&_unique_id=65b3a18a8d226

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.