显示标签为“inductionhotforming”的博文。显示所有博文

2024年4月17日星期三

Induction forging and induction hot forming

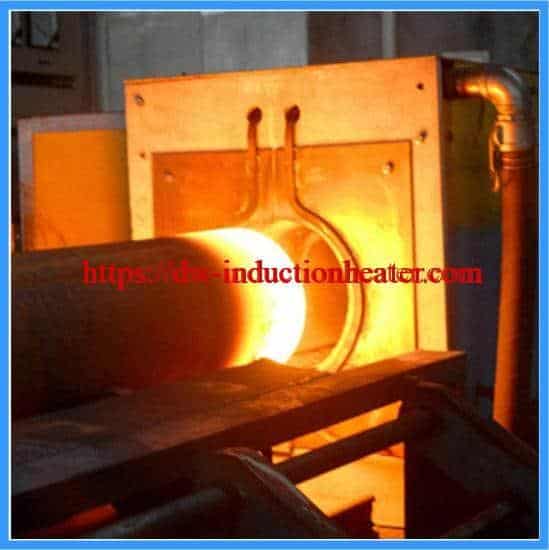
Induction forging machine Induction forging and induction hot forming refer to the use of an induction heating machine to pre-heat metals prior to deformation using a press or hammer. Typically metals are heated to between 1,100 and 1,200 °C (2,010 and 2,190 °F) to increase their malleability and aid flow in the forging die. Metal induction forging and induction hot forming are excellent induction heating applications. Industrial forging and hot forming processes involve bending or shaping a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Blocks of non-ferrous materials can also be used. Induction heating machines or conventional furnaces are used for the initial heating process. Billets can be transported through the inductor via a pneumatic or hydraulic pusher; pinch roller drive; tractor drive; or walking beam. Non-contact pyrometers are used to measure the billet temperature. Other machines such as mechanical impact presses, bending machines, and hydraulic extrusion presses are used to bend or shape the metal. The approximate hot forming temperatures of the most commonly used industrial materials are: • Steel 1200º C • Brass 750º C • Aluminium 550º C

Total Forming Applications

Induction heating machines are commonly used to heat steel billets, bars, brass blocks, and titanium blocks to the proper temperature for forging and hot forming.

Partial Forming Applications

Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts, and bar ends for partial forming and forging processes.Induction hot forming machine

The Induction Heating Advantage

When compared to conventional furnaces, induction heating machines for forging offer significant process and quality advantages:
  • Much shorter heating times, minimizing scaling and oxidation
  • Easy and accurate temperature temperature control. Parts at temperatures outside specifications can be detected and removed
  • No time lost waiting for the furnace to ramp up to the required temperature
  • Automated induction heating machines require minimal manual labor
  • Heat can be directed to one specific point, which is highly important for parts with only one forming area.
  • Greater thermal efficiency - heat is generated in the part itself and does not need to be heated in a large chamber.
  • Better working conditions. The only heat present in the air is that of the parts themselves. The working conditions are much more pleasant than with a fuel furnace.
https://dw-inductionheater.com/induction-forging-and-induction-hot-forming.html?feed_id=241938&_unique_id=661f761073e58

2024年2月10日星期六

Induction Hot Forming Steel Pipe

Induction Hot Forming Steel Pipe

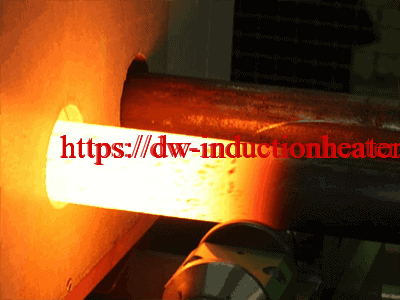
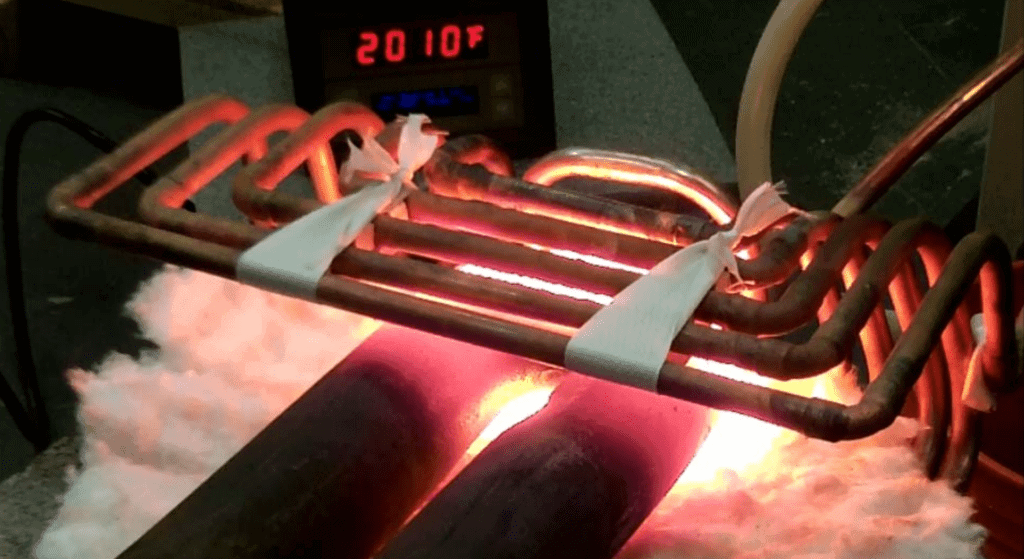
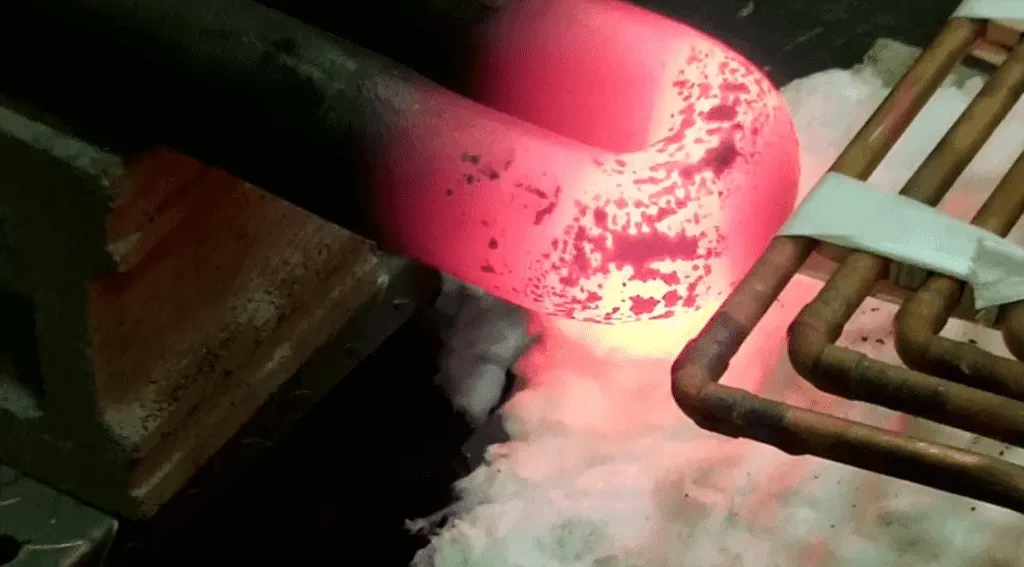
Objective : To heat a magnetic steel pipe to the targeted temperature to enable pipe induction bending; the objective is to create u-bends in pipes for boiler systems Material:  Steel pipes (2.5”/64 mm OD bent steel pipe) Temperature:  2010 °F (1099 °C) Frequency:  8.8 kHz Equipment :  DW-MF-250 kW, 5-15 kHz induction heating power supply with a remote workhead containing eight 6.63 μF capacitors for a total of 53 μF. - A single position six-turn channel induction heating coil designed and developed for this application Process:  The steel pipe was placed inside the induction coil, and it heated to temperature within 120 seconds with an DW-MF- 250kW/10 kHz induction heating system. Results/Benefits: Speed: A large steel pipe heated to the targeted temperature quickly - Repeatability: Induction is highly repeatable and easy-tointegrate into manufacturing processes - Precise heating: Induction is able to target the portion of the tube that requires bending while not heating the remainder of the tube - Energy efficiency: Induction offers fast, flameless, instant on/instant off heating https://dw-inductionheater.com/induction-hot-forming-steel-pipe.html?feed_id=233806&_unique_id=65c7a023646c2

2024年1月26日星期五

steel plate-shovels hot forming with induction preheating

Steel plate-shovels hot forming with induction preheating system

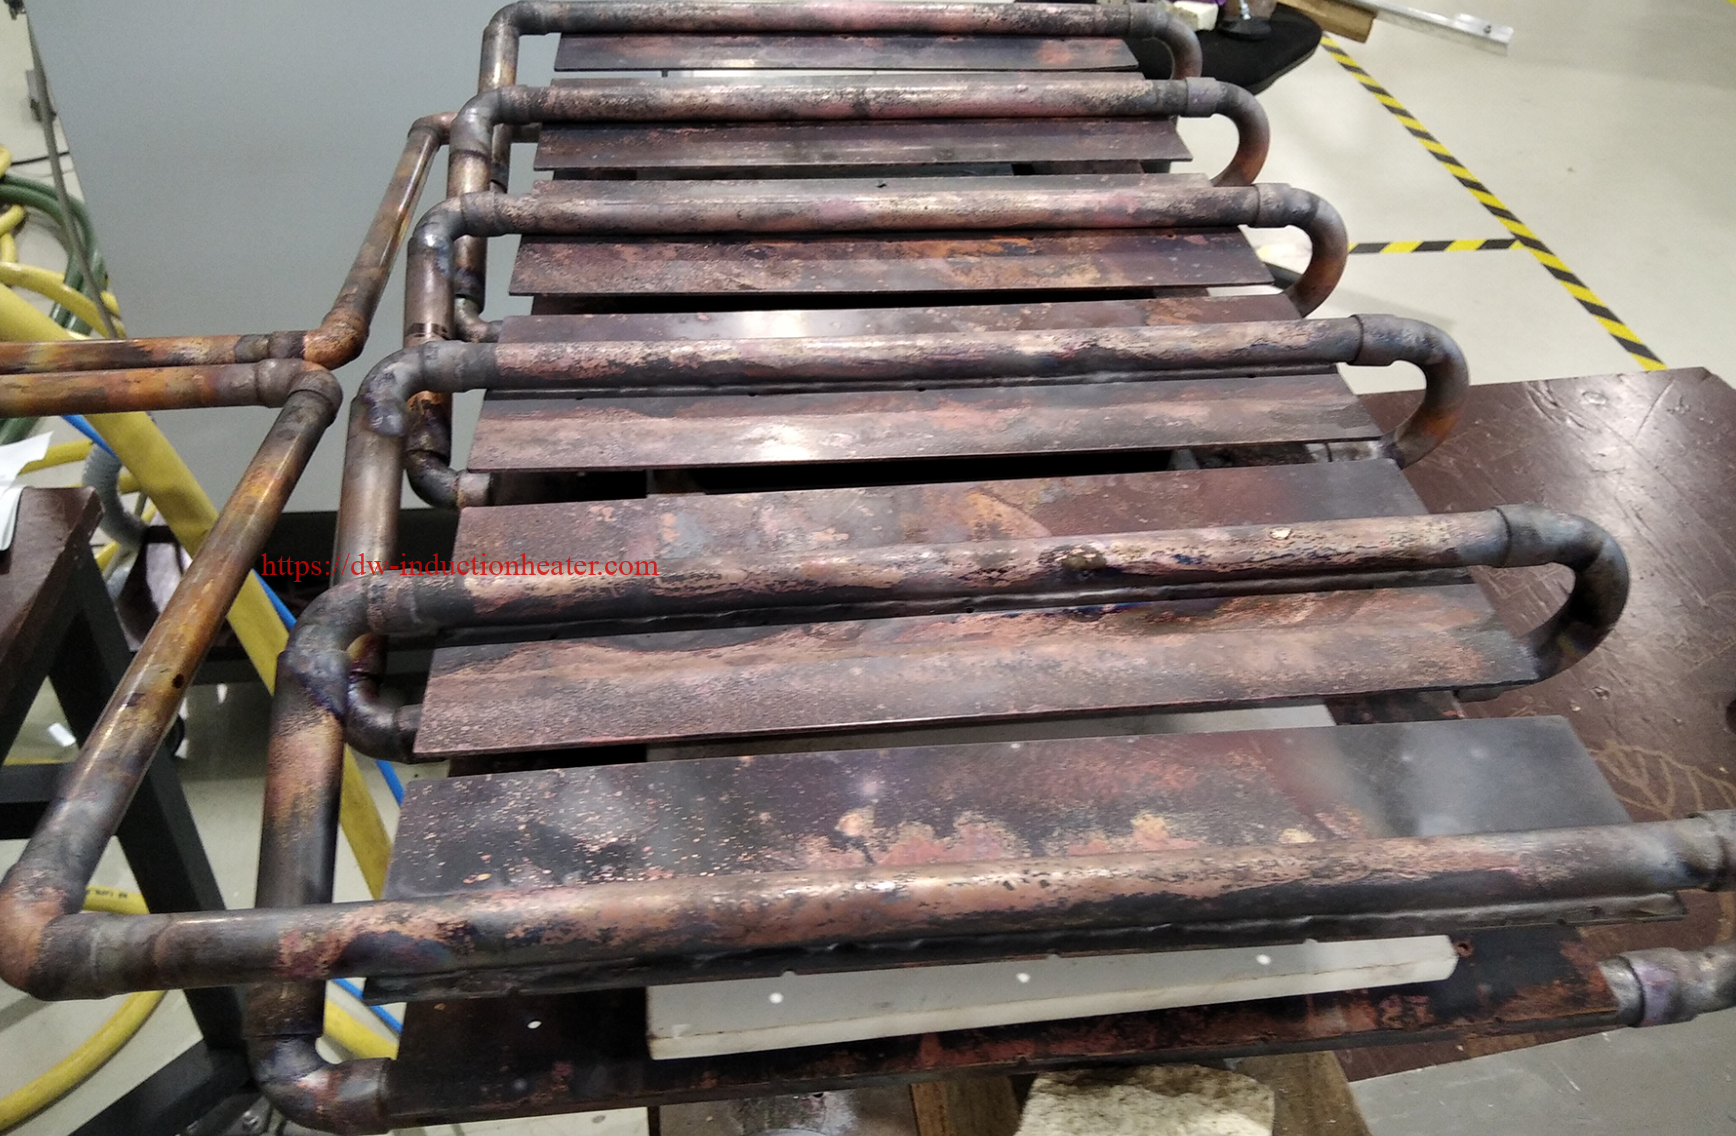
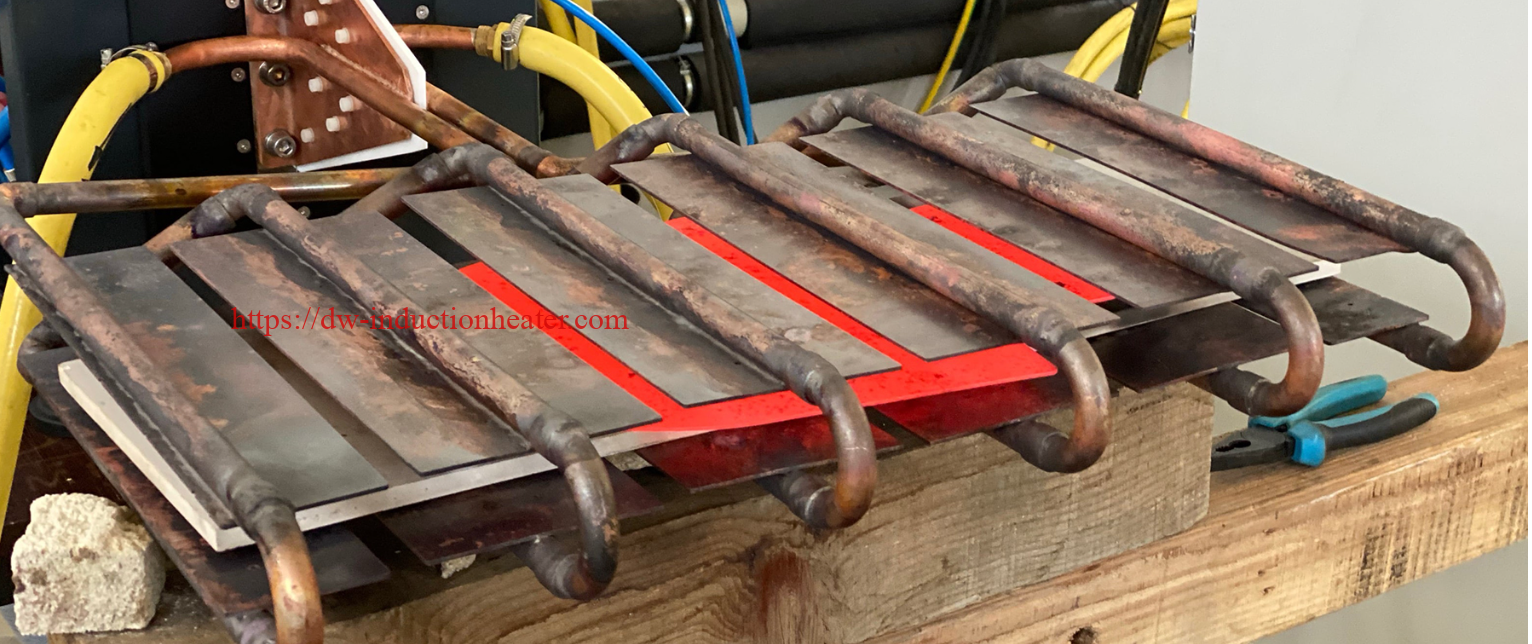
What is induction pre-heating? Induction preheating is a process where materials or workpieces are heated by induction prior to further processing. The reasons for pre-heating vary. In the cable and wire industry, cable cores are pre-heated before insulation extrusion. Steels strips are pre-heated prior to pickling and zinc coating. Induction pre-heating also softens metals before bending, and prepares tubes and pipes for welding. Mobile pre-heating solutions facilitate onsite repairs of bearing assemblies. The induction preheating process is an efficient means of preheating steel plate-shovels for hot forming. This involves bending or shaping a metal billet after being heated to a temperature at which there is less resistance to forming. Induction Heating Objective: A steel shovel manufacturer is looking for an induction heating solution to replace a gas furnace and achieve temperature uniformity, repeatability, and fast heat cycles. Induction Heating Equipment: High Frequency Induction Heater DW-HF-45KW is the recommended induction heating equipment for this induction preheating application. With this induction heating generator, the customer heats the steel shovel molds sustainably and achieves faster heat cycles, especially for the bigger samples. Induction Heating Process: This application aims to preheat 4 steel plate sheets to 1742 F/950 C before posting them in a press to form them as shovels. The goal is for the shovel to reach the desired temperature in less than 5 seconds. Benefits: Implementing induction heating has significant advantages:
  • Greater thermal efficiency, resulting in substantial decrease in energy consumption.
  • Shorter heating times
  • Improved uniformity
  • Improved working conditions
https://dw-inductionheater.com/steel-plate-shovels-hot-forming-with-induction-preheating.html?feed_id=232996&_unique_id=65b4584045c27

2023年8月25日星期五

Induction forging and induction hot forming

Induction forging machine Induction forging and induction hot forming refer to the use of an induction heating machine to pre-heat metals prior to deformation using a press or hammer. Typically metals are heated to between 1,100 and 1,200 °C (2,010 and 2,190 °F) to increase their malleability and aid flow in the forging die. Metal induction forging and induction hot forming are excellent induction heating applications. Industrial forging and hot forming processes involve bending or shaping a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Blocks of non-ferrous materials can also be used. Induction heating machines or conventional furnaces are used for the initial heating process. Billets can be transported through the inductor via a pneumatic or hydraulic pusher; pinch roller drive; tractor drive; or walking beam. Non-contact pyrometers are used to measure the billet temperature. Other machines such as mechanical impact presses, bending machines, and hydraulic extrusion presses are used to bend or shape the metal. The approximate hot forming temperatures of the most commonly used industrial materials are: • Steel 1200º C • Brass 750º C • Aluminium 550º C

Total Forming Applications

Induction heating machines are commonly used to heat steel billets, bars, brass blocks, and titanium blocks to the proper temperature for forging and hot forming.

Partial Forming Applications

Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts, and bar ends for partial forming and forging processes.Induction hot forming machine

The Induction Heating Advantage

When compared to conventional furnaces, induction heating machines for forging offer significant process and quality advantages:
  • Much shorter heating times, minimizing scaling and oxidation
  • Easy and accurate temperature temperature control. Parts at temperatures outside specifications can be detected and removed
  • No time lost waiting for the furnace to ramp up to the required temperature
  • Automated induction heating machines require minimal manual labor
  • Heat can be directed to one specific point, which is highly important for parts with only one forming area.
  • Greater thermal efficiency - heat is generated in the part itself and does not need to be heated in a large chamber.
  • Better working conditions. The only heat present in the air is that of the parts themselves. The working conditions are much more pleasant than with a fuel furnace.
https://dw-inductionheater.com/induction-forging-and-induction-hot-forming.html?feed_id=224836&_unique_id=64e8ce2947895

2023年8月15日星期二

Induction Hot Forming Steel Pipe

Induction Hot Forming Steel Pipe

Objective : To heat a magnetic steel pipe to the targeted temperature to enable pipe induction bending; the objective is to create u-bends in pipes for boiler systems Material:  Steel pipes (2.5”/64 mm OD bent steel pipe) Temperature:  2010 °F (1099 °C) Frequency:  8.8 kHz Equipment :  DW-MF-250 kW, 5-15 kHz induction heating power supply with a remote workhead containing eight 6.63 μF capacitors for a total of 53 μF. - A single position six-turn channel induction heating coil designed and developed for this application Process:  The steel pipe was placed inside the induction coil, and it heated to temperature within 120 seconds with an DW-MF- 250kW/10 kHz induction heating system. Results/Benefits: Speed: A large steel pipe heated to the targeted temperature quickly - Repeatability: Induction is highly repeatable and easy-tointegrate into manufacturing processes - Precise heating: Induction is able to target the portion of the tube that requires bending while not heating the remainder of the tube - Energy efficiency: Induction offers fast, flameless, instant on/instant off heating

2023年7月24日星期一

Induction forging and induction hot forming

Induction forging machine Induction forging and induction hot forming refer to the use of an induction heating machine to pre-heat metals prior to deformation using a press or hammer. Typically metals are heated to between 1,100 and 1,200 °C (2,010 and 2,190 °F) to increase their malleability and aid flow in the forging die. Metal induction forging and induction hot forming are excellent induction heating applications. Industrial forging and hot forming processes involve bending or shaping a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Blocks of non-ferrous materials can also be used. Induction heating machines or conventional furnaces are used for the initial heating process. Billets can be transported through the inductor via a pneumatic or hydraulic pusher; pinch roller drive; tractor drive; or walking beam. Non-contact pyrometers are used to measure the billet temperature. Other machines such as mechanical impact presses, bending machines, and hydraulic extrusion presses are used to bend or shape the metal. The approximate hot forming temperatures of the most commonly used industrial materials are: • Steel 1200º C • Brass 750º C • Aluminium 550º C

Total Forming Applications

Induction heating machines are commonly used to heat steel billets, bars, brass blocks, and titanium blocks to the proper temperature for forging and hot forming.

Partial Forming Applications

Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts, and bar ends for partial forming and forging processes.Induction hot forming machine

The Induction Heating Advantage

When compared to conventional furnaces, induction heating machines for forging offer significant process and quality advantages:
  • Much shorter heating times, minimizing scaling and oxidation
  • Easy and accurate temperature temperature control. Parts at temperatures outside specifications can be detected and removed
  • No time lost waiting for the furnace to ramp up to the required temperature
  • Automated induction heating machines require minimal manual labor
  • Heat can be directed to one specific point, which is highly important for parts with only one forming area.
  • Greater thermal efficiency - heat is generated in the part itself and does not need to be heated in a large chamber.
  • Better working conditions. The only heat present in the air is that of the parts themselves. The working conditions are much more pleasant than with a fuel furnace.

2023年6月19日星期一

Induction Hot Forming Steel Pipe

Induction Hot Forming Steel Pipe

Objective : To heat a magnetic steel pipe to the targeted temperature to enable pipe induction bending; the objective is to create u-bends in pipes for boiler systems Material:  Steel pipes (2.5”/64 mm OD bent steel pipe) Temperature:  2010 °F (1099 °C) Frequency:  8.8 kHz Equipment :  DW-MF-250 kW, 5-15 kHz induction heating power supply with a remote workhead containing eight 6.63 μF capacitors for a total of 53 μF. - A single position six-turn channel induction heating coil designed and developed for this application Process:  The steel pipe was placed inside the induction coil, and it heated to temperature within 120 seconds with an DW-MF- 250kW/10 kHz induction heating system. Results/Benefits: Speed: A large steel pipe heated to the targeted temperature quickly - Repeatability: Induction is highly repeatable and easy-tointegrate into manufacturing processes - Precise heating: Induction is able to target the portion of the tube that requires bending while not heating the remainder of the tube - Energy efficiency: Induction offers fast, flameless, instant on/instant off heating https://dw-inductionheater.com/induction-hot-forming-steel-pipe.html?feed_id=214411&_unique_id=649025feefe81

2023年6月11日星期日

Induction forging and induction hot forming

Induction forging machine Induction forging and induction hot forming refer to the use of an induction heating machine to pre-heat metals prior to deformation using a press or hammer. Typically metals are heated to between 1,100 and 1,200 °C (2,010 and 2,190 °F) to increase their malleability and aid flow in the forging die. Metal induction forging and induction hot forming are excellent induction heating applications. Industrial forging and hot forming processes involve bending or shaping a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Blocks of non-ferrous materials can also be used. Induction heating machines or conventional furnaces are used for the initial heating process. Billets can be transported through the inductor via a pneumatic or hydraulic pusher; pinch roller drive; tractor drive; or walking beam. Non-contact pyrometers are used to measure the billet temperature. Other machines such as mechanical impact presses, bending machines, and hydraulic extrusion presses are used to bend or shape the metal. The approximate hot forming temperatures of the most commonly used industrial materials are: • Steel 1200º C • Brass 750º C • Aluminium 550º C

Total Forming Applications

Induction heating machines are commonly used to heat steel billets, bars, brass blocks, and titanium blocks to the proper temperature for forging and hot forming.

Partial Forming Applications

Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts, and bar ends for partial forming and forging processes.Induction hot forming machine

The Induction Heating Advantage

When compared to conventional furnaces, induction heating machines for forging offer significant process and quality advantages:
  • Much shorter heating times, minimizing scaling and oxidation
  • Easy and accurate temperature temperature control. Parts at temperatures outside specifications can be detected and removed
  • No time lost waiting for the furnace to ramp up to the required temperature
  • Automated induction heating machines require minimal manual labor
  • Heat can be directed to one specific point, which is highly important for parts with only one forming area.
  • Greater thermal efficiency - heat is generated in the part itself and does not need to be heated in a large chamber.
  • Better working conditions. The only heat present in the air is that of the parts themselves. The working conditions are much more pleasant than with a fuel furnace.
2023年6月4日星期日

steel plate-shovels hot forming with induction preheating

Steel plate-shovels hot forming with induction preheating system

What is induction pre-heating? Induction preheating is a process where materials or workpieces are heated by induction prior to further processing. The reasons for pre-heating vary. In the cable and wire industry, cable cores are pre-heated before insulation extrusion. Steels strips are pre-heated prior to pickling and zinc coating. Induction pre-heating also softens metals before bending, and prepares tubes and pipes for welding. Mobile pre-heating solutions facilitate onsite repairs of bearing assemblies. The induction preheating process is an efficient means of preheating steel plate-shovels for hot forming. This involves bending or shaping a metal billet after being heated to a temperature at which there is less resistance to forming. Induction Heating Objective: A steel shovel manufacturer is looking for an induction heating solution to replace a gas furnace and achieve temperature uniformity, repeatability, and fast heat cycles. Induction Heating Equipment: High Frequency Induction Heater DW-HF-45KW is the recommended induction heating equipment for this induction preheating application. With this induction heating generator, the customer heats the steel shovel molds sustainably and achieves faster heat cycles, especially for the bigger samples. Induction Heating Process: This application aims to preheat 4 steel plate sheets to 1742 F/950 C before posting them in a press to form them as shovels. The goal is for the shovel to reach the desired temperature in less than 5 seconds. Benefits: Implementing induction heating has significant advantages:
  • Greater thermal efficiency, resulting in substantial decrease in energy consumption.
  • Shorter heating times
  • Improved uniformity
  • Improved working conditions
https://dw-inductionheater.com/steel-plate-shovels-hot-forming-with-induction-preheating.html?feed_id=210436&_unique_id=647cda352040f

2023年5月29日星期一

Induction Hot Forming Steel Pipe

Induction Hot Forming Steel Pipe

Objective : To heat a magnetic steel pipe to the targeted temperature to enable pipe induction bending; the objective is to create u-bends in pipes for boiler systems Material:  Steel pipes (2.5”/64 mm OD bent steel pipe) Temperature:  2010 °F (1099 °C) Frequency:  8.8 kHz Equipment :  DW-MF-250 kW, 5-15 kHz induction heating power supply with a remote workhead containing eight 6.63 μF capacitors for a total of 53 μF. - A single position six-turn channel induction heating coil designed and developed for this application Process:  The steel pipe was placed inside the induction coil, and it heated to temperature within 120 seconds with an DW-MF- 250kW/10 kHz induction heating system. Results/Benefits: Speed: A large steel pipe heated to the targeted temperature quickly - Repeatability: Induction is highly repeatable and easy-tointegrate into manufacturing processes - Precise heating: Induction is able to target the portion of the tube that requires bending while not heating the remainder of the tube - Energy efficiency: Induction offers fast, flameless, instant on/instant off heating

2023年5月28日星期日

steel plate-shovels hot forming with induction preheating

Steel plate-shovels hot forming with induction preheating system

What is induction pre-heating? Induction preheating is a process where materials or workpieces are heated by induction prior to further processing. The reasons for pre-heating vary. In the cable and wire industry, cable cores are pre-heated before insulation extrusion. Steels strips are pre-heated prior to pickling and zinc coating. Induction pre-heating also softens metals before bending, and prepares tubes and pipes for welding. Mobile pre-heating solutions facilitate onsite repairs of bearing assemblies. The induction preheating process is an efficient means of preheating steel plate-shovels for hot forming. This involves bending or shaping a metal billet after being heated to a temperature at which there is less resistance to forming. Induction Heating Objective: A steel shovel manufacturer is looking for an induction heating solution to replace a gas furnace and achieve temperature uniformity, repeatability, and fast heat cycles. Induction Heating Equipment: High Frequency Induction Heater DW-HF-45KW is the recommended induction heating equipment for this induction preheating application. With this induction heating generator, the customer heats the steel shovel molds sustainably and achieves faster heat cycles, especially for the bigger samples. Induction Heating Process: This application aims to preheat 4 steel plate sheets to 1742 F/950 C before posting them in a press to form them as shovels. The goal is for the shovel to reach the desired temperature in less than 5 seconds. Benefits: Implementing induction heating has significant advantages:
  • Greater thermal efficiency, resulting in substantial decrease in energy consumption.
  • Shorter heating times
  • Improved uniformity
  • Improved working conditions
https://dw-inductionheater.com/steel-plate-shovels-hot-forming-with-induction-preheating.html?feed_id=208636&_unique_id=6473d58721dc8

2023年4月24日星期一

Induction forging and induction hot forming

Induction forging machine Induction forging and induction hot forming refer to the use of an induction heating machine to pre-heat metals prior to deformation using a press or hammer. Typically metals are heated to between 1,100 and 1,200 °C (2,010 and 2,190 °F) to increase their malleability and aid flow in the forging die. Metal induction forging and induction hot forming are excellent induction heating applications. Industrial forging and hot forming processes involve bending or shaping a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Blocks of non-ferrous materials can also be used. Induction heating machines or conventional furnaces are used for the initial heating process. Billets can be transported through the inductor via a pneumatic or hydraulic pusher; pinch roller drive; tractor drive; or walking beam. Non-contact pyrometers are used to measure the billet temperature. Other machines such as mechanical impact presses, bending machines, and hydraulic extrusion presses are used to bend or shape the metal. The approximate hot forming temperatures of the most commonly used industrial materials are: • Steel 1200º C • Brass 750º C • Aluminium 550º C

Total Forming Applications

Induction heating machines are commonly used to heat steel billets, bars, brass blocks, and titanium blocks to the proper temperature for forging and hot forming.

Partial Forming Applications

Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts, and bar ends for partial forming and forging processes.Induction hot forming machine

The Induction Heating Advantage

When compared to conventional furnaces, induction heating machines for forging offer significant process and quality advantages:
  • Much shorter heating times, minimizing scaling and oxidation
  • Easy and accurate temperature temperature control. Parts at temperatures outside specifications can be detected and removed
  • No time lost waiting for the furnace to ramp up to the required temperature
  • Automated induction heating machines require minimal manual labor
  • Heat can be directed to one specific point, which is highly important for parts with only one forming area.
  • Greater thermal efficiency - heat is generated in the part itself and does not need to be heated in a large chamber.
  • Better working conditions. The only heat present in the air is that of the parts themselves. The working conditions are much more pleasant than with a fuel furnace.
2023年4月13日星期四

Induction Hot Forming Steel Pipe

Induction Hot Forming Steel Pipe

Objective : To heat a magnetic steel pipe to the targeted temperature to enable pipe induction bending; the objective is to create u-bends in pipes for boiler systems Material:  Steel pipes (2.5”/64 mm OD bent steel pipe) Temperature:  2010 °F (1099 °C) Frequency:  8.8 kHz Equipment :  DW-MF-250 kW, 5-15 kHz induction heating power supply with a remote workhead containing eight 6.63 μF capacitors for a total of 53 μF. - A single position six-turn channel induction heating coil designed and developed for this application Process:  The steel pipe was placed inside the induction coil, and it heated to temperature within 120 seconds with an DW-MF- 250kW/10 kHz induction heating system. Results/Benefits: Speed: A large steel pipe heated to the targeted temperature quickly - Repeatability: Induction is highly repeatable and easy-tointegrate into manufacturing processes - Precise heating: Induction is able to target the portion of the tube that requires bending while not heating the remainder of the tube - Energy efficiency: Induction offers fast, flameless, instant on/instant off heating

2023年4月6日星期四

steel plate-shovels hot forming with induction preheating

Steel plate-shovels hot forming with induction preheating system

What is induction pre-heating? Induction preheating is a process where materials or workpieces are heated by induction prior to further processing. The reasons for pre-heating vary. In the cable and wire industry, cable cores are pre-heated before insulation extrusion. Steels strips are pre-heated prior to pickling and zinc coating. Induction pre-heating also softens metals before bending, and prepares tubes and pipes for welding. Mobile pre-heating solutions facilitate onsite repairs of bearing assemblies. The induction preheating process is an efficient means of preheating steel plate-shovels for hot forming. This involves bending or shaping a metal billet after being heated to a temperature at which there is less resistance to forming. Induction Heating Objective: A steel shovel manufacturer is looking for an induction heating solution to replace a gas furnace and achieve temperature uniformity, repeatability, and fast heat cycles. Induction Heating Equipment: High Frequency Induction Heater DW-HF-45KW is the recommended induction heating equipment for this induction preheating application. With this induction heating generator, the customer heats the steel shovel molds sustainably and achieves faster heat cycles, especially for the bigger samples. Induction Heating Process: This application aims to preheat 4 steel plate sheets to 1742 F/950 C before posting them in a press to form them as shovels. The goal is for the shovel to reach the desired temperature in less than 5 seconds. Benefits: Implementing induction heating has significant advantages:
  • Greater thermal efficiency, resulting in substantial decrease in energy consumption.
  • Shorter heating times
  • Improved uniformity
  • Improved working conditions

2023年3月10日星期五

Induction forging and induction hot forming

Induction forging machine Induction forging and induction hot forming refer to the use of an induction heating machine to pre-heat metals prior to deformation using a press or hammer. Typically metals are heated to between 1,100 and 1,200 °C (2,010 and 2,190 °F) to increase their malleability and aid flow in the forging die. Metal induction forging and induction hot forming are excellent induction heating applications. Industrial forging and hot forming processes involve bending or shaping a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Blocks of non-ferrous materials can also be used. Induction heating machines or conventional furnaces are used for the initial heating process. Billets can be transported through the inductor via a pneumatic or hydraulic pusher; pinch roller drive; tractor drive; or walking beam. Non-contact pyrometers are used to measure the billet temperature. Other machines such as mechanical impact presses, bending machines, and hydraulic extrusion presses are used to bend or shape the metal. The approximate hot forming temperatures of the most commonly used industrial materials are: • Steel 1200º C • Brass 750º C • Aluminium 550º C

Total Forming Applications

Induction heating machines are commonly used to heat steel billets, bars, brass blocks, and titanium blocks to the proper temperature for forging and hot forming.

Partial Forming Applications

Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts, and bar ends for partial forming and forging processes.Induction hot forming machine

The Induction Heating Advantage

When compared to conventional furnaces, induction heating machines for forging offer significant process and quality advantages:
  • Much shorter heating times, minimizing scaling and oxidation
  • Easy and accurate temperature temperature control. Parts at temperatures outside specifications can be detected and removed
  • No time lost waiting for the furnace to ramp up to the required temperature
  • Automated induction heating machines require minimal manual labor
  • Heat can be directed to one specific point, which is highly important for parts with only one forming area.
  • Greater thermal efficiency - heat is generated in the part itself and does not need to be heated in a large chamber.
  • Better working conditions. The only heat present in the air is that of the parts themselves. The working conditions are much more pleasant than with a fuel furnace.
2023年3月2日星期四

Induction forging and induction hot forming

Induction forging machine
Induction forging and induction hot forming 
refer to the use of an induction heating machine to pre-heat metals prior to deformation using a press or hammer. Typically metals are heated to between 1,100 and 1,200 °C (2,010 and 2,190 °F) to increase their malleability and aid flow in the forging die.

Metal induction forging and induction hot forming are excellent induction heating applications. Industrial forging and hot forming processes involve bending or shaping a metal billet or bloom after it has been heated to a temperature at which its resistance to deformation is weak. Blocks of non-ferrous materials can also be used.

Induction heating machines or conventional furnaces are used for the initial heating process. Billets can be transported through the inductor via a pneumatic or hydraulic pusher; pinch roller drive; tractor drive; or walking beam. Non-contact pyrometers are used to measure the billet temperature.

Other machines such as mechanical impact presses, bending machines, and hydraulic extrusion presses are used to bend or shape the metal.

The approximate hot forming temperatures of the most commonly used industrial materials are:

• Steel 1200º C • Brass 750º C • Aluminium 550º C

Total Forming Applications


Induction heating machines are commonly used to heat steel billets, bars, brass blocks, and titanium blocks to the proper temperature for forging and hot forming.

Partial Forming Applications


Induction heating is also used to heat parts such as pipe ends, axle ends, automotive parts, and bar ends for partial forming and forging processes.Induction hot forming machine

The Induction Heating Advantage


When compared to conventional furnaces, induction heating machines for forging offer significant process and quality advantages:

  • Much shorter heating times, minimizing scaling and oxidation

  • Easy and accurate temperature temperature control. Parts at temperatures outside specifications can be detected and removed

  • No time lost waiting for the furnace to ramp up to the required temperature

  • Automated induction heating machines require minimal manual labor

  • Heat can be directed to one specific point, which is highly important for parts with only one forming area.

  • Greater thermal efficiency - heat is generated in the part itself and does not need to be heated in a large chamber.

  • Better working conditions. The only heat present in the air is that of the parts themselves. The working conditions are much more pleasant than with a fuel furnace.

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.