显示标签为“mediumfrequencyheating”的博文。显示所有博文

2024年2月15日星期四

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

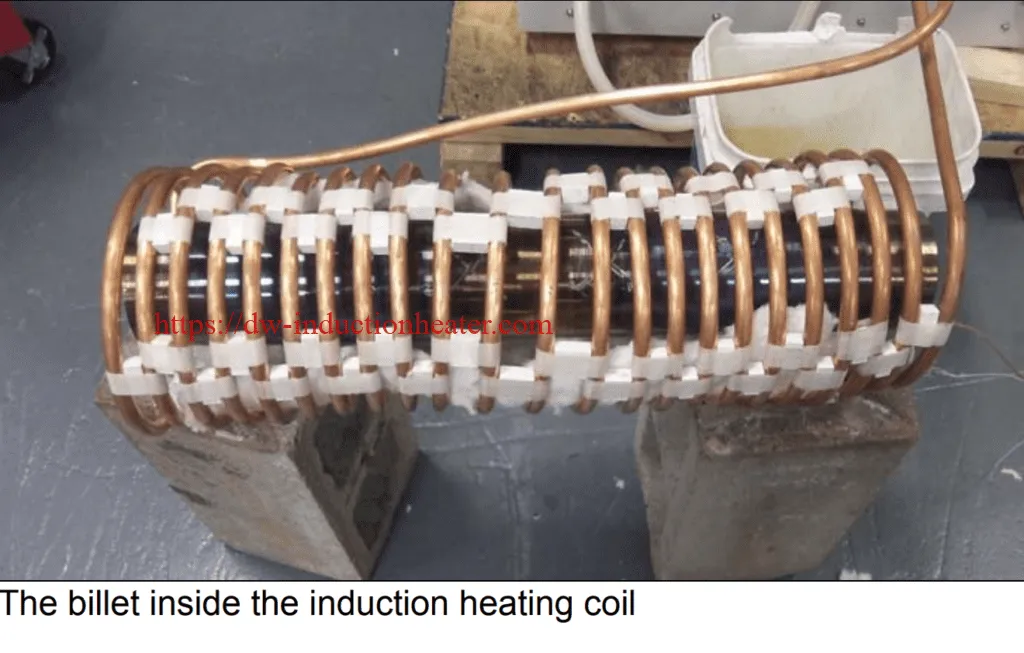
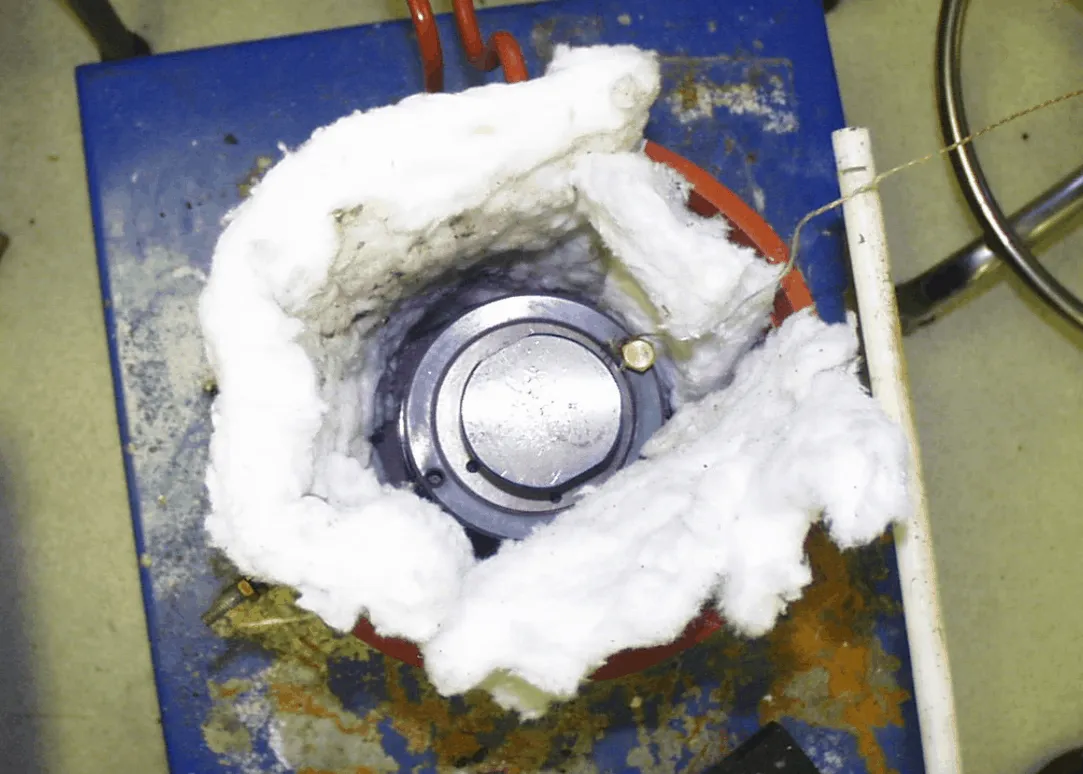
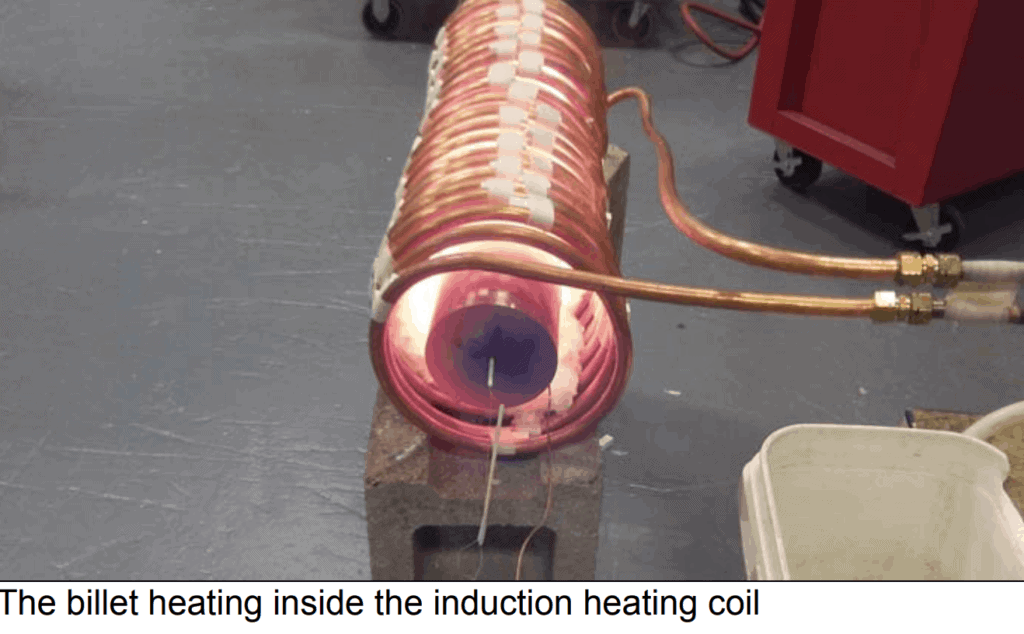
Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time https://dw-inductionheater.com/induction-preheating-titanium-billet-for-rolling.html?feed_id=234103&_unique_id=65ce0d6f14711

2023年7月13日星期四

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年7月1日星期六

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年6月24日星期六

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time https://dw-inductionheater.com/induction-preheating-titanium-billet-for-rolling.html?feed_id=215761&_unique_id=6496949b650ff

2023年5月5日星期五

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年2月23日星期四

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年1月14日星期六

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年1月13日星期五

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年12月6日星期二

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年11月7日星期一

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年9月25日星期日

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年9月9日星期五

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年1月19日星期三

MFS medium frequency heating systems

medium frequency induction heating systems and heating power supplies

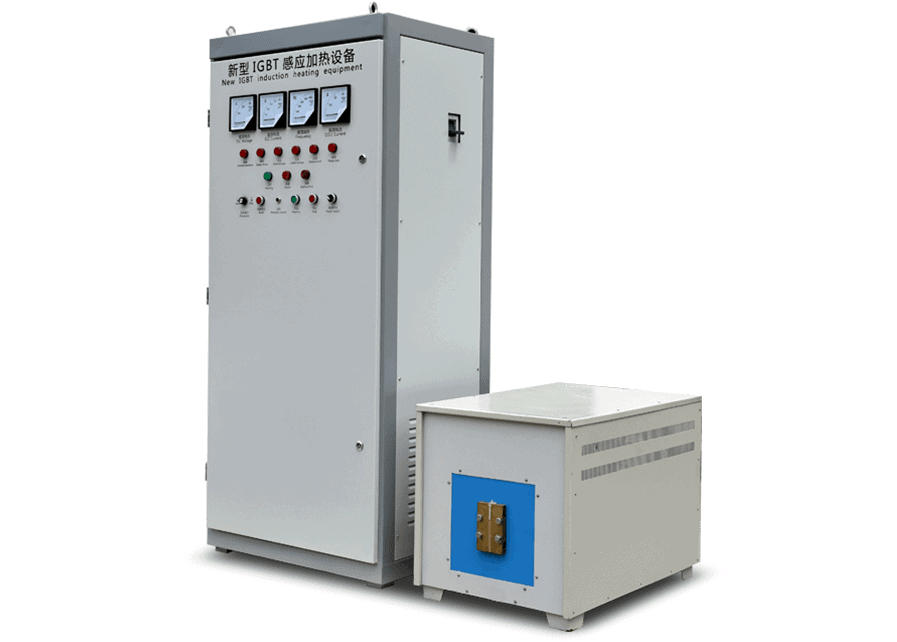
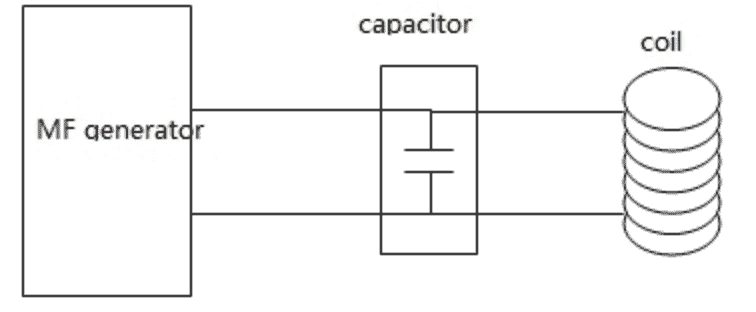
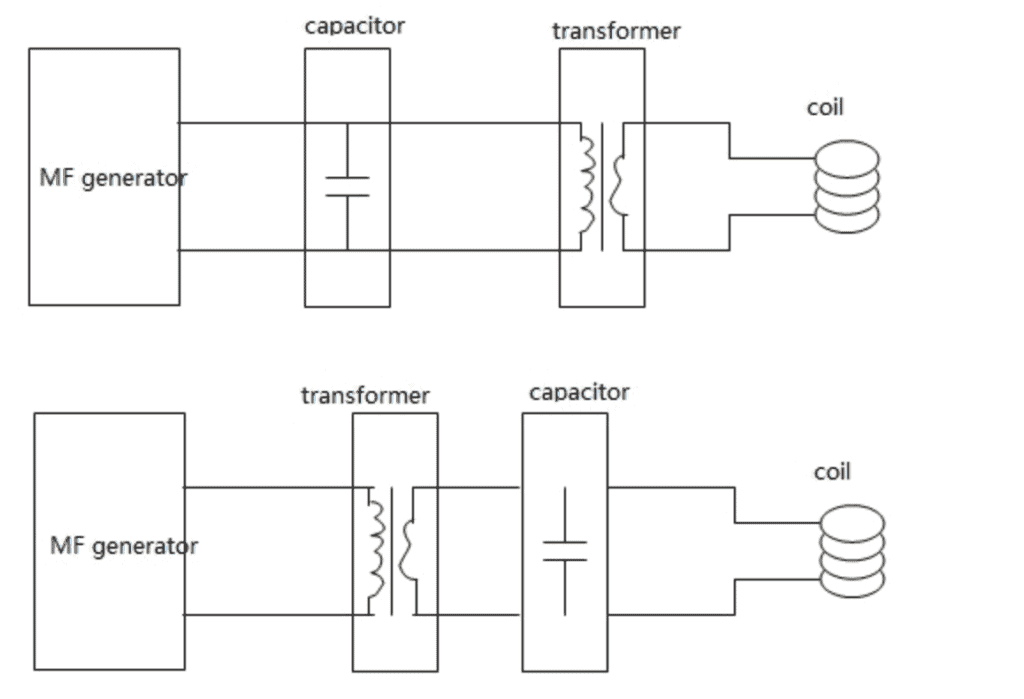
Medium frequency induction heating systems (MFS series) are acetized by frequency range 500Hz~10KHz and power100~1500KW,they are mainly used for penetrated  heating, such as rod heating for shaping, melting, fitting and preheat for welding. Due to its wide frequency range, satisfied heating effect is easily achieved by design to considerate all factors such as penetrating desire, heating efficiency, working noise, magnetic stirring force and so on. In MFS medium frequency machines,parallel oscillating structure is used . IGBT module power components and our fourth generation inverting control technologies are applied to ensure high quality and reliability. Fully protection is adopted such as over current protection, water fail protection, over temperature protection, over voltage protection, short circuit protection and phase fail protection.  When working, output current, output voltage , oscillating frequency and output power are all displayed on the operating panel to help in the design of the coil and adjust of the machine. According to different usage, two main structures are used: (1) structure 1 :MF generator + capacitor + coil This structure is adopted often in many uses, such as rod induction heating machine and melting machine.  This structure is simple, low lost and high efficient in heating. In this structure, usually  3 to 15 meters copper tube is needed to make the coil;  voltage of the coil  is high to 550V, and not isolated to the power supply system, so coil must be insulated properly to ensure the safety of operators. (2)structure 2:MF generator + cap + transformer + coil This structure is also used often, such as melting in vacuum, medium frequency induction hardening machine and so on.   Through the design of transformer ratio,  output current and voltage can be controlled to satisfy different heating desire. In this structure,  coil is safe for operators,  coil tube can exposed directly with out insulation.  Coil is easy to make with only a few turns. Of course, transformer will increase the cost and consumption the machine. Specifications
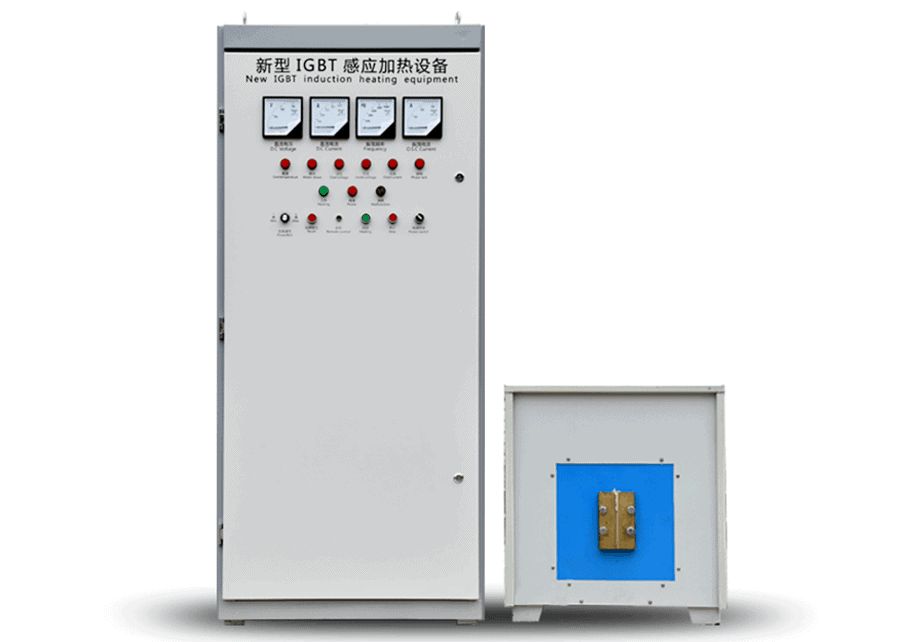
Models Rated output power Frequency rage Input current Input voltage Duty cycle Water flow weight Dimension
MFS-100 100KW 0.5-10KHz 160A 3phase 380V 50Hz 100% 10-20m³/h 175KG 800x650x1800mm
MFS-160 160KW 0.5-10KHz 250A 10-20m³/h 180KG 800x 650 x 1800mm
MFS-200 200KW 0.5-10KHz 310A 10-20m³/h 180KG 800x 650 x 1800mm
MFS-250 250KW 0.5-10KHz 380A 10-20m³/h 192KG 800x 650 x 1800mm
MFS-300 300KW 0.5-8KHz 460A 25-35m³/h 198KG 800x 650 x 1800mm
MFS-400 400KW 0.5-8KHz 610A 25-35m³/h 225KG 800x 650 x 1800mm
MFS-500 500KW 0.5-8KHz 760A 25-35m³/h 350KG 1500 x 800 x 2000mm
MFS-600 600KW 0.5-8KHz 920A 25-35m³/h 360KG 1500 x 800 x 2000mm
MFS-750 750KW 0.5-6KHz 1150A 50-60m³/h 380KG 1500 x 800 x 2000mm
MFS-800 800KW 0.5-6KHz 1300A 50-60m³/h 390KG 1500 x 800 x 2000mm
Main characteristics
  • Voltage feedback design and adopt IGBT based LC series resonance circuit .
  • IGBT inversion technology ,high energy conversion over 97.5% .
  • Energy saving 30%up compared with SCR technology. In series resonance circuit, induction coil with high voltage and low current, so energy loss is very low. Soft switch technology applied then switch loss is very low.
  • It can be started up 100% under any condition.
  • 100% duty cycle , 24hours continuous working ability at maximum power.
  • Less harmonic current and high power factor. Power factor always remaining 0.95 above during machine running.
  • The frequency tracking automatically technology enables power factor to remaining high level throughout heating process.
  • Good reliability, IGBT is a self turn-off transistor that ensures inversion with success and takes protection instantly; IGBT used from infineon company, world-renowned manufacturer.
  • Easy to operate and maintain, IGBT MF induction generator is easy to prevent and maintain due to its simple circuit structure. It has perfect protection.
Options
  • A range of heating furnace, customized different type of induction heating furnace according customer’s requires.
  • Infarared sensor.
  • Temperature controller.
  • CNC or PLC controlled mechanical fixture for hardening application.
  • Water cooling system.
  • Pneumatic rod feeder.
  • Customized whole automatic heating system.
Main applications
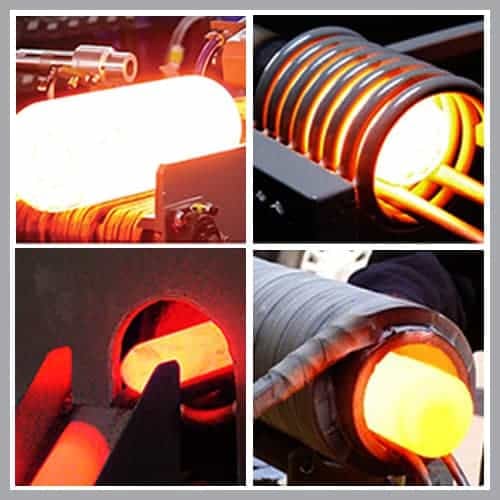
  • Hot Forging/forming for large workpiece.
  • Surface hardening for large part.
  • Preheating of pipe bending.
  • Annealing of pipe welding.
  • Melting of copper aluminum and so on.
  • Shrink-fit of sleeve of roller.

2022年1月13日星期四

Steel Die Induction Heating

Steel die induction heating in a thermal process of an enclosed powder

Objective : A steel die is heated with induction in a thermal process of an enclosed powder Material: Steel die with a compressed powder solid inside Temperature: 400 ºC (750 ºF) Frequency: 22 kHz Induction Heating Equipment: DW-MF-70kW/30kHz induction heating system, equipped with a remote workhead containing one 53μF capacitor - An induction heating coil designed and developed specifically for this application. Process Induction Heating is evaluated to replace an oven/batch process. Advantages include reduced heating/cooling ramp times and floor space requirements. A nine-turn helical induction heating coil is used to heat the steel die while temperature of the die is monitored with a thermocouple. Die heating soak time is one hour. induction heating principle Results/Benefits Induction heating provides: - heat generated within the part, saving energy and time - easy integration with a press - anticipated process energy savings - greatly reduced footprint compared with oven, batch, carts - precise controllable heat - rapid ramp-up and cool-down times - automatic ramp and soak capability induction heating steel dies

2021年12月12日星期日

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time
关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.