显示标签为“heatingtitaniumbillettorolling”的博文。显示所有博文

2024年2月15日星期四

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

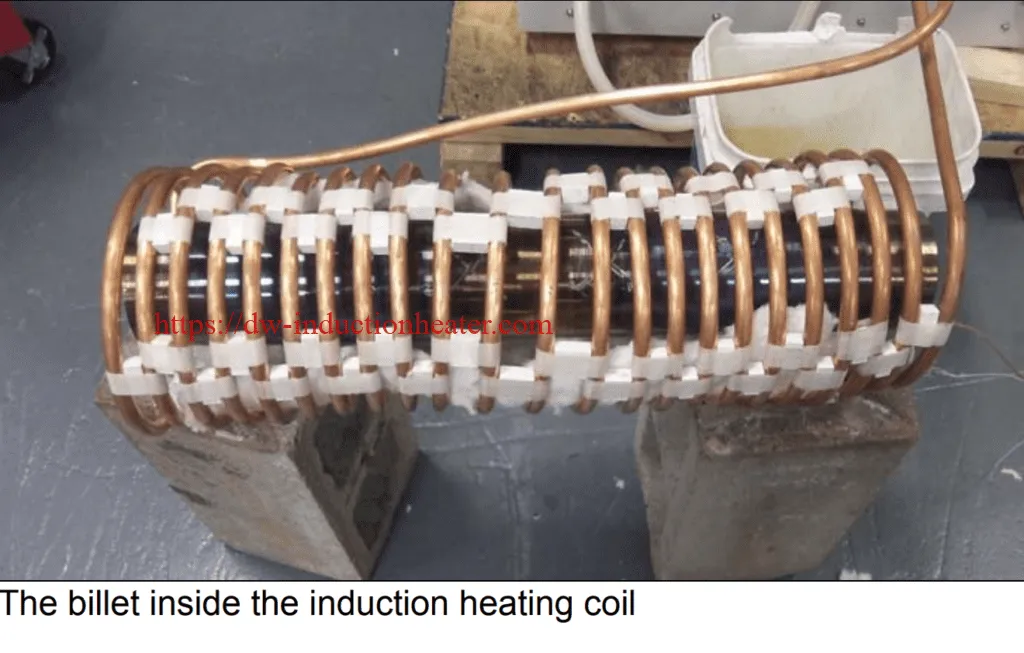
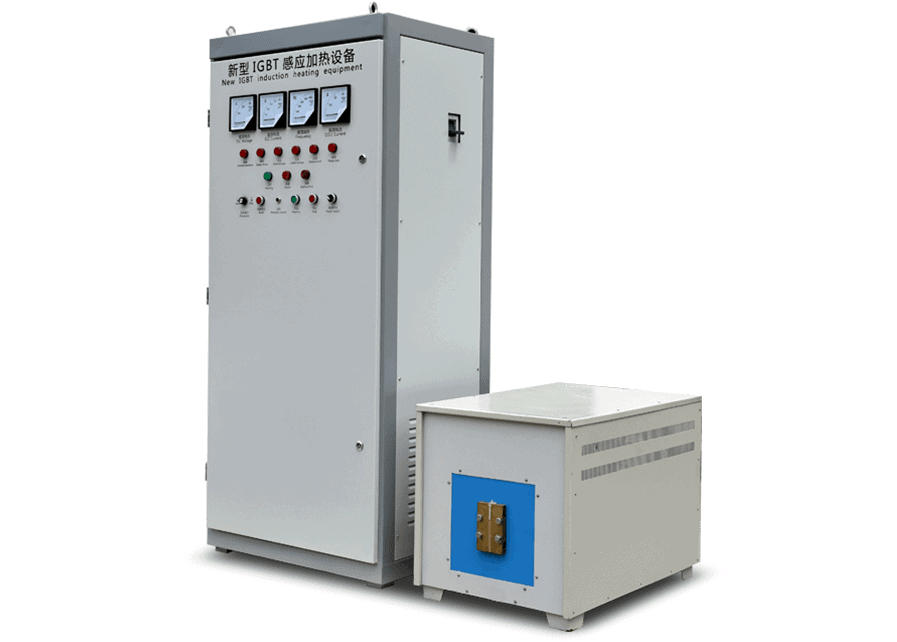
Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time https://dw-inductionheater.com/induction-preheating-titanium-billet-for-rolling.html?feed_id=234103&_unique_id=65ce0d6f14711
2023年7月13日星期四

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

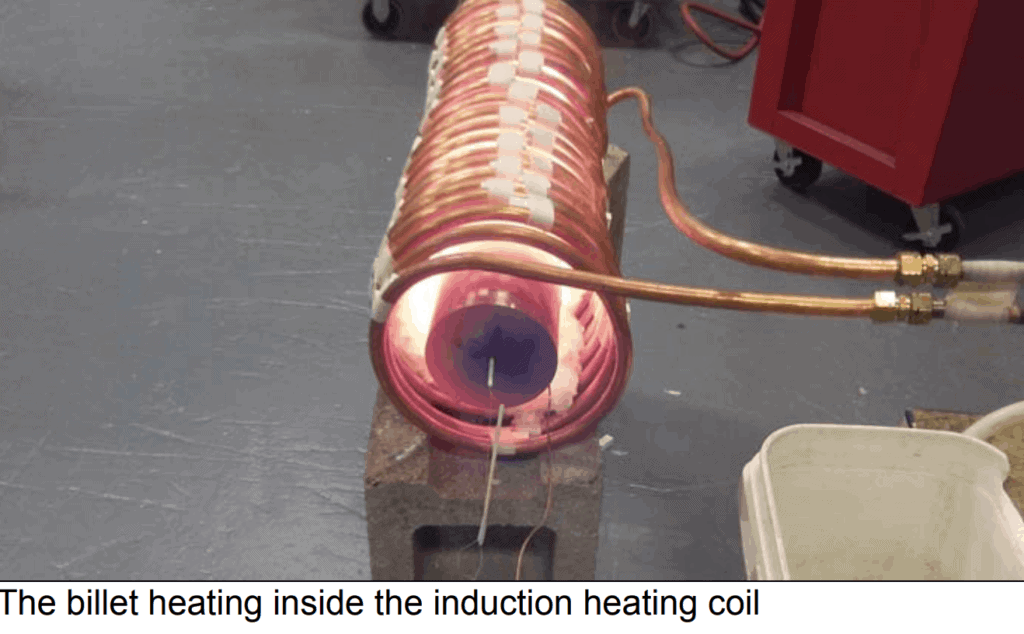
Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time
2023年7月1日星期六

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年6月24日星期六

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time https://dw-inductionheater.com/induction-preheating-titanium-billet-for-rolling.html?feed_id=215761&_unique_id=6496949b650ff

2023年5月5日星期五

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年2月23日星期四

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年1月14日星期六

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2023年1月13日星期五

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年12月6日星期二

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年11月7日星期一

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年9月25日星期日

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2022年9月9日星期五

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2021年12月12日星期日

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

2021年11月2日星期二

induction preheating titanium billet for rolling

induction preheating titanium billet for rolling with MF induction heating system

Objective:  To preheat a titanium billet to 1800 ºF prior to entering a rolling mill Material : Customer supplied 4” (102mm) diameter/24” (610mm) long titanium billet Temperature: 1800 ºF (1000 ºC) Frequency : 2.7 kHz Induction Heating Equipment:medium frequency MFS-200kW 1.5-4.5 kHz induction heating system equipped with a remote work head containing six 40 μF capacitors -- A multi-turn helical induction heating coil designed and developed specifically for this application Induction Heating Process:  The titanium billet was placed inside the multi-turn induction heating coil. The part was heated for five minutes, which was necessary to reduce the temperature difference between the center and outside of the billet. Due to the considerable diameter of the part, a high power, low frequency induction heating power supply was used. Considerable effort went into designing the coil to ensure the most uniform heating possible while still minimizing heating time. Results/Benefits  -Speed: Induction heated the large billet quickly, and will also heat the client’s longer 15 foot billets - Uniform heating: Induction’s rapid, even heating enabled a uniform temperature throughout the billet - Repeatability: This process will provide consistent results, so the client can design their process around the fiveminute heating time

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.