显示标签为“inductionpreheatingwelding”的博文。显示所有博文

2024年6月3日星期一

Induction Preheating Welding Steel Pipe

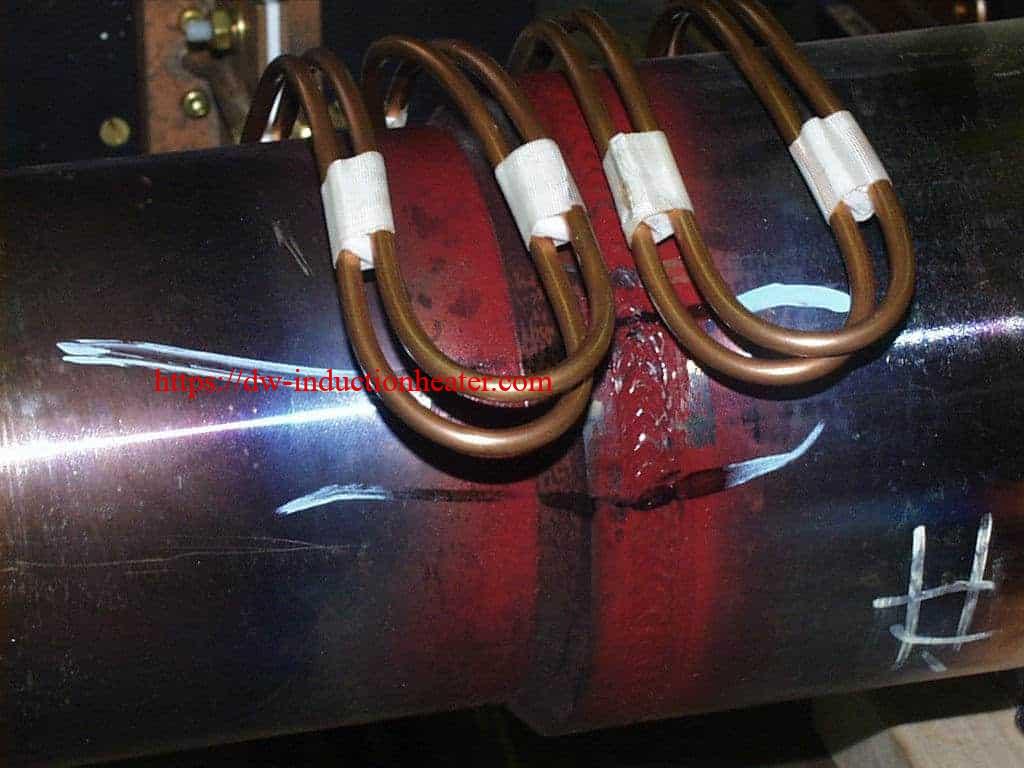
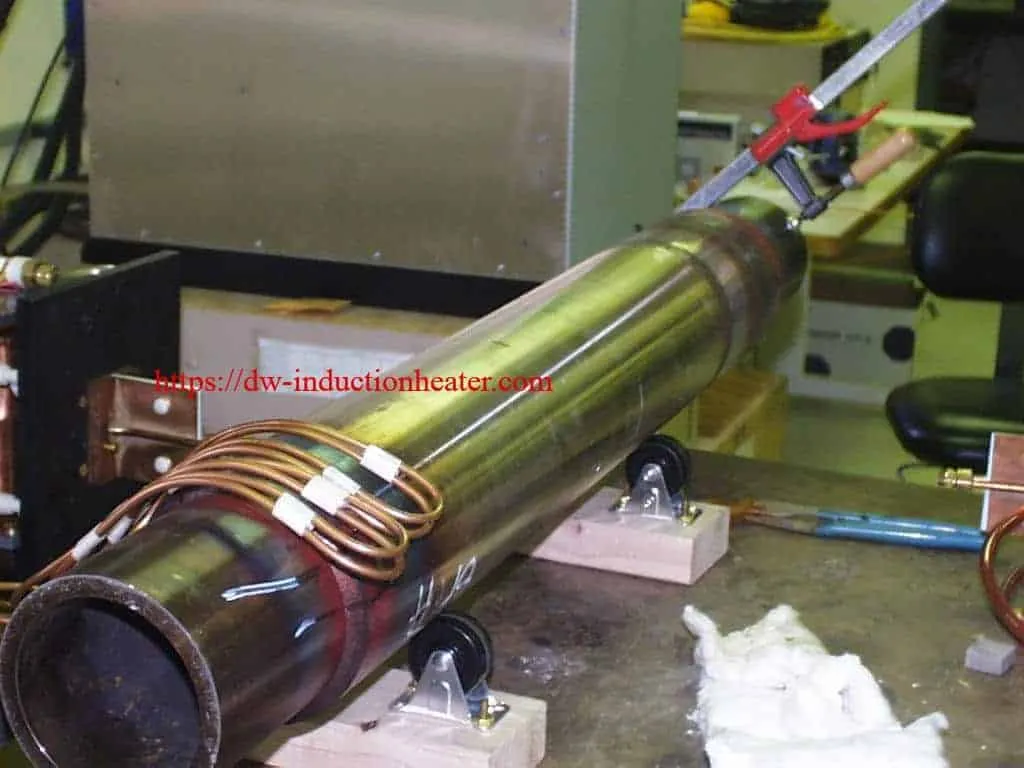
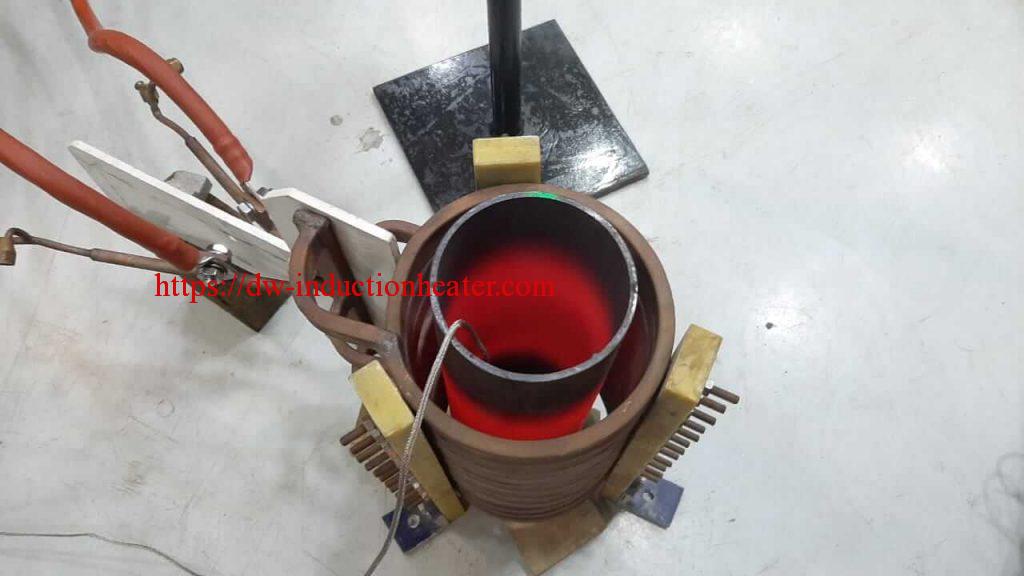
Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding https://dw-inductionheater.com/induction-preheating-welding-steel-pipe.html?feed_id=248453&_unique_id=665d970cc2908

2023年10月11日星期三

Induction Preheating Welding Steel Pipe

Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding https://dw-inductionheater.com/induction-preheating-welding-steel-pipe.html?feed_id=228846&_unique_id=6526f3569c2da

2023年3月24日星期五

Induction Preheating Welding Steel Pipe

Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding

2023年2月26日星期日

Induction Preheating Welding Steel Pipe

Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding

2023年2月1日星期三

Induction Preheating Welding Steel Pipe

Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding

2022年9月1日星期四

Induction Preheating Welding Steel Pipe

Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding

2022年8月16日星期二

Induction Preheating Welding Steel Pipe

Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding

2022年3月29日星期二

Induction Preheating Welding Steel Pipe

Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding

2022年3月27日星期日

Induction Preheating Welding Steel Pipe

Induction Preheating Welding Steel Pipe With High Frequency Heating System Objective To preheat a steel pipe to 500ºF (260ºC) before welding. Material Steel shaft assembly 5” to 8” OD (127-203.2mm) with a 2” (50.8mm) heat zone. Temperature 500ºF (260ºC), if higher temperatures are required, heat time can be increased. Frequency 60 kHz Equipment • DW-HF-60kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8 μF. • An induction heating coil designed and developed specifically for this application. Process A multi-turn two position channel “C” coil, adjustable on a busbar is used to heat the desired heat zone. The coil is adjustable to fit various diameter pipes. The shaft is rotated in a fixture and heated for 3 minutes to achieve a temperature of 500ºF (260ºC). Results/Benefits Induction heating provides: • Preheating prevents shock to shaft which eliminates cracking in the welding phase. • Hands-free heating that involves no operator skill for manufacturing. • Even distribution of heating between the shank and the  sleeve. induction preheating welding steel pipe             induction preheating steel pipe before welding

2021年12月25日星期六

induction preheating steel tube for welding

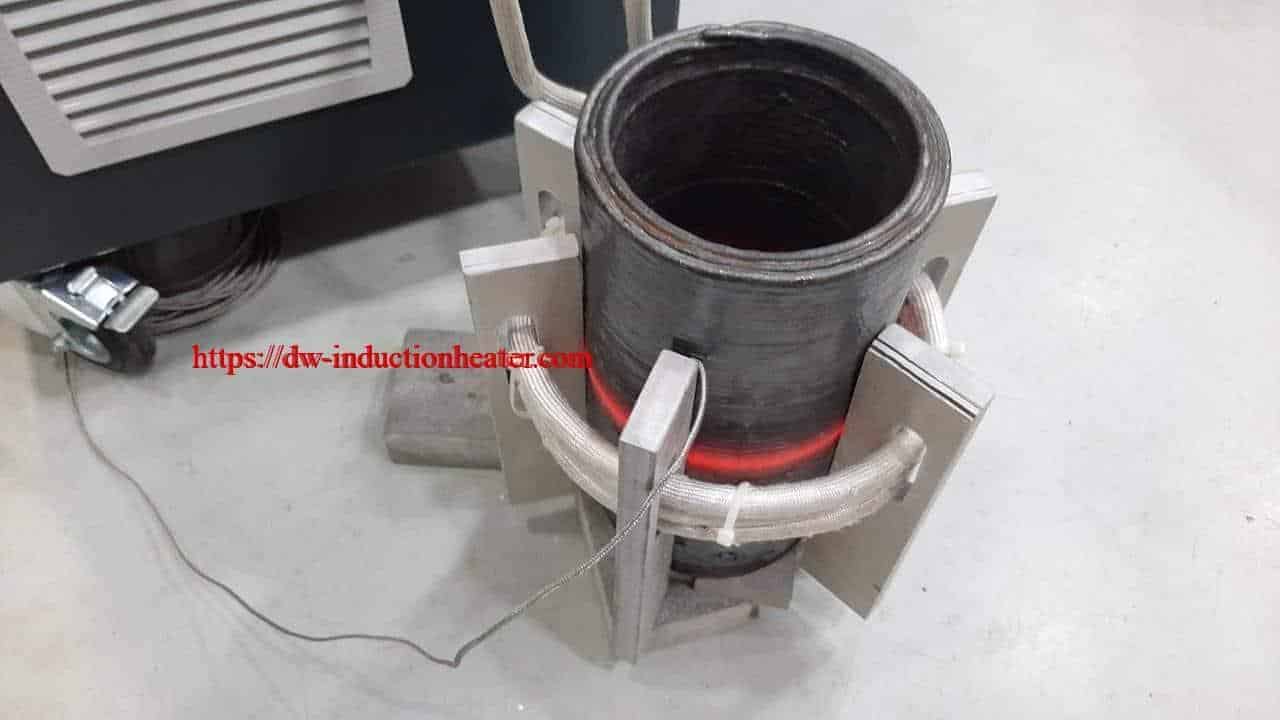
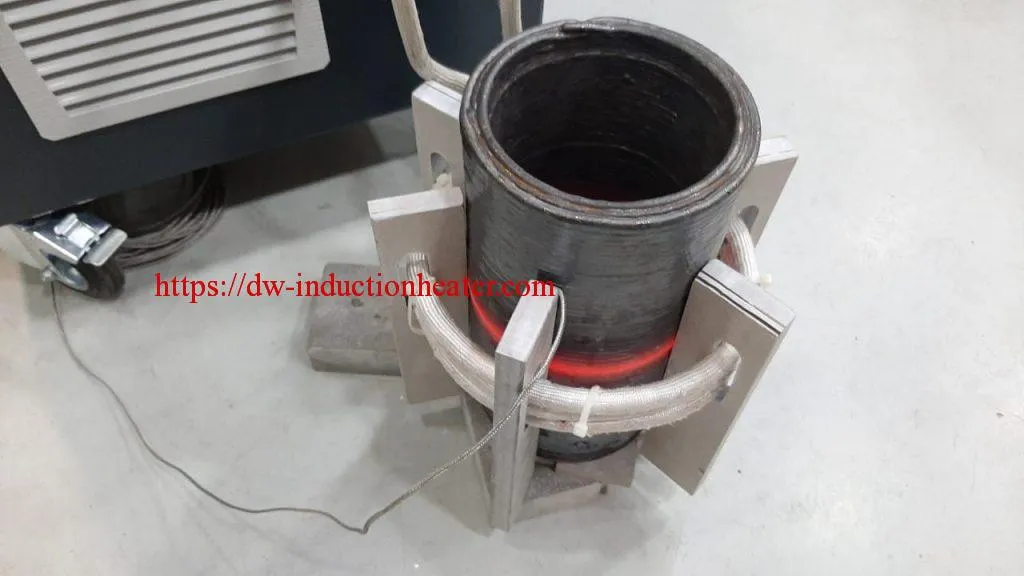
This induction heating application shows the preheating of steel pipe before welding with MF-25kw (25kW) air-cooled power supply and air-cooled coil.  Inductively preheating of the pipe section to be welded ensures faster welding time and a better quality of the welding joint. Industry: Manufacturing Equipment: MF-25kw air cooled induction heating system Time: 300 secs. Temperature: Required from ambient temperature 600 ° C +/- 10 °C  (1112° F/ +/- 50°F) Materials: Steel pipe Details for butt-welded steel pipe: Total length: 300 mm (11.8 inch) DIA: 152.40 mm (5.9 inch) Thickness: 18.26 mm (0.71 inch) Heating length: 30-45 mm from middle (1.1 – 1.7 inch) Details for butt welded steel plate. Total size: 300 mm (11.8 inch) X 300 mm (11.8 inch) Thickness: 10 mm (0.39 inch) Heating length: 20-30 mm (0.7-1.1 inch) from middle. Fixture details for butt welded steel pipe: Material: Mica. Total Size: 300 mm (11.8 inch) X 60 mm (2.3 inch) Thickness: 20 mm (0.7 inch) Withstands temperature of 900 °C (1652°F) Process: We are using our  MF-25kw air cooled induction heating system which allows to easily move the system and the heating coil to various welding locations, without the need to provide additional water cooling systems or hoses. Induction heating provides consistent heat throughout the process. The preheat temperatures can be easily measured with temeperature monitoring tools. The induction heating method is very efficient because it  minimizes the heat loss that often occurs during other heating methods.  
2021年12月2日星期四

Induction Preheating Welding Automotive Parts

Induction Preheating Welding Automotive Parts With Induction Heating Equipment Objective To pre-heat the seam of a truck axle to over 300°F within 15 seconds for a welding application and maintain temperature within the welding zone for 15 seconds after the power is turned off. Material Steel truck axle; 350° and 400°F temperature indicating paint;350°, 375°and 400°F temperature indicating “crayons” Temperature 350°F Frequency 75 kHz Equipment DW-HF-35kW power supply, remote heat station with four 1.2 μF capacitors and a specially designed pancake induction coil. Process A fixture was constructed to rotate the axle 400° in 15 seconds and the induction coil was placed above the axle. The circumference of the axle (beneath the coil) was painted with 350° and 400°F temperature indicating paint. While the axle was being rotated, RF power was applied for 15 seconds. All of the paint melted, confirming that the axle temperature was above 400°F. The RF power was shut off and the temperature “crayons” were immediately placed against the axle to monitor temperature. The 400°F crayon did not melt; the 375°F crayon melted for 15 seconds; the 350°F crayon melted for 30 seconds. Results The steel axle was heated to over 400°F within 15 seconds and temperatures above 350°F were maintained for 30 seconds after power was turned off, meeting the requirements of the welding application.

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.