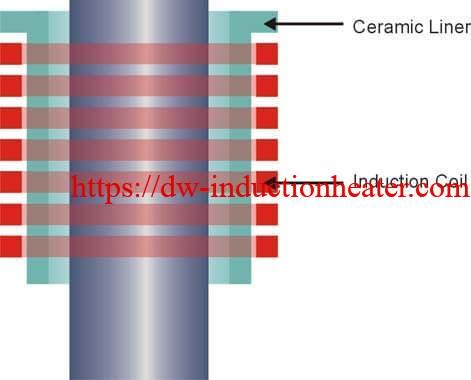
显示标签为“highfrequencyheatinghot”的博文。显示所有博文

2024年5月29日星期三

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate   https://dw-inductionheater.com/induction-hot-plate.html?feed_id=247814&_unique_id=6657e065e3507

2024年5月3日星期五

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner Temperature 1500 ºF (815.5ºC) Frequency 75 kHz Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF • An induction heating coil designed and developed specifically for this application. Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a ceramic liner is used so the rod does not touch the coil. Results/Benefits Induction heating provides: • Low pressure and minimal residual stress • Better grain flow and microstructure • Even distribution of heating • Improved production rates with minimal defects Preheating Hot Rod Heading https://dw-inductionheater.com/induction-preheating-hot-rod-heading.html?feed_id=244236&_unique_id=6635996cba754

2023年10月7日星期六

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate   https://dw-inductionheater.com/induction-hot-plate.html?feed_id=228551&_unique_id=65213cad40313

2023年9月11日星期一

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner Temperature 1500 ºF (815.5ºC) Frequency 75 kHz Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF • An induction heating coil designed and developed specifically for this application. Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a ceramic liner is used so the rod does not touch the coil. Results/Benefits Induction heating provides: • Low pressure and minimal residual stress • Better grain flow and microstructure • Even distribution of heating • Improved production rates with minimal defects Preheating Hot Rod Heading https://dw-inductionheater.com/induction-preheating-hot-rod-heading.html?feed_id=227111&_unique_id=64fef3dacce34

2023年7月8日星期六

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2023年6月16日星期五

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2023年6月7日星期三

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2023年4月30日星期日

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner Temperature 1500 ºF (815.5ºC) Frequency 75 kHz Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF • An induction heating coil designed and developed specifically for this application. Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a ceramic liner is used so the rod does not touch the coil. Results/Benefits Induction heating provides: • Low pressure and minimal residual stress • Better grain flow and microstructure • Even distribution of heating • Improved production rates with minimal defects Preheating Hot Rod Heading

2023年4月27日星期四

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2023年2月26日星期日

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units

Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application
Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner
Temperature 1500 ºF (815.5ºC)
Frequency 75 kHz
Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF
• An induction heating coil designed and developed specifically for this application.
Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds
providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a
ceramic liner is used so the rod does not touch the coil.
Results/Benefits Induction heating provides:
• Low pressure and minimal residual stress
• Better grain flow and microstructure
• Even distribution of heating
• Improved production rates with minimal defects
Preheating Hot Rod Heading

2023年1月3日星期二

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner Temperature 1500 ºF (815.5ºC) Frequency 75 kHz Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF • An induction heating coil designed and developed specifically for this application. Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a ceramic liner is used so the rod does not touch the coil. Results/Benefits Induction heating provides: • Low pressure and minimal residual stress • Better grain flow and microstructure • Even distribution of heating • Improved production rates with minimal defects Preheating Hot Rod Heading

2022年12月20日星期二

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2022年11月29日星期二

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2022年9月25日星期日

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2022年9月20日星期二

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner Temperature 1500 ºF (815.5ºC) Frequency 75 kHz Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF • An induction heating coil designed and developed specifically for this application. Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a ceramic liner is used so the rod does not touch the coil. Results/Benefits Induction heating provides: • Low pressure and minimal residual stress • Better grain flow and microstructure • Even distribution of heating • Improved production rates with minimal defects Preheating Hot Rod Heading

2022年8月13日星期六

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner Temperature 1500 ºF (815.5ºC) Frequency 75 kHz Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF • An induction heating coil designed and developed specifically for this application. Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a ceramic liner is used so the rod does not touch the coil. Results/Benefits Induction heating provides: • Low pressure and minimal residual stress • Better grain flow and microstructure • Even distribution of heating • Improved production rates with minimal defects Preheating Hot Rod Heading

2022年7月31日星期日

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2022年7月26日星期二

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner Temperature 1500 ºF (815.5ºC) Frequency 75 kHz Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF • An induction heating coil designed and developed specifically for this application. Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a ceramic liner is used so the rod does not touch the coil. Results/Benefits Induction heating provides: • Low pressure and minimal residual stress • Better grain flow and microstructure • Even distribution of heating • Improved production rates with minimal defects Preheating Hot Rod Heading

2022年5月11日星期三

Induction Hot Plate

High Frequency Induction Hot Plate with a Tin Coating for Flow-Melting  Objective Heat a carbon steel plate coated with tin to 450 ºF (232 ºC) for flow-melting Material 7.9” (200mm) x 4.7” (120mm) steel plates with a tin layer of 100 to 1000nm thickness, temperature sensing paint, water for quenching Temperature 450 ºF (232 ºC) Frequency 350 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25μF • An induction heating coil designed and developed specifically for this application. Process A nine turn “Dog Bone” style coil is used for the flow-melting process. The tin coated carbon steel plate is placed in the coil for 1.34 seconds to uniformly reflow the tin coating. The plate is then quenched in cool water to retain sufficient free tin at the surface. Results/Benefits Induction heating provides: • Uniform heating • Rapid focused heat high frequency induction heating plate             induction heating steel plate  

2022年4月19日星期二

Induction Preheating Hot Rod Heading

Induction Preheating Hot Rod Heading With IGBT Heating Units Objective Heat a waspaloy rod to 1500ºF (815.5ºC) for hot heading application Material Waspaloy rod 0.5” (12.7mm)OD, 1.5” (38.1mm) length, ceramic liner Temperature 1500 ºF (815.5ºC) Frequency 75 kHz Equipment • DW-HF- 20 kW induction heating system, equipped with a remote workhead containing two 1.32μF capacitors for a total of .66μF • An induction heating coil designed and developed specifically for this application. Process A seven turn helical coil is used to heat the rod. The rod is placed inside the coil and power is applied for two seconds providing enough heat to penetrate the inner core. An optical pyrometer is used for close loop temperature control and a ceramic liner is used so the rod does not touch the coil. Results/Benefits Induction heating provides: • Low pressure and minimal residual stress • Better grain flow and microstructure • Even distribution of heating • Improved production rates with minimal defects Preheating Hot Rod Heading

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.