 https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=267806&_unique_id=67969bdb81a85
2025年1月26日星期日
Induction Brazing Carbide To Steel
Induction Brazing Carbide To Steel
https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=267806&_unique_id=67969bdb81a85
https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=267806&_unique_id=67969bdb81a85

2025年1月21日星期二
2020年5月8日星期五
Induction Brazing Carbide to Steel
Objective
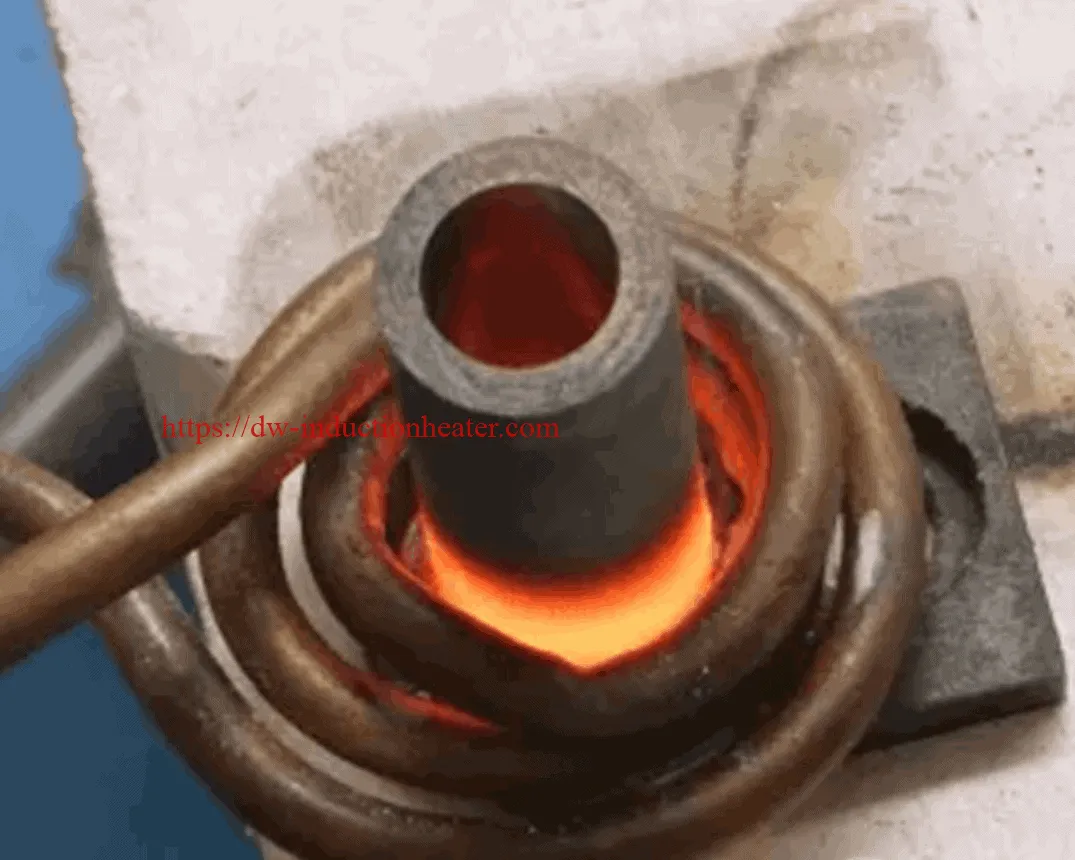
High frequency induction brazing carbide to steel.

Recommended Equipment
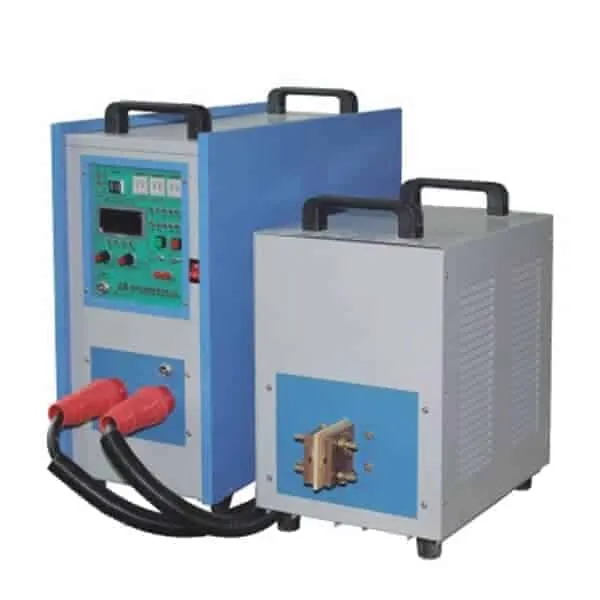
The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
 Materials:
- Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
- Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.

Power: Up to 37kW
Temperature: 1500°F + (815°C+)
Time: Alloy flows at the outer most carbides in 50 seconds. The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.

Results and Conclusions:
Tests results show that carbide removal is possible. Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out. It is important to fixture the part with carbides facing down. An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.


https://dw-inductionheater.com/wp-content/uploads/2020/05/Induction-Brazing-Carbide-to-Steel-4.png?v=1588941803
https://dw-inductionheater.com/induction-brazing-carbide-to-steel-2.html
brazing carbide, brazing carbide inserts to steel, brazing carbide machine, Brazing carbide to steel, brazing steel to carbide, brazing tungsten carbide steel, brazing tungsten carbide to steel, high frequency brazing carbide, induction brazing carbide, Induction Brazing Carbide to Steel, silver brazing carbide to steel
2020年4月22日星期三
Induction Brazing Carbide To Steel
Objective
Induction Brazing carbide to steel parts
Equipment
DW-HF-15kw Induction Heating Power Supply
HLQ custom coil
Key Parameters
Power: 5.88 kW
Temperature: Approximately 1500°F (815°C)
Time: 10 sec

Materials
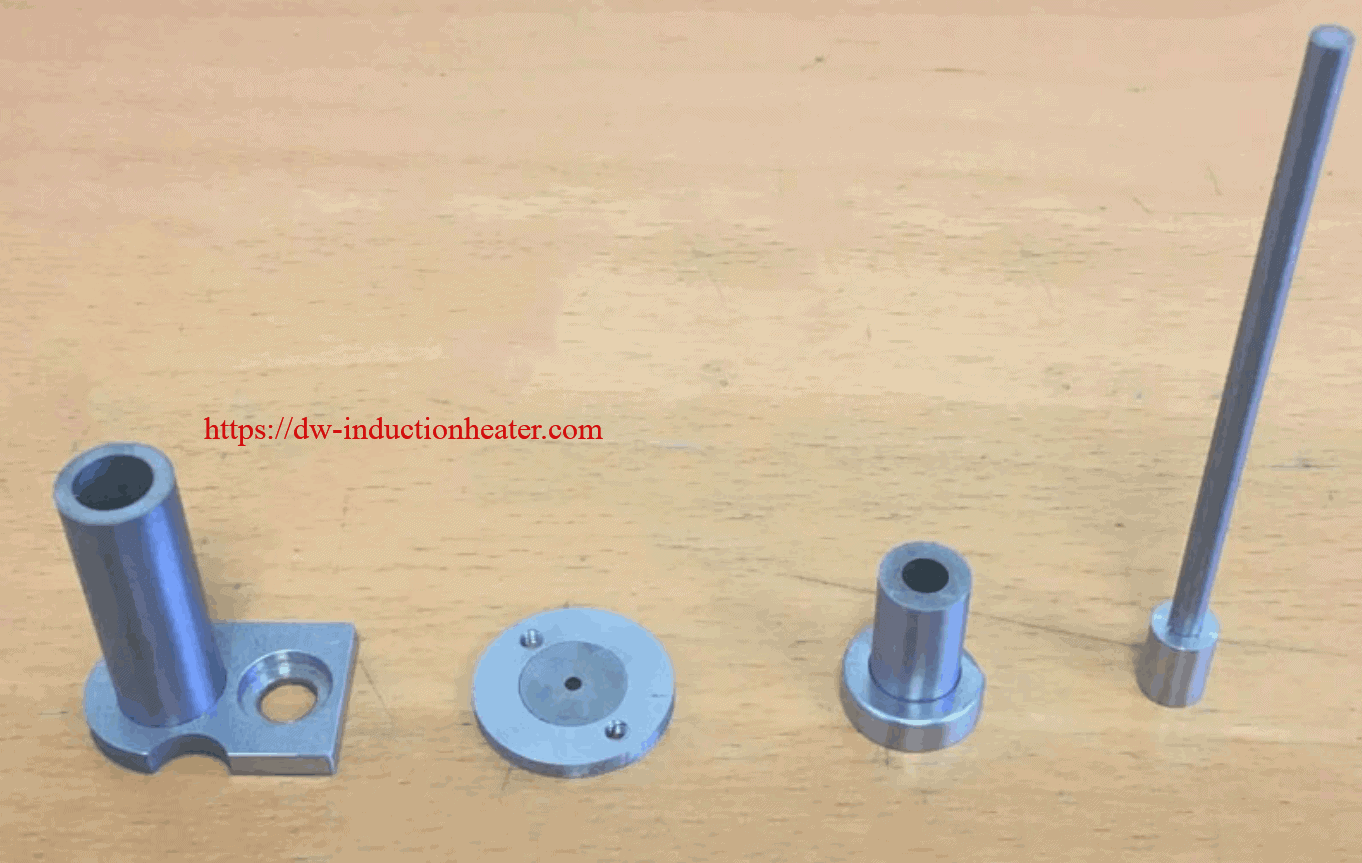
Coil-
2 helical turns (20 mm ID)
1 planar turn (40 mm OD, 13 mm Height)
Carbide-
13 mm OD, 3 mm wall thickness
Steel piece–
20 mm OD, 13 mm ID
Process:
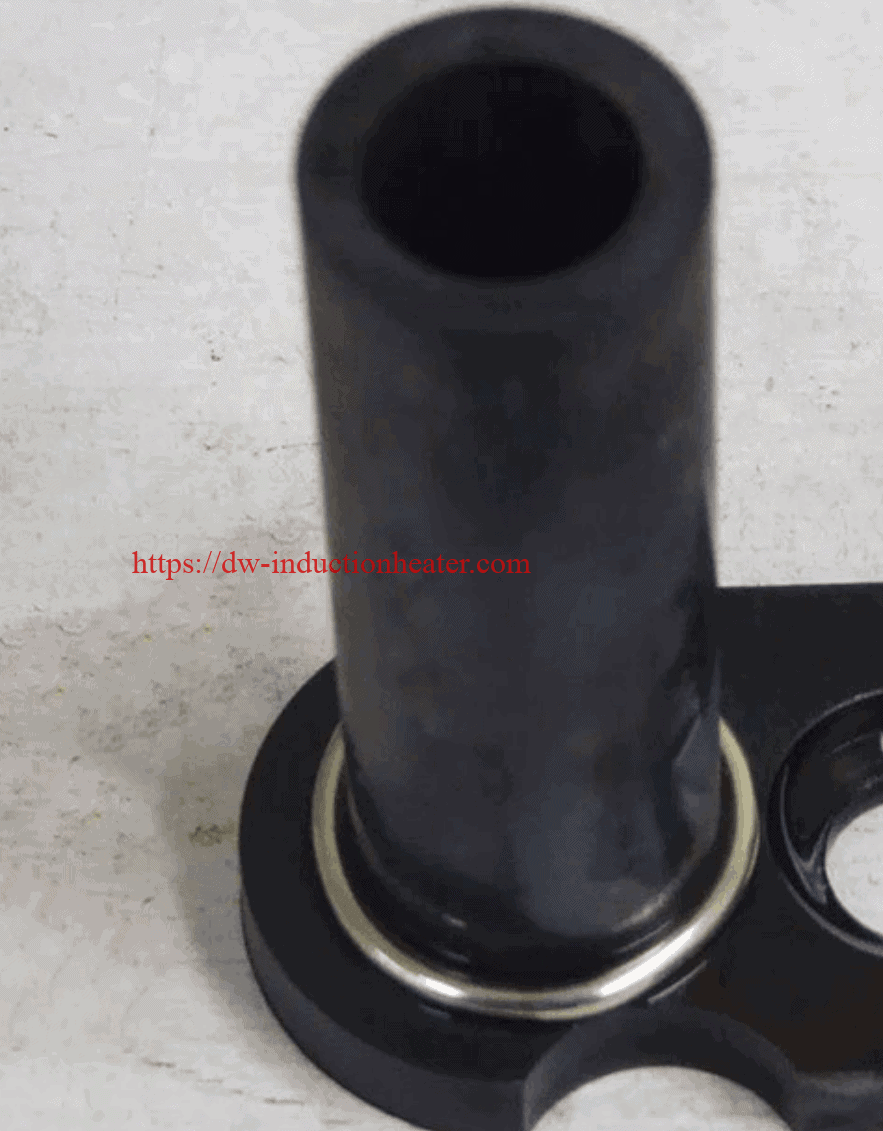
- To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
- The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
- The alloy was heated at approximately 1500°F (815)°C
- The whole piece is left alone and cooled with ambient air


Results/Benefits:
- Induction Brazing was successful all in under 15 seconds with 8kW
- High quality and repeatability of the brazed joints
- Increased productivity
- Rings will need to be developed for specific joints to prevent the use of too much alloy
- Precise control of the time and temperature

https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-brazing-carbide-to-steel-part-process-1024x819.png
https://dw-inductionheater.com/induction-brazing-carbide-to-steel-parts.html
brazing carbide, brazing carbide machine, Brazing carbide to steel, carbide to steel brazing, HF brazing carbide, high frequency brazing carbide, induction brazing carbide, Induction Brazing Carbide to Steel, induction soldering carbide, radio frequency brazing carbide, soldering carbide to steel
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.