 https://dw-inductionheater.com/induction-brazing-carbide-onto-steel-part.html?feed_id=270735&_unique_id=67bd2b8c328d1
2025年2月24日星期一
Induction Brazing Carbide Onto Steel Part
Induction Brazing Carbide Onto Steel Part
https://dw-inductionheater.com/induction-brazing-carbide-onto-steel-part.html?feed_id=270735&_unique_id=67bd2b8c328d1
https://dw-inductionheater.com/induction-brazing-carbide-onto-steel-part.html?feed_id=270735&_unique_id=67bd2b8c328d1

2025年1月26日星期日
2025年1月21日星期二
2024年12月19日星期四
Brazing Carbide to Steel Part With Induction Heating
Brazing Carbide to Steel Part With Induction Heating
 https://dw-inductionheater.com/brazing-carbide-to-steel-part-with-induction-heating.html?feed_id=263978&_unique_id=67642e66ce323
2024年6月26日星期三
Brazing Carbide To Steel With Induction
 Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
https://dw-inductionheater.com/brazing-carbide-to-steel-with-induction.html?feed_id=251678&_unique_id=667d02fb8f6ce
2024年6月23日星期日
Brazing Carbide-Steel Tool with Induction
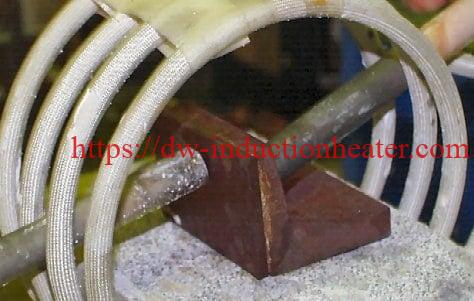 Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
https://dw-inductionheater.com/brazing-carbide-steel-tool-with-induction.html?feed_id=251175&_unique_id=6678ba0cf1926
2024年6月20日星期四
Brazing Carbide To Steel Shank
 Brazing Carbide To Steel Shank with Induction
Objective :Brazing carbide teeth to a steel jaw in less than 5 minutes
Material: Steel pipe jaw, 0.5” (12.7mm) dia, 1.25” (31.75mm) long, 0.25”(6.35mm) thick carbide teeth, black flux and silver copper braze shims
Temperature: 1292ºF (700ºC)
Frequency: 300kHz
Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing one 0.66μF capacitor
• An induction heating coil designed and developed specifically for this application.
Process: A two turn rectangular helical coil is used to heat the carbide and steel to 1292ºF (700ºC) for 4 to 5 minutes. Three braze shims control the amount of braze and the even heat allows for
a good flow of braze creating an aesthetically pleasing bond.
Results/Benefits Induction heating provides:
• Hands-free heating that involves no operator skill for manufacturing
• Consistent, repeatable aesthetically pleasing brazes
• Even distribution of heating
https://dw-inductionheater.com/brazing-carbide-to-steel-shank.html?feed_id=250672&_unique_id=6674711612cba
2020年5月8日星期五
Induction Brazing Carbide to Steel
Objective
High frequency induction brazing carbide to steel.

Recommended Equipment
The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
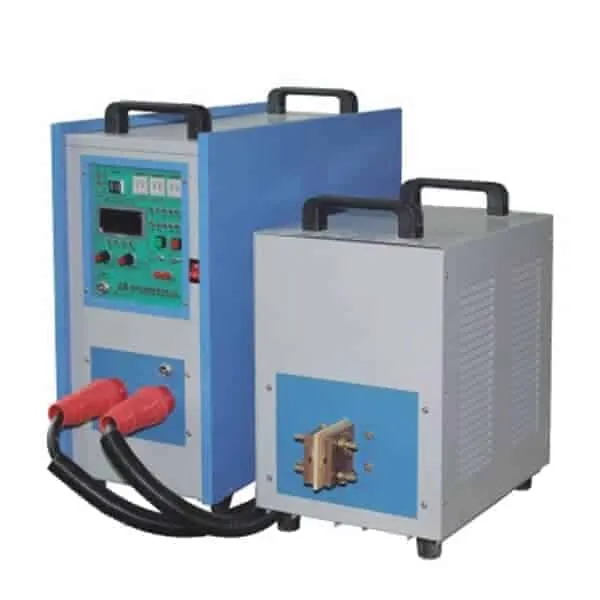 Materials:
- Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
- Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.

Power: Up to 37kW
Temperature: 1500°F + (815°C+)
Time: Alloy flows at the outer most carbides in 50 seconds. The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.

Results and Conclusions:
Tests results show that carbide removal is possible. Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out. It is important to fixture the part with carbides facing down. An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.


https://dw-inductionheater.com/wp-content/uploads/2020/05/Induction-Brazing-Carbide-to-Steel-4.png?v=1588941803
https://dw-inductionheater.com/induction-brazing-carbide-to-steel-2.html
brazing carbide, brazing carbide inserts to steel, brazing carbide machine, Brazing carbide to steel, brazing steel to carbide, brazing tungsten carbide steel, brazing tungsten carbide to steel, high frequency brazing carbide, induction brazing carbide, Induction Brazing Carbide to Steel, silver brazing carbide to steel
2020年4月22日星期三
Induction Brazing Carbide To Steel
Objective
Induction Brazing carbide to steel parts
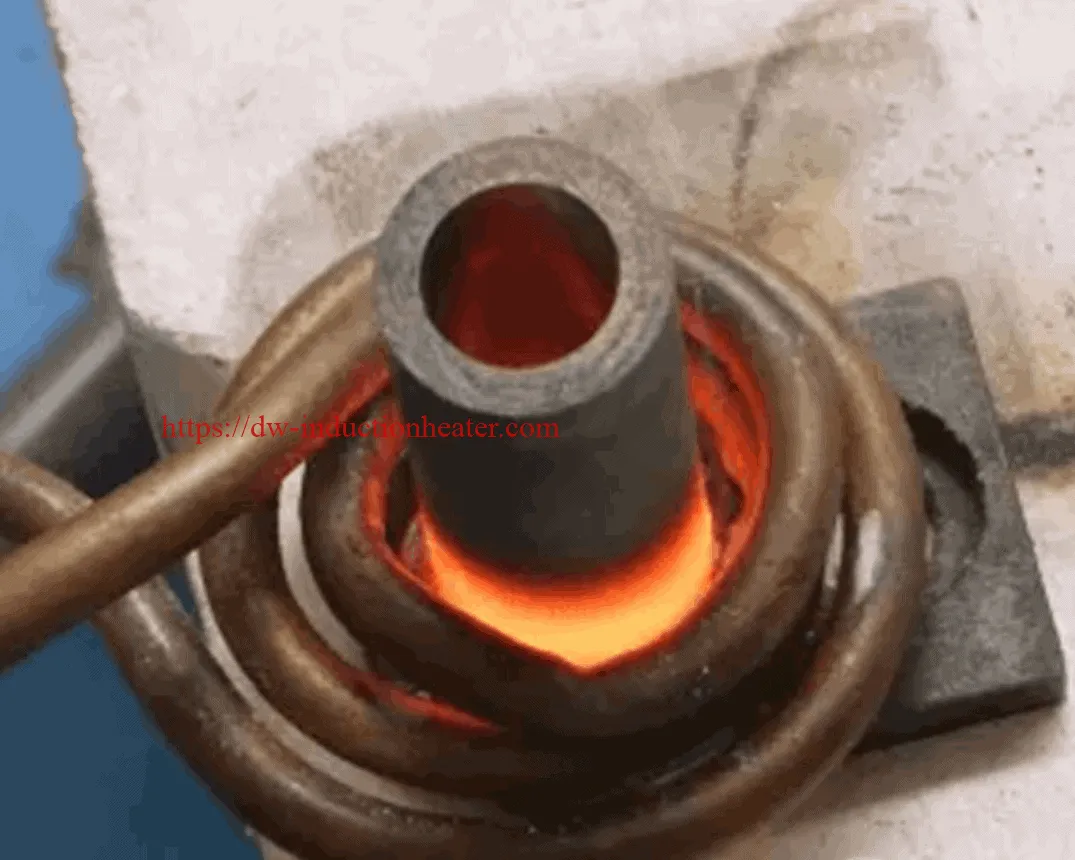
Equipment
DW-HF-15kw Induction Heating Power Supply
HLQ custom coil
Key Parameters
Power: 5.88 kW
Temperature: Approximately 1500°F (815°C)
Time: 10 sec

Materials
Coil-
2 helical turns (20 mm ID)
1 planar turn (40 mm OD, 13 mm Height)
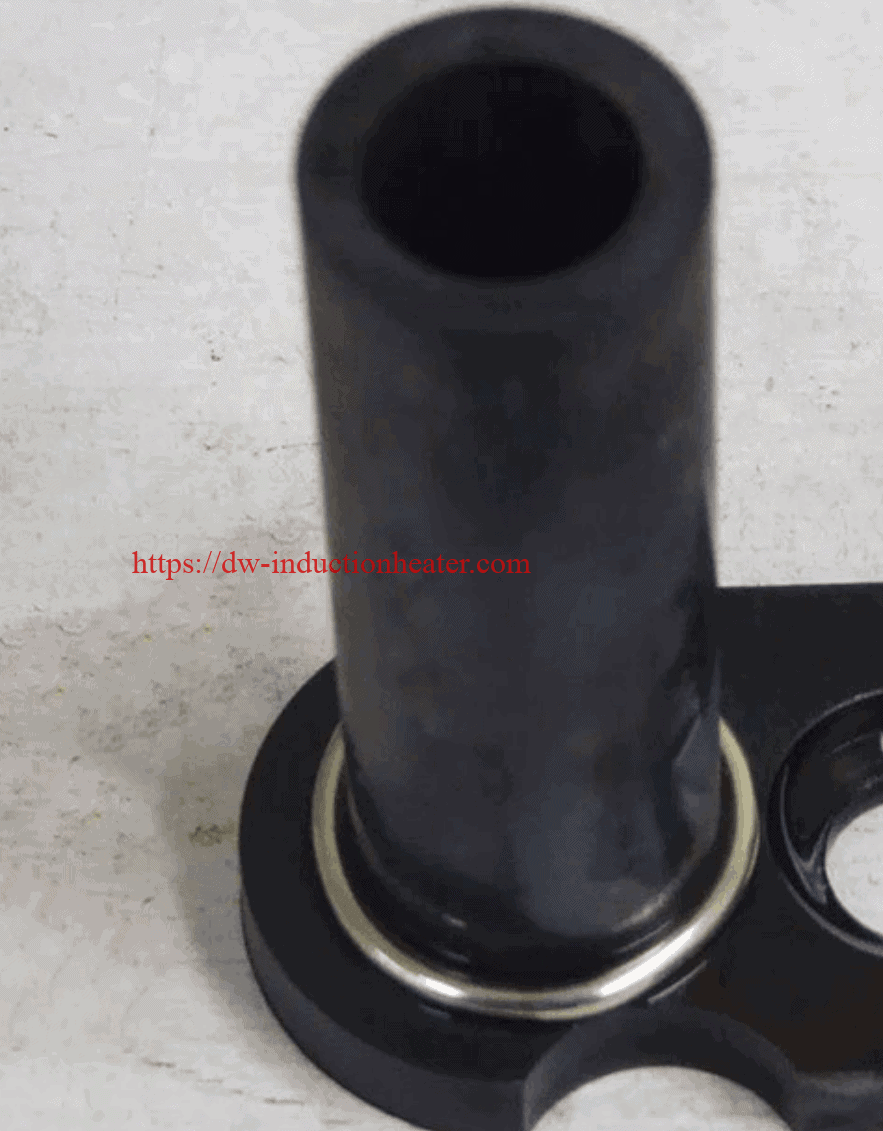
Carbide-
13 mm OD, 3 mm wall thickness
Steel piece–
20 mm OD, 13 mm ID
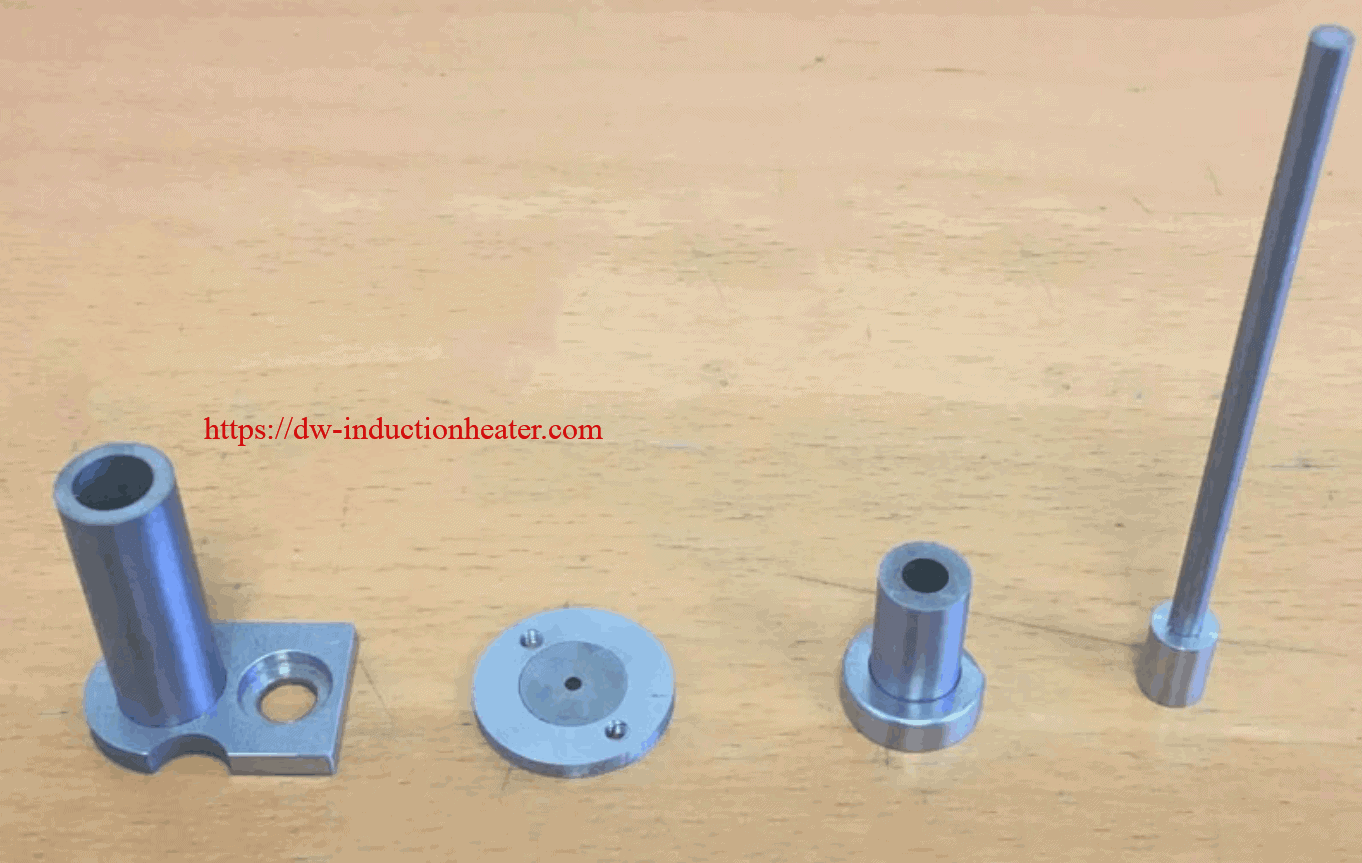
Process:
- To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
- The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
- The alloy was heated at approximately 1500°F (815)°C
- The whole piece is left alone and cooled with ambient air


Results/Benefits:
- Induction Brazing was successful all in under 15 seconds with 8kW
- High quality and repeatability of the brazed joints
- Increased productivity
- Rings will need to be developed for specific joints to prevent the use of too much alloy
- Precise control of the time and temperature

https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-brazing-carbide-to-steel-part-process-1024x819.png
https://dw-inductionheater.com/induction-brazing-carbide-to-steel-parts.html
brazing carbide, brazing carbide machine, Brazing carbide to steel, carbide to steel brazing, HF brazing carbide, high frequency brazing carbide, induction brazing carbide, Induction Brazing Carbide to Steel, induction soldering carbide, radio frequency brazing carbide, soldering carbide to steel
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.