显示标签为“ShrinkFittingSteel”的博文。显示所有博文

2024年5月10日星期五

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube       https://dw-inductionheater.com/induction-shrink-fitting-steel-tube.html?feed_id=245052&_unique_id=663e2b192793f
2023年9月17日星期日

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube       https://dw-inductionheater.com/induction-shrink-fitting-steel-tube.html?feed_id=227471&_unique_id=650786de3142b
2023年3月24日星期五

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      
2023年3月9日星期四

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units

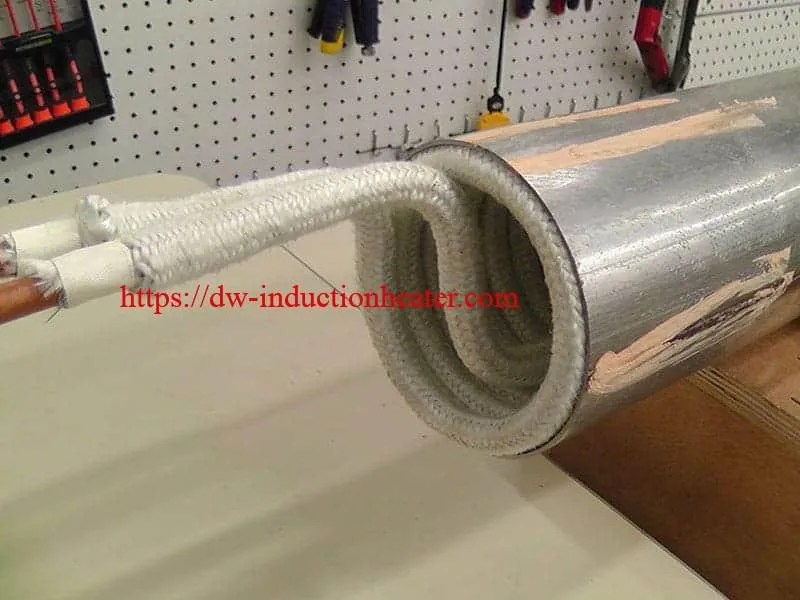
Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures.
Material Steel tubes 7” OD x 4.75” ID x 5” heat zone
Type ‘K’ thermocouple to measure temperature
Thermal blanket
Temperature 500, 800, 1000 °F (260, 427, 538° C)
Frequency 66 kHz
Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF)
A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application.
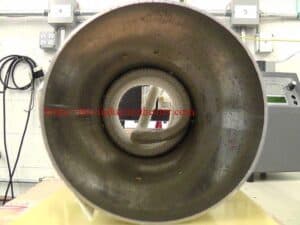
Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured
4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes.
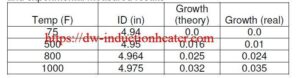
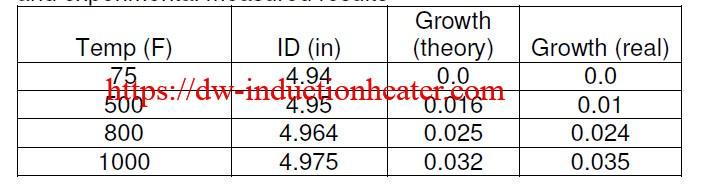
The chart below shows the comparison between theoretical and experimental measured results

1

Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a
thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).


Heating shrink tube


induction shrink fitting tube


Shrink Fitting Steel Tube


2023年1月28日星期六

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      
2022年12月23日星期五

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      

2022年12月18日星期日

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      
2022年12月11日星期日

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      

2022年9月9日星期五

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      

2022年1月19日星期三

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      

2021年11月26日星期五

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      

2021年11月22日星期一

Induction Shrink Fitting Steel Tube

Induction Shrink Fitting Steel Tube With IGBT Heating Units Objective Heating a steel tube to 500-1000°F for a shrink-fitting application. Determine expansion (growth) of ID at varying temperatures. Material Steel tubes 7” OD x 4.75” ID x 5” heat zone Type ‘K’ thermocouple to measure temperature Thermal blanket Temperature 500, 800, 1000 °F (260, 427, 538° C) Frequency 66 kHz Equipment DW-HF-7.5, 7.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 1.5 μF capacitors (for a total of 0.75 μF) A multi-turn, special series-parallel induction heating coil designed and developed specifically for this application. Process Initial tests were completed on a sample without a thermal blanket. A thermocouple is slipped between the copper ring and the steel tube to measure temperature. The part measured 4.940” (at room temperature with an ID gauge.) The part reaches 1000°F (538°C) in about 10 minutes. The chart below shows the comparison between theoretical and experimental measured results 1 Results/Benefits The part measures 4.975” at 1000°F yielding an expansion of 0.035” (4.975 minus 4.94). At 500 and 800°F the expansion numbers were 4.950 and 4.964 respectively. When using a thermal blanket the heat time is reduced by about 90 seconds (8.5 minutes as opposed to 10 minutes).   Heating shrink tube             induction shrink fitting tube               Shrink Fitting Steel Tube      

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.