显示标签为“inductionsolderingsteel”的博文。显示所有博文

2024年5月13日星期一

Induction Soldering Steel Cover

Induction Soldering Steel Cover With High Frequency Heating Units Objective Soldering a nickel plated steel cover onto a nickel plated steel EMI filter housing without damaging the RF circuit Material 2” x 2” (50.8mm) nickel plated steel cover, 2” x 2” (50.8mm) nickel plated steel box and lead-free solder and flux Temperature 573 ºF (300 ºC) Frequency 229 kHz Equipment • DW-UHF-3 kW induction heating system, equipped with a remote workhead containing two 1.2μF capacitors for a total of 2.4μF • An induction heating coil designed and developed specifically for this application. Process A single turn square helical coil is used to solder the cover to the filter box. Solder flux is applied to the filter box and two solder turns (preforms) are placed covering the perimeter of the cover. The assembly is positioned under the coil and power is applied for 7 seconds to solder the seam. Results/Benefits Induction heating provides: • Hands-free heating that involves no operator skill for manufacturing • Repeatable, non-contact clean heating • Fast precise heating • Good solder flow without over heating the box and damaging RF circuits. • Even distribution of heating induction soldering steel cover https://dw-inductionheater.com/induction-soldering-steel-cover.html?feed_id=245460&_unique_id=664273e3b12a0

2024年3月31日星期日

Induction Soldering Stainless Steel Tubes to Brass Base

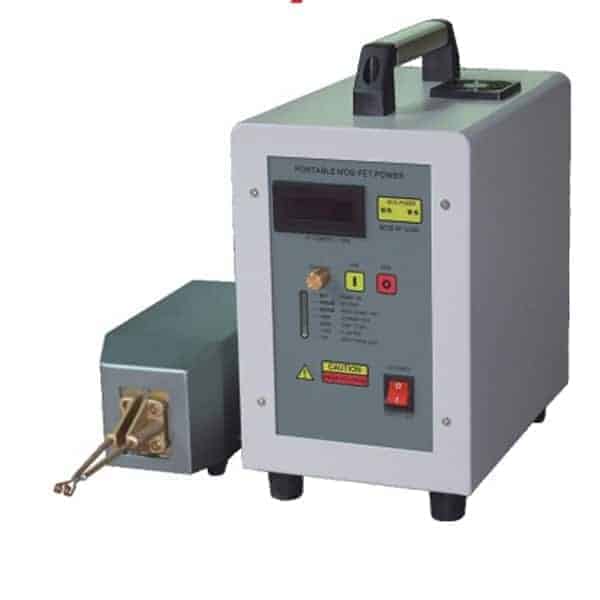
Objective Induction Soldering stainless steel tubes to brass base Equipment DW-UHF-6KW-III handheld induction heater
Materials Customer material including flux Key Parameters Power: 2 kW Temperature: 482°F (250°C not measured) Time: 14 -16 sec
Process Steps Customer process instruction has been followed DW-UHF-6KW-III induction heating system was limited to 2kW Results and Conclusions Sample position according to the coil is vital.Induction Soldering Stainless steel is heated much fasted than the brass. So, the coil is positioned over the brass part (around 95%)
https://dw-inductionheater.com/induction-soldering-stainless-steel-tubes-to-brass-base.html?feed_id=239460&_unique_id=660a09f1c983d

2024年3月27日星期三

Induction Soldering magnetic steel pins

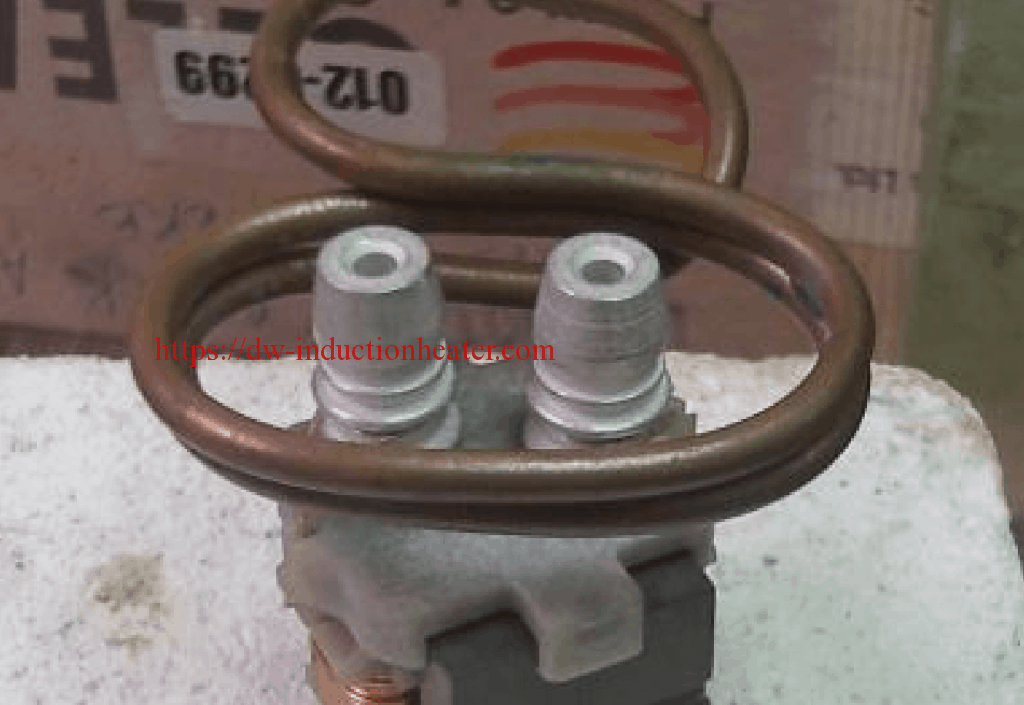
Objective Induction soldering magnetic steel pins/posts to create an automotive component Material • Coil and steel pin assembly (5/16”/7.9 mm pin/post O.D.) • Solder rosin core Temperature.   470 ºF (243 ºC) Frequency.   214 kHz Equipment • DW-UHF- 6kW-I Induction heating machine,  150 to 400 kHz induction heating system equipped with a remote workhead containing one 1.33 uf capacitor for a total of 1.33 uf • A single-position two-turn pancake induction heating coil designed and developed specifically for this application Process. Any remaining insulation on the wire was removed with sand paper. A foot peddle was part of the induction heating system setup to facilitate manual feeding of the solder. The part was placed in the coil and the power was turned on. After seven seconds the solder began to flow and the solder was fed to the joint. Power was pulsed for one additional second to allow the solder to continue to be fed. The overall process took less than ten seconds. Results/Benefits Speed: Induction Heating took less than 10 seconds, and while this is a new process for the client, other heating methods would be slower • Precise, repeatable heating: Induction is a highly repeatableprocess so the customer can expect the same result everytime with only the portion of the part requiring heating being heated • Safety: There is no open flame with induction, which makes it a safer method of heating than torch heating   https://dw-inductionheater.com/high-frequency-induction-soldering-magnetic-steel-pins.html?feed_id=238889&_unique_id=66050a0769f57
2023年8月23日星期三

Induction Soldering Stainless Steel Tubes to Brass Base

Objective Induction Soldering stainless steel tubes to brass base Equipment DW-UHF-6KW-III handheld induction heater
Materials Customer material including flux Key Parameters Power: 2 kW Temperature: 482°F (250°C not measured) Time: 14 -16 sec
Process Steps Customer process instruction has been followed DW-UHF-6KW-III induction heating system was limited to 2kW Results and Conclusions Sample position according to the coil is vital.Induction Soldering Stainless steel is heated much fasted than the brass. So, the coil is positioned over the brass part (around 95%)

2023年8月9日星期三

Induction Soldering Stainless Steel Tubes to Brass Base

Objective Induction Soldering stainless steel tubes to brass base Equipment DW-UHF-6KW-III handheld induction heater
Materials Customer material including flux Key Parameters Power: 2 kW Temperature: 482°F (250°C not measured) Time: 14 -16 sec
Process Steps Customer process instruction has been followed DW-UHF-6KW-III induction heating system was limited to 2kW Results and Conclusions Sample position according to the coil is vital.Induction Soldering Stainless steel is heated much fasted than the brass. So, the coil is positioned over the brass part (around 95%)
https://dw-inductionheater.com/induction-soldering-stainless-steel-tubes-to-brass-base.html?feed_id=222436&_unique_id=64d35e9b55ffe

2023年8月5日星期六

Induction Soldering magnetic steel pins

Objective Induction soldering magnetic steel pins/posts to create an automotive component Material • Coil and steel pin assembly (5/16”/7.9 mm pin/post O.D.) • Solder rosin core Temperature.   470 ºF (243 ºC) Frequency.   214 kHz Equipment • DW-UHF- 6kW-I Induction heating machine,  150 to 400 kHz induction heating system equipped with a remote workhead containing one 1.33 uf capacitor for a total of 1.33 uf • A single-position two-turn pancake induction heating coil designed and developed specifically for this application Process. Any remaining insulation on the wire was removed with sand paper. A foot peddle was part of the induction heating system setup to facilitate manual feeding of the solder. The part was placed in the coil and the power was turned on. After seven seconds the solder began to flow and the solder was fed to the joint. Power was pulsed for one additional second to allow the solder to continue to be fed. The overall process took less than ten seconds. Results/Benefits Speed: Induction Heating took less than 10 seconds, and while this is a new process for the client, other heating methods would be slower • Precise, repeatable heating: Induction is a highly repeatableprocess so the customer can expect the same result everytime with only the portion of the part requiring heating being heated • Safety: There is no open flame with induction, which makes it a safer method of heating than torch heating   https://dw-inductionheater.com/high-frequency-induction-soldering-magnetic-steel-pins.html?feed_id=221911&_unique_id=64ce5ddc591ca

2023年6月26日星期一

Induction Soldering magnetic steel pins

Objective Induction soldering magnetic steel pins/posts to create an automotive component Material • Coil and steel pin assembly (5/16”/7.9 mm pin/post O.D.) • Solder rosin core Temperature.   470 ºF (243 ºC) Frequency.   214 kHz Equipment • DW-UHF- 6kW-I Induction heating machine,  150 to 400 kHz induction heating system equipped with a remote workhead containing one 1.33 uf capacitor for a total of 1.33 uf • A single-position two-turn pancake induction heating coil designed and developed specifically for this application Process. Any remaining insulation on the wire was removed with sand paper. A foot peddle was part of the induction heating system setup to facilitate manual feeding of the solder. The part was placed in the coil and the power was turned on. After seven seconds the solder began to flow and the solder was fed to the joint. Power was pulsed for one additional second to allow the solder to continue to be fed. The overall process took less than ten seconds. Results/Benefits Speed: Induction Heating took less than 10 seconds, and while this is a new process for the client, other heating methods would be slower • Precise, repeatable heating: Induction is a highly repeatableprocess so the customer can expect the same result everytime with only the portion of the part requiring heating being heated • Safety: There is no open flame with induction, which makes it a safer method of heating than torch heating  

2023年5月5日星期五

Induction Soldering magnetic steel pins

Objective Induction soldering magnetic steel pins/posts to create an automotive component Material • Coil and steel pin assembly (5/16”/7.9 mm pin/post O.D.) • Solder rosin core Temperature.   470 ºF (243 ºC) Frequency.   214 kHz Equipment • DW-UHF- 6kW-I Induction heating machine,  150 to 400 kHz induction heating system equipped with a remote workhead containing one 1.33 uf capacitor for a total of 1.33 uf • A single-position two-turn pancake induction heating coil designed and developed specifically for this application Process. Any remaining insulation on the wire was removed with sand paper. A foot peddle was part of the induction heating system setup to facilitate manual feeding of the solder. The part was placed in the coil and the power was turned on. After seven seconds the solder began to flow and the solder was fed to the joint. Power was pulsed for one additional second to allow the solder to continue to be fed. The overall process took less than ten seconds. Results/Benefits Speed: Induction Heating took less than 10 seconds, and while this is a new process for the client, other heating methods would be slower • Precise, repeatable heating: Induction is a highly repeatableprocess so the customer can expect the same result everytime with only the portion of the part requiring heating being heated • Safety: There is no open flame with induction, which makes it a safer method of heating than torch heating  

2023年4月9日星期日

Induction Soldering magnetic steel pins

Objective Induction soldering magnetic steel pins/posts to create an automotive component Material • Coil and steel pin assembly (5/16”/7.9 mm pin/post O.D.) • Solder rosin core Temperature.   470 ºF (243 ºC) Frequency.   214 kHz Equipment • DW-UHF- 6kW-I Induction heating machine,  150 to 400 kHz induction heating system equipped with a remote workhead containing one 1.33 uf capacitor for a total of 1.33 uf • A single-position two-turn pancake induction heating coil designed and developed specifically for this application Process. Any remaining insulation on the wire was removed with sand paper. A foot peddle was part of the induction heating system setup to facilitate manual feeding of the solder. The part was placed in the coil and the power was turned on. After seven seconds the solder began to flow and the solder was fed to the joint. Power was pulsed for one additional second to allow the solder to continue to be fed. The overall process took less than ten seconds. Results/Benefits Speed: Induction Heating took less than 10 seconds, and while this is a new process for the client, other heating methods would be slower • Precise, repeatable heating: Induction is a highly repeatableprocess so the customer can expect the same result everytime with only the portion of the part requiring heating being heated • Safety: There is no open flame with induction, which makes it a safer method of heating than torch heating  

2023年3月15日星期三

Induction Soldering Stainless Steel Tubes to Brass Base


Objective
Induction Soldering stainless steel tubes to brass base


Equipment
DW-UHF-6KW-III handheld induction heater


Materials
Customer material
including flux

Key Parameters
Power: 2 kW
Temperature: 482°F (250°C not measured)
Time: 14 -16 sec


Process Steps

Customer process instruction has been followed
DW-UHF-6KW-III induction heating system was limited to 2kW

Results and Conclusions

Sample position according to the coil is vital.Induction Soldering Stainless steel is heated much fasted than the brass. So, the coil is positioned over the brass part (around 95%)


2023年2月2日星期四

Induction Soldering Stainless Steel Tubes to Brass Base

Objective Induction Soldering stainless steel tubes to brass base Equipment DW-UHF-6KW-III handheld induction heater
Materials Customer material including flux Key Parameters Power: 2 kW Temperature: 482°F (250°C not measured) Time: 14 -16 sec
Process Steps Customer process instruction has been followed DW-UHF-6KW-III induction heating system was limited to 2kW Results and Conclusions Sample position according to the coil is vital.Induction Soldering Stainless steel is heated much fasted than the brass. So, the coil is positioned over the brass part (around 95%)

Induction Soldering Steel Cover

Induction Soldering Steel Cover With High Frequency Heating Units Objective Soldering a nickel plated steel cover onto a nickel plated steel EMI filter housing without damaging the RF circuit Material 2” x 2” (50.8mm) nickel plated steel cover, 2” x 2” (50.8mm) nickel plated steel box and lead-free solder and flux Temperature 573 ºF (300 ºC) Frequency 229 kHz Equipment • DW-UHF-3 kW induction heating system, equipped with a remote workhead containing two 1.2μF capacitors for a total of 2.4μF • An induction heating coil designed and developed specifically for this application. Process A single turn square helical coil is used to solder the cover to the filter box. Solder flux is applied to the filter box and two solder turns (preforms) are placed covering the perimeter of the cover. The assembly is positioned under the coil and power is applied for 7 seconds to solder the seam. Results/Benefits Induction heating provides: • Hands-free heating that involves no operator skill for manufacturing • Repeatable, non-contact clean heating • Fast precise heating • Good solder flow without over heating the box and damaging RF circuits. • Even distribution of heating induction soldering steel cover

2023年1月26日星期四

Induction Soldering Stainless Steel Tubes to Brass Base

Objective Induction Soldering stainless steel tubes to brass base Equipment DW-UHF-6KW-III handheld induction heater
Materials Customer material including flux Key Parameters Power: 2 kW Temperature: 482°F (250°C not measured) Time: 14 -16 sec
Process Steps Customer process instruction has been followed DW-UHF-6KW-III induction heating system was limited to 2kW Results and Conclusions Sample position according to the coil is vital.Induction Soldering Stainless steel is heated much fasted than the brass. So, the coil is positioned over the brass part (around 95%)

2022年12月25日星期日

Induction Soldering magnetic steel pins

Objective Induction soldering magnetic steel pins/posts to create an automotive component Material • Coil and steel pin assembly (5/16”/7.9 mm pin/post O.D.) • Solder rosin core Temperature.   470 ºF (243 ºC) Frequency.   214 kHz Equipment • DW-UHF- 6kW-I Induction heating machine,  150 to 400 kHz induction heating system equipped with a remote workhead containing one 1.33 uf capacitor for a total of 1.33 uf • A single-position two-turn pancake induction heating coil designed and developed specifically for this application Process. Any remaining insulation on the wire was removed with sand paper. A foot peddle was part of the induction heating system setup to facilitate manual feeding of the solder. The part was placed in the coil and the power was turned on. After seven seconds the solder began to flow and the solder was fed to the joint. Power was pulsed for one additional second to allow the solder to continue to be fed. The overall process took less than ten seconds. Results/Benefits Speed: Induction Heating took less than 10 seconds, and while this is a new process for the client, other heating methods would be slower • Precise, repeatable heating: Induction is a highly repeatableprocess so the customer can expect the same result everytime with only the portion of the part requiring heating being heated • Safety: There is no open flame with induction, which makes it a safer method of heating than torch heating  

2022年11月15日星期二

Induction Soldering magnetic steel pins

Objective Induction soldering magnetic steel pins/posts to create an automotive component Material • Coil and steel pin assembly (5/16”/7.9 mm pin/post O.D.) • Solder rosin core Temperature.   470 ºF (243 ºC) Frequency.   214 kHz Equipment • DW-UHF- 6kW-I Induction heating machine,  150 to 400 kHz induction heating system equipped with a remote workhead containing one 1.33 uf capacitor for a total of 1.33 uf • A single-position two-turn pancake induction heating coil designed and developed specifically for this application Process. Any remaining insulation on the wire was removed with sand paper. A foot peddle was part of the induction heating system setup to facilitate manual feeding of the solder. The part was placed in the coil and the power was turned on. After seven seconds the solder began to flow and the solder was fed to the joint. Power was pulsed for one additional second to allow the solder to continue to be fed. The overall process took less than ten seconds. Results/Benefits Speed: Induction Heating took less than 10 seconds, and while this is a new process for the client, other heating methods would be slower • Precise, repeatable heating: Induction is a highly repeatableprocess so the customer can expect the same result everytime with only the portion of the part requiring heating being heated • Safety: There is no open flame with induction, which makes it a safer method of heating than torch heating  

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.