显示标签为“inductionheatingmold”的博文。显示所有博文

2024年5月31日星期五

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                   https://dw-inductionheater.com/induction-heating-steel-mold.html?feed_id=248086&_unique_id=665abb997897c

2023年10月13日星期五

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries https://dw-inductionheater.com/induction-heating-steel-casting.html?feed_id=228936&_unique_id=652917b3bdc1b

2023年10月9日星期一

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                   https://dw-inductionheater.com/induction-heating-steel-mold.html?feed_id=228726&_unique_id=6524180b6fa37

2023年9月5日星期二

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                  

2023年8月22日星期二

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                  

2023年8月7日星期一

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                  

2023年7月14日星期五

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries

2023年4月24日星期一

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries

2023年3月22日星期三

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries

2023年3月17日星期五

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System

Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization
Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width,
approximately 77.2 lbs (35kg)
Temperature 392ºF (200ºC)
Frequency 20kHz
Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF
• An induction heating coil designed and developed specifically for this application.
Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the
mold.
Results/Benefits Induction heating provides:
• Repeatable and consistent heat
• Quicker process time, increased production
• Even distribution of heating
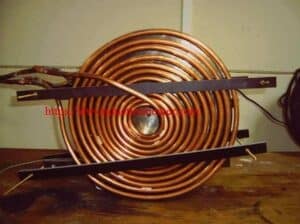
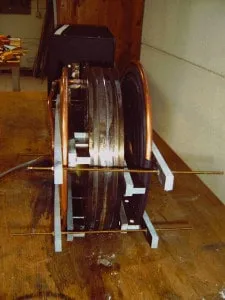
induction heating steel mold


RF heating steel mold


2023年1月29日星期日

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                  

2023年1月21日星期六

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                  

2022年12月29日星期四

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries

2022年11月8日星期二

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries

2022年10月24日星期一

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                  

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries

2022年9月14日星期三

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                  

2022年9月11日星期日

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries

2022年9月8日星期四

Induction Heating Steel Mold

Induction Heating Steel Mold For Rubber Seal With High Frequency Heating System Objective To heat a steel mold evenly to 392ºF (200ºC) to be used on a press for rubber seal vulcanization Material Steel mold 13.4” (340mm) diameter, 2.16” (55mm) width, approximately 77.2 lbs (35kg) Temperature 392ºF (200ºC) Frequency 20kHz Equipment • DW-MF-70kW induction heating system, equipped with a remote workhead containing eight 0.3μF capacitors for a total of 0.6μF • An induction heating coil designed and developed specifically for this application. Process Two thirteen turn pancake coils are used to heat both sides of the mold simultaneously for 170 seconds to reach an external temperature of 392ºF (200ºC). The power is continually decreased over the next 390 seconds to reach a uniform temperature of 392ºF (200ºC) ± 41ºF (5ºC) throughout the mold. Results/Benefits Induction heating provides: • Repeatable and consistent heat • Quicker process time, increased production • Even distribution of heating induction heating steel mold             RF heating steel mold                  

2022年8月3日星期三

induction heating steel casting

induction heating steel casting of rubber mold with high frequency induction heater Objective To preheat two irregularly shaped steel castings to be molded and bonded with synthetic rubber Material Two steel castings, 17 lb. irregularly shaped, approximately 6” (152mm) x 9” (229mm) x 1” (25.4mm) Temperature 400 ºF (204 ºC) Frequency 20 kHz Equipment • DW-MF-45kW induction heating system, equipped with a remote workhead containing four 1.0 μF capacitors (for a total of 1.0 μF). • An induction heating coil designed and developed specifically for this application. Process Two steel castings are placed onto an insulated plate with brass guide location pins. The plate is placed onto a table which slides into a large multi-turn helical coil. The parts are induction heated to 400 ºF in 180 seconds. The slow heating time allows the parts to come up to temperature evenly. When the heating cycle is completed each part is placed into a press for the molding and bonding operation. Results/Benefits Induction heating for bulk preheating of steel castings produces: • efficient and repeatable heat vs. a torch or an oven. • even heating of parts throughout Large multi-turn coils provide: • easy loading and unloading of the parts • flexibility for varying bulk castings sizes and geometries

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.