显示标签为“highfrequencyannealingtubes”的博文。显示所有博文

2024年3月26日星期二

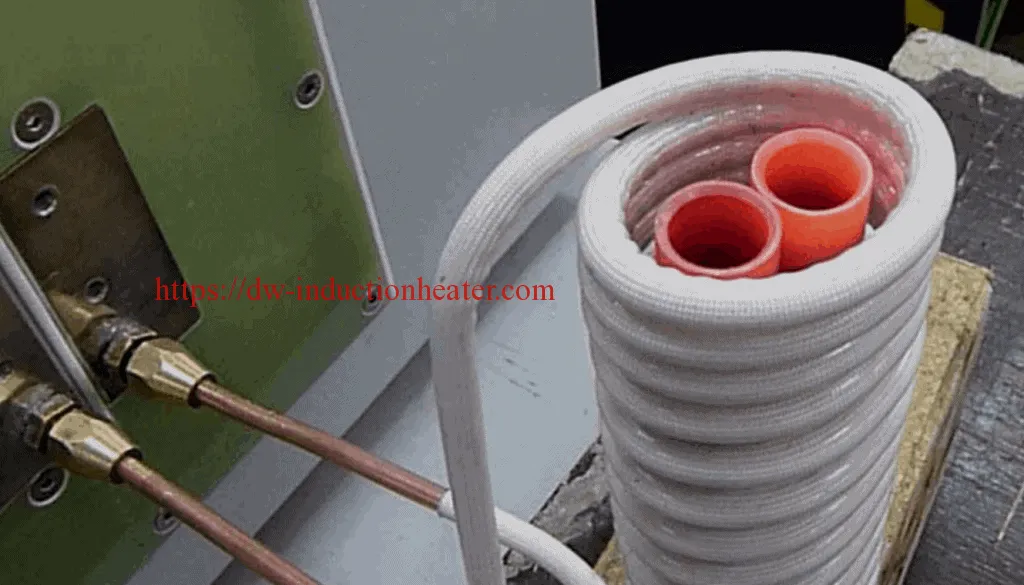
Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe
https://dw-inductionheater.com/induction-annealing-copper-tubes.html?feed_id=238658&_unique_id=66039c78a290b

2023年10月18日星期三

Induction Annealing Stainless Steel Tubes

Induction Annealing Stainless Steel Tubes With High Frequency Heating Equipment Objective To anneal a ¼” area around an oval cutout on a stainless steel tube prior to extrusion Material .75” (19mm), 1.5” (38.1mm) and 4” (101.6mm) diameter steel tubes Temperature 1900 ºF ( 1038 ºC) Frequency 300 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A single turn helical coil is used on the 4” (101.6mm) diameter tubes and a two turn helical coil is used on the smaller diameters. The coil is placed over the oval cutout and power is supplied for 15 seconds to anneal a .25 (6.35mm) diameter around the cutout. Results/Benefits Induction heating provides: • Precise and controllable placement of heat to anneal only the required area • Faster process than flame • Repeatable results • Hands-free heating that involves no operator skill for manufacturing Annealing Stainless Steel Tubes   https://dw-inductionheater.com/induction-annealing-stainless-steel-tubes.html?feed_id=229206&_unique_id=652f852306c8c

2023年10月2日星期一

Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe

2023年9月29日星期五

Induction Annealing Stainless Steel Tubes

Induction Annealing Stainless Steel Tubes With High Frequency Heating Equipment Objective To anneal a ¼” area around an oval cutout on a stainless steel tube prior to extrusion Material .75” (19mm), 1.5” (38.1mm) and 4” (101.6mm) diameter steel tubes Temperature 1900 ºF ( 1038 ºC) Frequency 300 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A single turn helical coil is used on the 4” (101.6mm) diameter tubes and a two turn helical coil is used on the smaller diameters. The coil is placed over the oval cutout and power is supplied for 15 seconds to anneal a .25 (6.35mm) diameter around the cutout. Results/Benefits Induction heating provides: • Precise and controllable placement of heat to anneal only the required area • Faster process than flame • Repeatable results • Hands-free heating that involves no operator skill for manufacturing Annealing Stainless Steel Tubes  

2023年9月2日星期六

Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe

2023年8月3日星期四

Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe
https://dw-inductionheater.com/induction-annealing-copper-tubes.html?feed_id=221761&_unique_id=64cc2c0bed1c7

2023年7月23日星期日

Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe

2023年5月4日星期四

Induction Annealing Stainless Steel Tubes

Induction Annealing Stainless Steel Tubes With High Frequency Heating Equipment Objective To anneal a ¼” area around an oval cutout on a stainless steel tube prior to extrusion Material .75” (19mm), 1.5” (38.1mm) and 4” (101.6mm) diameter steel tubes Temperature 1900 ºF ( 1038 ºC) Frequency 300 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A single turn helical coil is used on the 4” (101.6mm) diameter tubes and a two turn helical coil is used on the smaller diameters. The coil is placed over the oval cutout and power is supplied for 15 seconds to anneal a .25 (6.35mm) diameter around the cutout. Results/Benefits Induction heating provides: • Precise and controllable placement of heat to anneal only the required area • Faster process than flame • Repeatable results • Hands-free heating that involves no operator skill for manufacturing Annealing Stainless Steel Tubes  

2023年4月23日星期日

Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe

2023年3月26日星期日

Induction Annealing Stainless Steel Tubes

Induction Annealing Stainless Steel Tubes With High Frequency Heating Equipment Objective To anneal a ¼” area around an oval cutout on a stainless steel tube prior to extrusion Material .75” (19mm), 1.5” (38.1mm) and 4” (101.6mm) diameter steel tubes Temperature 1900 ºF ( 1038 ºC) Frequency 300 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A single turn helical coil is used on the 4” (101.6mm) diameter tubes and a two turn helical coil is used on the smaller diameters. The coil is placed over the oval cutout and power is supplied for 15 seconds to anneal a .25 (6.35mm) diameter around the cutout. Results/Benefits Induction heating provides: • Precise and controllable placement of heat to anneal only the required area • Faster process than flame • Repeatable results • Hands-free heating that involves no operator skill for manufacturing Annealing Stainless Steel Tubes  

2023年3月19日星期日

Induction Annealing Stainless Steel Tubes

Induction Annealing Stainless Steel Tubes With High Frequency Heating Equipment Objective To anneal a ¼” area around an oval cutout on a stainless steel tube prior to extrusion Material .75” (19mm), 1.5” (38.1mm) and 4” (101.6mm) diameter steel tubes Temperature 1900 ºF ( 1038 ºC) Frequency 300 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A single turn helical coil is used on the 4” (101.6mm) diameter tubes and a two turn helical coil is used on the smaller diameters. The coil is placed over the oval cutout and power is supplied for 15 seconds to anneal a .25 (6.35mm) diameter around the cutout. Results/Benefits Induction heating provides: • Precise and controllable placement of heat to anneal only the required area • Faster process than flame • Repeatable results • Hands-free heating that involves no operator skill for manufacturing Annealing Stainless Steel Tubes  

2023年3月18日星期六

Induction Annealing Copper Tubes


Objective
Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.


Equipment
DW-HF-45kw induction heater


Helical coil

Material
• Two copper tubes
– OD: 0.69’’ (1.75 cm)
– ID: 0.55’’ (1.40 cm)
– Length: 5.50’’ (14.0 cm).

Key Parameters
Power: 27kW
Temperature: 842°F (450°C)
Time: 5 sec


Process:

  1. The two copper tubes were placed together in the coil.

  2. Induction heating was applied for 5s.


Results/Benefits:

  • Improved process control for uniform induction heating to a desired temperature

  • Power on demand and rapid, consistent heat cycles

  • Technology without pollution, which is both clean and safe


2023年2月24日星期五

Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe

2023年1月28日星期六

Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe

2023年1月27日星期五

Induction Annealing Copper Tubes

Objective Uniformly high frequency annealing copper tubes simultaneously to 800°F (426°C) in under 10 seconds with induction heating.
Equipment DW-HF-45kw induction heater Helical coil Material • Two copper tubes – OD: 0.69’’ (1.75 cm) – ID: 0.55’’ (1.40 cm) – Length: 5.50’’ (14.0 cm). Key Parameters Power: 27kW Temperature: 842°F (450°C) Time: 5 sec
Process:
  1. The two copper tubes were placed together in the coil.
  2. Induction heating was applied for 5s.
Results/Benefits:
  • Improved process control for uniform induction heating to a desired temperature
  • Power on demand and rapid, consistent heat cycles
  • Technology without pollution, which is both clean and safe

2023年1月9日星期一

Induction Annealing Stainless Steel Tubes

Induction Annealing Stainless Steel Tubes With High Frequency Heating Equipment Objective To anneal a ¼” area around an oval cutout on a stainless steel tube prior to extrusion Material .75” (19mm), 1.5” (38.1mm) and 4” (101.6mm) diameter steel tubes Temperature 1900 ºF ( 1038 ºC) Frequency 300 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A single turn helical coil is used on the 4” (101.6mm) diameter tubes and a two turn helical coil is used on the smaller diameters. The coil is placed over the oval cutout and power is supplied for 15 seconds to anneal a .25 (6.35mm) diameter around the cutout. Results/Benefits Induction heating provides: • Precise and controllable placement of heat to anneal only the required area • Faster process than flame • Repeatable results • Hands-free heating that involves no operator skill for manufacturing Annealing Stainless Steel Tubes  

2022年11月12日星期六

Induction Annealing Stainless Steel Tubes

Induction Annealing Stainless Steel Tubes With High Frequency Heating Equipment Objective To anneal a ¼” area around an oval cutout on a stainless steel tube prior to extrusion Material .75” (19mm), 1.5” (38.1mm) and 4” (101.6mm) diameter steel tubes Temperature 1900 ºF ( 1038 ºC) Frequency 300 kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A single turn helical coil is used on the 4” (101.6mm) diameter tubes and a two turn helical coil is used on the smaller diameters. The coil is placed over the oval cutout and power is supplied for 15 seconds to anneal a .25 (6.35mm) diameter around the cutout. Results/Benefits Induction heating provides: • Precise and controllable placement of heat to anneal only the required area • Faster process than flame • Repeatable results • Hands-free heating that involves no operator skill for manufacturing Annealing Stainless Steel Tubes  

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.