2021年11月17日星期三
Induction Brazing Stainless Steel Tubes
Induction Brazing Stainless Steel Tubes With High Frequency Heating System
Research Objective
To braze two lengths of stainless steel tubing together at low temperature within 20 seconds
Parts & Materials Description
(2) .350 O.D. steel tubes, one with a slight flare at edge; BAg-24 brazing wire, black flux
Temperature Required
1330°F
Induction Heating Equipment
DW-UHF-10kW RF Induction power supply, 4-turn helical inductor (coil) with 1.5” O.D.
Operating Frequency
300 kHz
Heating Procedure
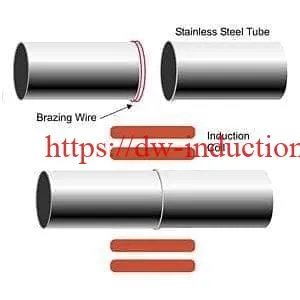
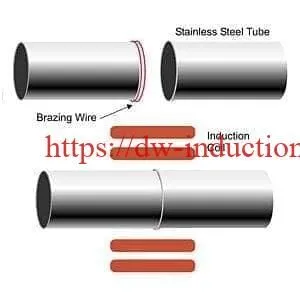
The testing was done in an open air atmosphere. A specially-designed, four turn helical inductor was used to provide optimal heating to the joint area. Initial tests were conducted with bare parts and temperature sensing paints to establish time-to-temperature and heating profiles. The BAg-24 brazing wire was shaped into preforms to fit the O.D of the straight tubing section. Black flux was also applied to both tubes. The two tube sections were then fit together with the braze preforms up against the flared tube section. After RF power was applied for 18 seconds, braze wire reached a temperature of 1330°F. The wire then melted and flowed into the joint. RF power was maintained for another two seconds to ensure that all the braze wire melted.
Conclusion
Consistent, repeatable results were achieved at 1330°F within 20 seconds. The braze wire melted and flowed evenly into the joint area.

2021年11月16日星期二
Induction Brazing Stainless Steel Tools
Induction Brazing Stainless Steel Tools With RF Heating Equipments
Research Objective
To braze three joints on a dental prophy jet assembly with induction heating; to improve yield consistency and reduce cycle time.
Parts & Materials Description
Stainless steel prophy nose piece, two tubes, tube support collar, braze alloy rings, B1 flux
Temperature Required
1400°F
Induction Heating Equipment
DW-UHF-4.5kW RF Induction Heating Power Supply, specially-designed inductor (coil)
Operating Frequency
400 kHz
Heating Procedure
Initial testing was done to establish time-to-temperature and heating profiles. It was determined that a two-stage process would deliver optimum results. For this application a specially designed four-turn, double-wound helical inductor was used to deliver even heat to the joint areas. The two tubes, tube support collar and nose piece were assembled and held in position with temporary fixturing. The braze alloy rings were placed in position and a thin coat of B1 flux was applied to the entire assembly. In the first stage of the heating process, the upper tube end of the assembly was placed in the heating zone and induction power was supplied for 10 seconds. In stage two, the assembly was reversed and the lower end of the assembly was heated for an additional 10 seconds. The assembly was then removed, bathed in hot water to remove the flux, and blown dry with hot air.
Conclusion
Consistent, repeatable results were obtained with with the DW-UHF-4.5kW power supply and 10 second heat cycles. Each braze joint was sealed with an even filet


订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.