显示标签为“Brazingcopperheater”的博文。显示所有博文

2024年3月24日星期日

Induction Brazing copper to copper pipes

High Frequency Induction Brazing copper to copper pipes Process

Objective: Induction Brazing copper to copper pipes Equipment: DW-UHF-6KW-III handheld induction brazing heater handheld inductino heater Materials:  Six Copper pipes (9.5 mm) Power: 6 kW Temperature: 1475 °F/ 800°C Time: 20 seconds
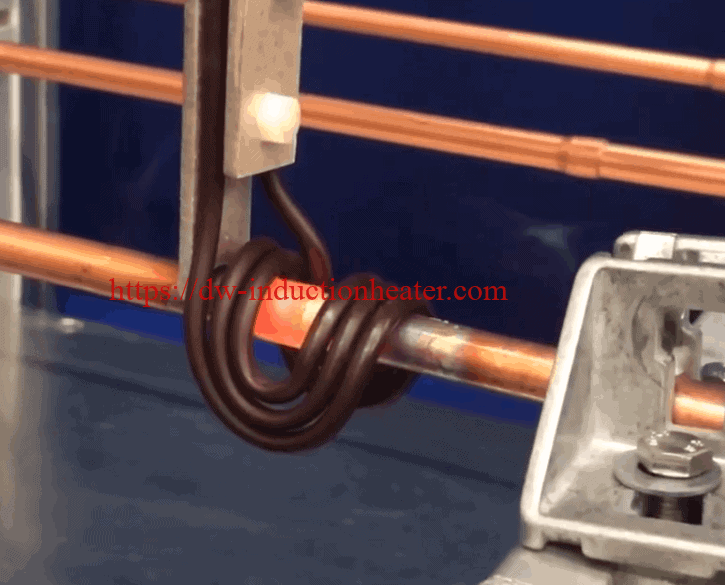
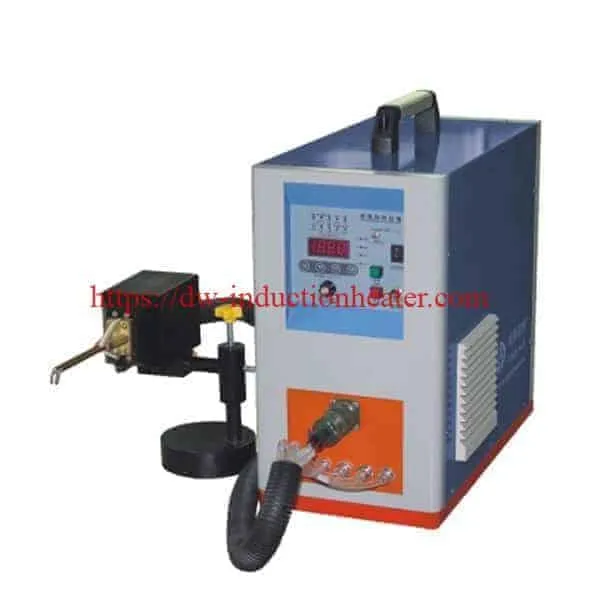
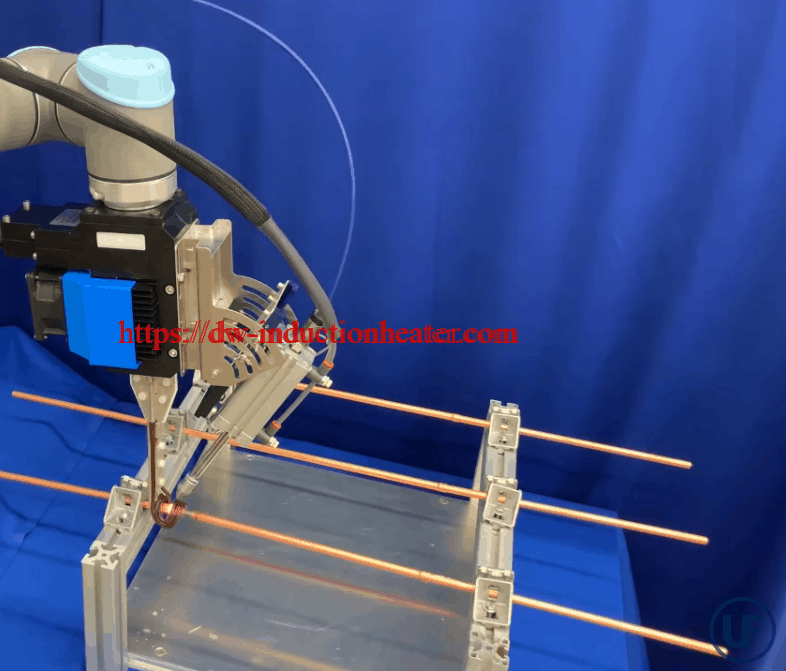
Process: The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F. The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.
https://dw-inductionheater.com/induction-brazing-copper-to-copper-pipes.html?feed_id=238262&_unique_id=6600c16a2964f

2023年11月10日星期五

Brazing Thin Copper Tube With Induction

Brazing Thin Copper Tube With Induction  Objective: To braze a thin copper oval tube to a brass fitting at 1400 º F and to cap the other end of the copper tube with a brass plate. Material: Brass fitting - 0.875 in2 and 2.5 in long (22mm2 x 64mm) Copper tube 0.01 in (0.254mm) wall Brass plate 0.10 in (2.54mm) thick and 0.5 in X 0.25 inch Braze alloy shim and white flux Temperature: 1400 ºF (760 °C) Frequency: 300 kHz Equipment: DW-UHF-10KW induction power supply equipped with a remote heat station using two 1.32μF capacitors (total 0.66 μF) Two custom-designed induction heating coils. Process A split, f our-turn induction coil is used to deliver the heat energy into the brass fitting (Fig. 1). To prevent over heating of the edges of the brass fitting and the thin copper tube, a smaller coil diameter (Fig. 2) was added to deliver heat into the brass fitting. A braze shim preform is placed at the joint area, and is then covered with white flux. The height of the coil is adjusted to deliver proportional heat to the assembly. This setting raises the temperature of the thicker brass piece and the thin copper tube at the same rate enabling a uniform flow of the braze shim preform. The other end of the copper tube is brazed successfully using a 2-turn helical coil (Fig.3.) Results/Benefits • Preservation of the copper's mechanical properties • Minimized heat migration along both ends of the tube • Reduced heat-up time (under 60 sec.) https://dw-inductionheater.com/brazing-thin-copper-tube-with-induction.html?feed_id=230526&_unique_id=654ef0bb61510

2023年11月6日星期一

Brazing Thin Copper Tube With Induction

Brazing Thin Copper Tube With Induction  Objective: To braze a thin copper oval tube to a brass fitting at 1400 º F and to cap the other end of the copper tube with a brass plate. Material: Brass fitting - 0.875 in2 and 2.5 in long (22mm2 x 64mm) Copper tube 0.01 in (0.254mm) wall Brass plate 0.10 in (2.54mm) thick and 0.5 in X 0.25 inch Braze alloy shim and white flux Temperature: 1400 ºF (760 °C) Frequency: 300 kHz Equipment: DW-UHF-10KW induction power supply equipped with a remote heat station using two 1.32μF capacitors (total 0.66 μF) Two custom-designed induction heating coils. Process A split, f our-turn induction coil is used to deliver the heat energy into the brass fitting (Fig. 1). To prevent over heating of the edges of the brass fitting and the thin copper tube, a smaller coil diameter (Fig. 2) was added to deliver heat into the brass fitting. A braze shim preform is placed at the joint area, and is then covered with white flux. The height of the coil is adjusted to deliver proportional heat to the assembly. This setting raises the temperature of the thicker brass piece and the thin copper tube at the same rate enabling a uniform flow of the braze shim preform. The other end of the copper tube is brazed successfully using a 2-turn helical coil (Fig.3.) Results/Benefits • Preservation of the copper's mechanical properties • Minimized heat migration along both ends of the tube • Reduced heat-up time (under 60 sec.)

2023年8月6日星期日

Brazing Thin Copper Tube With Induction

Brazing Thin Copper Tube With Induction  Objective: To braze a thin copper oval tube to a brass fitting at 1400 º F and to cap the other end of the copper tube with a brass plate. Material: Brass fitting - 0.875 in2 and 2.5 in long (22mm2 x 64mm) Copper tube 0.01 in (0.254mm) wall Brass plate 0.10 in (2.54mm) thick and 0.5 in X 0.25 inch Braze alloy shim and white flux Temperature: 1400 ºF (760 °C) Frequency: 300 kHz Equipment: DW-UHF-10KW induction power supply equipped with a remote heat station using two 1.32μF capacitors (total 0.66 μF) Two custom-designed induction heating coils. Process A split, f our-turn induction coil is used to deliver the heat energy into the brass fitting (Fig. 1). To prevent over heating of the edges of the brass fitting and the thin copper tube, a smaller coil diameter (Fig. 2) was added to deliver heat into the brass fitting. A braze shim preform is placed at the joint area, and is then covered with white flux. The height of the coil is adjusted to deliver proportional heat to the assembly. This setting raises the temperature of the thicker brass piece and the thin copper tube at the same rate enabling a uniform flow of the braze shim preform. The other end of the copper tube is brazed successfully using a 2-turn helical coil (Fig.3.) Results/Benefits • Preservation of the copper's mechanical properties • Minimized heat migration along both ends of the tube • Reduced heat-up time (under 60 sec.)

2023年8月1日星期二

Induction Brazing copper to copper pipes

High Frequency Induction Brazing copper to copper pipes Process

Objective: Induction Brazing copper to copper pipes Equipment: DW-UHF-6KW-III handheld induction brazing heater handheld inductino heater Materials:  Six Copper pipes (9.5 mm) Power: 6 kW Temperature: 1475 °F/ 800°C Time: 20 seconds
Process: The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F. The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.
https://dw-inductionheater.com/induction-brazing-copper-to-copper-pipes.html?feed_id=221461&_unique_id=64c9503f47546

2023年6月3日星期六

Induction Brazing copper to copper pipes

High Frequency Induction Brazing copper to copper pipes Process

Objective: Induction Brazing copper to copper pipes Equipment: DW-UHF-6KW-III handheld induction brazing heater handheld inductino heater Materials:  Six Copper pipes (9.5 mm) Power: 6 kW Temperature: 1475 °F/ 800°C Time: 20 seconds
Process: The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F. The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.

2023年2月11日星期六

Induction Brazing copper to copper pipes

High Frequency Induction Brazing copper to copper pipes Process


Objective: Induction Brazing copper to copper pipes


Equipment: DW-UHF-6KW-III handheld induction brazing heater

handheld inductino heater

Materials:  Six Copper pipes (9.5 mm)

Power: 6 kW


Temperature: 1475 °F/ 800°C

Time: 20 seconds


Process:

The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F.
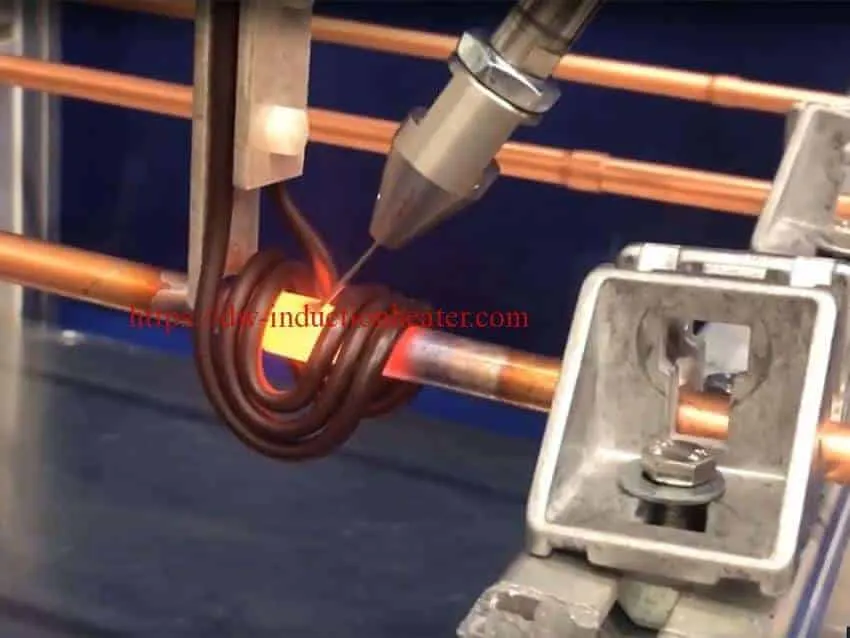
The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.


2022年11月28日星期一

Brazing Thin Copper Tube With Induction

Brazing Thin Copper Tube With Induction  Objective: To braze a thin copper oval tube to a brass fitting at 1400 º F and to cap the other end of the copper tube with a brass plate. Material: Brass fitting - 0.875 in2 and 2.5 in long (22mm2 x 64mm) Copper tube 0.01 in (0.254mm) wall Brass plate 0.10 in (2.54mm) thick and 0.5 in X 0.25 inch Braze alloy shim and white flux Temperature: 1400 ºF (760 °C) Frequency: 300 kHz Equipment: DW-UHF-10KW induction power supply equipped with a remote heat station using two 1.32μF capacitors (total 0.66 μF) Two custom-designed induction heating coils. Process A split, f our-turn induction coil is used to deliver the heat energy into the brass fitting (Fig. 1). To prevent over heating of the edges of the brass fitting and the thin copper tube, a smaller coil diameter (Fig. 2) was added to deliver heat into the brass fitting. A braze shim preform is placed at the joint area, and is then covered with white flux. The height of the coil is adjusted to deliver proportional heat to the assembly. This setting raises the temperature of the thicker brass piece and the thin copper tube at the same rate enabling a uniform flow of the braze shim preform. The other end of the copper tube is brazed successfully using a 2-turn helical coil (Fig.3.) Results/Benefits • Preservation of the copper's mechanical properties • Minimized heat migration along both ends of the tube • Reduced heat-up time (under 60 sec.)

2022年9月6日星期二

Brazing Thin Copper Tube With Induction

Brazing Thin Copper Tube With Induction  Objective: To braze a thin copper oval tube to a brass fitting at 1400 º F and to cap the other end of the copper tube with a brass plate. Material: Brass fitting - 0.875 in2 and 2.5 in long (22mm2 x 64mm) Copper tube 0.01 in (0.254mm) wall Brass plate 0.10 in (2.54mm) thick and 0.5 in X 0.25 inch Braze alloy shim and white flux Temperature: 1400 ºF (760 °C) Frequency: 300 kHz Equipment: DW-UHF-10KW induction power supply equipped with a remote heat station using two 1.32μF capacitors (total 0.66 μF) Two custom-designed induction heating coils. Process A split, f our-turn induction coil is used to deliver the heat energy into the brass fitting (Fig. 1). To prevent over heating of the edges of the brass fitting and the thin copper tube, a smaller coil diameter (Fig. 2) was added to deliver heat into the brass fitting. A braze shim preform is placed at the joint area, and is then covered with white flux. The height of the coil is adjusted to deliver proportional heat to the assembly. This setting raises the temperature of the thicker brass piece and the thin copper tube at the same rate enabling a uniform flow of the braze shim preform. The other end of the copper tube is brazed successfully using a 2-turn helical coil (Fig.3.) Results/Benefits • Preservation of the copper's mechanical properties • Minimized heat migration along both ends of the tube • Reduced heat-up time (under 60 sec.)

2022年9月4日星期日

Induction Brazing copper to copper pipes

High Frequency Induction Brazing copper to copper pipes Process

Objective: Induction Brazing copper to copper pipes Equipment: DW-UHF-6KW-III handheld induction brazing heater handheld inductino heater Materials:  Six Copper pipes (9.5 mm) Power: 6 kW Temperature: 1475 °F/ 800°C Time: 20 seconds
Process: The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F. The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.

2022年8月7日星期日

Induction Brazing copper to copper pipes

High Frequency Induction Brazing copper to copper pipes Process

Objective: Induction Brazing copper to copper pipes Equipment: DW-UHF-6KW-III handheld induction brazing heater handheld inductino heater Materials:  Six Copper pipes (9.5 mm) Power: 6 kW Temperature: 1475 °F/ 800°C Time: 20 seconds
Process: The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F. The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.

2022年8月2日星期二

Induction Brazing copper to copper pipes

High Frequency Induction Brazing copper to copper pipes Process

Objective: Induction Brazing copper to copper pipes Equipment: DW-UHF-6KW-III handheld induction brazing heater handheld inductino heater Materials:  Six Copper pipes (9.5 mm) Power: 6 kW Temperature: 1475 °F/ 800°C Time: 20 seconds
Process: The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F. The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.

2022年5月18日星期三

Brazing Thin Copper Tube With Induction

Brazing Thin Copper Tube With Induction  Objective: To braze a thin copper oval tube to a brass fitting at 1400 º F and to cap the other end of the copper tube with a brass plate. Material: Brass fitting - 0.875 in2 and 2.5 in long (22mm2 x 64mm) Copper tube 0.01 in (0.254mm) wall Brass plate 0.10 in (2.54mm) thick and 0.5 in X 0.25 inch Braze alloy shim and white flux Temperature: 1400 ºF (760 °C) Frequency: 300 kHz Equipment: DW-UHF-10KW induction power supply equipped with a remote heat station using two 1.32μF capacitors (total 0.66 μF) Two custom-designed induction heating coils. Process A split, f our-turn induction coil is used to deliver the heat energy into the brass fitting (Fig. 1). To prevent over heating of the edges of the brass fitting and the thin copper tube, a smaller coil diameter (Fig. 2) was added to deliver heat into the brass fitting. A braze shim preform is placed at the joint area, and is then covered with white flux. The height of the coil is adjusted to deliver proportional heat to the assembly. This setting raises the temperature of the thicker brass piece and the thin copper tube at the same rate enabling a uniform flow of the braze shim preform. The other end of the copper tube is brazed successfully using a 2-turn helical coil (Fig.3.) Results/Benefits • Preservation of the copper's mechanical properties • Minimized heat migration along both ends of the tube • Reduced heat-up time (under 60 sec.)

2022年5月10日星期二

Induction Brazing copper to copper pipes

High Frequency Induction Brazing copper to copper pipes Process

Objective: Induction Brazing copper to copper pipes Equipment: DW-UHF-6KW-III handheld induction brazing heater handheld inductino heater Materials:  Six Copper pipes (9.5 mm) Power: 6 kW Temperature: 1475 °F/ 800°C Time: 20 seconds
Process: The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F. The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.