显示标签为“solderingfiberopticcable”的博文。显示所有博文

2024年5月23日星期四

induction soldering fiber optic cable

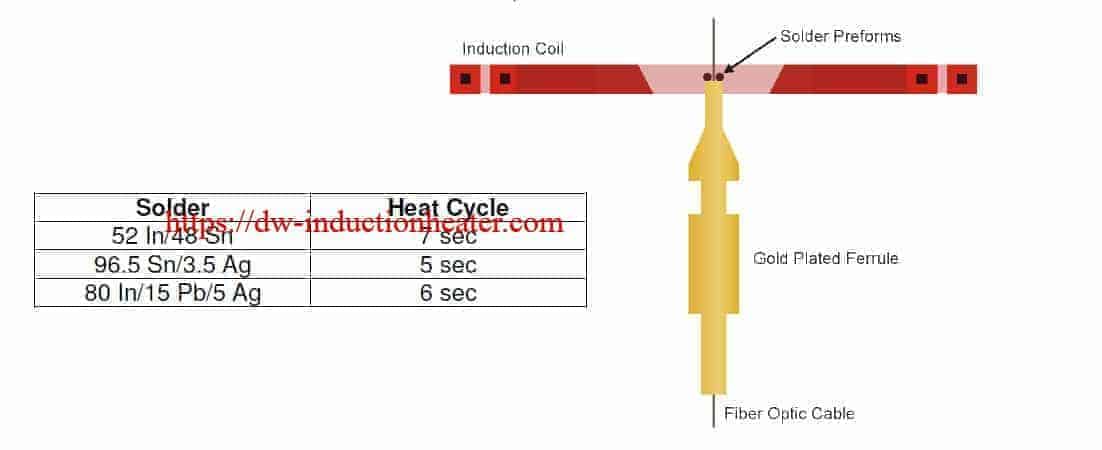
Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable https://dw-inductionheater.com/induction-soldering-fiber-optic-cable.html?feed_id=246876&_unique_id=6650053beac2d

Soldering Fiber Optic for Hermetic Sealing

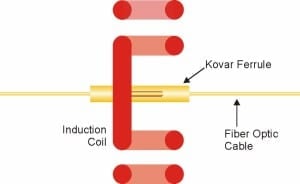
Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable https://dw-inductionheater.com/soldering-fiber-optic-for-hermetic-sealing.html?feed_id=246808&_unique_id=664f4e6a77a79
2023年10月1日星期日

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable https://dw-inductionheater.com/induction-soldering-fiber-optic-cable.html?feed_id=228221&_unique_id=651961d2ad49f

2023年9月30日星期六

Soldering Fiber Optic for Hermetic Sealing

Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable https://dw-inductionheater.com/soldering-fiber-optic-for-hermetic-sealing.html?feed_id=228191&_unique_id=6518aaeb13cef
2023年5月20日星期六

Soldering Fiber Optic for Hermetic Sealing

Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable

2023年5月16日星期二

Soldering Fiber Optic for Hermetic Sealing

Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable

2023年5月13日星期六

Soldering Fiber Optic for Hermetic Sealing

Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable

2023年4月29日星期六

Soldering Fiber Optic for Hermetic Sealing

Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable

2023年3月27日星期一

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

2023年1月2日星期一

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

2022年12月20日星期二

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

2022年11月7日星期一

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

2022年11月4日星期五

Soldering Fiber Optic for Hermetic Sealing

Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable

2022年10月21日星期五

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

2022年9月17日星期六

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

2022年9月7日星期三

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

2022年5月11日星期三

Soldering Fiber Optic for Hermetic Sealing

Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable

2022年4月11日星期一

Soldering Fiber Optic for Hermetic Sealing

Soldering Fiber Optic Cable for Hermetic Sealing With IGBT Induction Soldering Heater Objective To heat a Kovar ferrule and fiber optic cable to 297°F within 10 seconds for a soldering application, to form a hermetic seal Material Gold-coated cable, Kovar ferrule, solder and flux Temperature 297 ºF Frequency 360 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil Process A specially designed, 4-turn “C” shape coil was used to provide uniform heat to the assembly near the joint area. With this design, the coil can be lowered directly onto the joint; it is not necessary to feed the ferrule assembly through the coil. Flux was applied to the assembly where the ferrule and fiber optic cable were to be joined. RF power was applied for 10 seconds, which caused the solder to melt and flow. Results/Benefits Consistent and repeatable results were achieved with the DW-UHF-4.5kW power supply and a 10-second heat cycle. The solder flowed evenly and bonded the fiber optic cable to the Kovar ferrule. With the induction coil’s compact design, a very small surface area was heated with pinpoint accuracy. induction soldering Fiber Optic cable

2022年4月7日星期四

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

2022年3月24日星期四

induction soldering fiber optic cable

Induction soldering fiber optic cable with high frequency induction heating units Objective To heat a gold-plated ferrule and fiber optic cable to 475°F within 8 seconds for a soldering application Material Gold-plated ferrule tube, fiber optic cable, solder preform Temperature 475 ºF Frequency 270 kHz Equipment DW-UHF-4.5kW power supply with a specially designed induction coil. Process A specially designed, two-turn plate concentrator coil was used to provide uniform heat to the fiber optic assembly. The assembly was placed in a specially designed fixture, then placed inside the induction coil. RF power was applied until the solder flowed and created a solid joint. Results Consistent and repeatable results were achieved using the DW-UHF-4.5kW power supply and induction coil with a 5 to 7 second heat cycle, depending on the type of solder used (see solder chart below). Induction soldering fiber optic cable

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.