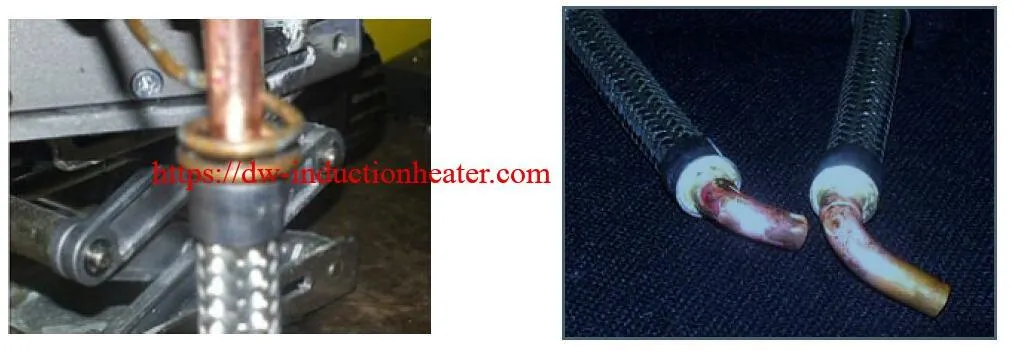
 Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
https://dw-inductionheater.com/brazing-stainless-steel-to-copper-with-induction.html?feed_id=229626&_unique_id=653984782f7fa
2023年10月25日星期三
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
https://dw-inductionheater.com/brazing-stainless-steel-to-copper-with-induction.html?feed_id=229626&_unique_id=653984782f7fa

2023年8月17日星期四
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2023年5月8日星期一
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2023年4月10日星期一
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2022年12月1日星期四
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2022年9月17日星期六
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2022年5月30日星期一
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2022年5月13日星期五
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2022年3月12日星期六
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2022年3月10日星期四
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
2022年1月23日星期日
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.