显示标签为“heatingshrinkring”的博文。显示所有博文

2024年5月6日星期一

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring   https://dw-inductionheater.com/induction-shrink-fitting-carbide-ring.html?feed_id=244576&_unique_id=66392b336b6be
2023年9月24日星期日

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring  
2023年2月19日星期日

Induction Shrink Fitting Carbide Ring

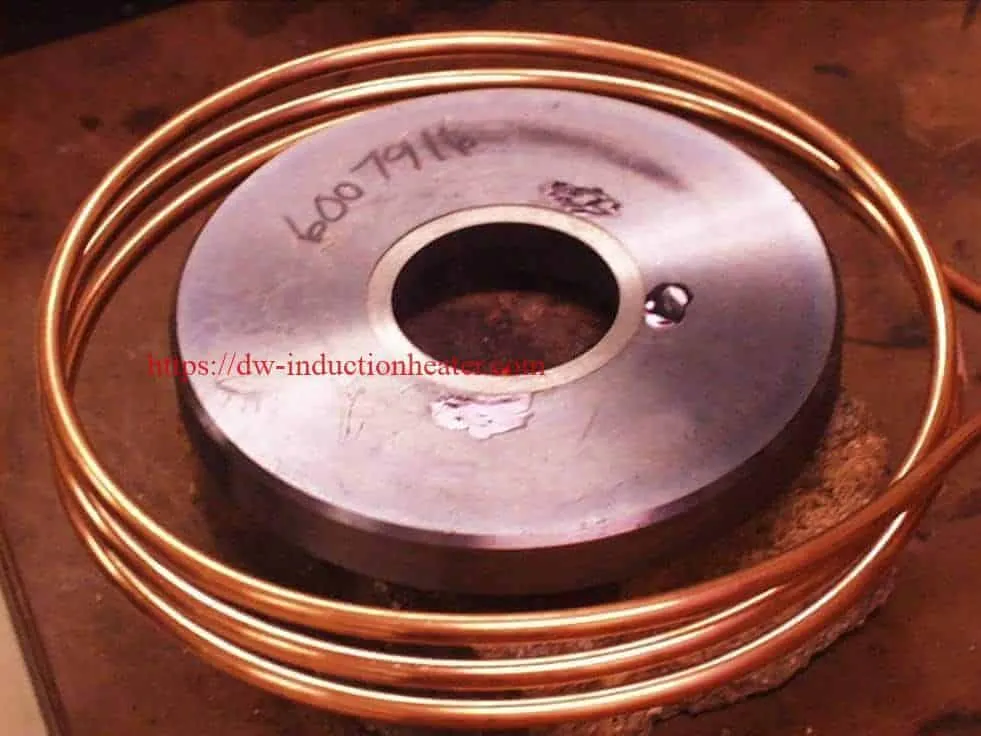
Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units

Objective Shrink fitting a carbide ring into a steel valve seat
Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring
Temperature 500 ºF ( 260 ºC)
Frequency 85 kHz
Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF
• An induction heating coil designed and developed specifically for this application.
Process A three turn helical coil is used to heat the steel valve seat.
The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in
for the shrink fitting process.
Results/Benefits Induction heating provides:
• Accurate and repeatable results
• Ease of integration into existing production lines
• Energy efficient, only heats the part, not the atmosphere around it
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating

shrink fitting carbide ring


2022年12月7日星期三

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring  

2022年8月27日星期六

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring  

2022年8月14日星期日

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring  

2022年6月4日星期六

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring  

2022年5月10日星期二

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring  

2022年1月2日星期日

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring  

2021年11月7日星期日

Induction Shrink Fitting Carbide Ring

Induction Shrink Fitting Carbide Ring With IGBT Induction Heating Units Objective Shrink fitting a carbide ring into a steel valve seat Material Steel valve seat 6” (152.4mm) OD with 3” (76.2mm) ID hole & .75” (19mm) thick, carbide ring Temperature 500 ºF ( 260 ºC) Frequency 85 kHz Equipment •DW-HF-15kW induction heating system, equipped with a remote workhead containing two 0.50 μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to heat the steel valve seat. The steel valve seat is placed in the coil and heated for 50 seconds to enlarge the center hole & drop the carbide ring in for the shrink fitting process. Results/Benefits Induction heating provides: • Accurate and repeatable results • Ease of integration into existing production lines • Energy efficient, only heats the part, not the atmosphere around it • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating shrink fitting carbide ring  

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.