显示标签为“HeatPlasticProcessingMachinery”的博文。显示所有博文

2022年3月3日星期四

Electromagnetic Induction Heater

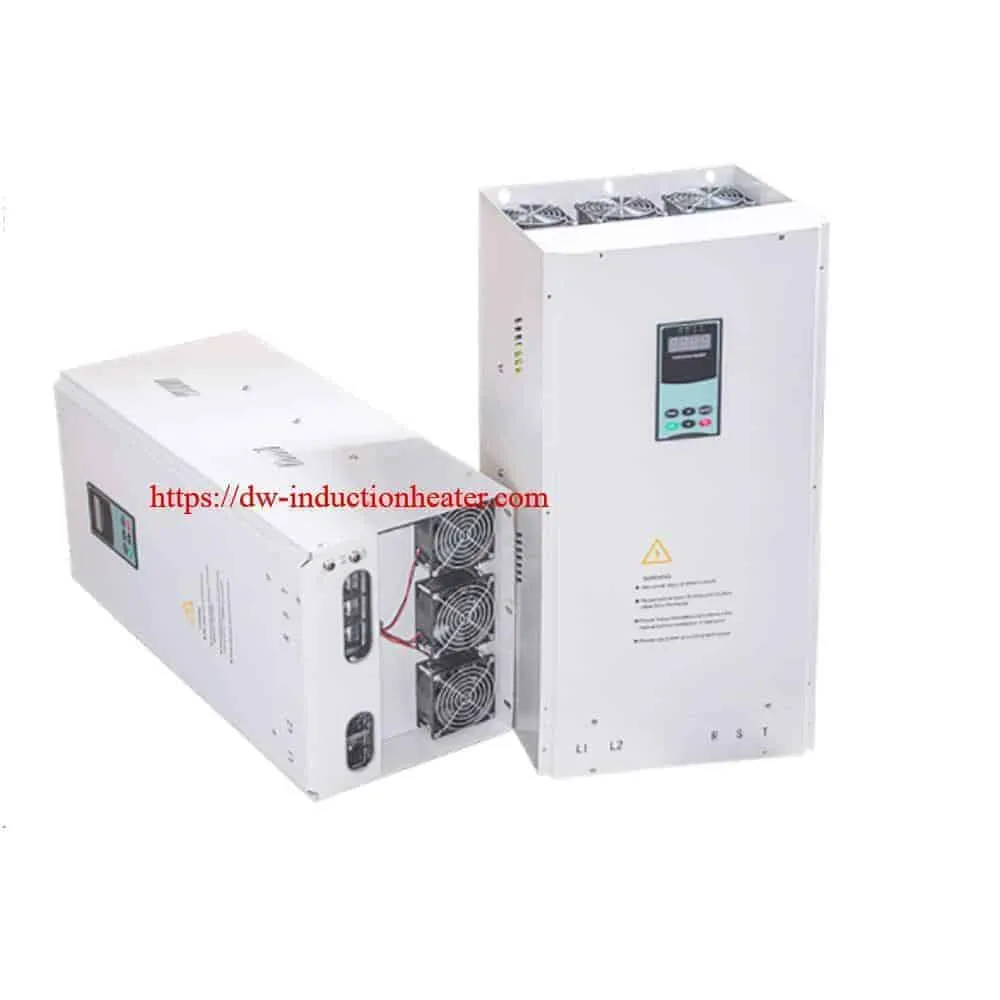
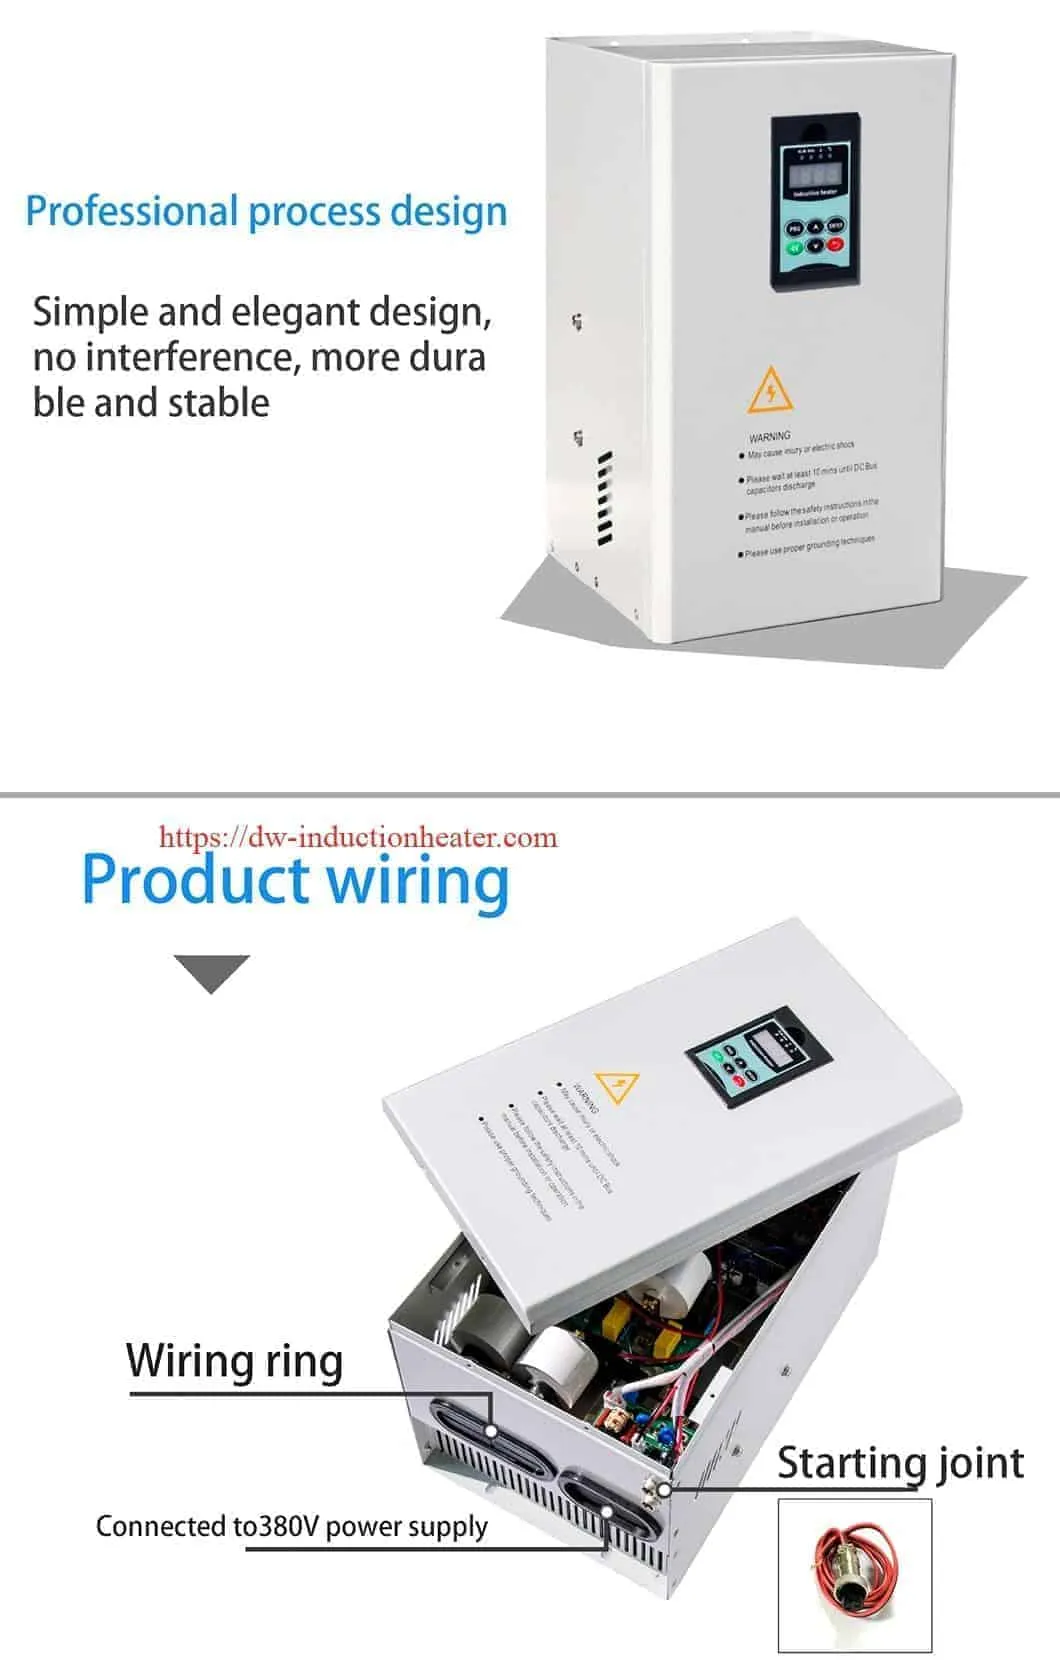
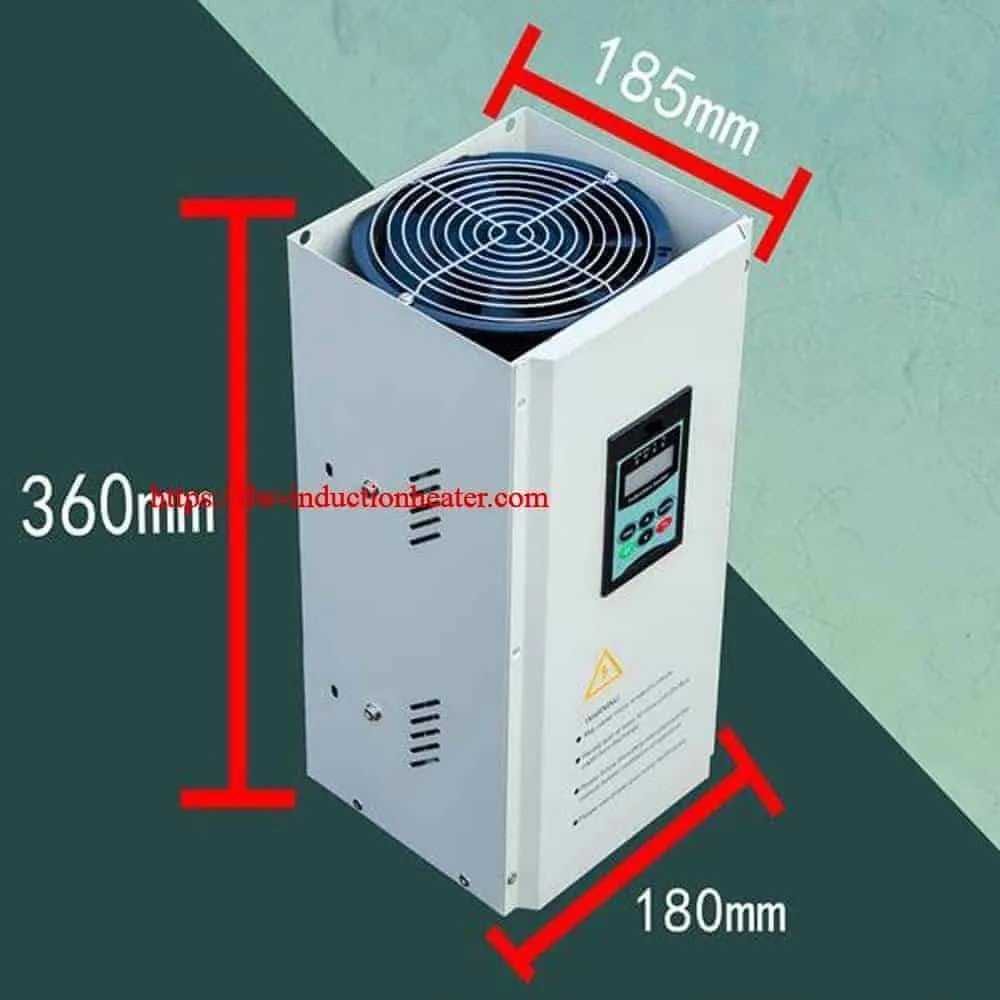
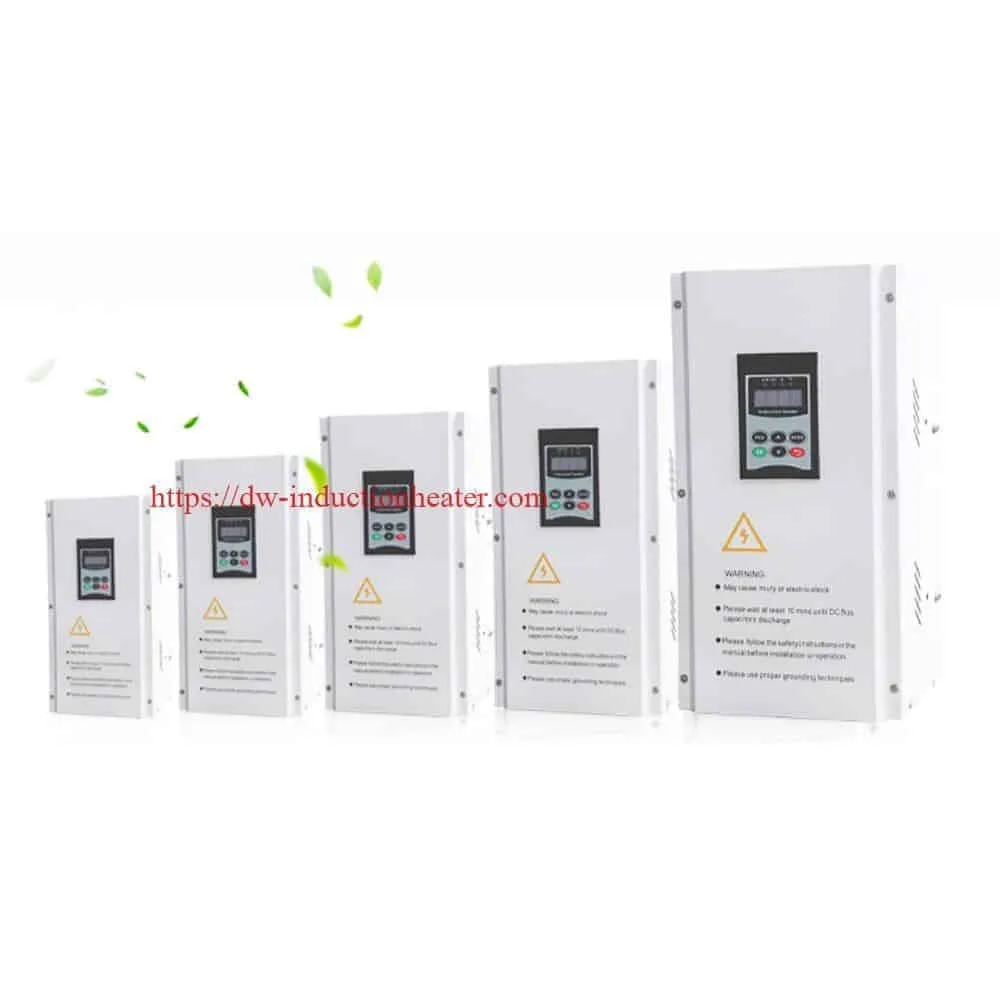
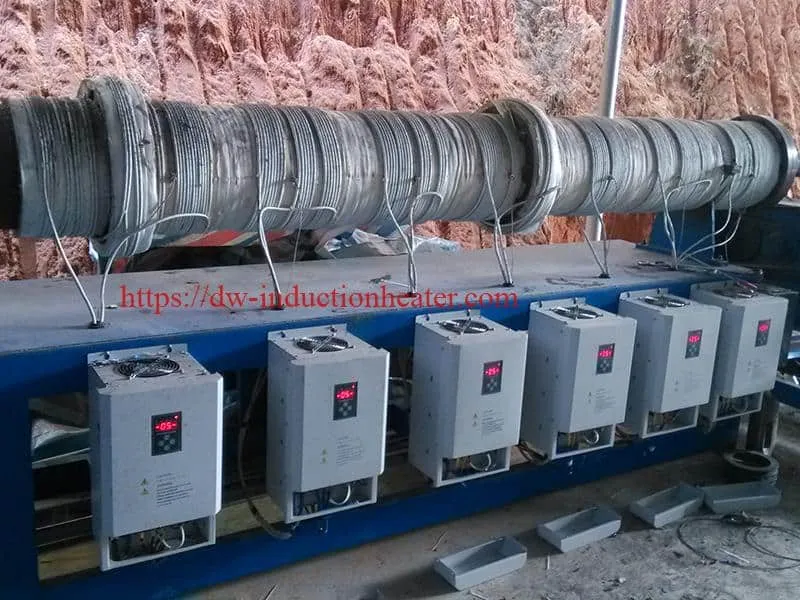
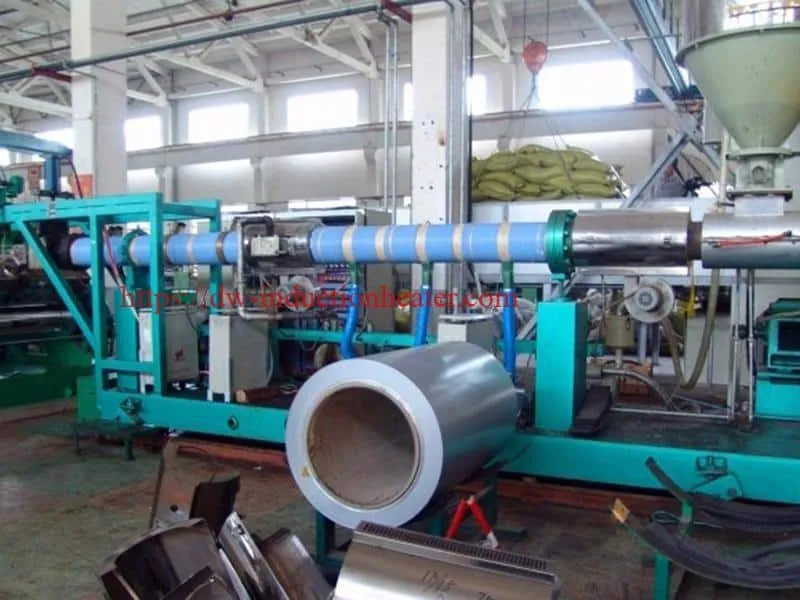
Electromagnetic Induction Heatersfor heating plastic injection molding machine

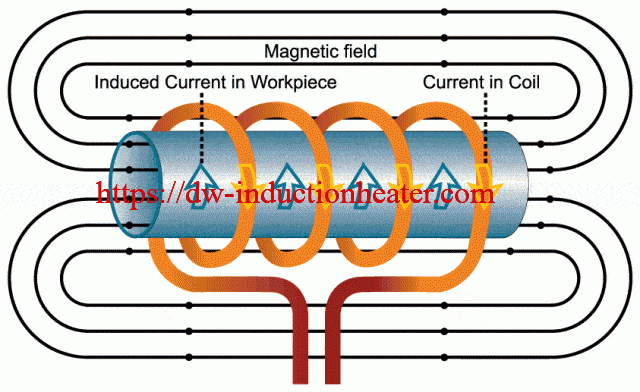
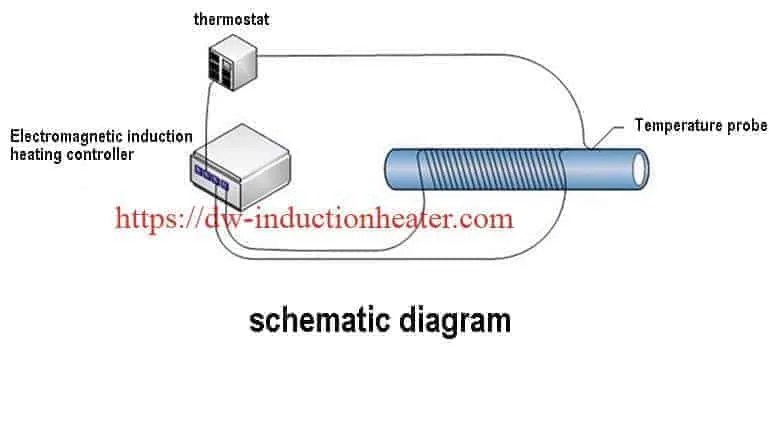
Principle of Electromagnetic Induction Heating: Most of the metal is heated by the high-frequency magnetic field and uses this principle to pass the high-frequency current through the coil, so that the coil generates a high-frequency magnetic field, so that the metal rod in the coil is induced to generate heat. The electrical energy can be converted into metal thermal energy by the above process. During the whole process, the metal rod does not have any physical contact with the coil, and the energy conversion is completed by the magnetic field eddy current and the metal induction.  Advantages of electromagnetic induction heating: 1.Energy saving and emission reduction (30-85%) 2.higher thermal efficiency 3.Reduced operating temperature 4.warm up fast 5'long service life 6.Maintenance is simple and convenient   What Advantages Does Induction Heater Have Compared With Traditional Heaters?
Advantage Comparison
Electromagnetic Induction Heater Traditional Heater
Heating Principles Electromagnetic Induction Heating the  Resdistance Wire
Heated Part Charging barrel is heated directly to get higher efficiency ,but the induction coil itself is not heated to guaratte longer using life heater itself,then heat transfered to the charging barrel
Surface Temperature & Safety Max. 60 Degree Centigrade,safe to touch by hands. The same with your heating temperature, Dangerous to touch
Heating Rate High Efficiency:save 50%-70%warming -up time Low Efficiency:No time-saving
Energy Saving Save 30-80% Power Consumption No Saving
Temperature Control High precision Low Precision
Using life 4-5year 2-3year
Working Environment Normal temperature for workers,easy and comfortable Hot,especially for low latitude Area
Cost Cost-effective,with30-80% energy-saving rate,it takes 6-10 months to recover the cost. The higher the rate is,the less time it takes. Low
 

Application of electromagnetic induction heater: 1.Plastic rubber industry: plastic film blowing machine, wire drawing machine, injection molding machine, granulator, rubber extruder, vulcanizing machine, cable production extruder, etc.; 2.Pharmaceutical and chemical industry: pharmaceutical infusion bags, plastic equipment production lines, liquid heating pipelines for the chemical industry; 3.Energy, food industry: heating of crude oil pipelines, food machinery, super freighters and other equipment that require electric heating; 4.Industrial high-power heating industry: machine for killing machine, reaction axe, steam generator (boiler); 5.Smelting heating industry: die casting furnace zinc alloy, aluminum alloy and other equipment; 6.Building materials industry: gas pipe production line, plastic pipe production line, PE plastic hard flat net, geonet net unit, automatic blow molding machine, PE honeycomb board production line, single and double wall corrugated pipe extrusion production line, composite air cushion film unit, PVC hard Tube, PP extrusion transparent sheet production line, extruded polystyrene foam tube, PE winding film unit; 7.high power commercial induction cooker movement; 8.Dry heating in printing equipment; 9.other similar industry heating; Technical Parameters
Item

Technical Parameters

Rated power 10KW,3phases, 380V (It can be customized)
Rated input current 10KW (14-15A)

Rated output current

10KW (50-60A)
Rated voltage frequency

AC 380V/50Hz

Voltage adaptation range constant power output at 300 ~ 400V
Adapt to ambient temperature -20ºC~50ºC
Adapt to environmental humidity ≤95%
Power adjustment range 20% ~ 100% stepless adjustment(That is: adjustment between 0.5 ~ 10KW)
Heat conversion efficiency ≥95%
Effective power

≥98%(Can be customized according to user needs)

working frequency

5~40KHz

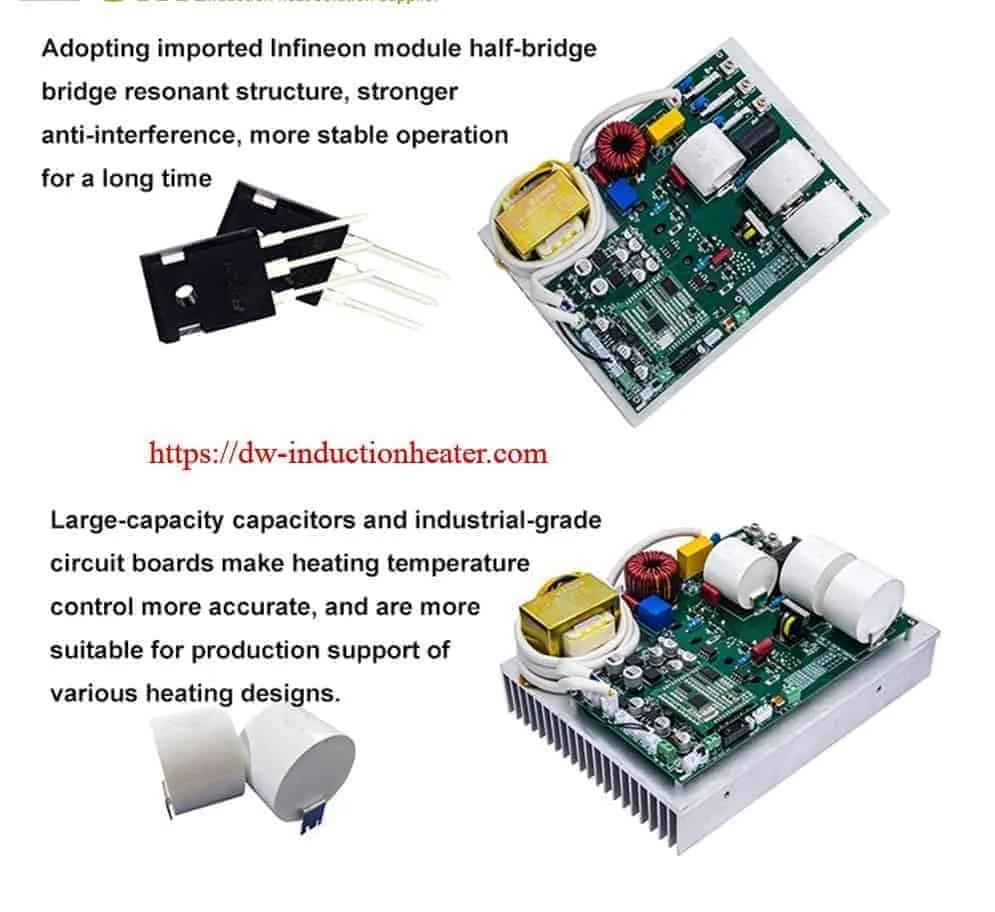
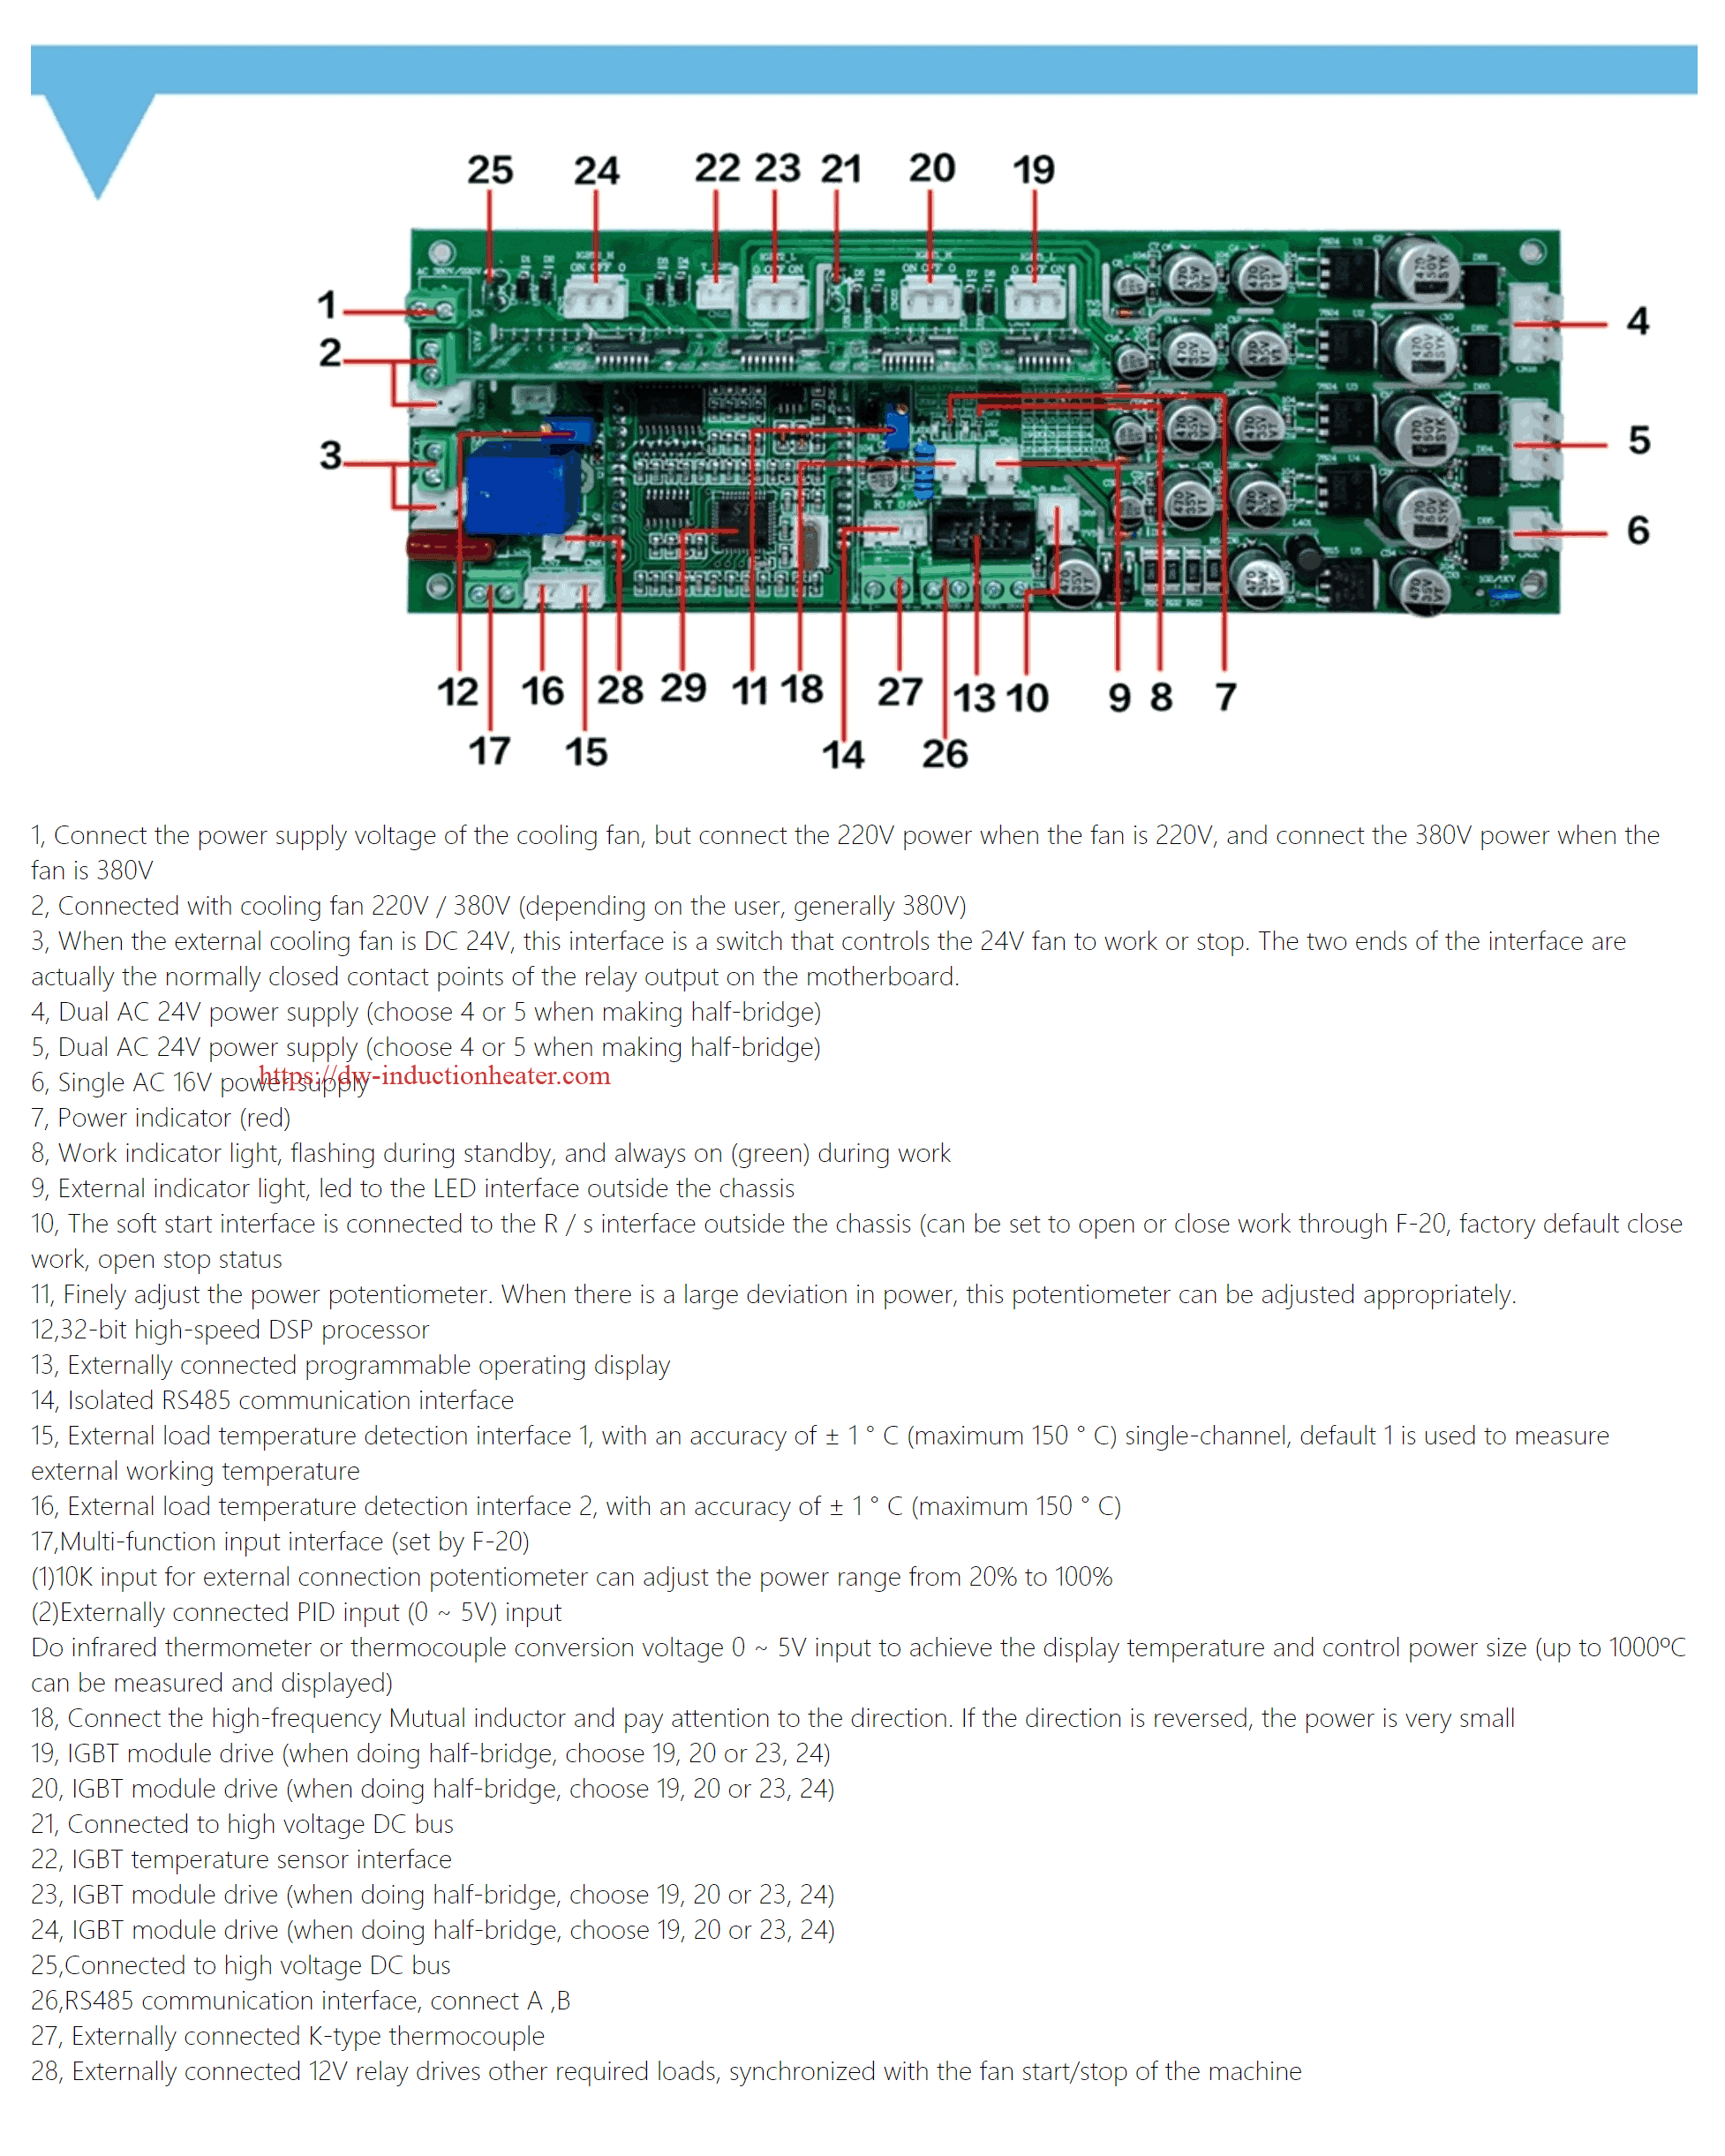
Main circuit structure Half-bridge series resonance
Control System DSP-based high-speed automatic phase-locking tracking control system
Application mode Open application platform
monitor Programmable digital display
start time <1S
Instantaneous overcurrent protection time ≤2US
Power overload protection 130% instantaneous protection
Soft start mode Fully electrically isolated soft start heating / stop mode
Support PID adjustment power Identify 0-5V input voltage
Support 0 ~ 150 ºC load temperature detection Accuracy up to ± 1 ºC
Adaptive coil parameters 10KW  10 square line, length 30~35m, inductance 150 ~ 180uH
Coil to load distance(Thermal insulation thickness) 20-25mm for circle, 15-20mm for plane, 10-15mm for ellipse and within 10 mm for super ellipse
Parameters
Model No. Input Voltage Rated Power Inductance Current Coil Wire
DW-2.5K220A AC220V 2.5KW 100uH 11A 4mm2
DW-3.5K220A AC220V 3.5KW 90uH 15A 4mm2
DW-5K220D AC220V 5KW 160uH 22.5A 6mm2
DW-6K220D AC220V 6KW 150uH 27A 6mm2
DW-8K220D AC220V 8KW 140uH 36A 10mm2
DW-10K220D AC220V 10KW 130uH 45A 10mm2
DW-3.5K380D AC380V 3.5KW 250uH 5A 4mm2
DW-5K380D AC380V 5KW 230uH 7.5A 6mm2
DW-8K380D AC380V 8KW 170uH 12A 6mm2
DW-10K380D AC380V 10KW 150uH 15A 10mm2
DW-12K380D AC380V 12KW 130uH 18A 10mm2
DW-15K380D AC380V 15KW 125uH 22.5A 16mm2
DW-20K380D AC380V 20KW 100uH 30A 20mm2
DW-25K380D AC380V 25KW 90uH 37.5A 25mm2
DW-30K380D AC380V 30KW 200uH 45A 16mm2
DW-40K380D AC380V 40KW 180uH 60A 20mm2
DW-50K380D AC380V 50KW 160uH 75A 25mm2
DW-60K380D AC380V 60KW 150uH 90A 30mm2
DW-80K380D AC380V 80KW 120uH 120A 50mm2

Electromagnetic Induction Heater

Electromagnetic Induction Heatersfor heating plastic injection molding machine

Principle of Electromagnetic Induction Heating: Most of the metal is heated by the high-frequency magnetic field and uses this principle to pass the high-frequency current through the coil, so that the coil generates a high-frequency magnetic field, so that the metal rod in the coil is induced to generate heat. The electrical energy can be converted into metal thermal energy by the above process. During the whole process, the metal rod does not have any physical contact with the coil, and the energy conversion is completed by the magnetic field eddy current and the metal induction.  Advantages of electromagnetic induction heating: 1.Energy saving and emission reduction (30-85%) 2.higher thermal efficiency 3.Reduced operating temperature 4.warm up fast 5'long service life 6.Maintenance is simple and convenient   What Advantages Does Induction Heater Have Compared With Traditional Heaters?
Advantage Comparison
Electromagnetic Induction Heater Traditional Heater
Heating Principles Electromagnetic Induction Heating the  Resdistance Wire
Heated Part Charging barrel is heated directly to get higher efficiency ,but the induction coil itself is not heated to guaratte longer using life heater itself,then heat transfered to the charging barrel
Surface Temperature & Safety Max. 60 Degree Centigrade,safe to touch by hands. The same with your heating temperature, Dangerous to touch
Heating Rate High Efficiency:save 50%-70%warming -up time Low Efficiency:No time-saving
Energy Saving Save 30-80% Power Consumption No Saving
Temperature Control High precision Low Precision
Using life 4-5year 2-3year
Working Environment Normal temperature for workers,easy and comfortable Hot,especially for low latitude Area
Cost Cost-effective,with30-80% energy-saving rate,it takes 6-10 months to recover the cost. The higher the rate is,the less time it takes. Low
 

Application of electromagnetic induction heater: 1.Plastic rubber industry: plastic film blowing machine, wire drawing machine, injection molding machine, granulator, rubber extruder, vulcanizing machine, cable production extruder, etc.; 2.Pharmaceutical and chemical industry: pharmaceutical infusion bags, plastic equipment production lines, liquid heating pipelines for the chemical industry; 3.Energy, food industry: heating of crude oil pipelines, food machinery, super freighters and other equipment that require electric heating; 4.Industrial high-power heating industry: machine for killing machine, reaction axe, steam generator (boiler); 5.Smelting heating industry: die casting furnace zinc alloy, aluminum alloy and other equipment; 6.Building materials industry: gas pipe production line, plastic pipe production line, PE plastic hard flat net, geonet net unit, automatic blow molding machine, PE honeycomb board production line, single and double wall corrugated pipe extrusion production line, composite air cushion film unit, PVC hard Tube, PP extrusion transparent sheet production line, extruded polystyrene foam tube, PE winding film unit; 7.high power commercial induction cooker movement; 8.Dry heating in printing equipment; 9.other similar industry heating; Technical Parameters
Item

Technical Parameters

Rated power 10KW,3phases, 380V (It can be customized)
Rated input current 10KW (14-15A)

Rated output current

10KW (50-60A)
Rated voltage frequency

AC 380V/50Hz

Voltage adaptation range constant power output at 300 ~ 400V
Adapt to ambient temperature -20ºC~50ºC
Adapt to environmental humidity ≤95%
Power adjustment range 20% ~ 100% stepless adjustment(That is: adjustment between 0.5 ~ 10KW)
Heat conversion efficiency ≥95%
Effective power

≥98%(Can be customized according to user needs)

working frequency

5~40KHz

Main circuit structure Half-bridge series resonance
Control System DSP-based high-speed automatic phase-locking tracking control system
Application mode Open application platform
monitor Programmable digital display
start time <1S
Instantaneous overcurrent protection time ≤2US
Power overload protection 130% instantaneous protection
Soft start mode Fully electrically isolated soft start heating / stop mode
Support PID adjustment power Identify 0-5V input voltage
Support 0 ~ 150 ºC load temperature detection Accuracy up to ± 1 ºC
Adaptive coil parameters 10KW  10 square line, length 30~35m, inductance 150 ~ 180uH
Coil to load distance(Thermal insulation thickness) 20-25mm for circle, 15-20mm for plane, 10-15mm for ellipse and within 10 mm for super ellipse
Parameters
Model No. Input Voltage Rated Power Inductance Current Coil Wire
DW-2.5K220A AC220V 2.5KW 100uH 11A 4mm2
DW-3.5K220A AC220V 3.5KW 90uH 15A 4mm2
DW-5K220D AC220V 5KW 160uH 22.5A 6mm2
DW-6K220D AC220V 6KW 150uH 27A 6mm2
DW-8K220D AC220V 8KW 140uH 36A 10mm2
DW-10K220D AC220V 10KW 130uH 45A 10mm2
DW-3.5K380D AC380V 3.5KW 250uH 5A 4mm2
DW-5K380D AC380V 5KW 230uH 7.5A 6mm2
DW-8K380D AC380V 8KW 170uH 12A 6mm2
DW-10K380D AC380V 10KW 150uH 15A 10mm2
DW-12K380D AC380V 12KW 130uH 18A 10mm2
DW-15K380D AC380V 15KW 125uH 22.5A 16mm2
DW-20K380D AC380V 20KW 100uH 30A 20mm2
DW-25K380D AC380V 25KW 90uH 37.5A 25mm2
DW-30K380D AC380V 30KW 200uH 45A 16mm2
DW-40K380D AC380V 40KW 180uH 60A 20mm2
DW-50K380D AC380V 50KW 160uH 75A 25mm2
DW-60K380D AC380V 60KW 150uH 90A 30mm2
DW-80K380D AC380V 80KW 120uH 120A 50mm2
https://dw-inductionheater.com/electromagnetic-induction-heater?feed_id=99280&_unique_id=62207bdf43271

2022年2月28日星期一

Induction Heating Barrel for Plastic Extruder and Injection Molding Machine

Induction heating barrel offers greater energy savings, reliability, and faster response.

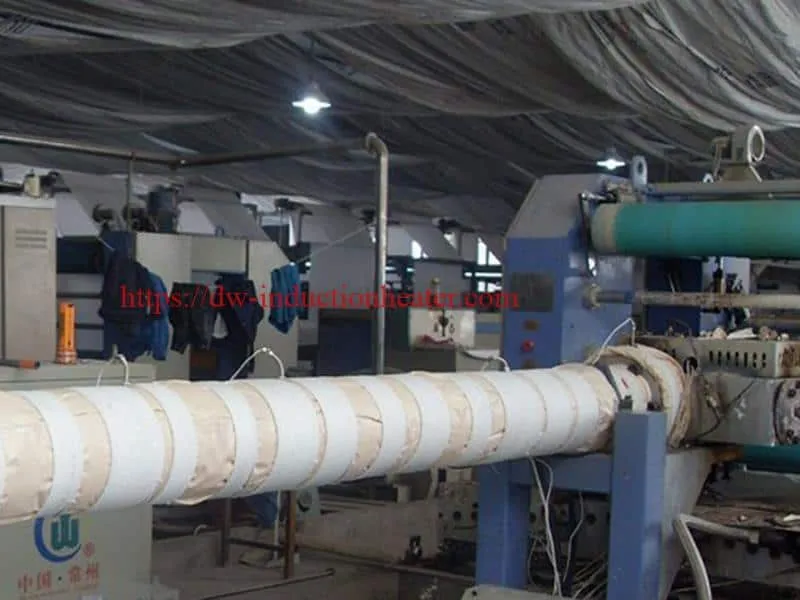
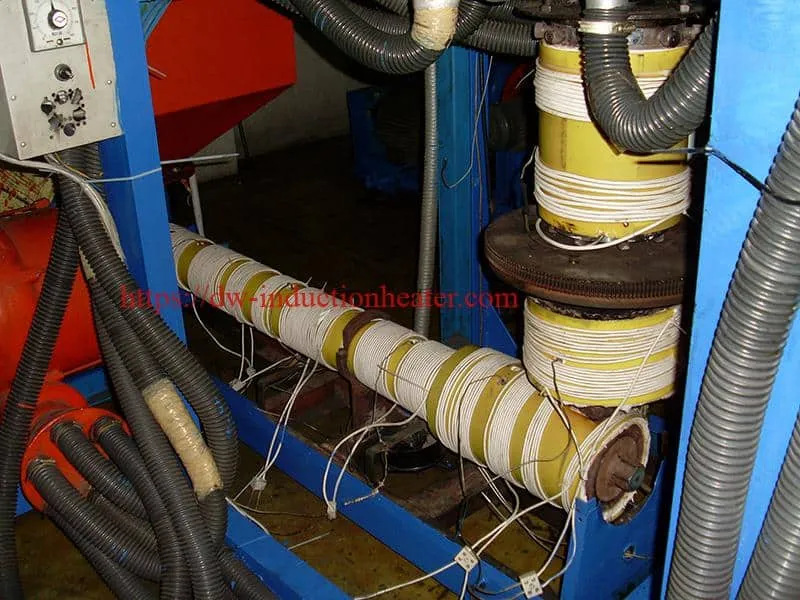
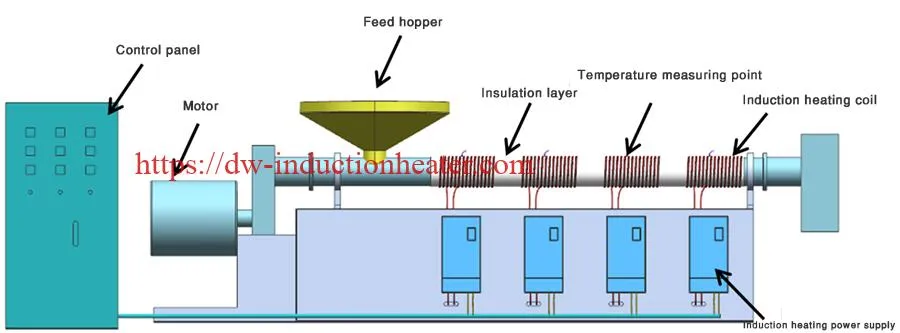
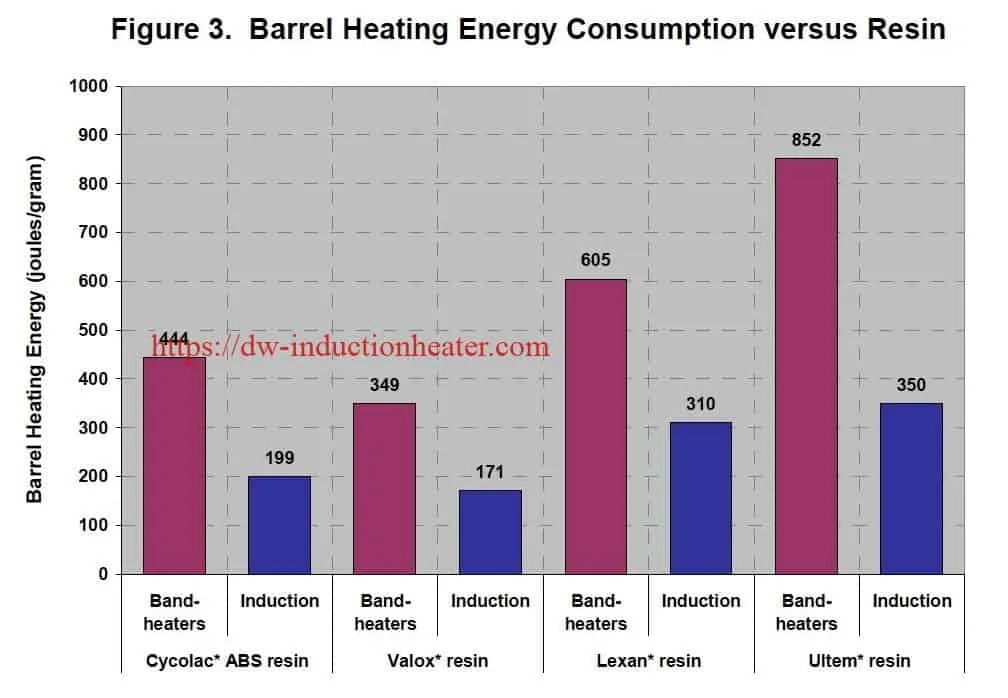
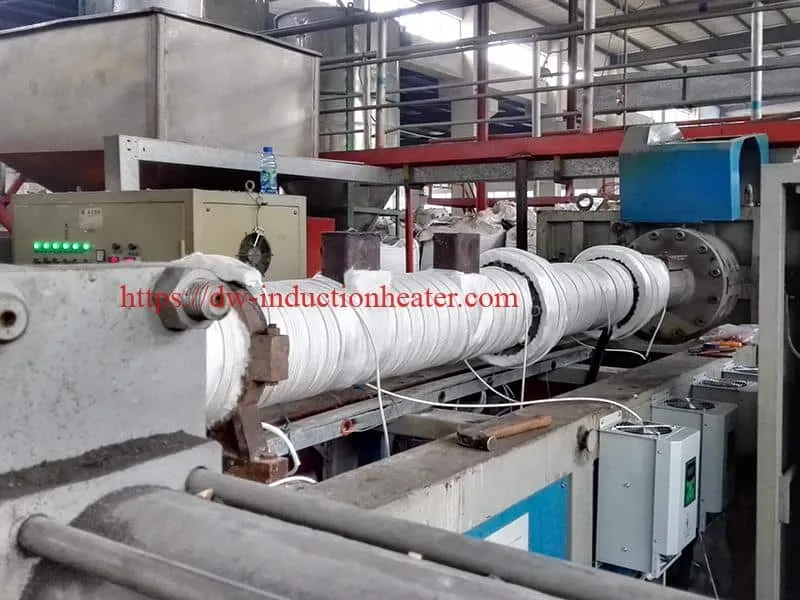
Spectacular energy savings, superior reliability and much faster response than conventional heater bands are some of the advantages offered by a newly developed induction heating system. The heating system uses electromagnetic induction - an old and well-known principle used to heat large industrial furnaces, special machines for injection moulding molten metal, thermoset molds, and some Japanese hot-runner nozzles. However, it is a relatively new concept for heating barrels of plastics extrusion and injection molding machines. The electromagnetic induction heating system, introduced by HLQ induction equipment Co from China turns the steel barrel itself into a resistance heater by generating electrical eddy currents in the metal near the outer surface of the barrel tube. Those eddy currents are induced by electrical current passing through a cable wrapped in a continuous coil around the barrel but not touching it. Although the initial cost is more than heater bands, induction heating reportedly pays for itself in several ways, and also at a faster pace, depending on machine size. Laboratory measurements indicate that the heating efficiency (relative to energy consumed) of typical mica band heaters at 200-300 degree C processing range (common in injection moulding) is likely to be only 40-60%, while that of a ceramic band heater may be 10-15% higher. The remaining energy is wasted by radiation and convection to the surrounding environment. What's more, a new mica band loses about 10% of its initial efficiency after the first 6 hours of use because it darkens, raising its surface emissivity and consequent radiation losses. At higher barrel temperatures for engineering resins, efficiency drops even more. In contrast, HLQ measures induction heating efficiency at about 95%. Radiation losses are minimized by the insulating sleeves, which rise to a temperature of around 60-70 degree C during operation. The low-resistance induction coils remain cool enough to touch.

Where can induction heating barrel?

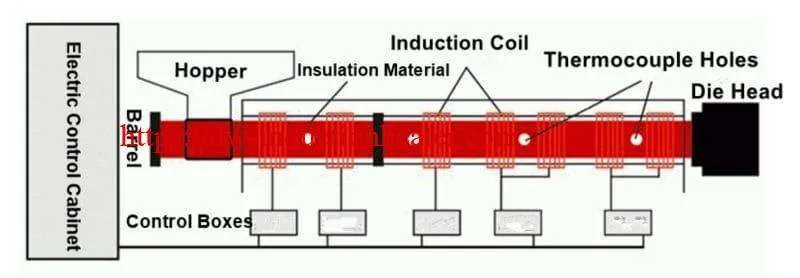
It is mainly applied to injection, extrusion; blow filming, wire drawing, granulating and recycling machines, etc. The product application includes film, sheet, profile, raw material etc. It can be used for heating the barrel, flange, die head, screw and other parts of the machines. It is excellent in energy-saving and cooling down work environment. Induction heating is the process of heating an electrically conducting object (usually a metal) by electromagnetic induction, where eddy currents are generated within the metal and resistance leads to Joule heating of the metal. The induction coil itself does not get heated. The heat generating object is the heated object itself.

Why and how induction heating barrel can save energy?

Presently,most of the plastic machines are using the conventional resistance heating method, where the resistance wire is heated up and then transfer the heat to the barrel via heater cover.So only the heat close to the barrel surface can be transferred to the barrel and the heat close to outside heater cover is lost to the air which causes a rise in environment temperature. Induction heater is technology where high frequency magnetic fields which cause he be heated up bu electro-magnetic field(EMF)that are brushing against each other.When the barrel is heated up and heat is minimum,there is very high heat efficiency and minimum heat loss to the environment where energy saving could reach30-80%.Due to the fact that the induction coil is not producing any high heat and also there is no resistance wire that gets oxidized and causes the heater to burn out, the induction heater has a longer service life and also less maintenance.

What are the advantages of induction heating barrel?

  • Energy efficiency 30%-85% Currently, plastic processing machinery mainly uses resistance heating elements which can produce a large amount of heat radiated to the surroundings. Induction heating is an ideal alternative to solve this issue. The surface temperature of induction heating coil ranges between 50ºC and 90ºC, the heat losses are significantly minimized, providing energy savings of 30%-85%. The energy saving effect is therefore more obvious when the induction heating system is used in high power heating equipment.
  • Safety Using induction heating system enables the surface of the machine to be safe for touching, and that means it can avoid burn injuries which often occur in plastic machines that use resistance heating elements, providing a safe workplace for operators.
  • Fast heating, high heating efficiency Compared to resistance heating whose energy conversion efficiency is approximately at 60%, the induction heating is over 98% efficient at converting electricity to heat.
  • Lower workplace temperature, higher operation comfort After using induction heating system, the temperature of entire production workshop is lowered by more than 5 degrees.
  • Long service life In contrast to resistance heating elements that have to long-lasting work at high temperature, the induction heating works at near ambient temperature, therefore efficiently prolonging the service life.
  • Accurate temperature control, high product qualification rate The induction heating provides low or no thermal inertia, so that it will not cause the temperature overshoot. And the temperature can remain at set value of 0.5 degree difference.

What is the superiority of induction heating barrel for plastic extrusion compared with traditional heaters?

Induction heater Traditional heaters
Heating method Induction heating is the process of heating an electrically conducting object (usually a metal) by electromagnetic induction, where eddy currents are generated within the metal and resistance leads to Joule heating of the metal. The induction coil itself does not get heated. The heat generating object is the heated object itself Resistance wires get heated directly and heat is transferred by contact.
 heating up time Quicker heating-up, higher efficiency slower heating-up, lower efficiency
 Energy saving rate

 Save 30-80% energy rate,reduce working temperature

Cannot save energy
 Installation  Easy to install Easy to install
 Operation  Easy to operate Easy to operate
 Maintenance

Control box is easy to replace  without turning off your machine

Easy to replace but have to turning off your machine

Temperature  Control Small thermal inertia and precise temperature control because the heater doesn’t get heated byitself. Big thermal inertia, low accuracy in temperature control
 Product Quality  Higher product quality because of precise temperature control Lower product quality
 Safety

 Outer sheath is safe to touch, lower surface temperature, no electric leakage.

 Temperature on outer sheath is much higher, easy to get burned. Electric leakage under wrong operation.
Service life of heater 2-4years 1-2 years
Service life of Barrel and Screw

Longer usage life for barrel, screw etc. due to lower frequency of changing heaters.

Shorter usage life for barrel, screw etc.

 Environment Lower environment temperature; No noise Much higher environment temperature and much noise

Induction Heating Power Calculation

In the case of knowing the heating power of existing heating system, selecting an appropriate power according to load rate

  • Load rate ≤ 60%, applicable power is 80% of the original power;
  • Load rate between 60%-80%, select the original power;
  • Load rate > 80%, applicable power is 120% of the original power;

When the heating power of existing heating system is unknown

  • For injection molding machine, blown film machine and extrusion machine, the power should be calculated as 3W per cm2 according to the actual surface area of the cylinder (barrel);
  • For dry cut pelletizing machine, the power should be calculated as 4W per cm2 according to the actual surface area of the cylinder (barrel);
  • For wet cut pelletizing machine, the power should be calculated as 8W per cm2 according to the actual surface area of the cylinder (barrel);
For example: cylinder diameter 160mm, length 1000mm (i.e. 160mm=16cm, 1000mm=100cm) Cylinder surface area calculation: 16*3.14*100=5024cm² Calculating as 3W per cm2: 5024*3=15072W, i.e. 15kW

Induction Heating Barrel for Plastic Extruder and Injection Molding Machine

Induction heating barrel offers greater energy savings, reliability, and faster response.

Spectacular energy savings, superior reliability and much faster response than conventional heater bands are some of the advantages offered by a newly developed induction heating system. The heating system uses electromagnetic induction - an old and well-known principle used to heat large industrial furnaces, special machines for injection moulding molten metal, thermoset molds, and some Japanese hot-runner nozzles. However, it is a relatively new concept for heating barrels of plastics extrusion and injection molding machines. The electromagnetic induction heating system, introduced by HLQ induction equipment Co from China turns the steel barrel itself into a resistance heater by generating electrical eddy currents in the metal near the outer surface of the barrel tube. Those eddy currents are induced by electrical current passing through a cable wrapped in a continuous coil around the barrel but not touching it. Although the initial cost is more than heater bands, induction heating reportedly pays for itself in several ways, and also at a faster pace, depending on machine size. Laboratory measurements indicate that the heating efficiency (relative to energy consumed) of typical mica band heaters at 200-300 degree C processing range (common in injection moulding) is likely to be only 40-60%, while that of a ceramic band heater may be 10-15% higher. The remaining energy is wasted by radiation and convection to the surrounding environment. What's more, a new mica band loses about 10% of its initial efficiency after the first 6 hours of use because it darkens, raising its surface emissivity and consequent radiation losses. At higher barrel temperatures for engineering resins, efficiency drops even more. In contrast, HLQ measures induction heating efficiency at about 95%. Radiation losses are minimized by the insulating sleeves, which rise to a temperature of around 60-70 degree C during operation. The low-resistance induction coils remain cool enough to touch.

Where can induction heating barrel?

It is mainly applied to injection, extrusion; blow filming, wire drawing, granulating and recycling machines, etc. The product application includes film, sheet, profile, raw material etc. It can be used for heating the barrel, flange, die head, screw and other parts of the machines. It is excellent in energy-saving and cooling down work environment. Induction heating is the process of heating an electrically conducting object (usually a metal) by electromagnetic induction, where eddy currents are generated within the metal and resistance leads to Joule heating of the metal. The induction coil itself does not get heated. The heat generating object is the heated object itself.

Why and how induction heating barrel can save energy?

Presently,most of the plastic machines are using the conventional resistance heating method, where the resistance wire is heated up and then transfer the heat to the barrel via heater cover.So only the heat close to the barrel surface can be transferred to the barrel and the heat close to outside heater cover is lost to the air which causes a rise in environment temperature. Induction heater is technology where high frequency magnetic fields which cause he be heated up bu electro-magnetic field(EMF)that are brushing against each other.When the barrel is heated up and heat is minimum,there is very high heat efficiency and minimum heat loss to the environment where energy saving could reach30-80%.Due to the fact that the induction coil is not producing any high heat and also there is no resistance wire that gets oxidized and causes the heater to burn out, the induction heater has a longer service life and also less maintenance.

What are the advantages of induction heating barrel?

  • Energy efficiency 30%-85% Currently, plastic processing machinery mainly uses resistance heating elements which can produce a large amount of heat radiated to the surroundings. Induction heating is an ideal alternative to solve this issue. The surface temperature of induction heating coil ranges between 50ºC and 90ºC, the heat losses are significantly minimized, providing energy savings of 30%-85%. The energy saving effect is therefore more obvious when the induction heating system is used in high power heating equipment.
  • Safety Using induction heating system enables the surface of the machine to be safe for touching, and that means it can avoid burn injuries which often occur in plastic machines that use resistance heating elements, providing a safe workplace for operators.
  • Fast heating, high heating efficiency Compared to resistance heating whose energy conversion efficiency is approximately at 60%, the induction heating is over 98% efficient at converting electricity to heat.
  • Lower workplace temperature, higher operation comfort After using induction heating system, the temperature of entire production workshop is lowered by more than 5 degrees.
  • Long service life In contrast to resistance heating elements that have to long-lasting work at high temperature, the induction heating works at near ambient temperature, therefore efficiently prolonging the service life.
  • Accurate temperature control, high product qualification rate The induction heating provides low or no thermal inertia, so that it will not cause the temperature overshoot. And the temperature can remain at set value of 0.5 degree difference.

What is the superiority of induction heating barrel for plastic extrusion compared with traditional heaters?

Induction heater Traditional heaters
Heating method Induction heating is the process of heating an electrically conducting object (usually a metal) by electromagnetic induction, where eddy currents are generated within the metal and resistance leads to Joule heating of the metal. The induction coil itself does not get heated. The heat generating object is the heated object itself Resistance wires get heated directly and heat is transferred by contact.
 heating up time Quicker heating-up, higher efficiency slower heating-up, lower efficiency
 Energy saving rate

 Save 30-80% energy rate,reduce working temperature

Cannot save energy
 Installation  Easy to install Easy to install
 Operation  Easy to operate Easy to operate
 Maintenance

Control box is easy to replace  without turning off your machine

Easy to replace but have to turning off your machine

Temperature  Control Small thermal inertia and precise temperature control because the heater doesn’t get heated byitself. Big thermal inertia, low accuracy in temperature control
 Product Quality  Higher product quality because of precise temperature control Lower product quality
 Safety

 Outer sheath is safe to touch, lower surface temperature, no electric leakage.

 Temperature on outer sheath is much higher, easy to get burned. Electric leakage under wrong operation.
Service life of heater 2-4years 1-2 years
Service life of Barrel and Screw

Longer usage life for barrel, screw etc. due to lower frequency of changing heaters.

Shorter usage life for barrel, screw etc.

 Environment Lower environment temperature; No noise Much higher environment temperature and much noise

Induction Heating Power Calculation

In the case of knowing the heating power of existing heating system, selecting an appropriate power according to load rate

  • Load rate ≤ 60%, applicable power is 80% of the original power;
  • Load rate between 60%-80%, select the original power;
  • Load rate > 80%, applicable power is 120% of the original power;

When the heating power of existing heating system is unknown

  • For injection molding machine, blown film machine and extrusion machine, the power should be calculated as 3W per cm2 according to the actual surface area of the cylinder (barrel);
  • For dry cut pelletizing machine, the power should be calculated as 4W per cm2 according to the actual surface area of the cylinder (barrel);
  • For wet cut pelletizing machine, the power should be calculated as 8W per cm2 according to the actual surface area of the cylinder (barrel);
For example: cylinder diameter 160mm, length 1000mm (i.e. 160mm=16cm, 1000mm=100cm) Cylinder surface area calculation: 16*3.14*100=5024cm² Calculating as 3W per cm2: 5024*3=15072W, i.e. 15kW

https://dw-inductionheater.com/induction-heating-barrel-for-plastic-extruder-and-injection-molding-machine?feed_id=98237&_unique_id=621cbd8bd661e

2022年2月27日星期日

induction heating plastic granulator

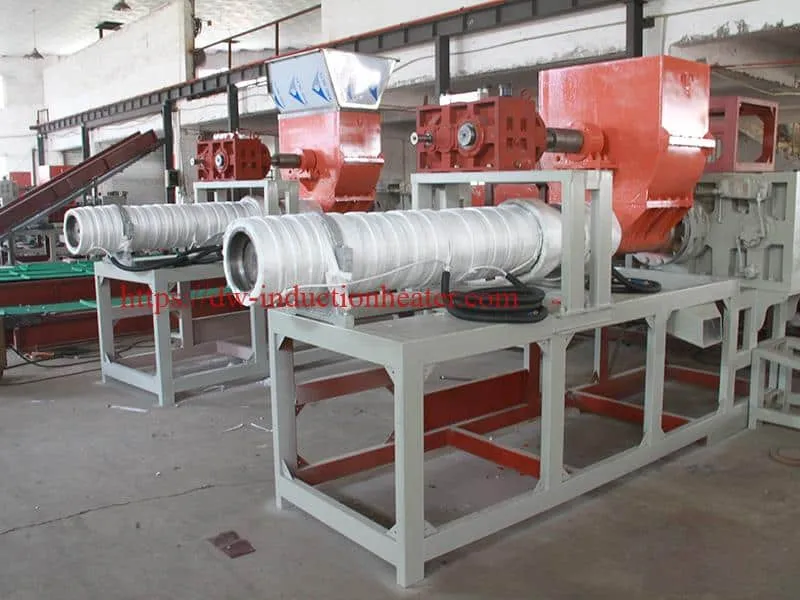
Brief Introduction of induction heating plastic granulator/plastic extrusion:

Induction heating plastic granulator/plastic extrusion is a one type of energy-saving heater. It has many advantages including significant energy-saving, fast heating up, high energy efficiency, low or zero maintenance etc. It can also lower environment temperature by generating much less heat. While installing the induction heater system, there will not involve any major changes to the electrical control system.

Where can induction heating plastic granulator/plastic extrusion?

It is mainly applied to injection, extrusion; blow filming, wire drawing, granulating and recycling machines, etc. The product application includes film, sheet, profile, raw material etc. It can be used for heating the barrel, flange, die head, screw and other parts of the machines. It is excellent in energy-saving and cooling down work environment. Induction heating is the process of heating an electrically conducting object (usually a metal) by electromagnetic induction, where eddy currents are generated within the metal and resistance leads to Joule heating of the metal. The induction coil itself does not get heated. The heat generating object is the heated object itself.

Why and how induction heating plastic granulator/plastic extrusion can save energy?

Presently,most of the plastic machines are using the conventional resistance heating method, where the resistance wire is heated up and then transfer the heat to the barrel via heater cover.So only the heat close to the barrel surface can be transferred to the barrel and the heat close to outside heater cover is lost to the air which causes a rise in environment temperature. Induction heater is technology where high frequency magnetic fields which cause he be heated up bu electro-magnetic field(EMF)that are brushing against each other.When the barrel is heated up and heat is minimum,there is very high heat efficiency and minimum heat loss to the environment where energy saving could reach30-80%.Due to the fact that the induction coil is not producing any high heat and also there is no resistance wire that gets oxidized and causes the heater to burn out, the induction heater has a longer service life and also less maintenance.

What are the advantages of induction heating plastic granulator/plastic extrusion?

  • Energy efficiency 30%-85% Currently, plastic processing machinery mainly uses resistance heating elements which can produce a large amount of heat radiated to the surroundings. Induction heating is an ideal alternative to solve this issue. The surface temperature of induction heating coil ranges between 50ºC and 90ºC, the heat losses are significantly minimized, providing energy savings of 30%-85%. The energy saving effect is therefore more obvious when the induction heating system is used in high power heating equipment.
  • Safety Using induction heating system enables the surface of the machine to be safe for touching, and that means it can avoid burn injuries which often occur in plastic machines that use resistance heating elements, providing a safe workplace for operators.
  • Fast heating, high heating efficiency Compared to resistance heating whose energy conversion efficiency is approximately at 60%, the induction heating is over 98% efficient at converting electricity to heat.
  • Lower workplace temperature, higher operation comfort After using induction heating system, the temperature of entire production workshop is lowered by more than 5 degrees.
  • Long service life In contrast to resistance heating elements that have to long-lasting work at high temperature, the induction heating works at near ambient temperature, therefore efficiently prolonging the service life.
  • Accurate temperature control, high product qualification rate The induction heating provides low or no thermal inertia, so that it will not cause the temperature overshoot. And the temperature can remain at set value of 0.5 degree difference.

What is the superiority of induction heating plastic granulator/plastic extrusion compared with traditional heaters?

Induction heater Traditional heaters
Heating method Induction heating is the process of heating an electrically conducting object (usually a metal) by electromagnetic induction, where eddy currents are generated within the metal and resistance leads to Joule heating of the metal. The induction coil itself does not get heated. The heat generating object is the heated object itself Resistance wires get heated directly and heat is transferred by contact.
 heating up time Quicker heating-up, higher efficiency slower heating-up, lower efficiency
 Energy saving rate

 Save 30-80% energy rate,reduce working temperature

Cannot save energy
 Installation  Easy to install Easy to install
 Operation  Easy to operate Easy to operate
 Maintenance

Control box is easy to replace  without turning off your machine

Easy to replace but have to turning off your machine

Temperature  Control Small thermal inertia and precise temperature control because the heater doesn’t get heated byitself. Big thermal inertia, low accuracy in temperature control
 Product Quality  Higher product quality because of precise temperature control Lower product quality
 Safety

 Outer sheath is safe to touch, lower surface temperature, no electric leakage.

 Temperature on outer sheath is much higher, easy to get burned. Electric leakage under wrong operation.
Service life of heater 2-4years 1-2 years
Service life of Barrel and Screw

Longer usage life for barrel, screw etc. due to lower frequency of changing heaters.

Shorter usage life for barrel, screw etc.

 Environment Lower environment temperature; No noise Much higher environment temperature and much noise

Induction Heating Power Calculation

In the case of knowing the heating power of existing heating system, selecting an appropriate power according to load rate

  • Load rate ≤ 60%, applicable power is 80% of the original power;
  • Load rate between 60%-80%, select the original power;
  • Load rate > 80%, applicable power is 120% of the original power;

When the heating power of existing heating system is unknown

  • For injection molding machine, blown film machine and extrusion machine, the power should be calculated as 3W per cm2 according to the actual surface area of the cylinder (barrel);
  • For dry cut pelletizing machine, the power should be calculated as 4W per cm2 according to the actual surface area of the cylinder (barrel);
  • For wet cut pelletizing machine, the power should be calculated as 8W per cm2 according to the actual surface area of the cylinder (barrel);
For example: cylinder diameter 160mm, length 1000mm (i.e. 160mm=16cm, 1000mm=100cm) Cylinder surface area calculation: 16*3.14*100=5024cm² Calculating as 3W per cm2: 5024*3=15072W, i.e. 15kW

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.